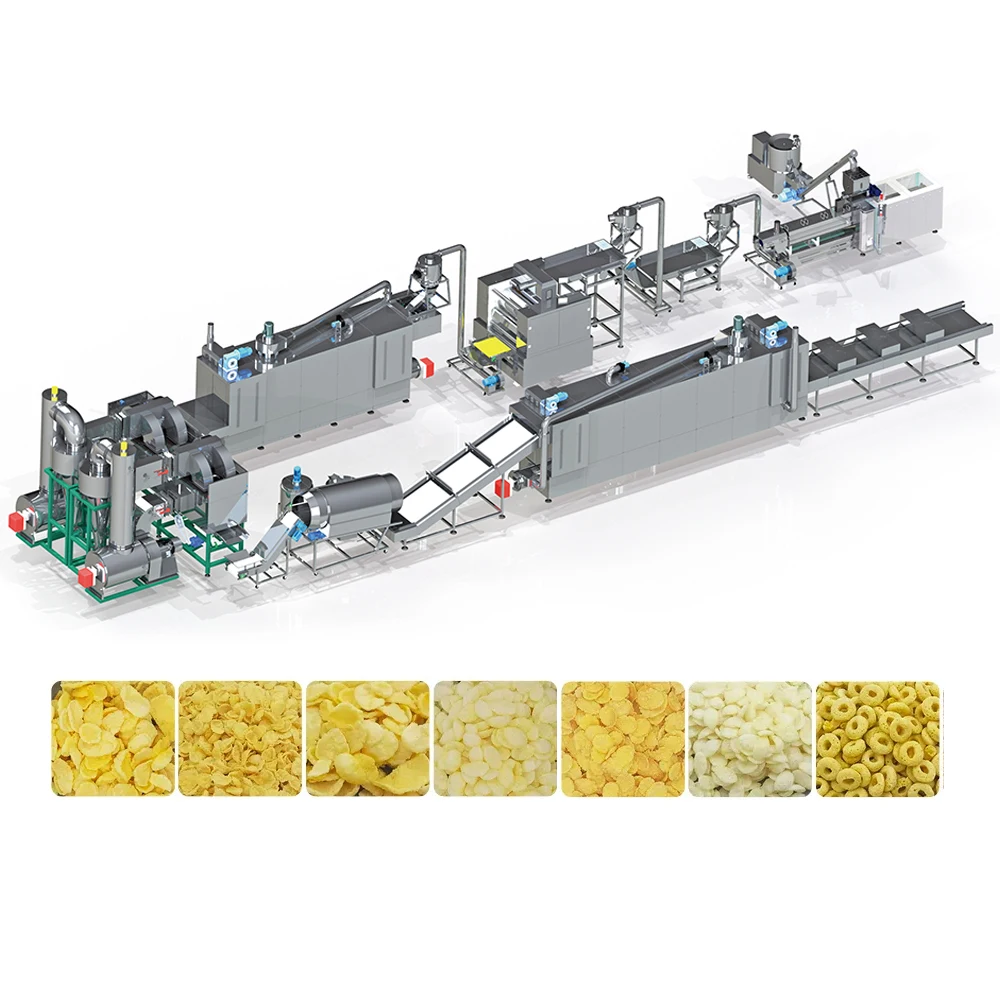
Precision screw configuration and die design — every barrel zone and roller gap tuned to your specific corn blend and target flake density before the line leaves our Jinan workshop.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Extruder Type | Twin Screw |
| Control System | PLC |
| Installed Power (MT70 / MT85 / MT75) | 160 kW / 190 kW / 210 kW |
| Power Consumption (MT70 / MT85 / MT75) | 120 kW / 140 kW / 150 kW |
| Output Capacity (MT70 / MT85 / MT75) | 150–200 kg/h / 300–400 kg/h / 300–500 kg/h (basis not stated in source) |
| Overall Dimensions (MT70 / MT85 / MT75) | 41 × 1.5 × 2.2 m / 43 × 1.5 × 3.2 m / 45 × 1.5 × 3.5 m |
| Flaking Machine | Hydraulic system, double rollers, double motors for separate driving |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air, vibrating pan, high-temperature spraying tubes, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Basic Materials | Corn, rice, wheat, oat, barley powder |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour blends |
| Sugar-coated breakfast cereals | Corn, rice, and oat mixtures with sugar syrup coating |
| Multi-shape cereal formats | Rings, balls, tubes, stars, wheels via interchangeable dies |
| Fortified breakfast cereals | Grain powders blended with vitamin and mineral premixes |
| Variety grain flake production | Wheat, barley, and oat-based raw formulations |
Why Barrel Temperature Profile Matters More Than Nominal Capacity on a Corn Flakes Extrusion Line
A corn flakes extrusion production line turnkey is only as reliable as the starch gelatinisation it achieves at your actual moisture level.
I have stood beside a flaking roller watching corn grits come out of the extruder under-gelatinised because the barrel zones were set for a different grain blend. The flakes cracked during roasting instead of blistering, and the entire batch was written off. Buyers often focus on the headline capacity number, but what determines whether your corn flakes extrusion production line turnkey delivers sellable product is the match between screw configuration, barrel temperature profile, and the raw material you actually feed into the hopper [NEED_CITE: starch gelatinisation temperature ranges for corn, rice, and wheat blends]. When that match is wrong, no amount of downstream adjustment compensates.
Screw Configuration and Starch Gelatinisation Control
The twin-screw extruder at the heart of this corn flakes extrusion production line turnkey uses modular screw elements arranged in a sequence that controls shear intensity and residence time. Corn grits require a different screw profile from oat or barley blends because each grain gelatinises at a different temperature and moisture threshold. The PLC system monitors barrel zone temperatures across multiple heating sections, allowing operators to adjust the thermal profile without stopping production.
Hydraulic Flaking and the Density Question
After extrusion, the cooked grain mass passes through the hydraulic flaking machine where double rollers driven by separate motors compress the material into thin flakes. The hydraulic system maintains consistent pressure across the roller gap, which directly determines flake thickness and final density. Inconsistent flake thickness causes uneven roasting — thick flakes remain doughy inside while thin ones scorch. The double-motor drive prevents roller slip that would otherwise introduce thickness variation across the belt width [NEED_CITE: hydraulic flaking pressure influence on cereal flake bowl life].
Reading the Spec Sheet Against Your Actual Production Conditions
The installed power across the three models ranges from 160 kW to 210 kW, with operating consumption proportionally lower. These figures matter because extrusion of corn-based cereals demands sustained thermal and mechanical energy input; an undersized motor will struggle to maintain screw speed under load, causing output density to drift. The roasting oven uses hot air circulation combined with a vibrating pan and high-temperature spraying tubes to produce the characteristic surface blisters on each flake. Cyclone dust removal captures fine particulate before it accumulates in the oven chamber, maintaining consistent heat transfer throughout long production runs. The coating system — double tumble for sugar melting, elevator, coating drum, and spraying nozzle — must be throughput-matched to the extruder and flaker so that flakes do not queue and cool before receiving their sugar layer.
What Happens When Extruder and Flaker Capacity Are Mismatched
I have seen lines where the extruder was specified correctly but the flaking rollers could not keep pace, creating a backlog of extruded dough that cooled and hardened before reaching the roller gap. The result was flakes that shattered during roasting and produced excessive fines in the packing station. A corn flakes extrusion production line turnkey only performs when every station — mixing, extruding, flaking, roasting, coating, cooling — is calculated against the same throughput basis [NEED_CITE: throughput matching principles in cereal processing lines]. When one vendor supplies the extruder and another supplies the flaker, that calculation often never happens.
Why Procurement Verification Starts Before the Machine Ships
Every line configuration we build is tested against the buyer’s actual raw material in our in-house testing workshop before shipment. The trial run verifies flake expansion, density, and crispness against your market specification, and the screw and die configuration record is documented for your specific grain blend. We provide a line layout and capacity calculation showing how each station relates to the others, along with electrical schematics that confirm voltage and frequency for your facility before production begins. The CE and ISO certifications are supported by complete documentation packages including factory test records and operation manuals.
Documentation & Verification
- Trial run report on your corn or grain blend verifying flake density and crispness before dispatch
- Screw and die configuration record matched to your raw material formulation
- Line layout drawing with throughput calculation across every station from mixer to packer
- Electrical schematic with voltage and frequency confirmed for your local grid standard
- Operation and maintenance manual with wear parts list for screws, dies, and roller surfaces
Installation, Commissioning & Support
- Foundation layout provided for the 41–45 m line footprint depending on model selected
- Dedicated electrical circuit sized to the 160–210 kW installed power requirement of your model
- Barrel zone temperature calibration and screw speed verification during on-site commissioning
- Hydraulic flaking roller pressure setting and gap alignment training for your operators
- PLC interface language and alarm configuration matched to your production team
- Wear parts supply schedule for screw elements, die plates, and flaking roller surfaces
What We Need to Configure Your Line
To build a proposal that matches your production reality, share your grain formulation and moisture content, the flake density and crispness specification your market requires, and the daily output target you need to sustain. Include your facility voltage and frequency standard, available floor space and ceiling height, and whether you plan to run natural flakes, sugar-coated flakes, or both on the same corn flakes extrusion production line turnkey.
Frequently Asked Questions
Q: How do you verify extruder capacity on my specific grain blend and moisture level?
A: We run your actual raw material through the extruder in our testing workshop and document output rate, flake expansion, and density against your target specification. The trial run report accompanies the shipment so you have a verified baseline before installation begins.
Q: How is screw configuration matched to natural versus sugar-coated corn flakes?
A: Natural flakes require a denser extrudate with lower expansion to maintain structural integrity through roasting. Sugar-coated flakes need a slightly more porous structure so the syrup penetrates evenly. We adjust screw element sequence and die geometry for each product target.
Q: What barrel temperature profile produces correct starch gelatinisation for crispy flakes?
A: Corn-based blends typically require a graduated temperature rise across barrel zones to achieve full gelatinisation without premature expansion. The PLC system allows zone-by-zone adjustment, and the correct profile is established during the trial run on your specific formulation and moisture level.
Q: How do you ensure downstream equipment matches extruder output?
A: We calculate throughput for the flaker, dryer, roasting oven, and coating drum against the same capacity basis as the extruder. The line layout document shows each station’s rated throughput so no single machine creates a bottleneck during continuous production.
Q: Can I run a trial on my raw material before the line ships?
A: Yes. Our in-house testing workshop is equipped for trial runs on customer-supplied raw materials. We verify flake expansion, density, crispness, and coating adhesion, and we document all process parameters so your team has a validated starting point at commissioning.