
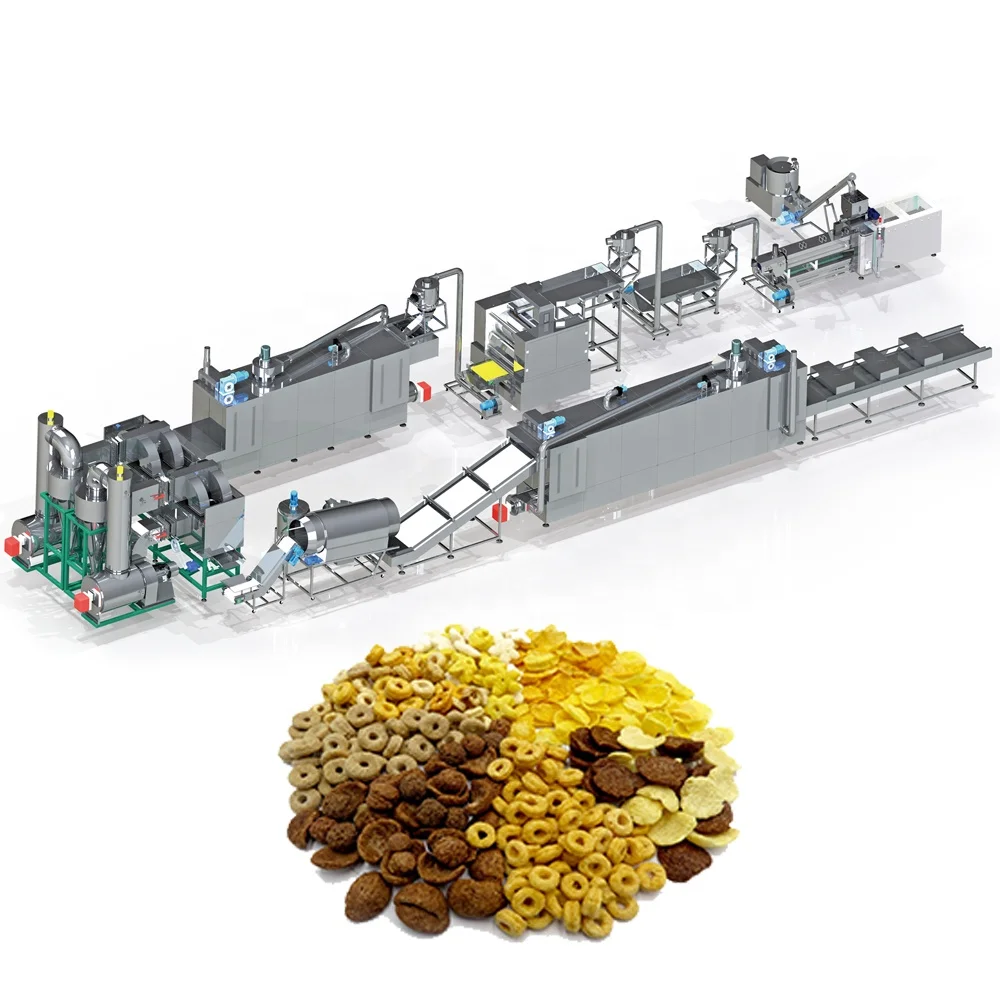
Matched screw geometry — Every MT-65, MT-70, MT-75, and MT-85 extruder is configured with sectional screw modules and die profiles matched to the buyer’s specific flour blend, moisture content, and target flake density before production begins.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Model Range | MT-65 / MT-70 / MT-75 / MT-85 |
| Screw Type | Twin-screw, co-rotating, sectional modules |
| Installed Power | MT-65: 84 kW; MT-70: 132 kW; MT-75: 186 kW; MT-85: 239 kW |
| Real Power Consumption | MT-65: 59 kW; MT-70: 92 kW; MT-75: 140 kW; MT-85: 167 kW |
| Output Capacity | MT-65: 120–150 kg/h (basis not stated in source); MT-70: 200–250 kg/h (basis not stated in source); MT-75: 300–400 kg/h (basis not stated in source); MT-85: 400–500 kg/h (basis not stated in source) |
| Line Sequence | Mixer → Screw Conveyor → Twin-Screw Extruder → Corn Flakes Press → High-Temperature Oven → Sugar Spraying System |
| Mixer Specification | 4 kW, φ600×500 mm tank, 1000×800×1200 mm |
| Extruder Dimensions | MT-65: 12000×1200×2200 mm; MT-70: 23000×1500×2200 mm; MT-75: 24000×1500×2800 mm; MT-85: 28000×1500×2800 mm |
| Flakes Press Machine | 16.12 kW, adjustable roller gap, integrated cooling, 510×310×1050 mm roller |
| High-Temperature Oven | 3.75 kW, gas-fired, both-side baking, 4.5×1.4×1.8 m |
| Sugar Spraying System | 28.75 kW, 4000×1900×1880 mm, approx. φ600×2700 mm roller |
| Self-Cleaning Function | Yes, via twin-screw design |
| Gear Box Lubrication | Oil forced automatic lubrication system |
| Contact Materials | Food-grade stainless steel |
| Control System | Separate controller box (PLC/MCC to be confirmed) |
| Voltage & Frequency | To be confirmed per installation site |
| Warranty | 1 year complete warranty + lifetime maintenance |
| Standards | CE certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional Corn Flakes | Corn grits, corn flour with sugar and malt syrup coating |
| Fortified Breakfast Cereals | Blends of corn, rice, wheat, and oat flour with vitamin premix |
| Sugar-Coated Cereal Variants | Plain extruded flakes passed through sugar spraying and drying stages |
| Mixed Grain Flakes | Rice flour, wheat flour, and soya bean blends adapted via screw profile |
| Core-Filled Snack Cereals | Corn and rice base with chocolate, peanut, or fruit paste filling |
Why "Nominal Capacity" Can Mislead on a Corn Flakes Extrusion Line
A corn flakes extrusion production line specifications sheet means little if the capacity figure was derived from standard corn flour rather than the buyer’s actual raw material.
I once configured a line based on trial runs using standard corn flour, only for the buyer to switch to degerminated corn grits after delivery. The starch gelatinisation behaviour changed entirely — the flakes came out uneven in thickness, and the oven produced a mix of burnt and undercooked product. This kind of mismatch happens more often than buyers realise when evaluating corn flakes extrusion production line specifications. The extruder may run at its rated RPM, but if the screw elements and barrel temperature profile do not match the specific flour blend and incoming moisture, the output quality collapses regardless of what the brochure states. [NEED_CITE: starch gelatinisation temperature variance between corn flour and degerminated corn grits]
Screw Module Selection and Starch Gelatinisation Control
The twin-screw extruder at the heart of this line uses co-rotating sectional screw modules. Each module can be configured as a forward-transport, reverse-transport, mixing, or shearing element. For a corn flakes extrusion production line, the arrangement of these modules directly controls residence time, shear intensity, and the degree of starch gelatinisation achieved inside the barrel. A longer cooking zone with moderate shear produces the firm, dense pellet needed for proper flaking downstream, while excessive shear creates over-expanded material that crumbles at the press rollers.
Barrel Temperature Profiling and Moisture Management
Achieving the correct gelatinisation requires a precise barrel temperature profile across multiple heating zones, combined with controlled steam or water injection at the mixer stage. If the moisture entering the extruder is too low, the starch remains partially raw and the flakes will have a hard, gritty mouthfeel. If moisture is too high, the extrudate sticks to the press rollers and tears during flaking. The gas-fired high-temperature oven then removes residual moisture through both-side baking to lock in crispness. [NEED_CITE: optimal moisture range for corn flake extrusion and subsequent oven drying]
How Key Parameters Shape the Final Flake
The installed power ratings across the MT-65 through MT-85 range reflect different barrel volumes and screw diameters, each suited to a specific throughput band. The real power consumption figures — considerably lower than installed capacity — indicate the actual energy draw during steady-state extrusion of a typical corn-based formulation. The adjustable roller gap on the flakes press machine determines final flake thickness; too thin and the flakes break during conveying and packing, too thick and they fail to crisp evenly in the oven. The oil-forced automatic lubrication system on the gear box prevents unplanned stops during long production runs, which matters when a batch interruption can cause material to solidify inside the barrel.
The Cost of Skipping a Raw Material Trial Run
When a corn flakes extrusion production line specifications package omits a trial run on the buyer’s actual flour blend, the consequences surface after installation. The screw configuration may produce pellets that are too soft to hold shape at the press, or too dense to expand properly in the oven. Sugar coating may fail to adhere because the flake surface porosity is wrong. These are not defects that operator adjustments can fix — they require physical screw element changes and die replacement, delaying commissioning and eroding buyer confidence. [NEED_CITE: post-installation screw reconfiguration costs and production downtime]
Why This Line Is Engineered for the Buyer’s Process
Every station on the line — from the 4 kW mixer through the twin-screw extruder, the press, the oven, and the sugar spraying system — is sized so that throughput matches across the sequence, preventing bottlenecks where one station runs faster than the next. The screw configuration and die geometry are specified after testing the buyer’s raw material in an in-house workshop, not copied from a generic template. The separate controller box allows electrical parameters, including voltage and frequency, to be confirmed for the installation site before build completion. Food-grade stainless steel contact materials are used throughout to meet hygiene requirements in breakfast cereal production. Documentation including a trial run report, screw and die configuration record, and electrical schematic is provided so the buyer has a complete technical baseline from day one.
Documentation & Verification
- Line layout and capacity calculation showing matched throughput across mixer, extruder, press, and oven stations
- Screw and die configuration record specific to the buyer’s flour blend and target flake thickness
- Trial run report generated on the buyer’s raw material in the testing workshop before shipment
- Electrical schematic with voltage, frequency, and control language confirmed for the destination site
- Machine specification sheet detailing all station dimensions, power ratings, and material grades
- Operation and maintenance manual covering daily lubrication checks and screw element inspection intervals
Installation, Commissioning & Support
- Floor space planning based on overall line dimensions, from 12 m (MT-65) to 28 m (MT-85) with clearance for maintenance access
- Dedicated power circuit sized to the line’s real power draw, ranging from 59 kW to 167 kW depending on model
- Oven gas supply connection and ventilation requirements confirmed before the high-temperature baking stage is commissioned
- Roller gap calibration on the 16.12 kW flakes press machine during initial startup to match target flake thickness
- Operator training covering screw module swaps, barrel temperature adjustment, and self-cleaning procedures
- Wear parts list including replacement screw elements, die plates, and press roller surfaces supplied with the initial shipment
What We Need to Configure Your Line
To prepare an accurate corn flakes extrusion production line specifications proposal, please share your raw material details — including flour type, particle size, and typical moisture content — along with your target daily output and desired flake thickness. Let us know the voltage, frequency, and control language required at your facility, and whether you need the sugar spraying system or plan to produce plain flakes initially.
Frequently Asked Questions
Q: How do you select screw configuration and die design for different flour blends?
A: We test the buyer’s specific flour blend in our workshop, adjusting the arrangement of forward, mixing, and shearing screw modules until the extrudate reaches the correct gelatinisation level and pellet density for clean flaking. The die geometry is then matched to produce a uniform rope cross-section that feeds the press rollers consistently.
Q: What barrel temperature and moisture range are needed for proper starch gelatinisation?
A: The required profile depends on the flour composition and particle size. Generally, incoming moisture and barrel zone temperatures are adjusted together so that starch fully gelatinises without over-expansion. We document the working parameters from the trial run so they can be replicated on your production floor.
Q: How do you confirm the output capacity holds on our actual raw material?
A: We run your flour blend through the extruder in our testing workshop and measure actual output weight over a timed period. The trial run report records these figures alongside the screw configuration, barrel temperatures, and moisture levels used, giving you a verified baseline rather than a generic rating.
Q: How is throughput matched between the extruder, press, oven, and sugar sprayer?
A: Each station is sized based on the extruder’s verified output on your raw material. The press roller speed, oven belt speed and length, and sugar drum rotation are calculated so that no station accumulates backlog or starves the next, maintaining continuous flow through the entire corn flakes extrusion production line.
Q: What parameters control flake density and bowl-life performance?
A: Flake density is shaped by the degree of starch gelatinisation in the extruder, the compression ratio at the press rollers, and the final moisture level after oven drying. Adjusting screw shear, roller gap, and oven temperature together determines whether the flake stays crisp in milk or becomes soggy too quickly.



