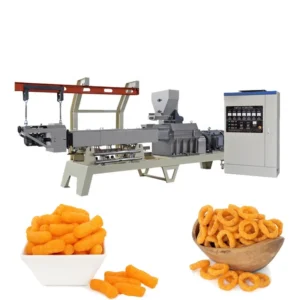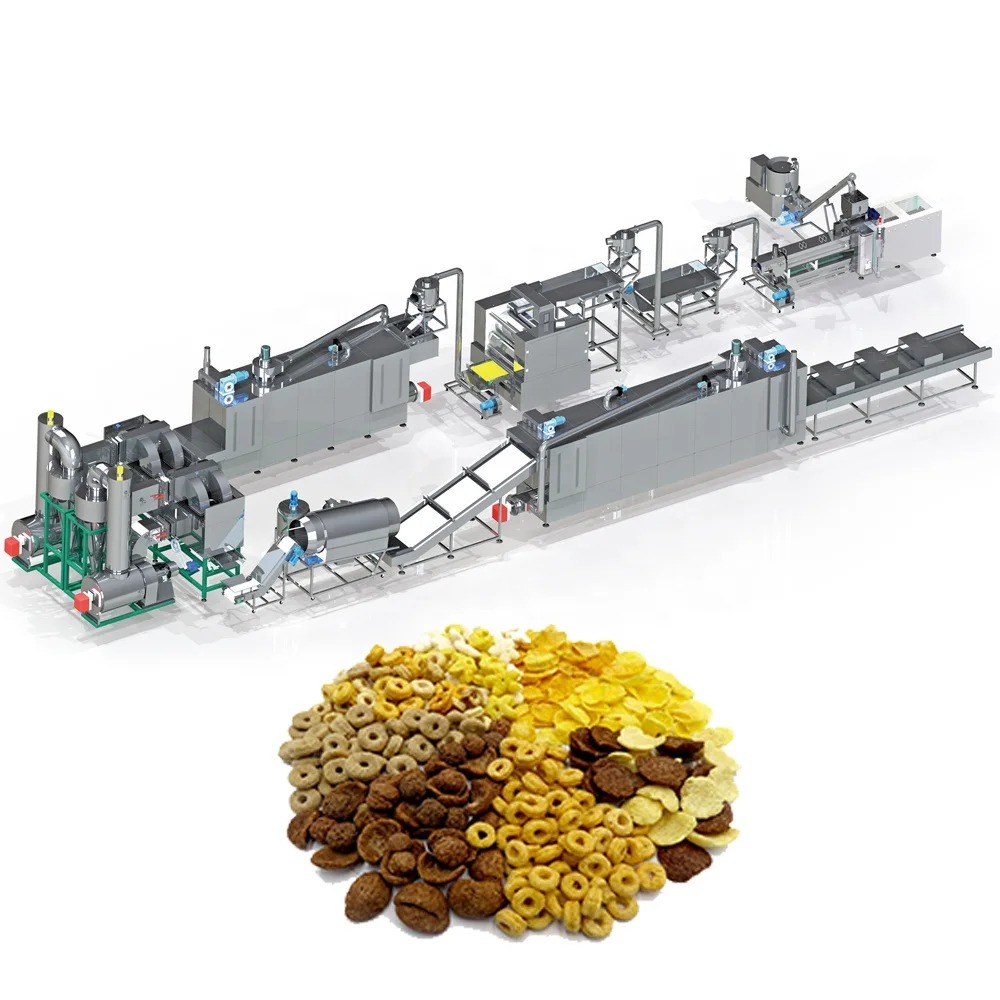
Throughput-Matched Extrusion Design — screw configuration and die geometry are specified to your actual corn flour lipid content and target flake density, not copied from a generic cereal build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Production Line (Twin Screw Extrusion) |
| Screw Type | Twin Screw |
| Installed Power | MT70: 160 kW; MT85: 190 kW; MT75: 210 kW |
| Power Consumption | MT70: 120 kW; MT85: 140 kW; MT75: 150 kW |
| Capacity (MT70) | 150–200 kg/hr (basis not stated in source — confirm raw material and moisture) |
| Capacity (MT85) | 300–400 kg/hr (basis not stated in source — confirm raw material and moisture) |
| Capacity (MT75) | 300–500 kg/hr (basis not stated in source — confirm raw material and moisture) |
| Overall Dimensions (MT70) | 41 × 1.5 × 2.2 m |
| Overall Dimensions (MT85) | 43 × 1.5 × 3.2 m |
| Overall Dimensions (MT75) | 45 × 1.5 × 3.5 m |
| Control System | PLC and MCC |
| Basic Materials | Corn, rice, wheat, oat, barley powder |
| Flaking Machinery | Hydraulic double-roller system, dual motors, infrared temperature pipe control |
| Hot Air Roasting Oven | Vibrating pan, high-temperature spraying tubes, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Dryer Heating Source | Gas or Electric |
| Final Product Shapes | Natural flakes, sugar-coated flakes, ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Assembly State | Complete turnkey line |
| Standards | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal retail | Corn grits or corn flour at controlled moisture |
| Sugar-coated corn flakes for mass-market packaging | Extruded corn pellets after hot air roasting |
| Multi-grain flaked cereal | Rice, wheat, oat, or barley powder blends |
| Multi-shape extruded cereal (rings, balls, stars) | Same twin-screw platform with adjusted die and mould |
Why "Rated Capacity" Tells Only Half the Story on a Corn Flakes Line
A number without raw material context is not a capacity — it is a guess.
When I first set up a corn flakes extrusion line for a Middle Eastern client, the factory trial ran smoothly on our standard corn flour. The moment we switched to their local supply — higher lipid content by a noticeable margin — the expansion ratio collapsed on site, and the entire roasting oven sat idle while we reworked the screw profile. That corn flakes extrusion production line turnkey project taught me something no spec sheet can: throughput depends on what you actually feed into the hopper, not what the brochure says [NEED_CITE: raw material variability in cereal extrusion processes].
Buyers who focus only on the headline kg/hr figure often discover that the extruder reaches that number on ideal laboratory flour while their production-grade corn grits behave entirely differently under shear and moisture. The downstream flaking rollers, dryer, and roasting oven were all sized around that optimistic number, so one station falling short cascades through the whole line.
How Screw Geometry and Barrel Profile Shape Your Flake Density
The twin-screw extrusion process for corn flakes depends on a precise balance between shear force, barrel temperature gradient, and residence time inside the barrel. A screw configuration designed for low-fat corn grits generates different gelatinisation behaviour than one built for oat-heavy blends, which means the die design and moisture injection points must be matched to your specific raw material before the line ever ships.
This corn flakes extrusion production line turnkey system uses PLC and MCC control to hold barrel zone temperatures within tight bands, giving operators repeatable starch gelatinisation across production runs. The screw elements can be reconfigured — forward-flight, reverse-flight, and kneading block sections rearranged — so the same extruder platform adapts when your cereal recipe changes or you introduce a new grain blend.
Why Flaking and Roasting Cannot Be Afterthoughts
Once the extruder produces a uniform pellet, the hydraulic double-roller flaking station compresses each piece to a target thickness. Infrared temperature pipe control keeps the roller surface consistent across the full width, preventing edge flakes that are thinner than centre flakes — a common cause of uneven browning further downstream. The dual-motor arrangement drives each roller independently, which matters when flake thickness tolerance is tight [NEED_CITE: roller pressure uniformity in flaked cereal production].
The hot air roasting oven then takes those flattened pellets and creates the surface bubbling and crispy texture the market expects. A vibrating pan moves the flakes through a high-temperature spraying zone while two separate circulating fans maintain even heat distribution. Cyclone dust removal pulls fine particulate out of the air stream before it can settle back onto the product or foul the heating elements.
Reading Between the Spec Sheet Numbers
The installed power range across the three models — 160 kW to 210 kW — reflects different barrel volumes and screw diameters, which directly determine how much raw material can be plasticised and pushed through the die per hour. Higher installed power supports a larger screw diameter and longer barrel, giving the material more residence time for complete starch gelatinisation before it exits the die.
The control system being PLC and MCC rather than simple relay logic means every barrel zone, the flaking roller pressure, and the roasting oven fan speed can be monitored and logged simultaneously. For a production manager running multiple cereal formats on the same corn flakes extrusion production line turnkey platform, this translates to recipe storage and recall — switch from natural corn flakes to sugar-coated rings without manually resetting every parameter.
Gas or electric heating options on the dryer and roaster let the line match the utility infrastructure at your facility. Regions with expensive industrial electricity typically favour gas-fired heating, while sites with strict emissions regulations may prefer electric elements for cleaner temperature control.
What Happens When Stations Are Sized Separately
An extruder running at its nominal output feeds flakes into a dryer that was quoted by a different vendor at a slightly lower throughput. The dryer becomes the bottleneck, forcing the extruder to idle in cycles, which causes temperature fluctuations in the barrel and inconsistent gelatinisation. Operators then adjust screw speed to compensate, pushing the product further outside specification [NEED_CITE: bottleneck cascade effects in multi-station food processing lines].
When the roasting oven capacity is mismatched, flakes pile up on the vibrating pan in a thicker layer than the hot air can penetrate evenly. The result is a mix of properly blistered flakes and under-roasted ones in the same batch, leading to texture complaints from end consumers that are difficult to trace back to the equipment imbalance.
Engineering Accountability Under One Roof
Every station on this line — from the batching and mixing system through extrusion, flaking, drying, roasting, optional sugar coating, cooling, and packing — is capacity-calculated as a single system. Throughput is matched at each hand-off point so no station starves or floods the next.
Screw configuration and die design are documented specifically against your raw material sample, not pulled from a generic cereal template. The in-house testing workshop runs your actual corn flour or grain blend before the line ships, so expansion ratio, flake thickness, and roasting behaviour are validated before installation begins.
Pre-sales consultation covers line layout, utility planning, and phased installation scheduling. On-site commissioning includes operator training on the PLC interface, recipe management, and daily maintenance routines for wear parts like screw elements and die plates.
Documentation & Verification
- Line layout and capacity calculation showing matched throughput at every station
- Screw and die configuration record tied to your specific raw material sample
- Trial run report from the testing workshop on your corn flour or grain blend
- Electrical schematic with confirmed voltage, frequency, and control language
- CE declaration of conformity and ISO certificate for the complete line
- Wear parts list with recommended replacement intervals for screws, dies, and roller sleeves
Installation, Commissioning & Support
- Foundation plan accounts for the full line footprint, up to 45 m in length for the MT75 configuration
- Dedicated electrical circuits sized to the model’s installed power, up to 210 kW at confirmed voltage
- Extruder barrel sections and flaking rollers arrive disassembled for rigging into position
- First production run verifies PLC recipe parameters against trial run benchmarks
- Operator training covers screw element replacement and hydraulic roller pressure adjustment
- Spare screw elements and die plates shipped with initial order to cover first maintenance cycle
What We Need to Move Your Inquiry Forward
Share your raw material specification — corn variety, lipid and moisture content, particle size distribution — along with the target flake dimensions and daily production volume you need to meet. Let us know your workshop dimensions and ceiling height, the local voltage and frequency standard, and whether you plan to run both natural and sugar-coated variants on the same line.
Frequently Asked Questions
Q: How is line capacity verified against my specific raw material and moisture level?
A: Before the line ships, we run your actual corn flour or grain blend through the extruder in our testing workshop. The trial documents expansion ratio, pellet density, and flake thickness under controlled moisture conditions. This report becomes the baseline for on-site commissioning, so capacity claims are grounded in your material behaviour rather than generic test flour.
Q: How are extruder, flaking, dryer, and roaster throughput matched to avoid station bottlenecks?
A: Each station is capacity-calculated as part of the complete line layout rather than sourced and quoted independently. The flaking roller feed rate, dryer belt loading, and roasting oven pan depth are all set so material flows continuously without accumulation or starvation between stations.
Q: What screw and die configuration is specified for corn flakes versus other cereal shapes?
A: Corn flakes require a screw profile that achieves full starch gelatinisation at moderate shear, producing a dense pellet suitable for hydraulic flaking. Multi-shape formats like rings or balls use a different die plate and often a higher-expansion screw arrangement. Both setups are documented and tested before shipment.
Q: How is factory layout designed and what utility planning is included?
A: The line layout document maps every station position, material flow direction, and utility connection point to your workshop dimensions. Gas lines for the roaster, electrical circuits for the PLC and MCC panels, and dust extraction ducting for the cyclone system are all specified so your contractor can prepare before equipment arrives.
Q: What does on-site installation, commissioning, and operator training cover?
A: Engineers supervise mechanical assembly, electrical termination, and the first production runs on your raw material. Training covers PLC recipe management, screw element inspection, hydraulic roller adjustment, and daily cleaning procedures. A wear parts list with replacement intervals is provided so your maintenance team can plan proactively.