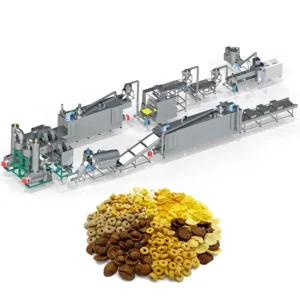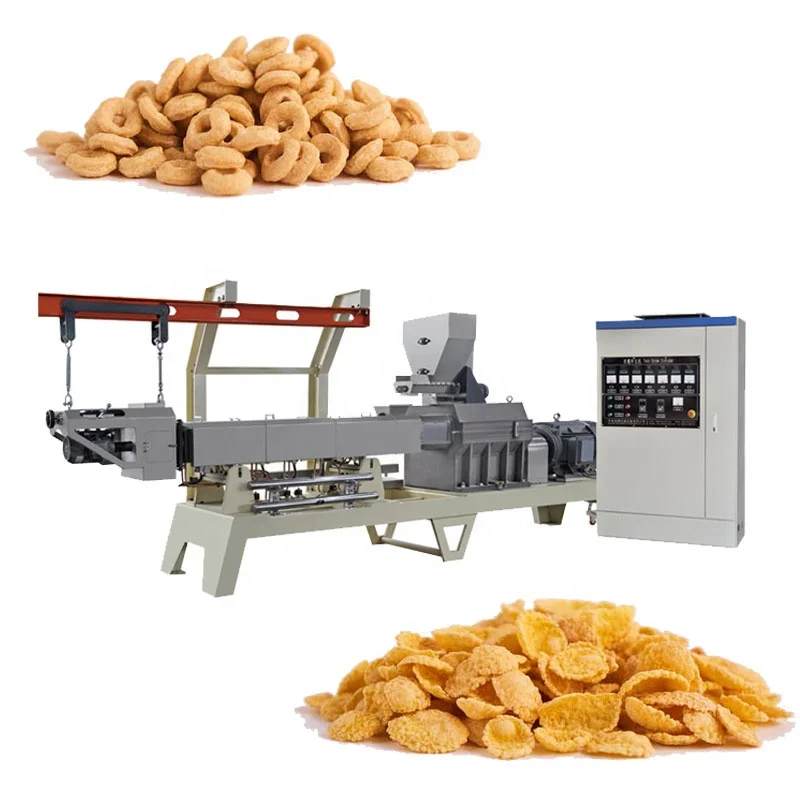
Twin-Screw Configuration Matched to Raw Material — screw module arrangement and die geometry are specified after in-house trial runs on the buyer’s actual cereal flour or grits, not copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65 / MT-70 / MT-85 / MT-75 |
| Product Type | Corn Flakes Production Line / Breakfast Cereal Extrusion Line |
| Screw Type | Co-rotating twin-screw, sectional modules |
| Output Capacity (MT-65) | 120–150 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| Output Capacity (MT-70) | 200–250 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| Output Capacity (MT-85) | 300–400 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| Output Capacity (MT-75) | 400–500 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| Installed Power (MT-65) | 84 kW |
| Installed Power (MT-70) | 132 kW |
| Installed Power (MT-85) | 239 kW |
| Installed Power (MT-75) | 186 kW |
| Real Power Consumption (MT-65) | 59 kW |
| Real Power Consumption (MT-70) | 92 kW |
| Real Power Consumption (MT-85) | 167 kW |
| Real Power Consumption (MT-75) | 140 kW |
| Overall Dimensions (MT-65) | 21000 × 1200 × 2200 mm |
| Overall Dimensions (MT-70) | 23000 × 1500 × 2200 mm |
| Overall Dimensions (MT-85) | 28000 × 3500 × 4300 mm |
| Overall Dimensions (MT-75) | 24000 × 1500 × 2800 mm |
| Press Roller Size | 510 × 310 × 1050 mm |
| Press Station Power | 16.12 kW |
| High-Temperature Oven Dimensions | 4.5 × 1.4 × 1.8 m |
| Oven Heating Source | Gas (source value — verify against manufacturer catalog) |
| Control System | Separate controller box (PLC/MCC not specified in source — verify against manufacturer catalog) |
| Certifications | CE (since 2014), ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn flakes breakfast cereal | Corn flour or corn grits, plain or lightly sweetened |
| Multi-grain flaked cereal | Blends of rice, millet, wheat, oat and barley powders |
| Fortified breakfast flakes | Cereal base with added vitamin and mineral premix |
| Extruded snack pellets | Wheat, rice or corn-based dough for secondary processing |
What a Copied Screw Profile Does to Your Flake Density
A screw and die configuration taken from a generic build produces flakes that bake unevenly, lose crispness in milk, and fail bowl-life tests before reaching the consumer.
I worked with a buyer who received an extruder with a standard screw stack designed for pure corn grits. When they switched to a local supplier’s blend with lower starch content, the pellets came out dense and refused to expand through the press rollers. The entire first production batch was written off. The corn flakes extrusion technology only works when the barrel zones, moisture input and screw pitch are set for the specific raw material running through the machine [NEED_CITE: raw material starch content and gelatinisation behaviour in twin-screw extrusion]. That is the difference between a line that runs on day one and one that needs weeks of trial-and-error adjustment.
Barrel Temperature Profiling and Starch Gelatinisation
The co-rotating twin-screw extruder uses sectional barrel zones, each with independent heating and cooling. For corn flakes extrusion technology, the temperature must climb progressively from the feed section through the cooking zone so that starch granules absorb moisture and swell at a controlled rate. If the profile is too flat, the dough passes through under-cooked and the flakes will be brittle rather than crisp after baking.
Moisture, Shear and the Pellet That Becomes a Flake
Water injection points along the barrel let operators fine-tune moisture content inside the extruder. The sectional screw modules create shear that works together with heat to complete gelatinisation. Getting this balance right determines whether the extrudate holds its shape through the press rollers or collapses into an uneven sheet. The breakfast cereal twin-screw extruder is configured so that each module position — conveying, mixing, de-gassing, cooking — can be re-arranged when the buyer changes from corn to a multi-grain formulation.
Press Gap, Oven Heat and Final Flake Geometry
After extrusion, the cooked dough passes through a dedicated press station where the roller gap sets flake thickness. The 510 mm roller width provides a consistent sheet that enters the gas-fired high-temperature oven for toasting on both sides. Oven residence time and temperature must match the moisture leaving the press; too short and the centre stays soft, too long and the edges scorch before the core dries [NEED_CITE: gas oven temperature profiling for breakfast cereal flake baking]. This three-stage sequence — extrusion, pressing, baking — is where density and crispness are actually locked in.
Reading the Spec Sheet Against Your Raw Material
The installed and real power figures across the MT-65, MT-70, MT-85 and MT-75 models show a wide range, reflecting different throughput targets and barrel diameters. Real power consumption sits well below installed capacity because the motor must handle start-up torque and viscosity spikes when cold material first enters the barrel. Overall line length varies from 21 m to 28 m, which tells you how many stations — mixer, extruder, dryer, press, oven, cooler, packer — are matched in sequence. A shorter line at a given capacity usually means fewer drying or cooling passes, which can leave residual moisture in the finished flake.
The Hidden Cost of a Mismatched Dryer or Oven
When the dryer or oven capacity is smaller than what the extruder can produce, the line bottlenecks at the thermal stage. Flakes pile up on the conveyor, cool unevenly, and develop moisture gradients that cause breakage during packing. I have seen installations where the extruder ran at full output but the oven could only handle a fraction, forcing the operator to slow the entire line and idle the press rollers [NEED_CITE: throughput mismatch between extruder and downstream thermal equipment]. The result is lower actual output than the nameplate suggests and higher energy cost per kilogram of saleable product.
Why Engineers Source This Line Here
Screw configuration and die design are specified to the buyer’s cereal formulation, not pulled from a catalogue default. The in-house testing workshop runs the buyer’s own raw material through the extruder before shipment, generating a trial run report that documents gelatinisation degree, pellet shape and post-bake flake density. Every station — from the batching mixer to the cooling conveyor — is sized so throughput matches across the entire corn flakes extrusion technology line rather than being assembled from separate vendors. Electrical schematics and voltage confirmation are completed before production starts, preventing commissioning delays. CE and ISO documentation is provided as standard, supporting import compliance in regulated markets.
Documentation & Verification
- Screw and die configuration record matched to your cereal flour or grit blend
- Trial run report on customer-supplied raw material confirming gelatinisation and flake density
- Line layout drawing with throughput calculation across every station
- Electrical schematic with voltage and frequency confirmed for your installation site
- CE declaration of conformity and ISO certificate for customs and regulatory filing
- Operation and maintenance manual with wear parts list for screws, dies and rollers
Installation, Commissioning & Support
- Foundation plan accounts for the 21–28 m line length and press station vibration load
- Dedicated power circuit sized to the model’s installed power, up to 239 kW for the MT-85
- Machine shipped in sectional modules for container loading and on-site re-assembly
- First-run commissioning includes barrel temperature calibration and press roller gap setting
- Operator training covers screw module changes for switching between corn and multi-grain recipes
- Wear parts inventory covers screws, dies and press roller bearings for the first replacement cycle
- Routine maintenance schedule tied to running hours for gearbox oil and barrel liner inspection
What to Include in Your Inquiry
To move from general interest to a line proposal, share the cereal raw material you plan to run — corn grits, wheat flour, oat blend — along with any nutrient premix additions. Confirm your target daily output and the floor space available, including ceiling height for the dryer and oven exhaust ducting. Specify local voltage and frequency, and whether the control interface needs to be in a language other than English. If you have existing upstream mixers or downstream packing machines, note their throughput so the new line can be matched at the connection points.
Frequently Asked Questions
Q: How is screw configuration matched to different cereal raw materials?
A: Each cereal has a distinct starch profile and particle size. Corn grits need higher shear and a longer cooking zone than fine wheat flour. We re-arrange the sectional screw modules and select die geometry after running your specific material in the testing workshop, documenting the setup so you can replicate it on your factory floor.
Q: What barrel temperature profile and moisture range are needed for proper starch gelatinisation in corn flakes?
A: Barrel zones typically step up from the feed section to the cooking zone, with moisture adjusted through water injection points. The exact profile depends on your raw material’s starch content and particle size. The trial run report records the temperature and moisture settings that produced acceptable gelatinisation for your formulation.
Q: How is flake density and crispness controlled through the extrusion-press-baking sequence?
A: Density starts with the degree of gelatinisation inside the extruder, then the press roller gap sets flake thickness, and finally the gas-fired oven toasts both sides. Adjusting any one stage affects the others, so all three are calibrated together during the in-house trial run before the line ships.
Q: Can the extrusion line produce both plain and fortified breakfast cereal flakes?
A: Yes, provided the nutrient premix is introduced at the correct stage — usually at the mixer before extrusion — and the barrel temperature is kept within a range that preserves heat-sensitive vitamins. The screw configuration and temperature profile are adjusted during the trial run to balance gelatinisation with nutrient retention.
Q: What trial run testing is performed on the buyer’s raw material before the extruder ships?
A: We run your actual flour or grits through the extruder in our testing workshop, recording gelatinisation degree, pellet shape, moisture content and post-bake flake density. The trial run report is shared before shipment so you can review results and request adjustments to the screw stack or die before the machine leaves the factory.