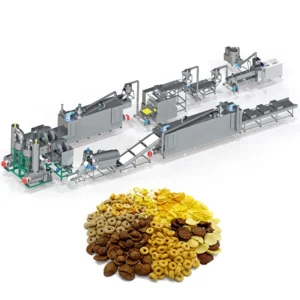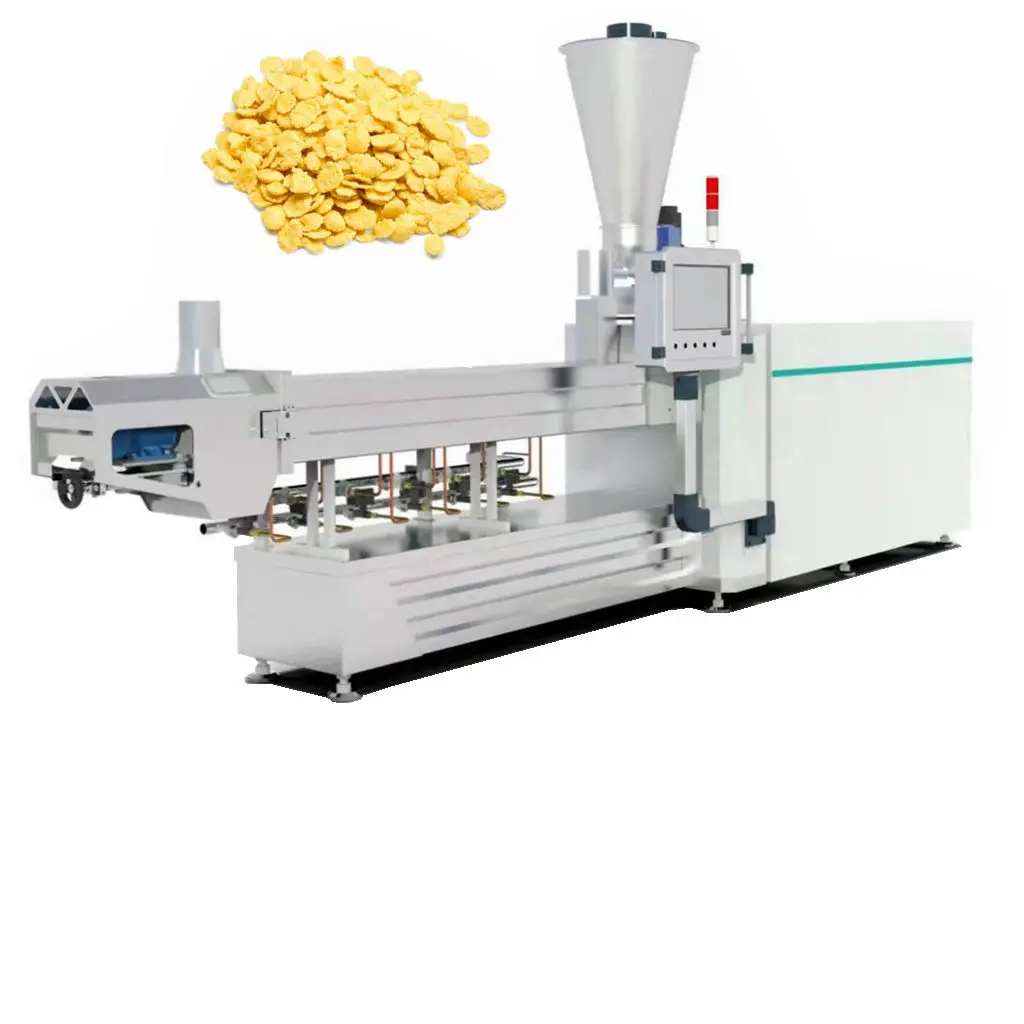
Screw Geometry Matched to Your Cereal — Every screw element and die specification on this corn flakes extrusion line is configured against your actual grain formulation before the line ships, not copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 (line also available in MT70, MT85 variants) |
| Product Type | Twin Screw Corn Flakes Extrusion Production Line |
| Extruder Type | Twin Screw |
| Installed Power | 210 kW (MT75) |
| Power Consumption | 150 kW (MT75) |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Overall Dimensions | 45 × 1.5 × 3.5 m (MT75) |
| Control System | PLC with MCC integration |
| Screw Features | Automatic lubrication and cooling function |
| Flaking Machinery | Hydraulic double-roller system with independent motor drive and infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Vibrating pan, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Material Compatibility | Corn, rice, wheat, oat, barley powder |
| Assembly State | Complete production line |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour formulations |
| Sugar-coated corn flakes | Corn base with sugar syrup coating stage |
| Multi-grain breakfast cereals | Rice, wheat, oat, and barley blends |
| Shaped cereal variants | Rings, stars, loops, balls, tubes, wheels via die changes |
What "300 kg/h" Means When the Screw Profile Is Wrong
A capacity figure means nothing if the screw configuration cannot hold that throughput on your specific grain blend and moisture level.
I have watched lines get commissioned in Southeast Asian plants where the extruder was set up for a standard corn grit recipe, only for the buyer to switch to a higher-fiber multi-grain mix on day two. The result was inconsistent gelatinisation, uneven flake thickness after the roller press, and a roasting oven that could not produce uniform blistering. The twin screw extruder corn flakes production line sat at half its quoted output for weeks while screw elements were reordered and barrel temperature profiles were re-mapped from scratch [NEED_CITE: starch gelatinisation behaviour across different cereal grain formulations].
How Screw Configuration Drives Flake Texture
The MT75 twin-screw extruder works through six integrated subsystems — feeding, extruding, cutting, heating, gearing, and controlling — each of which influences how starch granules respond to shear and thermal input. The screw element arrangement determines residence time and mechanical energy input, which directly controls the degree of starch gelatinisation. For corn flakes, the target is partial gelatinisation: enough to bind the pellet into a coherent half-product, but not so much that the dough becomes overly plastic and loses its ability to blister during roasting. The corn flakes extrusion technology at this stage is about restraint as much as it is about energy input.
Barrel Temperature Profile and Moisture Interaction
The barrel sections are individually heated, allowing a gradient that typically starts lower at the feed zone and rises through the compression and metering zones. Moisture content of the incoming mix interacts with this profile — higher moisture requires more thermal energy to reach the same gelatinisation point, while lower moisture risks premature drying inside the barrel. In our testing workshop, we run the buyer’s actual cereal formulation to map the relationship between barrel setpoints, screw speed, and feed moisture. This trial establishes the baseline process window before the line is cleared for shipment [NEED_CITE: barrel temperature profiling for twin-screw cereal extrusion].
Reading the Specs That Matter for Corn Flake Quality
The installed power of 210 kW on the MT75 tells you the thermal and mechanical headroom available, but power consumption at 150 kW reflects what the line actually draws under typical operating conditions — a difference that matters for your electrical infrastructure planning. The hydraulic double-roller flaking machinery uses independent motors for each roller, which means the gap and pressure can be adjusted dynamically rather than relying on a single fixed drive. Infrared sensors monitor roller surface temperature continuously; this prevents the dough pellets from sticking on one side and tearing on the other, which is a common source of thickness variation. The roasting oven’s conciliation burner with dual circulating fans and cyclone dust removal creates a controlled hot-air environment where surface blistering happens consistently — the characteristic visual signature of a proper corn flake depends on this stage as much as on the extruder itself. The PLC control system with MCC integration allows operators to store and recall process recipes, so switching between a natural corn flake run and a sugar-coated variant does not require manual re-entry of every parameter.
When a Generic Build Reaches the Buyer’s Floor
A twin screw extruder corn flakes production line assembled from generic screw configurations and untested die geometry will produce pellets that look acceptable at the extruder exit but fail downstream. Flakes that are too dense will not blister in the roasting oven. Flakes that are too thin will over-dry and shatter during coating and packing. I have seen plants run for an entire first production cycle before the quality team flagged bowl-life failures — the flakes went soggy in milk within minutes because the internal cell structure never developed correctly during extrusion. Retracing the problem to screw configuration and re-cutting dies adds weeks of downtime and parts cost that a pre-shipment trial would have prevented entirely [NEED_CITE: post-installation rework costs from untested extrusion configurations].
Why This Line Is Built Around Your Formulation
Every station on this line — mixing, extruding, flaking, drying, roasting, coating, cooling, and packing — is sized so that throughput does not bottleneck at any single point. The screw configuration and die design are specified to the buyer’s raw material and target flake density, not pulled from a catalogue default. Our in-house testing workshop runs your cereal formulation on the actual extruder before the line ships, producing a trial run report that documents screw arrangement, barrel settings, and flake output quality. Electrical schematics are prepared with your local voltage and frequency confirmed before production begins, eliminating the commissioning delays that happen when a control panel arrives wired for the wrong supply. Documentation includes a complete screw and die configuration record so that replacement wear parts match the original specification exactly.
Documentation & Verification
- Line layout engineered to your factory footprint with station throughput calculations
- Screw and die configuration record specific to your cereal formulation
- Trial run report on your raw material from our testing workshop before dispatch
- Electrical schematic with voltage and frequency confirmed to your local supply
- CE declaration of conformity and ISO certificate included with shipment
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation plan provided based on the 45 × 1.5 × 3.5 m line footprint and station weights
- Dedicated circuit sizing for the 210 kW installed power draw with voltage confirmation before build
- Assembled line shipped in modular sections for reassembly aligned to your floor layout
- On-site commissioning includes barrel temperature mapping and screw speed calibration for your formulation
- Operator training covers PLC recipe storage, hydraulic roller gap adjustment, and roasting oven burner tuning
- Wear parts list covers screws, dies, and roller surfaces with recommended replacement intervals
What We Need to Configure Your Line
To build an accurate line proposal, share your target cereal formulation including grain types and approximate moisture content, your intended daily or hourly production volume, and the available floor space and ceiling height in your plant. We also need your local voltage and frequency specification along with preferred control language, so the PLC interface and electrical build match your site from day one.
Frequently Asked Questions
Q: How is screw configuration determined for my specific cereal formulation?
A: We analyse your grain blend’s starch content, protein level, and target moisture, then select screw element geometry and L:D ratio accordingly. The configuration is validated by running your actual raw material in our testing workshop, adjusting element arrangement until the extruded pellet achieves the correct density and gelatinisation level for proper downstream flaking and roasting.
Q: What moisture range does the extrusion process require for corn flakes?
A: The typical feed moisture window for corn flake extrusion falls within a narrow band that allows partial starch gelatinisation without over-plasticising the dough. Exact setpoints depend on your grain composition and are established during the pre-shipment trial run. The PLC stores these parameters as a saved recipe for consistent batch-to-batch repeatability.
Q: How does flaking roller gap and temperature affect final flake quality?
A: The hydraulic double-roller system on this line adjusts gap and pressure independently for each roller, while infrared sensors maintain consistent surface temperature. Too wide a gap leaves pellets under-flattened and prone to uneven roasting; too narrow a gap causes edge cracking and breakage. Both parameters are tuned during commissioning against your target flake thickness.
Q: Can the same extruder produce different breakfast cereal shapes?
A: Yes. The MT75 extruder accepts different die configurations to produce rings, stars, loops, balls, tubes, wheels, and other shapes. Each die geometry interacts with the screw configuration differently, so we document the screw and die pairing for every shape you plan to run, ensuring that texture and density remain within specification across format changes.
Q: How is the roasting oven tuned for proper surface blistering?
A: The conciliation burner, dual circulating fans, and vibrating pan work together to create a controlled hot-air profile across the flake bed. Burner temperature, air velocity, and residence time are adjusted during commissioning to produce the characteristic surface blister without over-drying the flake interior, preserving both crispness and acceptable bowl-life in milk.