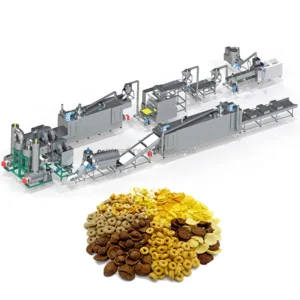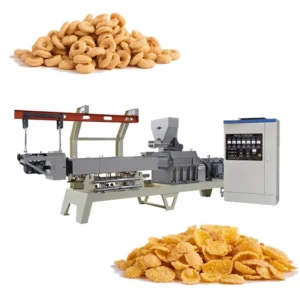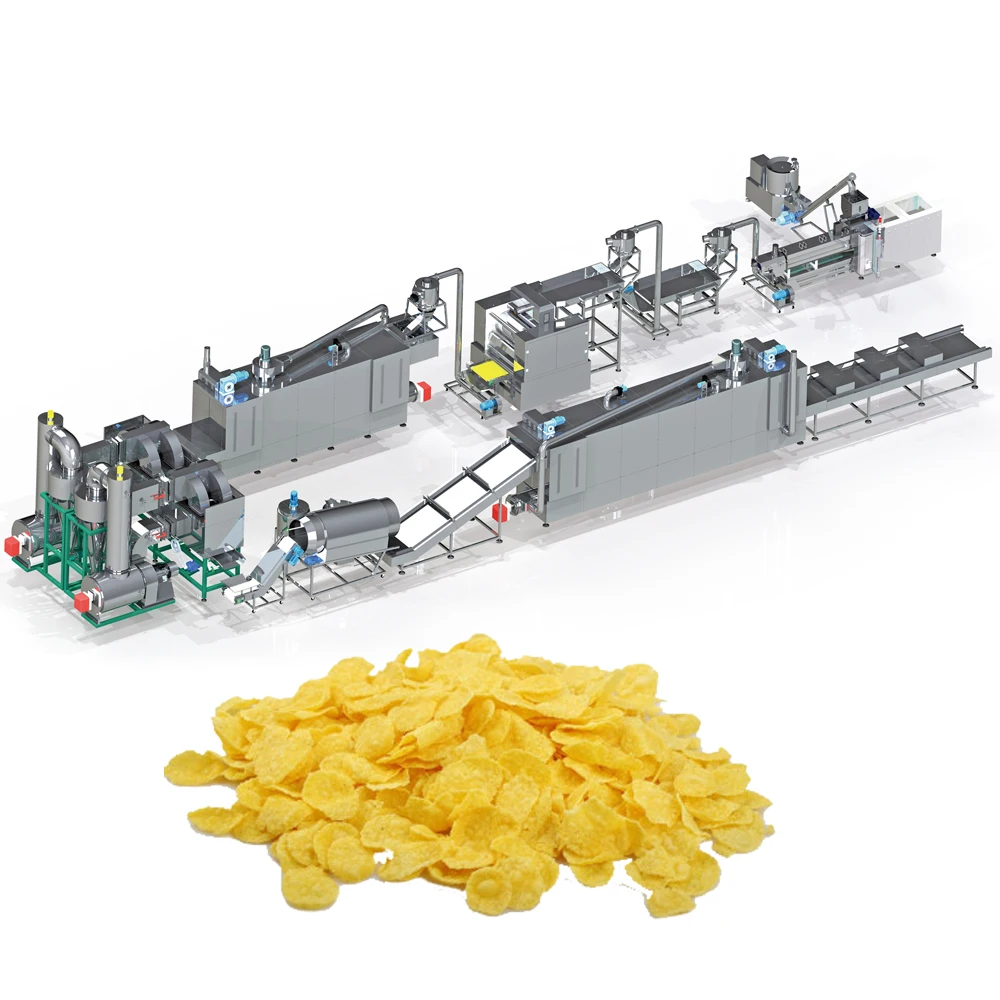
Screw Configuration Matched to Your Raw Material — We map every sectional module to your specific corn grits or multigrain blend, ensuring gelatinisation and flake density hold across sustained production runs.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Model | MT-65 / MT-70 / MT-75 / MT-85 |
| Extruder Type | Co-rotating Twin Screw with sectional modules |
| Installed Power (MT-65) | 84 kW |
| Real Power (MT-65) | 59 kW |
| Installed Power (MT-70) | 132 kW |
| Real Power (MT-70) | 92 kW |
| Installed Power (MT-75) | 186 kW |
| Real Power (MT-75) | 140 kW |
| Installed Power (MT-85) | 239 kW |
| Real Power (MT-85) | 167 kW |
| Output Capacity (MT-65) | 120–150 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| Output Capacity (MT-70) | 200–250 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| Output Capacity (MT-75) | 300–400 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| Output Capacity (MT-85) | 400–500 kg/h (basis not stated in source — confirm raw material, moisture, flake thickness) |
| Overall Dimensions (MT-65 Line) | 12,000 × 1,200 × 2,200 mm |
| Overall Dimensions (MT-75 Line) | 24,000 × 1,500 × 2,800 mm |
| Overall Dimensions (MT-85 Line) | 28,000 × 1,500 × 2,800 mm |
| Mixer Tank Size | φ600 × 500 mm |
| Mixer Power | 4 kW |
| Flaking Roller Size | 510 × 310 × 1,050 mm |
| Flaking Machine Power | 16.12 kW |
| Flaking Machine Features | Cooling system, adjustable roller gap |
| Oven Heating | Gas-fired, dual-side baking |
| Oven Power | 3.75 kW |
| Sugar Spraying System Power | 28.75 kW |
| Sugar Spraying Roller Size | approx. φ600 × 2,700 mm |
| Gear Box Lubrication | Forced automatic oil lubrication |
| Screw Self-Cleaning | Yes |
| Cutting System | Non-stop cutting |
| Line Stations | Mixer → Screw Conveyor → Twin-Screw Extruder → Flaking Press → High-Temperature Oven → Sugar Spraying System |
| Standards | CE, ISO |
| Warranty | 1 year complete warranty + lifetime maintenance |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flakes for breakfast cereal retail | De-germed corn grits, varying particle size and moisture |
| Multigrain breakfast flakes | Blends of corn, rice, wheat, oat |
| Oat-based snack flakes | Oat groats and oat flour blends |
| Fortified breakfast cereals | Grain blends with added vitamin and mineral premix |
| Sweetened coated cereal flakes | Corn or multigrain flakes with sugar or syrup coating |
Why "Nominal Capacity" Is the Wrong Starting Point for Corn Flakes Extrusion
Sustained output depends entirely on how the corn flakes extrusion line screw configuration die design responds to your actual raw material.
A breakfast cereal line rated at a certain throughput on standard corn flour can behave very differently when you switch to the de-germed corn grits available in your local market. I once spent two weeks reconfiguring the screw combination and die geometry for a client whose local grits had different moisture content and particle distribution than the trial material. Flake thickness became uneven, and nearly half the output cracked during baking. [NEED_CITE: raw material variability in grain processing across regional supply chains]
The extrusion variables — moisture content entering the barrel, starch gelatinisation temperature, residence time, and die land length — all shift when you change feedstock. A line that performs well during a factory test on one material can struggle on another if the screw configuration and barrel temperature profile were never adjusted. This is why a trial run on your actual raw material is not optional — it is the only way to verify that the corn flakes extrusion line screw configuration die design will deliver stable output in your facility.
Barrel Temperature Zones and Starch Gelatinisation
A co-rotating twin-screw extruder processes material through distinct functional zones — feeding, compression, gelatinisation, and metering — each controlled by independent barrel heating and cooling circuits. For corn flakes, the degree of starch gelatinisation directly determines how well the pellet holds together during flaking and how the final flake behaves in milk. The corn flakes extrusion line screw configuration die design must balance shear intensity and residence time so that gelatinisation is thorough without causing premature expansion at the die face.
Die Geometry and Pellet Integrity Before Flaking
The die plate determines pellet shape, size, and density before the material reaches the flaking press. A die with incorrect land length or orifice diameter produces pellets that either expand too much — becoming hollow and fragile — or too little, resulting in dense pellets that resist flattening. Matching die geometry to the specific screw configuration and raw material blend is what keeps pellet structure consistent, which is the foundation of uniform flake thickness and reliable bowl-life. [NEED_CITE: extrusion die design principles for cereal pellet forming]
Decoding the Power and Dimension Data Across Line Variants
The gap between installed power and real power across the MT-65 through MT-85 models reflects actual energy consumption during steady-state extrusion, not motor nameplate totals. For a process engineer evaluating utility load, the real power figures — ranging from 59 kW on the MT-65 to 167 kW on the MT-85 — give a more accurate basis for electrical infrastructure planning. The forced automatic oil lubrication on the gearbox maintains thermal stability during continuous gelatinisation cycles, which matters when the extruder runs for extended shifts. Line footprint scales accordingly, from 12 metres for the MT-65 line to 28 metres for the MT-85, so floor planning must account for the full station sequence from mixer through sugar spraying. The flaking press includes a cooling system and adjustable roller gap, which directly controls flake thickness and prevents pellet adhesion to the roller surface during high-throughput runs.
The Hidden Cost of Skipping Configuration Verification
When an extruder ships with a generic screw build copied from a standard template rather than matched to the buyer’s material, the problems do not appear until production starts. Flakes come out too thin and shatter in the oven, or too thick and remain doughy in the centre. The flaking press may bottleneck because pellet consistency is poor, or the oven cannot remove moisture evenly across irregularly shaped flakes. These issues consume weeks of line downtime and raw material waste while the process is re-tuned from scratch. [NEED_CITE: cost of unplanned downtime in continuous food processing lines]
Why Process Engineers Source This Extrusion Platform Here
Screw configuration and die design are specified against your raw material and target flake density, not copied from a default build sheet. The in-house testing workshop runs your actual corn grits or multigrain blend before shipment, producing a trial run report that documents gelatinisation degree, expansion ratio, and flake density. Every line variant is configured as a complete sequence from batching through coating, so throughput is matched between the extruder, flaking press, oven, and sugar spraying stations rather than assembled from mismatched vendors. Twin-screw expertise spans breakfast cereals, pet food, aquatic feed, and snack applications, meaning the engineering team understands how material behaviour differs across product categories. Pre-sales consultation covers line layout, utility planning, and barrel temperature profiling, extending through on-site installation and operator training.
Documentation & Verification
- Trial run report on your specific corn grits or multigrain blend confirming flake density and gelatinisation before dispatch
- Screw and die configuration record documenting exact sectional module layout matched to your product target
- Line layout drawing with capacity calculation verifying throughput balance across every station
- Electrical schematic with voltage and frequency confirmation matching your facility power supply
- CE declaration of conformity and ISO certificate in electronic format for import documentation
- Wear parts list with part numbers for screws, dies, and flaking roller components
Installation, Commissioning & Support
- Floor space planning based on line dimensions up to 28,000 mm length, including utility connection points for gas-fired oven and electrical panels
- Dedicated electrical circuit sized for real power draw up to 167 kW on the MT-85 variant, with voltage and frequency matched to local supply
- Equipment arrives in sectional modules requiring on-site assembly and alignment of extruder barrel, flaking press, and oven conveyor
- First-run commissioning includes barrel temperature profile calibration, screw speed tuning, and flaking roller gap adjustment to target flake thickness
- Operator training covers screw module changeover procedures, die plate replacement, and daily cleaning of the self-cleaning twin-screw assembly
- Forced automatic oil lubrication system requires periodic fluid level checks and filter replacement per the maintenance schedule
What to Include in Your Inquiry
Provide the specific type and source of your raw material — de-germed corn grits, oat blends, or multigrain formulations — along with typical moisture content and particle size range. Specify your target flake thickness, bowl-life requirement, and daily production volume so the line variant and station sizing can be matched accordingly. Include your facility voltage, frequency, and available floor space so the electrical and layout configuration is confirmed before production begins. Indicate whether you need a trial run on your material before the equipment ships.
Frequently Asked Questions
Q: How is output capacity verified against my specific raw material and moisture content?
A: We run your actual corn grits or multigrain blend through the extruder in our testing workshop before shipment. The trial run measures gelatinisation degree, pellet structure, and resulting flake density under controlled moisture and temperature conditions. A full report documents the parameters, so you know the line will hold its rated output on your material before it arrives at your facility.
Q: How do you select screw configuration and die geometry for corn grits versus oat or multigrain blends?
A: Each raw material has different starch composition, fibre content, and moisture absorption behaviour. We select forward and reverse screw elements, mixing blocks, and die land length to match the gelatinisation profile your material requires. The die orifice diameter is set to produce pellets with the correct density for your target flake thickness after pressing.
Q: What barrel temperature profile is needed for proper starch gelatinisation without over-expansion?
A: The profile typically starts low in the feeding zone and increases through the compression and cooking zones, then drops slightly before the die to control expansion. The exact temperatures depend on your raw material’s starch type and moisture level. During the trial run, we map the profile that achieves full gelatinisation while keeping pellet expansion within the range your flaking press can handle.
Q: How do you ensure flaking roller gap and cooling match the extruder output to avoid bottlenecks?
A: The flaking press is sized to handle the full output of the selected extruder model. The adjustable roller gap sets flake thickness, and the integrated cooling system prevents pellet sticking during continuous operation. We verify during the trial run that pellet temperature and moisture entering the flaking press produce clean, uniform flakes without roller adhesion or throughput restriction.
Q: Can the line be reconfigured with different screw modules to switch between corn flakes and puffed snacks?
A: The co-rotating twin-screw extruder uses sectional modules that can be rearranged to change the functional zone layout. Switching from a flaking configuration to a direct-expansion puffed snack setup involves changing screw elements and the die plate. We document both configurations during commissioning so your operators can perform the changeover with the standard spare module set.