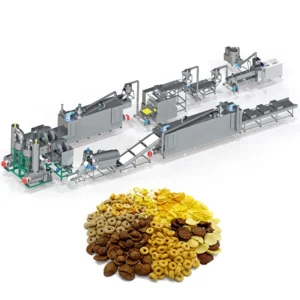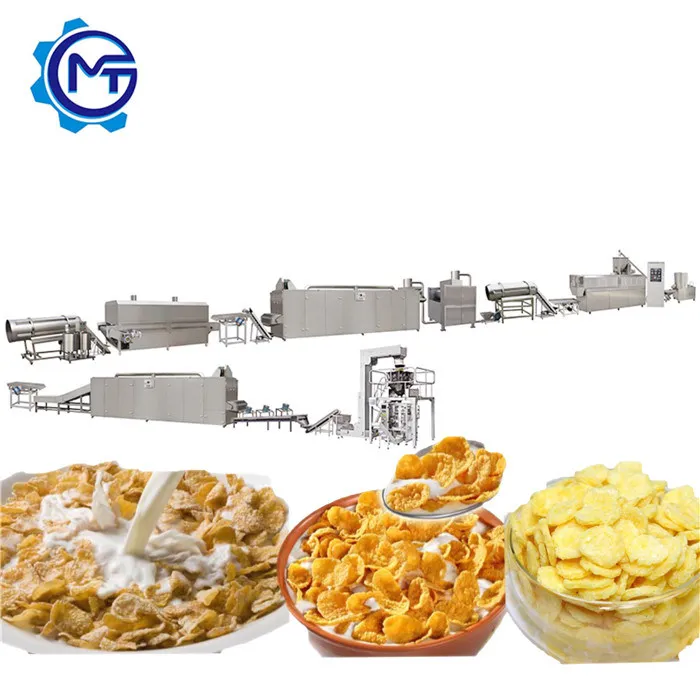
Screw configuration matched to formulation — every MT75 barrel zone and die land is selected after testing the buyer’s actual cereal blend, preventing flakes that sink or refuse to blister in the roaster.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Corn Flakes Processing Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material, moisture and product format) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC with MCC available |
| Flaking Drive | Double motors with hydraulic roller pressure |
| Flaking Temperature Control | Infrared sensor for even roller conditioning |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air with dual circulating fans and cyclone dust removal |
| Coating System | Double tumble sugar melter, elevator, coating drum, spray nozzle |
| Raw Materials | Corn, rice, wheat, oat, barley powders |
| Lubrication | Automatic lubricating and cooling |
| Screw Material | Wear-resistant special technology |
| Standards | CE, ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | De-germed corn grits, whole corn flour |
| Sugar-coated corn flakes | Corn or rice base with sugar syrup coating |
| Multi-grain breakfast cereals | Blends of wheat, oat, barley and rice |
| Shaped cereal pieces | Ball, tube, ring, star, flower, heart via extruder die |
What "300 kg/h" Means When Raw Material Changes
Output only holds when screw profile, moisture and barrel heat match the exact cereal blend running through the hopper.
I have watched lines rated at high capacity on fine corn flour drop noticeably when the buyer switches to de-germed corn grits on site. The starch granules in coarser grits need different shear and residence time to gelatinise fully. Without that adjustment, flakes leave the roaster hard instead of crisp, blistering never develops, and the whole batch drifts outside the density window the market expects [NEED_CITE: starch gelatinisation behaviour in coarse versus fine cereal fractions]. That is why capacity must always be tied to raw material specification, moisture content and target flake format.
Barrel Zoning and Starch Gelatinisation
The MT75 barrel is divided into independent heating zones, each set to a specific temperature. Early zones hydrate the cereal matrix, while mid-barrel zones push starch past its gelatinisation threshold under controlled shear. Getting this gradient right is the core of corn flakes extrusion technology twin screw operators depend on — too flat a profile and the dough exits undercooked, too steep and it burns at the die face.
Die Land Length and Flake Density Control
Die geometry determines how much the extrudate expands as it leaves the barrel. A shorter die land lets moisture flash off quickly, producing a lighter rope that flakes into a thinner, crisper sheet. A longer land restrains expansion, yielding a denser flake with longer bowl life. Matching die land to the target specification is where generic builds fail [NEED_CITE: die land length and expansion ratio in cereal extrusion].
Reading the Power and Dimension Data
The 210 kW installed power across the MT75 line covers extruder main drive, flaking hydraulics, dryer burners and roaster fans. Power consumption at 150 kW reflects typical running load once all stations reach steady state. The 45 m line length includes mixing, extrusion, flaking, drying, roasting, cooling and packing — each station spaced for maintenance access. PLC control coordinates roller speed, barrel temperature and dryer conveyor rate from one interface, so a recipe change propagates across the entire line without manual resets at each station.
When Flaking Pressure Drifts
Hydraulic roller pressure and infrared-monitored surface temperature keep flake thickness consistent across the full roller width. If pressure is uneven, one edge of the sheet comes out thinner than the other, roasting unevenly and creating a mix of over-browned and undercooked flakes in the same batch. Operators end up rejecting product that a well-tuned hydraulic circuit would have kept inside specification [NEED_CITE: hydraulic flaking roller uniformity in cereal sheeting].
Why the Extrusion Technology Angle Matters Here
Buying a corn flakes line on nameplate capacity alone leaves too many variables unresolved. The screw configuration, barrel temperature curve and die design must all respond to the specific cereal formulation the buyer intends to run. Lines configured this way produce consistent density, reliable blistering and predictable bowl life. Lines assembled from generic settings leave those outcomes to chance.
Why Source This Line From Meiteng
Complete throughput matching from batching to packing means the extruder output, flaker width, dryer belt speed and roaster volume are all calculated together rather than pulled from separate vendor catalogues. Screw and die combinations are specified after reviewing the buyer’s raw material data, not copied from a default build. Every MT75 line runs a trial on the customer’s actual cereal blend in the in-house testing workshop before crating. Pre-sales engineering covers layout, utility planning and voltage confirmation, so commissioning on site starts from a verified baseline rather than a guess.
Documentation & Verification
- Line layout drawing with station-by-station throughput calculation for your target capacity
- Screw and die configuration record matched to your specific cereal formulation
- Trial run report on your raw material produced in the testing workshop before shipment
- Electrical schematic with voltage and frequency confirmed for your destination market
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Wear parts list with reorder codes for screws, dies and roller sleeves
Installation, Commissioning & Support
- Foundation plan sized to the 45 m line footprint with anchor bolt schedule for extruder and flaker
- Dedicated power circuit rated for 210 kW installed load with MCC panel and PLC integration
- Extruder barrel segments and flaking rollers shipped assembled to reduce on-site build time
- First-run parameter logging covering barrel zones, roller gap and roaster temperature on your raw material
- Operator training on PLC recipe storage, hydraulic pressure adjustment and daily lubrication checks
- Spare screw elements and die plates stocked for dispatch within typical multi-week lead times
Before You Send an Inquiry
To configure the extrusion section properly, share your raw material type — corn grits, whole flour or multi-grain blend — along with target flake density and any sugar-coating requirement. Confirm your local voltage and frequency so the MCC and PLC panels are wound correctly before shipping. If you have existing upstream mixers or downstream packing equipment, provide their throughput data so the line can be balanced around them.
Frequently Asked Questions
Q: How is screw configuration and die design matched to a specific cereal raw material and target flake density?
A: We review the buyer’s particle size distribution, starch content and target moisture, then select screw element pitch, kneading block arrangement and die land length accordingly. The chosen configuration is validated during a trial run in the testing workshop, and adjustments are made before the extruder ships.
Q: What barrel temperature profile and moisture range produce optimal starch gelatinisation for corn flakes?
A: Typical profiles ramp from moderate heat in the feed zone to higher temperatures through the metering and die zones, with moisture held within a narrow band. Exact values depend on whether the raw material is fine flour or coarse grits, and are finalised during the pre-shipment trial run on the buyer’s actual blend.
Q: How is output capacity verified on the buyer’s actual raw material before shipment?
A: The buyer sends a representative batch of raw material to our testing workshop. We run the MT75 extruder on that material, measure throughput at steady state, check flake density and blistering after roasting, and document results in a trial run report shared before the order ships.
Q: What causes corn flakes to sink, lack blistering or fall outside target density?
A: These defects usually trace back to under-gelatinised starch from incorrect barrel temperature, insufficient shear or the wrong screw configuration for the particle size. Die land length may also be mismatched, allowing too much or too little expansion. Corrections are made at the extrusion stage, not downstream.
Q: How do flaking roller pressure, temperature uniformity and hydraulic control affect final flake thickness?
A: The hydraulic system maintains constant pressure across both rollers while the infrared sensor monitors surface temperature. Uneven pressure or hot spots produce variable thickness, leading to inconsistent roasting. The dual-motor drive allows independent roller speed fine-tuning to keep the sheet centred and uniform.