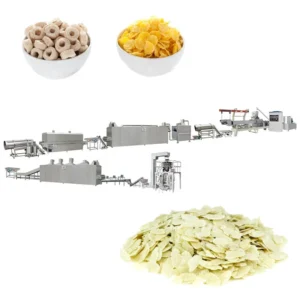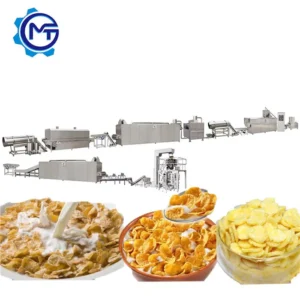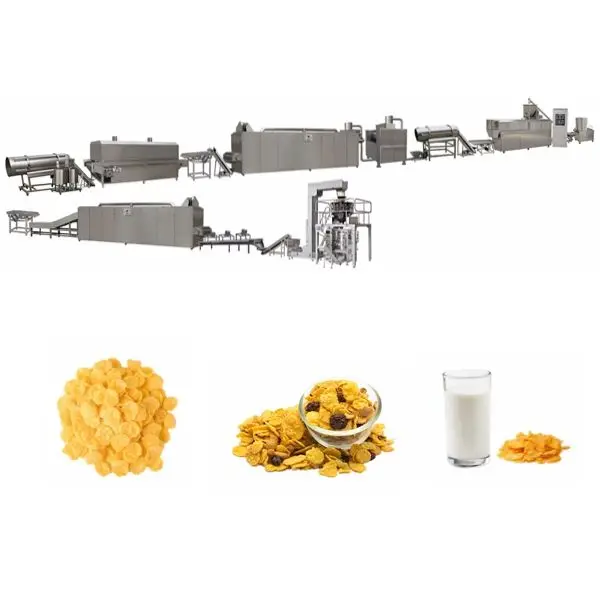
Customized screw and die configuration — Every MT75 line ships with a screw profile and die design matched to the buyer’s actual grain blend and target flake density, verified by an in-house trial run before dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Corn Flakes Extrusion Production Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW (MT75) |
| Power Consumption | 150 kW (MT75) |
| Output Capacity | 300–500 kg/h (basis to be confirmed) |
| Overall Dimensions | 45 × 1.5 × 3.5 m (MT75) |
| Control System | PLC (flaking machinery); MCC / PLC (extruder) |
| Flaking Drive | Double motors for separate roller driving; hydraulic system |
| Flaking Temperature Control | Infrared sensor |
| Dryer Heating Source | Gas or Electric (configurable) |
| Roasting Oven | Conciliation burner, twin circulating fans, cyclone dust removal, vibrating pan with high-temperature spraying tubes |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Extruder Working Principle | Feeding, extruding, cutting, heating, gearing, controlling systems |
| Assembly State | Complete line from batching to packing |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour blends |
| Sugar-coated corn flakes | Corn base with sugar syrup coating |
| Multi-grain breakfast cereals | Rice, wheat, oat, and barley powder blends |
| Shaped cereal variants | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart forms via die change |
Why Generic Screw Profiles Sabotage Corn Flake Density
Starch gelatinisation degree inside the barrel determines whether the final flake holds its bowl-life or turns to mush in milk — and that degree is set by the screw configuration, not the motor size.
When a corn flakes extrusion technology production line arrives with a screw profile copied from a generic build, the symptoms show up fast: flakes that shatter under their own weight, pellets that refuse to flatten evenly through the flaking rollers, or surface bubbles that never form during roasting. I saw this firsthand on a Southeast Asian project where the local corn flour carried a higher fat content than standard test material. The extruder ate inconsistently, expansion dropped, and the whole line sat idle until we flew out and reconfigured the screw combination on site. That kind of downtime is what drives the need for a trial run on the buyer’s actual raw material before the machine ever leaves the factory [NEED_CITE: impact of raw material fat content on twin-screw extrusion stability].
Barrel Temperature Profiling and Gelatinisation Control
The twin-screw barrel is divided into multiple heating zones, each set to a specific temperature that governs how completely the starch granules absorb moisture and rupture. For corn flakes extrusion technology production line applications, the target is a controlled partial gelatinisation — enough to bind the pellet together but not so much that the dough becomes sticky and blocks the flaking rollers downstream. The PLC system on the MT75 allows operators to adjust each zone independently, matching the profile to the grain blend’s moisture content and starch composition.
Die Geometry and the Flaking Interface
The die at the extruder outlet shapes the cooked dough into a continuous ribbon or discrete pellets that feed directly into the hydraulic flaking rollers. Die aperture, land length, and face configuration together determine the initial thickness and surface texture of the extrudate — variables that directly influence how evenly the flaking rollers compress the material. On the MT75, die design is specified against the buyer’s target flake thickness and the roller gap range of the hydraulic flaking unit, so the two stations work in register rather than fighting each other.
Reading the Specs That Matter for Flake Quality
The MT75’s installed power of 210 kW and power consumption of 150 kW reflect a twin-screw configuration sized for continuous cereal duty — not a repurposed snack extruder pushed beyond its thermal envelope. The hydraulic flaking station uses independent double-motor drive, meaning each roller can be speed-matched to compensate for uneven feed, while the infrared sensor monitors roller surface temperature in real time to keep flake thickness consistent across the full web width. In the roasting oven, the conciliation burner paired with two separate circulating fans and a cyclone dust removal device maintains a uniform air temperature, which is what generates the signature surface bubbles and crispness that buyers expect in a premium breakfast cereal. The vibrating pan with high-temperature spraying tubes adds a final drying pass that locks in bowl-life without scorching. For sugar-coated variants, the double tumble system — melting unit, elevator, coating drum, and spraying nozzle — applies syrup in controlled layers so that coating weight stays within specification from the first kilogram to the last [NEED_CITE: relationship between roasting oven air uniformity and cereal surface bubble formation].
The Hidden Cost of Skipping a Raw-Material Trial Run
A line that performs perfectly on standard corn grits in the factory can behave entirely differently on the buyer’s local grain. Without a pre-shipment trial, the first indication of a mismatch is a production floor full of off-spec flakes — too dense, too thin, or too fragile to survive packing. By that point, the cost includes not just wasted raw material and lost production time but also the logistics of flying a service engineer overseas to reconfigure screws, adjust barrel temperatures, and re-tune the flaking roller gap from scratch. The downtime compounds when downstream stations like the roasting oven and coating drum were sized for a throughput the extruder can no longer deliver [NEED_CITE: cost of unplanned commissioning visits for extrusion line reconfiguration].
Why Sourcing This Line From Meiteng Works
The MT75 is built as a complete corn flakes extrusion technology production line from mixing through packing, which means throughput at every station — extruder, flaker, dryer, roaster, coater — is calculated together rather than assembled from separate vendors who each quote their own nominal capacity. Screw configuration and die design are specified to the buyer’s raw material formulation, not pulled from a generic catalog. Every line undergoes a trial run in the in-house testing workshop using the customer’s actual grain blend, producing a documented report before shipment. The PLC and MCC control architecture is configured to the buyer’s voltage, frequency, and preferred operating language, so commissioning starts with parameter verification rather than electrical rewiring. Wear parts — screws, dies, roller shells — are cataloged and available from the first day of production, eliminating the scramble for replacements when the initial set reaches end of life.
Documentation & Verification
- Line layout and capacity calculation showing station-by-station throughput matching
- Screw and die configuration record tied to your grain blend formulation
- Electrical schematic with confirmed voltage, frequency, and control language
- Trial run report produced on your raw material in our testing workshop
- CE declaration of conformity and ISO certificate for market entry
- Operation and maintenance manual with wear parts replacement schedule
Installation, Commissioning & Support
- Foundation plan accounts for the 45 m line length and flaking station vibration isolation
- Dedicated power circuit sized for 210 kW installed load with local voltage confirmation
- Extruder, flaker, dryer, and roaster arrive as pre-assembled modules for sequential positioning
- PLC parameter upload and barrel zone calibration completed during first production run
- Operator training covers screw combination changes for different grain blends and die swaps
- Wear parts list with reorder intervals for screws, dies, and flaking roller shells
What We Need to Configure Your Line
To prepare a line layout and screw specification, we need your target flake type — natural or sugar-coated — along with the grain blend formulation and any local raw material characteristics such as fat content or moisture range. Share your factory floor dimensions, ceiling height, and the local voltage and frequency standard so that the electrical package is built correctly from the start. If you have existing upstream milling or downstream packing equipment, let us know the interface points so the line throughput is balanced end to end.
Frequently Asked Questions
Q: How is screw configuration selected for different grain blends and target flake densities?
A: We start with your raw material data sheet — grain type, particle size, fat and moisture content — then map the required starch gelatinisation degree to a specific screw element sequence and compression ratio. The die aperture is matched to the hydraulic flaking roller gap so the extrudate enters the flaker at the correct thickness. A trial run on your actual grain confirms the configuration before shipment.
Q: What barrel temperature profile and moisture range produce optimal starch gelatinisation for corn flakes?
A: Corn flakes need a partial gelatinisation that binds the pellet without making the dough too sticky for flaking. The MT75’s multi-zone barrel heaters and PLC control allow each zone to be tuned independently. Typical conditioning moisture is adjusted at the mixing station, and the exact profile is finalised during the in-house trial run on your specific grain blend.
Q: How is throughput capacity verified on the buyer’s actual raw material before shipment?
A: We run a documented trial in our testing workshop using your grain formulation at your target flake thickness. The report records extruder amperage, barrel temperatures, flaking roller pressure, and output weight over a sustained period. This confirms that every station — from mixer to roaster — can sustain the quoted rate without bottlenecking.
Q: What is the relationship between extruder die design, flake thickness, and final roasting behaviour?
A: The die determines the extrudate cross-section entering the flaking rollers, which in turn sets the flake thickness. Thicker flakes require longer roasting dwell time and higher air volume to develop surface bubbles and achieve the target crispness. Die land length and aperture are specified together with the roasting oven’s fan speed and burner setting to balance these variables.
Q: How are voltage, control language, and PLC parameters confirmed before commissioning?
A: During the specification stage we collect your local voltage, frequency, and preferred HMI language. The electrical schematic and PLC program are built to those values and verified during the factory test. When the line arrives on site, commissioning starts with parameter validation rather than rewiring or reprogramming from scratch.