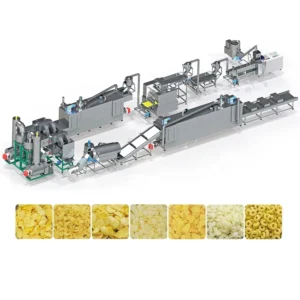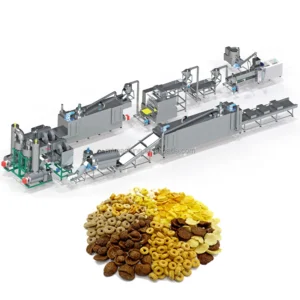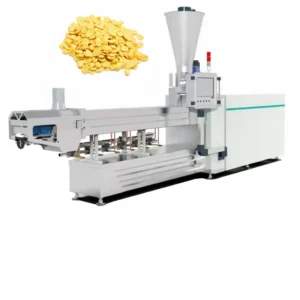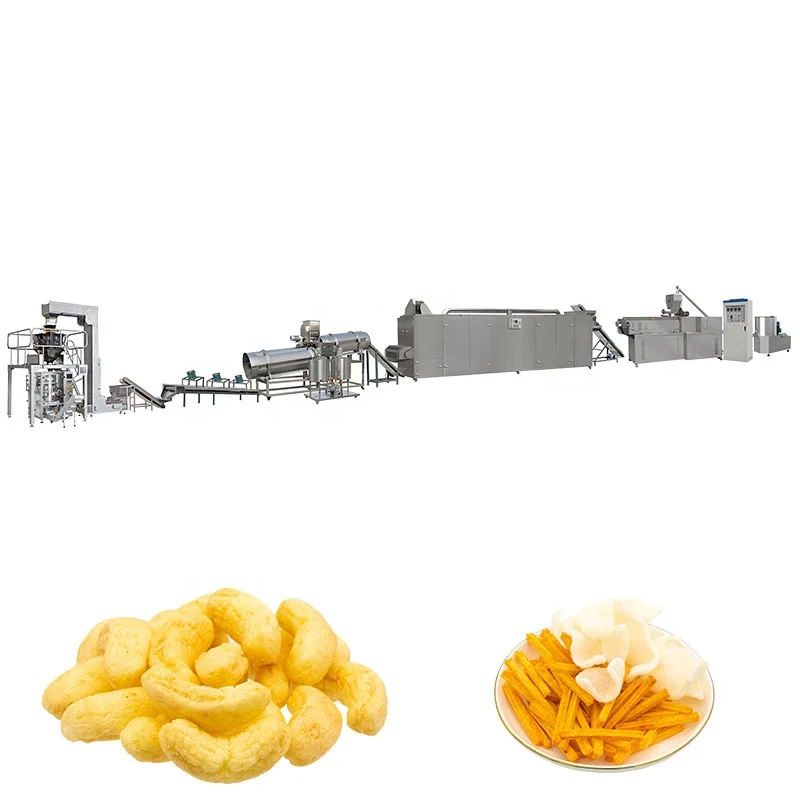
Matched screw profiles — configuration is built around your specific grain blend and target flake density, not copied from a generic catalog.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Production Line (Twin-Screw Extrusion System) |
| Extruder Type | Twin Screw |
| Installed Power (MT70 / MT85 / MT75) | 160 kW / 190 kW / 210 kW |
| Power Consumption (MT70 / MT85 / MT75) | 120 kW / 140 kW / 150 kW |
| Output Capacity (MT70) | 150–200 kg/h (basis not stated in source — confirm raw material, moisture content, and product format) |
| Output Capacity (MT85) | 300–400 kg/h (basis not stated in source — confirm raw material, moisture content, and product format) |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material, moisture content, and product format) |
| Overall Dimensions (MT70 / MT85 / MT75) | 41 × 1.5 × 2.2 m / 43 × 1.5 × 3.2 m / 45 × 1.5 × 3.5 m |
| Control System | PLC and MCC |
| Screw Configuration | Matched to raw material and target product |
| Flaking Machinery Drive | Double motors for separate roller driving; hydraulic system for double rollers |
| Flaking Temperature Control | Infrared sensor |
| Dryer Heating Source | Gas / Electric |
| Roasting Oven | Hot air roasting with vibrating pan, high-temperature spraying tubes, two separate circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Lubrication | Automatic lubricating system on extruder |
| Cooling | Integrated cooling function on extruder |
| Assembly State | Complete turnkey line |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal packs | Corn grits, corn flour |
| Sugar-coated corn flakes | Corn base with sugar coating drum finish |
| Multi-grain breakfast cereals | Rice, wheat, oat, barley powder blends |
| Puffed snack shapes on same extrusion platform | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart via adjustable die |
| Small-to-medium cereal manufacturer scale-up | Production volumes from pilot batches to continuous commercial runs |
What "Rated Capacity" Actually Means for Corn Flake Extrusion
A line is only as fast as its slowest matched station — and the extruder screw profile decides whether the downstream flaking and roasting stages can deliver the crispness your market expects.
When a buyer receives a capacity number without knowing which grain formulation, moisture level, and flake thickness it was measured on, that figure becomes a liability. I have watched lines arrive on site where the extruder could push the nominal throughput, but the flakes came out dense and chewy because the screw configuration was a generic build never adjusted for the buyer’s actual high-fiber or multi-grain recipe. The starch gelatinisation window shifted, the flaking rollers could not produce an even sheet, and the roasting oven could not blister the surface properly. Reconfiguring the screw elements after installation costs weeks of lost production and raw material waste [NEED_CITE: starch gelatinisation temperature ranges for cereal grains].
How Barrel Temperature Profiling Shapes the Flake
The barrel on a twin-screw extruder is divided into multiple heating and cooling zones. Each zone controls a different stage of the starch transformation — from initial hydration through gelatinisation to the final melt temperature at the die. For corn flakes, the corn flakes extrusion technology twin screw process demands a precise temperature ramp so that starch granules swell uniformly without over-shearing. If zone three runs too hot, the dough becomes sticky and the flakes clump after flaking; too cool, and the granules remain partially crystalline, producing a hard, glassy bite after roasting.
Screw Element Sequencing and Shear Balance
Beyond temperature, the arrangement of conveying, kneading, and reverse-flight screw elements determines how much mechanical shear the dough receives. High-fiber blends with oat or barley require a different kneading block sequence than pure corn grits because fiber interrupts the starch matrix and changes how the material flows through the barrel. Getting this sequencing right is what separates a flake that blisters evenly in the hot air roasting oven from one that stays flat and dense. The screw configuration is therefore not a fixed catalog part — it is an engineered variable that must respond to the buyer’s raw material spec [NEED_CITE: twin-screw element geometry and food extrusion].
Reading the Specs That Matter
The installed power across the three models — 160 kW, 190 kW, and 210 kW — reflects the torque available to push viscous cereal dough through the barrel at different throughputs. Power consumption figures (120 kW, 140 kW, 150 kW) indicate typical running load under matched conditions, which is what actually shows up on the electricity meter. The flaking station uses hydraulic double rollers with independent motor drives and an infrared sensor for temperature feedback, meaning roller gap and surface heat are managed separately to hold flake thickness within a tight band. The roasting oven employs two circulating fans and a cyclone dust removal device so that hot air distribution stays even across the vibrating pan — an arrangement that directly affects whether every flake blisters uniformly or only the ones near the air inlet do.
When the Wrong Screw Configuration Ships With the Line
A generic screw build might produce acceptable flakes on standard corn grits during a factory test, but the moment the buyer switches to a multi-grain or reduced-sugar formulation, the extrusion behavior changes completely. Flakes come out thicker on one side, the roasting oven cannot compensate, and the final pack fails the crunch test that retailers require. The cost is not just scrap material — it is the downtime while replacement screw elements are sourced, shipped, and tested on site [NEED_CITE: extrusion process deviation costs in cereal manufacturing].
Engineering the Line Around Your Material
Every MT corn flakes line starts with the buyer’s raw material sample and target product specification. The screw configuration and die design are specified to that formulation rather than pulled from a standard build list. Before shipment, the line runs a trial in the in-house testing workshop using the buyer’s actual grain blend, producing real flakes that can be measured for thickness, density, and roast response. This trial run generates a documented report so the buyer sees — and approves — the product before the machine leaves the factory floor. The PLC and MCC control system is configured to the buyer’s local voltage and frequency, with the interface language confirmed in advance so that commissioning on site starts with parameters that already match the validated recipe.
Documentation & Verification
- Screw and die configuration record matched to your grain formulation
- Trial run report on your raw material produced in the testing workshop before dispatch
- Electrical schematic with voltage and frequency confirmed to your local supply
- Line layout drawing showing throughput matching across every station from mixer to packer
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Operation and maintenance manual with wear parts list for screws, dies, and roller surfaces
Installation, Commissioning & Support
- Foundation plan accounts for line lengths up to 45 m and the roasting oven’s gas supply requirements
- Dedicated electrical circuits sized to the confirmed installed power draw, up to 210 kW for the MT75 model
- PLC and MCC panels pre-wired and labeled in the agreed language before crating
- First-run commissioning includes screw profile fine-tuning on your actual raw material on site
- Operator training covers barrel zone temperature adjustment and flaking roller gap calibration
- Wear parts inventory recommendation covers screw elements, die plates, and flaking roller sleeves
What to Include in Your Inquiry
To receive a line configuration and layout proposal, provide your primary grain types and any secondary ingredients, along with the target flake dimensions and whether sugar coating is required. Specify your available workshop length and ceiling height so the layout can be drafted to fit. Include your local voltage, frequency, and preferred control language to avoid rework at the electrical stage. If you are running a new formulation, sending a raw material sample enables a pre-shipment trial run to validate the screw configuration against your exact recipe.
Frequently Asked Questions
Q: How is the screw configuration matched to my specific grain blend?
A: The screw element sequence — conveying, kneading, and reverse-flight sections — is designed around your raw material’s starch content, fiber level, and target flake density. We run your actual grain sample in our testing workshop before shipment and document the configuration that produces the correct gelatinisation and expansion for your product spec.
Q: Can the line produce both natural and sugar-coated corn flakes?
A: Yes. The coating section includes a double tumble sugar melting system, elevator, coating drum, and spraying nozzle. Switching between natural and coated production involves activating or bypassing the coating and secondary drying stages, which the PLC program manages as separate recipe routines.
Q: What does the trial run report include?
A: The report documents the screw configuration used, barrel temperature profile, moisture injection rate, flake thickness measurements, and visual assessment of blister uniformity after roasting. It is generated from a production run on your raw material in the testing workshop before the line ships.
Q: How does the flaking station maintain consistent flake thickness?
A: The flaking unit uses hydraulic double rollers driven by independent motors, with an infrared sensor monitoring roller surface temperature. Roller gap and temperature are controlled separately, keeping flake thickness within a narrow tolerance across the full production run.
Q: What electrical information do I need to confirm before production?
A: We require your site voltage, frequency, and phase specification along with the preferred language for the PLC and MCC interface. This is confirmed before production begins so that all electrical panels, motor ratings, and control labels match your local supply and operator requirements upon arrival.