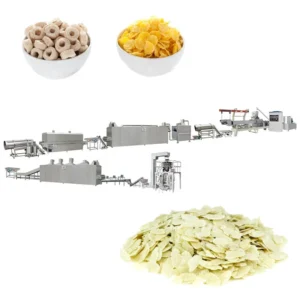
Extrusion Geometry Matched to Grain — screw configuration, die design and barrel temperature profile are specified to your corn, rice or oat formulation, ensuring starch gelatinisation and expansion behave predictably across every batch rather than relying on a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Extruder Production Line |
| Screw Type | Twin-screw |
| Installed Power | MT70 160 kW / MT85 190 kW / MT75 210 kW |
| Power Consumption | MT70 120 kW / MT85 140 kW / MT75 150 kW |
| Output Capacity | MT70 150–200 kg/h / MT85 300–400 kg/h / MT75 300–500 kg/h (basis not stated in source — confirm raw material, moisture, flake size) |
| Overall Dimensions | MT70 41 × 1.5 × 2.2 m / MT85 43 × 1.5 × 3.2 m / MT75 45 × 1.5 × 3.5 m |
| Control System | PLC and MCC |
| Flaking Station | Hydraulic double rollers, independent motor drives, infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Production Procedure | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Coating → Drying → Cooling → Packing |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for retail breakfast cereal market | Corn grits or corn flour |
| Sugar-coated breakfast flakes | Corn, rice, wheat or multi-grain blends with sugar glaze |
| Flaked cereal from alternative grains | Rice, oat or barley powder formulations |
| Varied extruded shapes before flaking | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart via die changes |
Why "Rated Capacity" Misses the Real Picture on a Corn Flakes Extrusion Production Line Turnkey
Capacity only matters if it holds on your actual grain formulation at your target moisture and flake thickness.
I have watched lines rated at a clean number on standard corn grits collapse the moment the buyer switched to a locally sourced corn flour with different starch content and particle size. The extruder ran, but expansion dropped, the flaker crushed rather than flattened, and roasting produced uneven blistering. The rated throughput was technically achievable — just not on the material the buyer actually intended to use. A corn flakes extrusion production line turnkey must be validated against your specific raw material, not a laboratory reference [NEED_CITE: grain formulation variability in extrusion processing].
Screw Configuration and Barrel Temperature for Starch Gelatinisation
The twin-screw extruder is where your corn flakes begin to take shape at a molecular level. Screw element sequencing — conveying, kneading, and reverse-flight sections — controls residence time and shear intensity, which directly govern how thoroughly starch granules absorb moisture and gelatinise under heat. A corn flakes extrusion production line turnkey configured for high-amylose corn will use a different screw profile than one designed for waxy rice or oat flour. Barrel temperature zones are set in tandem, moving from preconditioning heat near the feed zone to peak gelatinisation temperature before the die.
Die Geometry and Expansion Control Before the Flaker
The die plate determines the cross-section of the extrudate — the rope or pellet that enters the flaking rolls. Die land length, orifice diameter and the number of ports all affect how the material expands as it exits the pressurised barrel into ambient conditions. Too much expansion and the flaker cannot compress the pellet into a dense, crisp flake; too little and the final product lacks the surface blistering consumers expect after roasting. Getting this balance right requires iterative adjustment on the actual formulation, not a theoretical calculation [NEED_CITE: die design parameters for flaked cereal extrusion].
Reading the Specs That Actually Shape Your Output
Installed power across the MT70, MT85 and MT75 models scales from 160 kW to 210 kW, but the number that matters more on the floor is power consumption — 120 kW, 140 kW and 150 kW respectively — because that reflects what the extruder and line draw under normal running conditions and determines your electrical infrastructure requirements. The hydraulic flaking station uses independent motors for each roller, which allows the gap and pressure to be adjusted asymmetrically when pellet size distribution varies across the die face. Infrared sensor temperature control on the flaker monitors roller surface heat in real time, preventing the sticking and tearing that occurs when cold rollers meet hot extrudate. The hot air roasting oven runs a conciliation burner with dual circulating fans, creating the even airflow required for uniform surface blistering without scorching one side of the belt while the other side remains underdone.
What Happens When Stations Are Not Throughput-Matched
An extruder running at full output feeds a dryer that cannot remove moisture fast enough, so flakes arrive at the roaster still too wet to blister properly. Or the coating drum receives more volume than the sugar spray system can distribute evenly, leaving some flakes over-glazed and others bare. These mismatches do not show up in a spec sheet that lists each machine’s individual rating. They surface during the first production run, when the buyer discovers that the bottleneck is not the extruder but a downstream station that was sized independently. Fixing it after installation means either replacing equipment or accepting a line that never reaches its intended output [NEED_CITE: throughput balancing in multi-station food processing lines].
Why Sourcing the Full Line From One Build Matters Here
Every station on this corn flakes line — from the batching mixer through the extruder, flaker, dryer, roaster and coater — is sized against the same throughput target, so material flow remains consistent from infeed to packing. The screw configuration and die design are locked to your grain formulation and target flake density before the extruder is assembled, rather than pulled from a generic template. Before shipment, the line runs a trial in the in-house testing workshop using your actual raw material, generating a documented parameter set that becomes your baseline recipe. The PLC and MCC control architecture coordinates speed and temperature references across all stations from a single interface, so an adjustment at the extruder automatically propagates to the flaker and dryer setpoints. Electrical schematics confirm voltage, frequency and control language before production starts, removing the commissioning delays that occur when a control panel arrives speaking the wrong language.
Documentation & Verification
- Line layout and capacity calculation showing throughput at every station
- Screw and die configuration record matched to your grain formulation
- Trial run report on your actual raw material before dispatch
- Electrical schematic with voltage and frequency confirmed for your market
- Operation and maintenance manual covering all stations in the line
- Wear parts list for screws, dies, rollers and spray nozzles
Installation, Commissioning & Support
- Foundation plan accounts for line length from 41 m to 45 m depending on model
- Electrical room must supply dedicated circuits matching 120–150 kW running load
- Extruder barrel sections and flaking rollers ship separated for site assembly
- First-run parameter tuning uses your grain formulation to set screw speed and barrel zones
- PLC and MCC interface language confirmed before operator training begins
- Wear parts package includes twin-screw elements, die plates and flaker roller sleeves
What We Need to Configure Your Line
To move from a general inquiry to a specific line layout, we need your target grain formulation — corn, rice, wheat, oat or a blend — along with the moisture content and particle size of the flour or grits you source locally. Tell us the daily output you plan to run and the number of shifts, so we can select the correct model and match downstream station capacity. We also need your facility voltage and frequency, plus the preferred control panel language, to ensure the PLC and MCC system arrives ready for your electricians.
Frequently Asked Questions
Q: How is the line capacity verified on my specific corn or grain formulation?
A: Before the line ships, we run your actual raw material through the extruder, flaker, dryer and roaster in our in-house testing workshop. We document screw speed, barrel temperature profile, flaking pressure and roasting time at each throughput level, producing a trial run report that confirms what output your formulation supports.
Q: How do you determine screw configuration and die design for my target flake density?
A: We start with your grain type, starch content and target flake thickness, then select screw element sequencing and die orifice geometry accordingly. The combination is tested during the in-house trial run, and the final configuration record is documented and shipped with the machine.
Q: What happens during the in-house trial run before the line ships?
A: We feed your raw material through the full extrusion, flaking, drying and roasting sequence, adjusting parameters until flake density, surface blistering and crispness meet your specification. You receive a trial run report with the validated parameter set.
Q: How are voltage, frequency and control language confirmed before production?
A: During the specification confirmation stage, we collect your facility electrical standards and operator language preference. The electrical schematic and PLC interface are built to those requirements, avoiding commissioning delays caused by mismatched control panels.
Q: How do you ensure downstream stations match the extruder output?
A: Every station — flaker, dryer, roaster and coater — is sized against the same throughput calculation as the extruder. The line layout document shows material flow rates at each station, so no single unit bottlenecks the corn flakes extrusion production line turnkey.