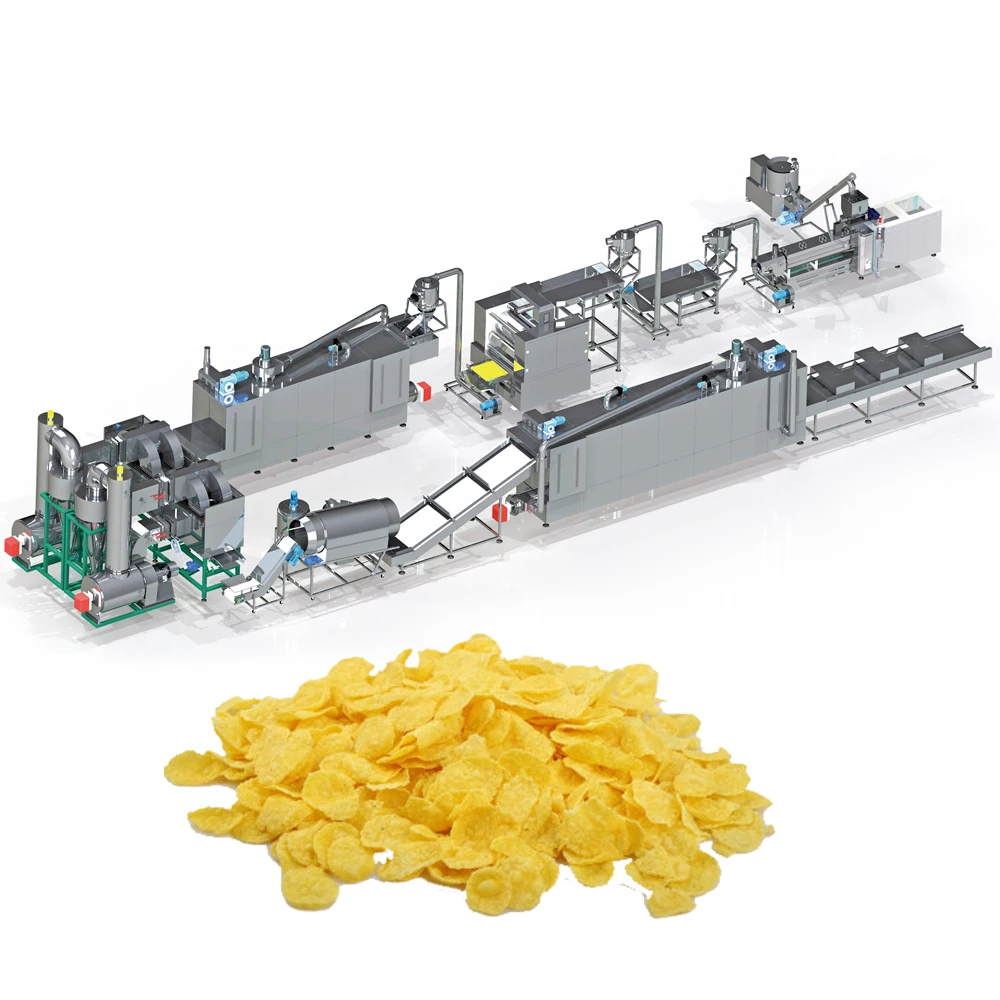
Screw Configuration Matched to Your Raw Material — Corn flake density and crunch are defined in the extruder barrel, and our twin-screw setup is dialed in through an in-house trial run on the buyer’s actual formulation before any machine ships.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line (Twin-Screw Extrusion Line) |
| Available Extruder Models | MT70 / MT85 / MT75 |
| Screw Configuration | Twin-screw with wear-resistant material |
| Installed Power | 160 kW (MT70) / 190 kW (MT85) / 210 kW (MT75) |
| Power Consumption | 120 kW (MT70) / 140 kW (MT85) / 150 kW (MT75) |
| Throughput Capacity | 150–200 kg/h (MT70) / 300–400 kg/h (MT85) / 300–500 kg/h (MT75) (basis not stated in source — confirm raw material, moisture content, and flake thickness) |
| Overall Dimensions | 41 × 1.5 × 2.2 m (MT70) / 43 × 1.5 × 3.2 m (MT85) / 45 × 1.5 × 3.5 m (MT75) |
| Control System | PLC control with MCC integration |
| Flaking Station | Hydraulic double rollers, separate motor drive, infrared sensor temperature control |
| Roasting Oven | Hot air roasting, dual circulating fans, conciliation burner, cyclone dust removal |
| Dryer Heating Source | Configurable for gas or electric supply |
| Coating System | Double tumble drum, elevator, coating drum, spraying nozzle (for sugar-coated variants) |
| Screw Lubrication | Automatic lubricating and cooling function |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn grits, rice, wheat, oat, and barley powder blends |
| Sugar-coated breakfast cereal | Corn-based extrudates with sugar syrup coating |
| Shaped cereal formats (rings, balls, loops, stars) | Corn, rice, and multigrain formulations via die exchange |
What "Nominal Output" Leaves Out About Corn Flake Density
A line is only as fast as the slowest station handling your specific raw material.
I remember a commissioning job a few years back where a buyer received their corn flakes extrusion production line turnkey, installed it, and ran their local corn blend. The flakes came out thick, hard, and nothing like the samples they approved. The line sat idle for weeks while we reconfigured the screw elements and die to match their actual starch content and moisture profile [NEED_CITE: raw material variability in breakfast cereal processing]. Nominal throughput numbers on a spec sheet mean very little if the material behaves differently than what was tested at the factory. The extruder might push the volume, but if the flaking rollers cannot press the sheet to the right thickness or the roasting oven cannot dry it evenly, the whole line backs up.
How Screw Profile Dictates Flake Texture
The twin-screw configuration is where starch gelatinisation actually happens. By adjusting the arrangement of conveying elements, kneading blocks, and reverse-flight sections inside the barrel, the residence time and shear intensity change directly. A higher-shear profile generates more expansion at the die, producing a lighter, more porous pellet that flakes into a thinner, crispier sheet. For denser corn varieties with lower starch content, a gentler profile with longer residence time ensures complete gelatinisation without burning the material at the barrel wall. This is not a one-setting operation — every formulation demands its own screw map.
Die Geometry and the Cut That Shapes the Pellet
The die plate sits at the discharge end of the extruder and defines the cross-section of the extrudate before the rotary cutter slices it into pellets. For corn flakes, the die orifice must produce a pellet that, once flaked, delivers the correct surface area-to-thickness ratio. Too thick and the roasting oven cannot drive off moisture fast enough, leaving a chewy centre. Too thin and the flakes shatter during conveying and packing. Die design also governs how the starch matrix sets during cooling — which is why the same corn flakes extrusion production line turnkey can switch to rings, balls, or fruit loops simply by swapping the die plate and adjusting the cutter speed.
Interpreting the Power and Capacity Figures
The installed power range across the three extruder models — 160 kW to 210 kW — reflects motor sizing for different barrel volumes and screw diameters. Power consumption figures are lower because the main drive motor rarely operates at full load during steady-state extrusion; the surplus capacity handles startup torque and variations in feed density [NEED_CITE: twin-screw extruder motor loading characteristics]. The throughput capacities listed carry a caveat: they depend on raw material type, incoming moisture, and target flake thickness. A line processing high-fat corn meal at a thick flake spec will run slower than one producing thin flakes from a lean, dry formulation. Always confirm the basis before sizing downstream equipment.
When a Mismatched Dryer Becomes the Bottleneck
An extruder pushing material faster than the dryer can handle creates a backlog of wet pellets that stick together and jam the flaking rollers. The downstream stations — the hydraulic flaking unit, the hot air roasting oven with its dual circulating fans, and the cooling conveyor — must all be sized to absorb the extruder’s actual output on the buyer’s material [NEED_CITE: throughput balancing in breakfast cereal lines]. A sugar-coated variant adds even more stages: sugar melting drums, a spraying nozzle array, a coating drum, and a second drying pass. If any one of these stations undershoots, the whole line throttles down to match the slowest link.
Why Sourcing from One Supplier Matters
The complete line from mixing through packing is engineered under one roof, which means throughput calculations are done holistically rather than station by station. The screw and die configuration is specified to the buyer’s formulation, not copied from a generic build. Every corn flakes extrusion production line turnkey we ship goes through a trial run in our testing workshop using the customer’s own raw material, producing actual flakes that get measured for density, thickness, and moisture content before the crate is sealed. The flaking rollers use hydraulic pressure with infrared temperature feedback to hold uniform sheet thickness. The roasting oven features a vibrating pan with high-temperature spraying tubes and cyclone dust removal, keeping the work environment clean.
Documentation & Verification
- Line layout drawing scaled to your factory footprint with utility connection points marked
- Screw and die configuration record tied to your specific corn blend and target flake thickness
- Trial run report showing flake density, moisture, and dimensional data from your raw material
- Electrical schematic with voltage, frequency, and PLC language confirmed for your destination market
- Operation and maintenance manual covering hydraulic flaking roller service intervals
Installation, Commissioning & Support
- Foundation plan provided for the extruder footprint (up to 45 m line length) with load-bearing specs
- Three-phase power supply sizing matched to the selected model’s installed power (160–210 kW)
- Extruder barrel and screw assembly completed on-site with alignment verification
- Hydraulic flaking roller pressure and infrared sensor calibration during first production run
- PLC parameter sets loaded for your specific raw material and target flake format
- Wear parts inventory list covering screw elements, die plates, and flaking roller surfaces
What We Need to Configure Your Line
Send us your raw material specification — corn variety, particle size, starch and moisture content — along with your target flake dimensions and daily production volume. Confirm your workshop dimensions so we can draft the line layout, and specify the local voltage and frequency so the MCC and PLC are built to match. If you can ship a sample batch of your material to our testing workshop, we will run a trial and return the data before you commit to the build.
Frequently Asked Questions
Q: How is line capacity verified before the equipment ships?
A: We conduct a trial run in our testing workshop using the buyer’s actual raw material. The run measures extruder throughput, flake thickness, moisture content after drying, and roasting oven cycle time under real conditions. A trial run report with these data points is provided before shipment, so the quoted capacity is tied to your specific formulation rather than a generic benchmark.
Q: How do you match screw configuration to my corn blend?
A: Each corn variety has a different starch-to-fibre ratio and gelatinisation temperature. We select conveying elements, kneading blocks, and reverse-flight sections to control shear intensity and residence time inside the barrel. The die orifice is then sized to produce a pellet that flakes to your target thickness without cracking or remaining undercooked at the centre.
Q: Can the same line produce both natural and sugar-coated corn flakes?
A: Yes. The natural corn flakes line runs through mixing, extruding, flaking, drying, roasting, cooling, and packing. Adding sugar-coated variants inserts a sugar melting drum, spraying nozzle, and coating drum after roasting, followed by a second drying pass. Both configurations share the same extrusion and flaking platform.
Q: When should voltage and control language be confirmed?
A: These must be locked in before production begins. The PLC interface language, MCC component ratings, and motor winding specifications are all built to the target market’s electrical standard. Changing them after assembly requires rewiring and reprogramming that delays commissioning on-site.
Q: What does the trial run report include?
A: The report documents raw material input weight, moisture content, extruder barrel temperature profile, screw speed, die pressure, flake dimensions, moisture after each drying stage, and final product bulk density. Photographs of the extrudate and finished flakes are included so the buyer can evaluate texture and colour before approving the build.