
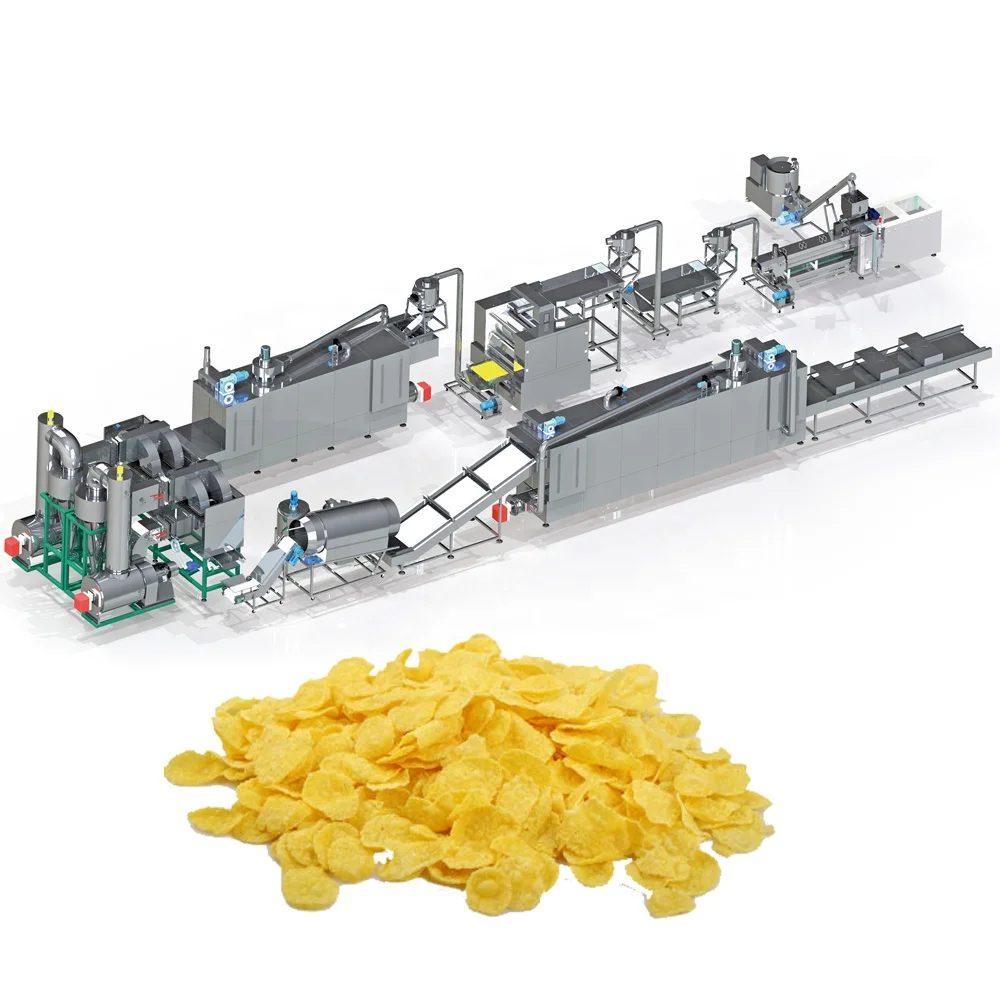
Engineered screw and barrel profiles — every MT70, MT85 and MT75 configuration is built around the buyer’s corn variety and target flake density rather than a generic twin-screw template.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Making Machine / Breakfast Cereals Processing Line |
| Model | MT70 / MT85 / MT75 |
| Screw Type | Twin Screw |
| Installed Power | MT70 — 160 kW; MT85 — 190 kW; MT75 — 210 kW |
| Power Consumption | MT70 — 120 kW; MT85 — 140 kW; MT75 — 150 kW |
| Output Capacity | MT70 — 150–200 kg/h; MT85 — 300–400 kg/h; MT75 — 300–500 kg/h (basis not stated in source — confirm raw material, moisture content and product format) |
| Voltage | 380V / 220V (frequency to be confirmed — 50 Hz or 60 Hz) |
| Overall Dimensions | MT70 — 41 × 1.5 × 2.2 m; MT85 — 43 × 1.5 × 3.2 m; MT75 — 45 × 1.5 × 3.5 m |
| Weight | Approximately 5,000 kg (full line weight to be verified against final configuration) |
| Control System | Available with PLC or MCC control |
| Contact Material | Stainless Steel |
| Heating Source (Dryer) | Gas or Electric |
| Line Stations | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Cooling → Packing (natural line); additional Sugar Spraying → Sugar Coating → Drying stations for coated line |
| Flaking Machinery | Hydraulic double-roller system, dual motors for separate roller drive, infrared temperature monitoring |
| Hot Air Roasting Oven | Vibrating pan, conciliation burner combustion chamber, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melter, elevator, coating drum, spraying nozzle |
| Warranty | 1 Year |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn flour or corn grits, plain and toasted |
| Sugar-coated corn flakes | Corn base with sugar spray and tumble coating |
| Multi-grain breakfast cereals | Powder blends of corn, rice, wheat, oat, barley |
| Shaped cereal formats | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (by die change) |
Why Generic Screw Builds Sink Your Corn Flake Line
A corn flakes extrusion machine screw configuration barrel temperature profile copied from a standard drawing will produce flakes that are either too dense for a satisfying bowl-life or too fragile to survive packing and transport. Matching the screw elements and die geometry to the buyer’s exact corn variety, particle size and moisture content is the single most important step before steel is cut.
I have seen lines arrive on site only to discover the customer’s corn flour was coarser than the supplier assumed. The result was uneven gelatinisation through the barrel zones, inconsistent expansion at the die face, and a flaking roller that could not hold uniform thickness. Two weeks of re-commissioning followed. [NEED_CITE: starch gelatinisation behaviour across corn varieties and particle size distributions]
Screw and Die Engineering for Flake Consistency
The twin-screw extruder at the heart of this line uses interchangeable screw elements arranged in zones that control shear, residence time and melt temperature. For natural corn flakes, the corn flakes extrusion machine screw configuration barrel temperature profile must deliver partial gelatinisation — enough to bind the pellet but not so much that the starch fully expands before it reaches the flaking rollers.
Barrel Zone Control and Moisture Management
Barrel sections are independently heated and cooled, allowing the operator to build a temperature ramp that matches the starch behaviour of the specific corn or multi-grain blend in use. Moisture injection points along the barrel let the process engineer fine-tune water activity, which directly governs how much expansion occurs at the die. Too little moisture and the pellet exits hard and glassy; too much and the pellet swells prematurely, leaving the flaking station with a crumbly sheet that breaks under roller pressure. [NEED_CITE: moisture content and expansion ratio relationship in twin-screw extrusion of cereal starches]
Reading the Specification Sheet Against Your Product Target
Installed power ranges from 160 kW on the MT70 to 210 kW on the MT75, reflecting the torque needed to push higher-throughput or higher-shear recipes through the barrel. Power consumption figures sit roughly 25–30 % below installed capacity, which is typical for lines that cycle between heating and cooling phases across barrel zones. The hydraulic double-roller flaking station uses separate motors for each roller, allowing independent speed adjustment so the nip gap and surface speed can be set to the pellet diameter coming off the die. Infrared temperature monitoring on the flaking rolls keeps the surface within a narrow band, preventing the pellet from sticking or shattering on contact. The hot-air roasting oven pairs a conciliation burner with dual circulating fans and a cyclone dust collector, giving precise control over the surface blistering and final moisture that define a corn flake’s crispness and shelf stability.
What Happens When Extruder and Dryer Are Mismatched
A line quoted on extruder nameplate output without matching dryer residence time and roasting oven throughput creates a bottleneck that surfaces only during the first full-speed run. Wet flakes pile up on the conveyor, moisture migrates into already-toasted product, and the packing station receives material outside specification. [NEED_CITE: throughput matching across extrusion, drying and roasting stations in cereal lines] These problems are avoidable when the corn flakes extrusion machine screw configuration barrel temperature profile is evaluated alongside dryer belt length, air velocity and roasting chamber volume as one integrated system.
Why Buy the Whole Line From One Supplier
The complete processing line — from batching mixer through extrusion, flaking, drying, roasting, cooling and packing — is configured under a single engineering scope, so throughput at every station is calculated against the same raw material and product target. Screw configuration and die design are specified after reviewing the buyer’s corn variety, particle size and desired flake density, not copied from a catalogue default. An in-house testing workshop runs the buyer’s actual raw material before shipment, generating a trial report that documents expansion ratio, flake thickness and roasting behaviour. Pre-sales consultation covers line layout, utility planning and electrical schematic review, and on-site installation includes operator training on the PLC or MCC control interface. Ongoing maintenance support includes a documented wear parts list covering screws, dies and roller surfaces.
Documentation & Verification
- Line layout drawing with capacity calculation matched to your corn variety and target flake density
- Screw and die configuration record documenting element arrangement and die orifice geometry
- Trial run report on your raw material showing expansion ratio, flake thickness and moisture curve
- Electrical schematic with voltage, frequency and control language confirmed for your facility
- CE declaration of conformity and ISO certificate for the complete processing line
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation plan accounting for the full line footprint up to 45 m length and 5,000 kg mass
- Dedicated power circuit sized for up to 210 kW installed load at confirmed voltage and frequency
- Modular shipment with reassembly supervised by factory technicians on your workshop floor
- First-run parameter setting covering barrel zones, roller nip gap and roasting temperature ramp
- Operator training on the PLC or MCC interface including recipe storage and alarm response
- Wear parts kit covering screw elements, die plates and flaking roller sleeves for the first replacement cycle
Preparing Your Enquiry
Send the corn or multi-grain flour you intend to use, along with the target flake thickness, final moisture content and daily output goal. Include your workshop floor dimensions, local voltage and frequency, and the control language your operators need so the line can be configured before production starts.
Frequently Asked Questions
Q: How is screw configuration and die design matched to my specific corn variety and target flake density?
A: We review your corn flour sample for particle size, starch content and moisture level, then select screw element geometry and die orifice diameter to deliver the partial gelatinisation and pellet size your flaking rollers require. A trial run in our testing workshop confirms the result before the machine ships.
Q: What barrel temperature profile and moisture range produce natural versus sugar-coated corn flakes?
A: Natural flakes need a lower barrel exit temperature and tighter moisture control to keep the pellet dense enough for thin rolling. Sugar-coated variants tolerate slightly higher expansion because the coating adds structural rigidity. Both profiles are documented in your screw and die configuration record.
Q: How is output capacity verified on my actual raw material before shipment?
A: We run your corn or multi-grain flour through the extruder in our in-house testing workshop, measuring throughput, expansion ratio and flake density. The trial run report accompanies the machine and serves as the baseline for on-site commissioning.
Q: How are extruder throughput, dryer capacity and roasting oven residence time matched to avoid line bottlenecks?
A: Each station is sized against the same raw material and product target during the line configuration phase. The layout proposal shows calculated residence time and belt speed at every stage, so no single unit limits the overall output.



