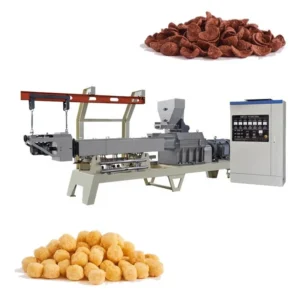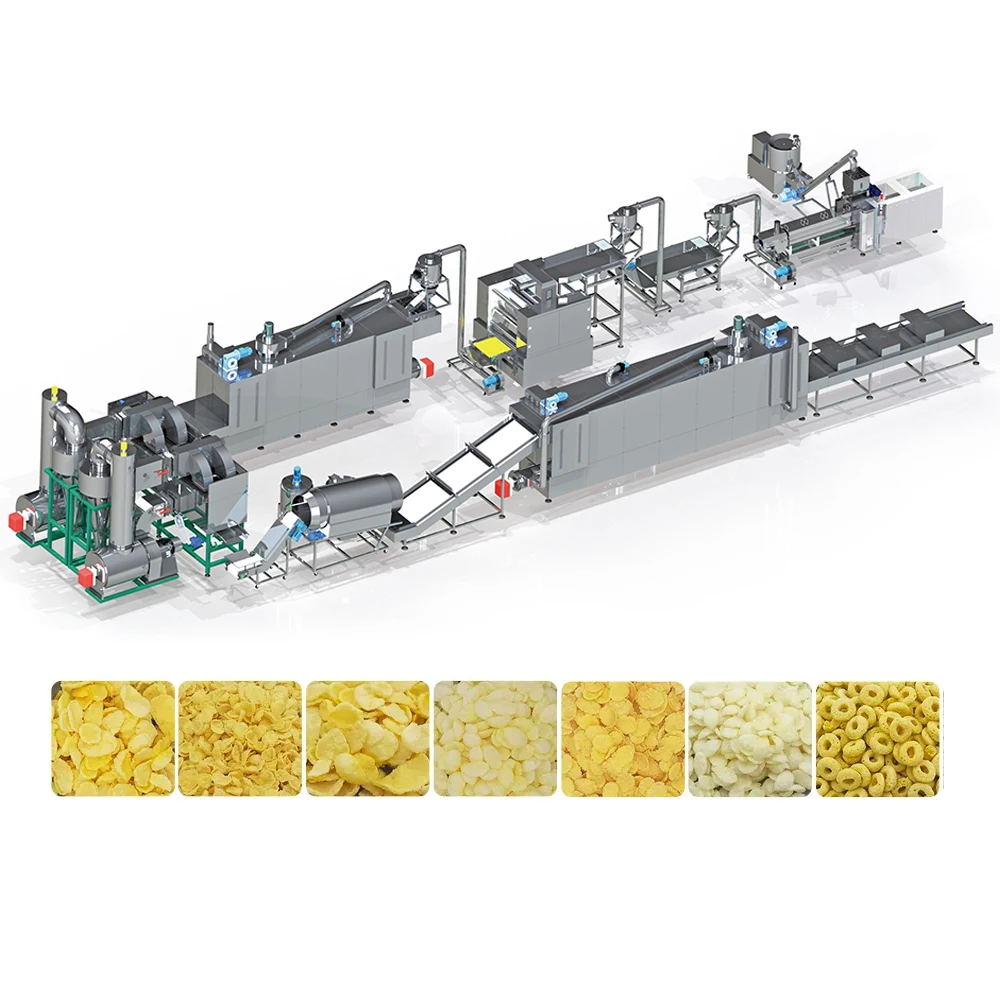
Screw Configuration Matched to Raw Material — the MT-65 twin-screw barrel sequence is built around the buyer’s specific grain blend and target flake density, not copied from a generic template.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65 |
| Product Type | Corn Flakes Breakfast Cereal Production Line |
| Extruder Type | Co-rotating Double Screw Extruder with sectional screw modules |
| Screw Functions | Forward and backward transport, mixing, de-gassing, cooking and forming |
| Mixer Output | 10–30 kg/load (basis not stated in source — confirm raw material type and moisture) |
| Mixer Power | 4 kW |
| Mixer Tank Size | φ600 × 500 mm |
| Mixer Dimension | 1000 × 800 × 1200 mm |
| Screw Conveyor Driving Power | 0.75 kW |
| Screw Conveyor Dimension | 2700 × 500 × 2400 mm |
| Corn Flakes Press Machine Power | 16.12 kW |
| Corn Flakes Press Machine Size | 1550 × 1300 × 2000 mm |
| Press Roller Size | 510 × 310 × 1050 mm |
| Press Material | Stainless Steel |
| Press Features | Large roller, integrated cooling system, adjustable roller distance for flake thickness |
| High-Temperature Oven Size | 4.5 × 1.4 × 1.8 m |
| High-Temperature Oven Power | 3.75 kW |
| Oven Heating Method | Gas-fired, both-side baking system |
| Sugar Spraying System Total Power | 28.75 kW |
| Sugar Spraying System Dimension | 4000 × 1900 × 1880 mm |
| Sugar Spraying Roller Size | Ø600 × 2700 mm |
| Control System | Separate Controller Box |
| Contact Material | Stainless steel on all product-contact surfaces |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flakes breakfast cereal | Corn grits and corn flour blends |
| Multi-grain breakfast flakes | Rice, oat and mixed grain powders |
| Fortified breakfast cereal | Grain flour with added vitamins and nutritional ingredients |
| Coated cereal snacks | Extruded shapes with sugar syrup or honey coating |
| Puffed snack shapes | Grain-based raw materials formed into ring, ball, star and stick shapes via die changes |
Why Generic Screw Builds Undermine Your Corn Flakes Extrusion Technology Production Line
Starch gelatinisation fails when screw modules are not staged to the actual flour blend running through the barrel.
I have watched lines ship with a screw configuration pulled from a standard build sheet, only for the corn flake to come out dense and brittle on the buyer’s own corn-to-oat ratio. The gelatinisation window shifts with every grain proportion change, and when the barrel temperature profile does not match, the flake either shatters in the bowl or refuses to crisp. That mismatch usually surfaces after installation, when the cost of flying an engineer across borders has already been added to the downtime tally. [NEED_CITE: starch gelatinisation temperature ranges across corn, rice and oat flours]
How Sectional Screw Modules Control Gelatinisation Stages
The co-rotating twin-screw design in this corn flakes extrusion technology production line uses modular screw elements that can be rearranged along the barrel. Each section handles a distinct function — forward transport, mixing, de-gassing, cooking and forming — so the residence time and shear profile can be tuned to the specific grain blend. Corn flour demands a different thermal ramp than oat-heavy mixes, and the sectional approach lets the process engineer adjust without swapping the entire screw assembly.
Barrel Temperature and Moisture Interaction at the Die
Gelatinisation degree at the die face determines whether the extrudate expands cleanly or collapses before it reaches the flaking press. The barrel zones work with the incoming moisture level to control how completely the starch granules rupture. Too little moisture and the corn flakes extrusion technology production line produces a hard pellet that cracks under the press roller; too much and the extrudate sticks to the belt and loses shape definition. [NEED_CITE: effect of extrusion moisture content on starch expansion ratio in cereal processing]
Press Roller Gap and Oven Uniformity
The flaking press features an adjustable roller distance backed by an integrated cooling system, giving direct control over final flake thickness. Downstream, the gas-fired high-temperature oven applies heat from both sides of the bed, which prevents the common problem of flakes on the tray centre remaining soft while edge flakes over-brown. Uniform crispness across the full tray width is what keeps bowl-life consistent from the first scoop to the last.
What Happens When Die Design Is an Afterthought
A die chosen for a generic shape catalogue will extrude, but the expansion ratio and cell structure will not match the market expectation for that specific flake or puff format. Ring shapes need different die land lengths than sticks, and when the corn flakes extrusion technology production line runs a one-size die across multiple SKUs, some shapes expand unevenly or develop internal voids that break during coating. This is why the die design record should reference the buyer’s target product, not a default drawing. [NEED_CITE: die land length influence on extrudate cell structure in twin-screw cereal extrusion]
Why the Trial Run Must Use Your Actual Raw Material
Every grain supplier delivers flour with slightly different particle size distributions and native moisture levels. A trial run conducted on the manufacturer’s stock corn grits tells you the machine works; a trial run on your shipment of corn, oat and rice flour tells you whether your formulation actually gelatinises and flakes as expected. Without that second test, the first real production run becomes the trial — and the raw material cost of that lesson is entirely avoidable.
Why Procurement Should Anchor on Process Data, Not Just Nameplate Capacity
Line throughput only matters when every station keeps pace. If the mixer delivers batches faster than the extruder can cook them, or if the dryer cannot reduce moisture before the coating drum, the bottleneck shifts and the rated output is never reached. This corn flakes extrusion technology production line is configured so that mixing, extruding, drying, pressing, baking and coating capacities are matched station to station, which is the only way the nameplate number translates to actual daily output. [NEED_CITE: throughput balancing principles in continuous food extrusion lines]
Documentation & Verification
- Screw and die configuration record specifying your grain blend ratios and target flake density
- Trial run report produced on your raw material sample before the line leaves the workshop
- Line layout drawing with capacity matched across mixing, extrusion and downstream stations
- Electrical schematic with voltage and frequency confirmed for your facility supply
- Operation and maintenance manual covering screw module changes and press roller adjustment
Installation, Commissioning & Support
- Foundation plan aligned to the oven footprint of 4.5 × 1.4 m and press weight distribution
- Dedicated electrical circuit sized for the combined 28.75 kW sugar spraying and 16.12 kW press loads
- Separate controller box positioned per site layout with cable routing confirmed before arrival
- First-run parameter setting covering barrel zone temperatures, screw speed and press roller gap
- Operator training on sectional screw module swap procedures and die change intervals
- Wear parts list covering screw elements, die plates and press roller bearings with replacement schedule
What to Prepare Before Requesting a Quote
Share your grain formulation ratios — corn, rice, oat or other cereals — along with any vitamin or nutritional additive inclusion rates. Confirm your facility voltage and frequency, and note whether your control operators need a specific interface language. If you have existing upstream mixers or downstream packing equipment, list their throughput so the line can be matched. Indicating whether you want a trial run on your own raw material before shipment helps the workshop schedule accordingly.
Frequently Asked Questions
Q: How does screw configuration affect starch gelatinisation and final flake density?
A: Sectional screw modules let the process engineer set distinct transport, mixing and cooking zones inside the barrel. The arrangement controls how much shear and heat the grain flour receives at each stage. Correct staging ensures starch granules fully rupture at the right moisture level, producing a flake with the density and bowl-life the market expects rather than a brittle or overly dense pellet.
Q: What barrel temperature profile is needed for corn versus rice versus oat-based cereals?
A: Each grain has a different gelatinisation onset temperature and moisture absorption rate. Corn typically requires a higher barrel temperature in the cooking zone than rice, while oat blends need gentler shear to avoid gumminess. The profile is set during the trial run on your specific flour ratios and documented in the configuration record before shipment.
Q: How does moisture level at extrusion influence expansion ratio and downstream flake texture?
A: Moisture determines how completely starch granules swell and rupture inside the barrel. Lower moisture limits expansion and yields a harder, denser pellet that may crack during pressing. Higher moisture increases expansion but can cause the extrudate to deform before cooling. The target range is established on your raw material during the pre-shipment trial.
Q: Can the die design be adjusted for different cereal shapes without changing the extruder?
A: Yes. The extruder barrel and screw assembly remain the same while the die plate is swapped to produce rings, balls, stars or sticks. Each shape requires a specific die land length and orifice geometry to control expansion uniformly. The die design is matched to your target product list and recorded in the configuration documentation.
Q: What trial run data is available on my specific raw material before shipment?
A: A full trial run is conducted in the in-house testing workshop using your grain flour sample. The resulting report covers extrusion temperature, screw speed, moisture at the die, expansion ratio and final flake thickness after pressing and baking. This data confirms your formulation performs as expected before the line is dispatched.