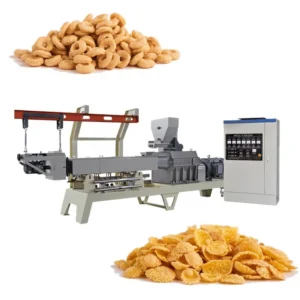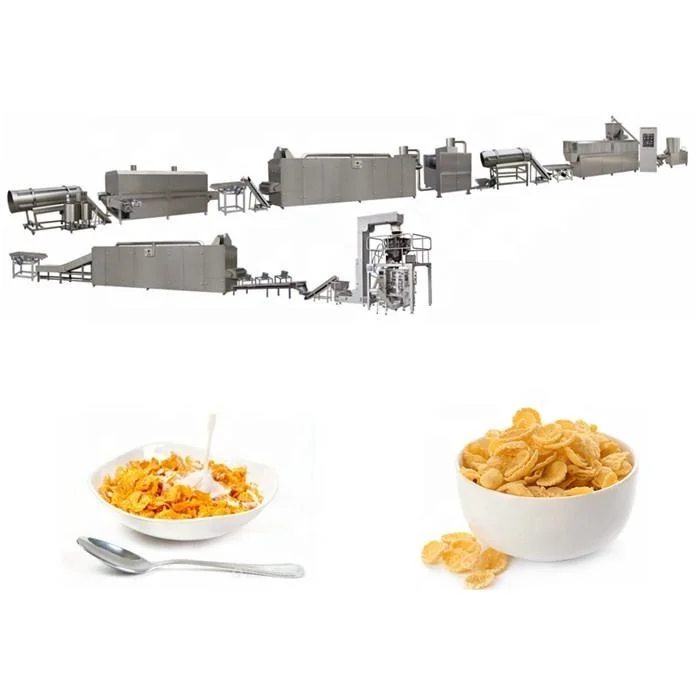
Custom screw geometry and die profiling — screw elements and die plates are configured to your grain blend before the corn flakes extrusion technology production line leaves our testing workshop.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Corn Flakes Production Line (Twin Screw Extrusion) |
| Extruder Unit | MT-75 Twin Screw Extruder |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Extruder Output | 200–300 kg/hr (basis to be confirmed) |
| Line Output | 300–500 kg/hr (basis to be confirmed) |
| Control System | PLC with MCC integration |
| Heating Source Options | Gas or electric for dryer and roasting oven |
| Flaking System | Hydraulic double rollers, dual independent motors, infrared temperature sensors |
| Roasting Oven | Vibrating pan, dual circulating fans, cyclone dust removal |
| Sugar Coating Option | Double tumble melter, elevator, coating drum, spray nozzle array |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Corn grits and corn flour blends |
| Multi-grain breakfast flakes | Oat, barley, wheat, and rice combinations |
| Sugar-coated cereal flakes | Corn or grain base with sugar slurry coating |
| Extruded cereal shapes | Rings, balls, sticks, fruit loops, stars, wheels, hearts via die change |
| Fortified breakfast cereal | Grain base blended with vitamin and mineral premix |
Why Generic Screw Profiles Undermine Your Corn Flake Density
A configuration pulled from a reference build rather than matched to your recipe will produce flakes that either shatter during roasting or emerge too dense to crisp properly.
When a European client sent us high-moisture oat stock last year, the flakes came out of the dryer soft and misshapen because the barrel temperature zones and screw compression ratio had been set for standard corn grits. The corn flakes extrusion technology production line only performed once we re-profiled the kneading blocks and adjusted moisture injection to match that specific blend. Generic builds skip this step entirely, leaving buyers to troubleshoot density and expansion problems during commissioning rather than in a controlled workshop [NEED_CITE: process variables in cereal extrusion and their impact on final product density].
Barrel Temperature Zones and Starch Gelatinisation
The MT75 barrel is segmented into independently heated zones, each with its own thermocouple and PID loop. For corn-based flakes, the feed zone is held cooler to prevent premature gelatinisation, while the compression and metering zones climb through the gelatinisation threshold of corn starch. The corn flakes extrusion technology production line relies on this gradient because incomplete gelatinisation leaves a raw core that roasts unevenly, while excessive heat too early causes the dough to stick and surge. Operators adjust these zones through the PLC touchscreen when switching between corn, oat, and barley recipes.
Screw Element Sequencing for Moisture and Shear Control
Twin-screw extruders use modular screw elements — conveying flights, kneading blocks, and reverse-pitch sections — arranged along the shaft. For flake stock that must exit the die as a dense, low-expansion ribbon rather than a puffed shape, the MT75 screw profile emphasises moderate shear with enough residence time for complete hydration. Kneading block stagger angles and the number of reverse elements determine how much mechanical energy converts to heat. Getting this sequence wrong produces a dough that either extrudes too wet, sticking to the flaking rollers, or too dry, cracking under roller pressure [NEED_CITE: twin screw element configuration principles for low-expansion cereal dough].
Reading the Specifications That Actually Matter
The 210 kW installed power and 150 kW operating consumption figure reflects the full line — extruder, dryer, roasting oven, and flaking motors combined — not just the extruder alone. The 45-metre line footprint includes mixing, extrusion, flaking, drying, hot air roasting, cooling, and packing stations in sequence. The PLC system governs feed rate, barrel temperatures, cutter speed, and flaking roller gap, while the MCC panel handles motor protection and power distribution. The hydraulic flaking station uses independent dual motors so roller speed and gap pressure are adjusted separately, which is critical when targeting a specific flake thickness for downstream roasting consistency.
The Hidden Cost of Mismatched Downstream Equipment
An extruder running at full capacity means little if the dryer cannot remove moisture fast enough or the roasting oven lacks uniform heat distribution. I have seen lines where the flaking rollers could not keep pace, forcing the extruder to idle and creating start-stop surges that wrecked flake consistency. The MT75 line addresses this by matching dryer belt length and roasting oven volume to extruder throughput. The dual circulating fans and cyclone dust removal in the roasting oven are not optional extras — they prevent scorching on one side of the pan while the other side remains underdone [NEED_CITE: importance of throughput balancing across extrusion, flaking, and drying stages].
Why Procurement Through This Workshop Works
Screw and die configurations are documented against your exact raw material formulation, so you receive a configuration record, not a generic parts list. Every MT75 line runs a trial on your supplied grain blend in our testing workshop before crating, and you receive the full trial run report showing moisture, expansion, and density readings. Electrical schematics are drawn and voltage confirmed against your factory supply before production begins, avoiding the commissioning delays that arise when a 400 V machine arrives at a 380 V site. The flaking station and roasting oven are designed and sourced as part of the same line, so throughput is matched across every station rather than patched together from separate vendors. Pre-sales consultation covers line layout, utility planning, and phased installation scheduling.
Documentation & Verification
- Line layout drawing with station-by-station throughput calculation for your target cereal format
- Screw and die configuration record matched to your grain blend and target flake density
- Trial run report from our testing workshop on your supplied raw material before shipment
- Electrical schematic with voltage and frequency confirmed to your site utility specification
- Machine specification sheet documenting L:D ratio, barrel zone count, and motor ratings
- CE declaration of conformity with packing photographs and customs documentation support
Installation, Commissioning & Support
- The 45 × 1.5 × 3.5 m line requires a level concrete floor with anchor points at each station base
- A dedicated 210 kW supply circuit with the confirmed voltage and frequency must be available before installation
- The line ships in modular sections; flaking rollers and roasting oven are assembled and aligned on site
- First-run commissioning includes PLC parameter loading, barrel zone calibration, and flaking gap setting
- Operator training covers recipe switching on the touchscreen and daily screw and die inspection
- Wear parts list identifies screw elements, die plates, and flaking roller sleeves with reorder intervals
What to Share When Requesting a Quotation
To configure the corn flakes extrusion technology production line correctly, we need your grain recipe and raw material moisture levels, the target flake thickness and final product format, your daily or hourly production target, and the available floor space and ceiling height. Please confirm your factory voltage and frequency, the preferred control language for the PLC interface, and whether you need the sugar coating circuit included. If you can send a sample of your raw material, we will run a trial in the testing workshop and include the results with the proposal.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal grain blends?
A: Each grain has a distinct starch gelatinisation temperature and fibre content that changes how the dough behaves under shear. We select kneading block geometry, stagger angle, and reverse-element placement based on your specific blend, then document the full configuration. A trial run on your material in our workshop confirms the profile before shipment.
Q: What barrel temperature profile is used for corn versus oat or barley-based flakes?
A: Corn typically requires higher compression-zone temperatures than oat or barley due to its gelatinisation range. Oat and barley blends need gentler heat progression to avoid gumminess. Operators store separate temperature recipes in the PLC so switching between grain types is a touchscreen selection, not a manual recalibration.
Q: How is flake density and expansion ratio controlled through moisture and die design?
A: Moisture injection rate, die aperture size, and the screw compression ratio together determine how much the dough expands at the die face. For dense flakes suitable for rolling, we use smaller die openings and higher barrel moisture. The flaking roller gap and hydraulic pressure then set the final thickness.
Q: Can the same extrusion platform run both natural and sugar-coated corn flakes?
A: Yes. The MT75 line flow for sugar-coated flakes adds a sugar melting tumble, coating drum, and spray nozzle array after the roasting oven, followed by a second drying pass. The extrusion and flaking stages remain identical, so format changeovers require only activating or bypassing the coating circuit.
Q: Is a trial run on our raw material performed before shipment, and what does the report cover?
A: We run your supplied grain blend through the MT75 in our testing workshop and record barrel temperatures, screw speed, moisture readings, expansion ratio, and flake density. The trial run report is included in your documentation package so you can verify product quality before the line is crated and dispatched.