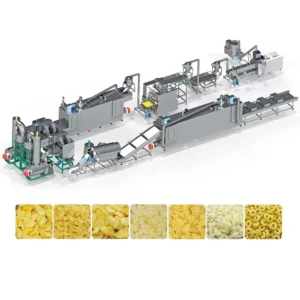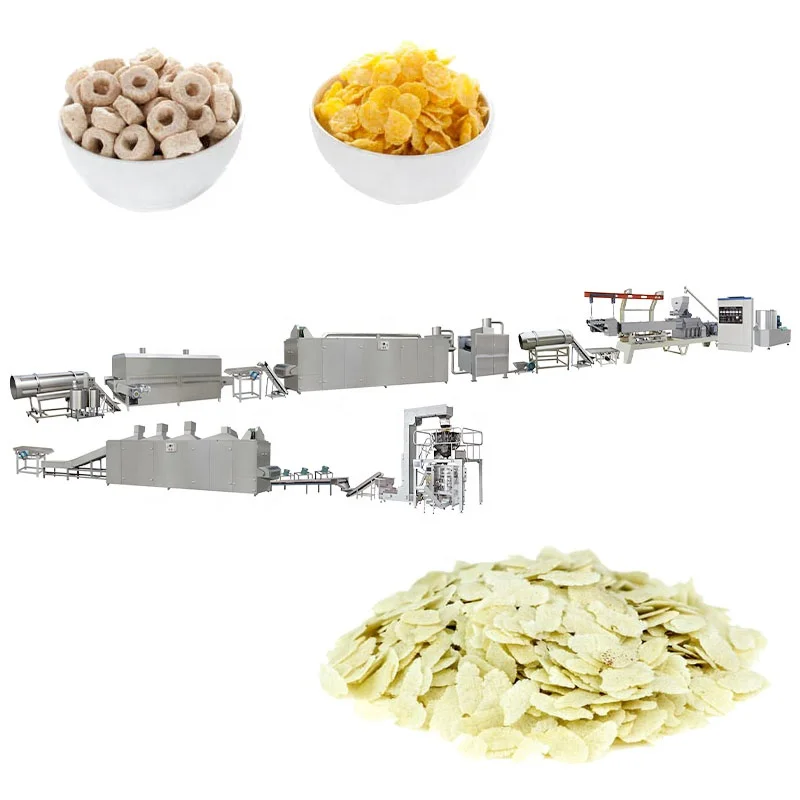
Screw Configuration Locked to Your Raw Material — every MT series extruder is set up with screw elements and die geometry matched to the buyer’s actual cereal formulation, validated through in-house trial runs before the machine leaves Jinan.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Breakfast Cereal Corn Flakes Extrusion Line |
| Model Options | MT70 / MT85 / MT75 |
| Screw Type | Twin Screw |
| Installed Power (MT70) | 160 kW |
| Installed Power (MT85) | 190 kW |
| Installed Power (MT75) | 210 kW |
| Power Consumption (MT70) | 120 kW |
| Power Consumption (MT85) | 140 kW |
| Power Consumption (MT75) | 150 kW |
| Output Capacity (MT70) | 150–200 kg/h (basis not stated in source — confirm raw material, moisture content, and flake thickness) |
| Output Capacity (MT85) | 300–400 kg/h (basis not stated in source — confirm raw material, moisture content, and flake thickness) |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material, moisture content, and flake thickness) |
| Overall Dimensions (MT70) | 41 × 1.5 × 2.2 m |
| Overall Dimensions (MT85) | 43 × 1.5 × 3.2 m |
| Overall Dimensions (MT75) | 45 × 1.5 × 3.5 m |
| Control System | PLC for flaking unit; MCC and PLC available for full line |
| Flaking Rollers | Dual-motor independent drive with hydraulic system |
| Flaking Temperature Control | Infrared sensor for even temperature pipe regulation |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air with conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble drum for sugar melting, elevator, coating drum, spraying nozzle |
| Die Configuration | Adjustable mould — ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Extruder Features | Automatic lubrication, cooling function, wear-resistant screws with special treatment |
| Certification | CE (since 2014), ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour at controlled moisture |
| Sugar-coated corn flakes | Extruded corn pellets through flaking, roasting, and sugar spraying |
| Multi-grain breakfast cereals | Blends of wheat, oat, barley, and rice flour |
| Shaped cereal products | Ring, fruit loop, star, and wheel forms via adjustable die |
| Fortified cereal lines | Vitamin- and mineral-enriched cereal powder blends |
What "Rated Capacity" Means When the Cereal Formula Changes
A capacity figure only holds when the raw material, moisture level, and flake thickness match the test conditions.
I learned this the hard way on a corn flake line we shipped a few years back. Trial runs in our workshop used standard corn grits and the extruder held steady throughput with good pellet density. When the line reached the buyer’s plant, their corn flour had a noticeably higher fat content. The pellets came out dense, the flakes refused to blister properly in the roasting oven, and the whole process window had to be rebuilt from scratch — half a month of lost production [NEED_CITE: effect of lipid content on starch gelatinisation in cereal extrusion]. That is why every breakfast cereal corn flakes extrusion line we build now starts with a raw material report, not a catalogue number.
How Screw Elements Shape the Pellet Before It Becomes a Flake
The extrusion stage determines everything downstream. In a breakfast cereal corn flakes extrusion line, the twin-screw configuration controls shear rate, residence time, and starch gelatinisation inside the barrel zones. We select conveying, kneading, and reverse-screw elements based on the starch-protein ratio of your cereal blend. A high-protein oat mix requires a different screw profile than pure corn grits — too much shear breaks the protein network, and the pellet collapses instead of expanding cleanly through the die.
Barrel Temperature Profile and Starch Gelatinisation Control
Each barrel zone carries independent heating and cooling circuits, allowing us to build a temperature gradient that drives starch gelatinisation progressively rather than in a single spike. The moisture window for corn flake extrusion sits in a narrow band — too dry and the pellet fractures during flaking, too wet and the flake sticks to the roller surface [NEED_CITE: barrel temperature zone control in twin-screw extrusion for cereal processing]. The die face design then governs the pellet cross-section, which directly determines flake uniformity after the hydraulic roller press.
Reading the Specifications Beyond the Nameplate
The installed power figures across MT70, MT85, and MT75 reflect not just motor size but the full thermal load of extrusion barrel heaters plus downstream drying. Power consumption numbers run lower because barrel heating cycles on and off once thermal equilibrium is reached. The overall line length — stretching past 40 metres in all three models — accounts for the sequential stations: extrusion, flaking, drying, hot air roasting, and optional sugar coating. The dual-motor hydraulic flaking system lets operators adjust roller gap independently, which matters when you switch between a thin corn flake and a thicker multi-grain format. Automatic lubrication and wear-resistant screw treatment reduce unplanned stops during continuous shifts, and the PLC on the flaking unit maintains roller pressure consistency without constant manual intervention.
The Hidden Cost of a Mismatched Extruder-to-Dryer Ratio
When the extruder pushes more wet pellet than the dryer can handle, moisture piles up in the flaking zone. Flakes come off the rollers sticky, bridging in the conveyor, and the roasting oven never reaches the surface blister temperature needed for proper crispness. I have walked into plants where the extruder was upgraded but the dryer stayed the same size — the line technically runs, but output quality drifts through the shift [NEED_CITE: throughput balancing between extruder and dryer stations in cereal lines]. Matching throughput across every station is not optional when starch-based products are involved.
Why Sourcing This Line Through a Single Extrusion Technology Supplier Matters
The screw configuration and die geometry we specify are based on your cereal formulation, not a generic build copied across product categories. Our in-house testing workshop runs trial extrusion on your actual raw material before shipment, so the barrel profile and flake density are documented — not guessed at during commissioning. The complete line from mixing through extrusion, flaking, drying, roasting, and packing comes under one supplier, meaning throughput calculations are matched station by station rather than assembled from mismatched vendors. CE certification has been maintained since 2014, and electrical schematics confirm voltage, frequency, and control language for the destination market before production begins. Wear parts lists for screws, dies, and roller surfaces ship with the line so first replacements are on hand when needed.
Documentation & Verification
- Line layout drawing showing station spacing matched to your factory footprint
- Screw and die configuration record tied to your cereal raw material report
- Trial run report from our testing workshop on your actual flour blend
- Electrical schematic confirming voltage, frequency, and PLC language for your market
- CE declaration of conformity and ISO certificate for the complete line
- Operation and maintenance manual covering extruder barrel zones through roasting oven
Installation, Commissioning & Support
- Foundation plan accounts for the 41–45 m line length and drying oven weight distribution
- Power supply specification covers MT75 peak draw of 210 kW with dedicated circuit for roasting oven burner
- Modular station delivery allows phased unloading where factory door height is limited
- Commissioning includes barrel temperature mapping and flaking roller gap calibration on your cereal blend
- Operator training covers PLC interface, hydraulic roller adjustment, and sugar coating drum speed
- Wear parts inventory includes replacement screw elements and die plates for the initial production run
What We Need to Size Your Line Correctly
To propose a configuration that actually runs your product, we need the cereal raw material specification — including grain type, particle size, fat and protein content, and target moisture at the extruder infeed. Share your desired flake thickness, final product density, and whether the SKU is natural or sugar-coated. Your workshop dimensions and available ceiling height determine the dryer and roasting oven layout, and the local voltage and frequency must be confirmed so motors and heating elements are wound correctly before build.
Frequently Asked Questions
Q: How is screw configuration determined for different cereal raw materials and target flake densities?
A: We start with the buyer’s raw material report — grain composition, protein-to-starch ratio, fat content, and particle size. Screw elements are then arranged to control shear intensity and residence time inside each barrel zone. A high-starch corn flour needs a different kneading block sequence than an oat-heavy blend. The configuration is validated through a trial run in our testing workshop before the extruder ships.
Q: What barrel temperature profile and moisture range are used to control starch gelatinisation in corn flake extrusion?
A: Corn flake extrusion typically requires a progressive temperature ramp across the barrel zones, with moisture content at the infeed held within a narrow band to achieve full gelatinisation without over-expansion. Each zone is independently heated and cooled through the PLC, allowing the operator to fine-tune the profile once the line is running on the production formulation.
Q: How is output capacity verified on the buyer’s actual formulation before line shipment?
A: We conduct a trial run in our Jinan testing workshop using the buyer’s own raw material or a closely matched substitute. Throughput is measured at the extruder discharge and again after flaking and drying, so the capacity figure reflects the entire line rather than just the extruder in isolation. A written trial report accompanies the shipment.
Q: How does die design affect pellet shape and downstream flake uniformity for multi-grain breakfast cereals?
A: The die orifice geometry controls the pellet cross-section, which sets the flake outline after the hydraulic roller press. For consistent flake thickness, the pellet must exit the die with uniform density across its profile. Our adjustable die mould covers ball, tube, ring, star, and other shapes, and the die selection is matched to both the cereal formulation and the target flake specification.
Q: What is the role of hot air roasting temperature and residence time in achieving target flake crispness?
A: The roasting oven uses a conciliation burner with dual circulating fans to drive surface blistering and moisture reduction to the target level. Residence time inside the oven is set by conveyor speed, and the cyclone dust removal device keeps fine cereal particles from scorching on the heating elements. The correct combination produces a crisp flake without burnt edges or a soft core.