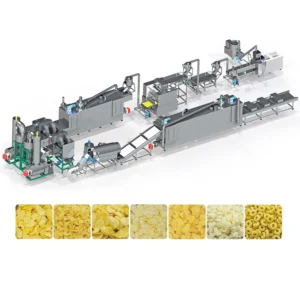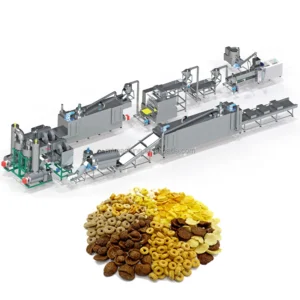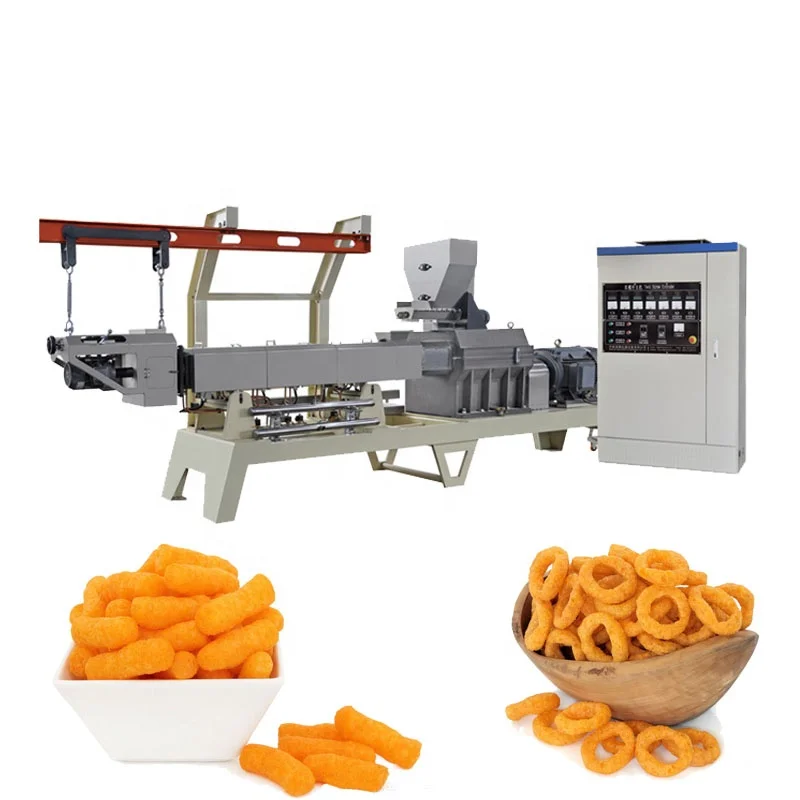
Customised Screw Profiles — every element sequence is mapped to your flour blend and target flake density before the barrel is ever assembled.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Corn Flakes Extrusion Production Line |
| Models Available | MT70, MT85, MT75 |
| Screw Type | Twin Screw |
| Installed Power | MT70 — 160 kW; MT85 — 190 kW; MT75 — 210 kW |
| Power Consumption | MT70 — 120 kW; MT85 — 140 kW; MT75 — 150 kW |
| Output Capacity | MT70 — 150–200 kg/h (basis not stated in source); MT85 — 300–400 kg/h (basis not stated in source); MT75 — 300–500 kg/h (basis not stated in source) |
| Overall Dimensions (L×W×H) | MT70 — 41 × 1.5 × 2.2 m; MT85 — 43 × 1.5 × 3.2 m; MT75 — 45 × 1.5 × 3.5 m |
| Control System | PLC (flaking station confirmed PLC; full line PLC/MCC not specified in source) |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Flaking Station | Hydraulic double-roller system with infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Hot Air Roasting Oven | Vibrating pan, two circulating fans, cyclone dust removal |
| Die Configuration | Adjustable mould for multiple shapes |
| Voltage & Frequency | Customised to local supply per customer |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits or corn flour at controlled moisture |
| Sugar-coated breakfast cereals | Extruded corn pellets through coating drum |
| Multi-grain flake lines | Blends of rice, wheat, oat, and barley powder |
| Shaped cereal pieces | Ball, tube, stick, ring, star, flower, and heart forms via interchangeable dies |
| Fortified breakfast cereal | Grain-based formulations with added nutritional premix |
What "300 kg/h" Actually Means When Your Corn Flour Arrives
Throughput only holds when the screw profile and barrel zones are matched to the exact particle size and moisture content of your raw material.
I watched a line lose half its rated output because the buyer’s corn flour was ground coarser than the sample we tested with. The extruder pushed material through, but the flakes came out thick and under-expanded. The corn flakes extrusion technology twin screw configuration that worked on one grind size simply failed on another. Once we reprofiled the screw elements and adjusted the die geometry, the line recovered — but that week of downtime and wasted raw material cost the buyer far more than a trial run would have [NEED_CITE: impact of raw material particle size on extrusion throughput].
How Screw Element Sequence Controls Flake Expansion
The twin-screw extruder processes material through distinct zones — feeding, kneading, shearing, and metering — each defined by the arrangement of screw elements. For corn flakes extrusion technology twin screw applications, the kneading block angle and stagger determine how thoroughly starch gelatinises before the material reaches the die. A steeper angle increases shear and raises the dough temperature, which can over-expand low-moisture corn flour and produce brittle flakes that shatter during flaking. Matching the element profile to your specific grain blend is the difference between a crisp, intact flake and a crumbly one.
Barrel Temperature Profile and the Moisture-Shear Balance
Each barrel zone carries independent heating and cooling control. The interplay between barrel temperature, injected moisture, and mechanical shear governs the expansion ratio at the die exit. Corn requires a different thermal ramp than oat or barley, because each starch has a distinct gelatinisation onset temperature [NEED_CITE: starch gelatinisation temperatures across cereal grains]. Running oat-heavy formulations on a barrel profile tuned for corn typically produces under-cooked centres and flakes that crack during the hot air roasting stage. The process engineer must map the temperature curve to the dominant starch in the blend before locking in the production recipe.
Reading the Specification Sheet Against Your Production Target
Installed power across the MT70, MT85, and MT75 models ranges from 160 kW to 210 kW, and actual power consumption sits roughly 25–30 percent below those figures during steady-state operation. The overall line length spans 41 to 45 metres, which dictates the conveyor run between the extruder, flaking station, dryer, and roasting oven. Twin screw corn flakes extrusion technology twin screw systems at this scale demand a facility with sufficient linear floor space and ceiling clearance — the MT75 reaches 3.5 metres in height. The hydraulic flaking station uses separate motors for each roller, allowing independent speed adjustment to control flake thickness without altering the extruder output. The hot air roasting oven employs a vibrating pan with two circulating fans and a cyclone dust removal device, which keeps fines from scorching and contaminating the product stream.
The Hidden Cost of a Generic Screw Build
When an extruder ships with a screw configuration copied from a different product category, the consequences surface gradually. Flakes may pass visual inspection on day one but show inconsistent bowl life by week three. Density drift forces the roasting oven to run longer cycles, consuming extra energy without improving quality [NEED_CITE: relationship between extrusion density and downstream drying energy]. The flaking station then compensates for uneven pellet thickness by increasing roller pressure, accelerating wear on the hydraulic seals. None of these failures appear in a factory acceptance test that only runs for a few hours on the supplier’s standard corn flour.
Why Sourcing the Extrusion Technology Here Matters
Every line configuration starts from your raw material sample, not from a catalogue template. The screw and die configuration record documents the exact element sequence and die geometry chosen for your product, giving your process team a baseline to adjust from. The in-house testing workshop runs your actual flour blend through the extruder before the machine leaves Shandong, generating a trial run report that confirms expansion ratio and flake integrity. Throughput calculations balance every station — extruder, flaker, dryer, roaster, coater — so no single unit bottlenecks the corn flakes extrusion technology twin screw line. Voltage, frequency, and control language are confirmed against your facility specifications before the electrical cabinets are wired [NEED_CITE: voltage and frequency standards by export market]. CE and ISO documentation accompanies every shipment.
Documentation & Verification
- Screw and die configuration record specifying element sequence for your grain blend
- Trial run report on your raw material from the in-house testing workshop
- Line layout and capacity calculation balancing throughput across all stations
- Electrical schematic with voltage and frequency confirmed to your facility
- CE declaration of conformity and ISO certificate included with shipment
Installation, Commissioning & Support
- MT75 line requires a 45-metre linear floor run with 3.5-metre ceiling clearance
- Power supply must support up to 210 kW installed capacity with dedicated circuit breaker
- Extruder ships partially assembled; barrel sections align on-site to the flaking station
- PLC parameters for barrel zones and flaking pressure calibrated during first production run
- Wear parts list covers screw elements, die plates, and flaking roller seals for initial spares
- Lubrication schedule for twin-screw gearbox and hydraulic flaking system provided at handover
What We Need to Configure Your Line
Send us your actual raw material — the specific corn flour or multi-grain blend you intend to run — along with target flake thickness and whether you need natural or sugar-coated output. Share your facility voltage, frequency, and preferred control language so the electrical cabinets match your plant. If you have existing upstream mixers or downstream packing equipment, let us know the interface points so the line layout accounts for them.
Frequently Asked Questions
Q: How do you match the screw configuration to my specific raw material?
A: We request a sample of your actual flour blend and run it through the extruder in our testing workshop. The screw element sequence, kneading block angles, and die geometry are then selected based on the expansion ratio and flake integrity observed during that trial, not copied from a generic template.
Q: Can I run a trial with my own flour before the line ships?
A: Yes. The in-house testing workshop conducts a full extrusion trial on your raw material, measuring throughput, expansion, and flake quality. You receive a trial run report documenting all process parameters before you approve shipment.
Q: How is output capacity verified, and on what basis?
A: The published figures for each model are measured under specific raw material and moisture conditions. Because corn flour particle size and blend composition vary, we confirm your line’s actual throughput during the trial run on your material and document it in the test report.
Q: What barrel temperature profile works for multi-grain flakes versus pure corn?
A: Each grain starch gelatinises at a different temperature, so the barrel zone profile must shift when oat, barley, or rice replaces part of the corn content. We establish the thermal ramp during your material trial and record the recommended zone settings in the configuration documentation.
Q: How do you prevent the flaking station from bottlenecking the extruder?
A: Line capacity calculations balance every station — extruder output, flaker roller speed, dryer residence time, and roaster throughput — before the layout is finalised. The hydraulic flaking station uses independent roller motors to adjust thickness without reducing upstream extrusion speed.