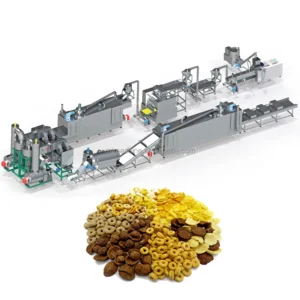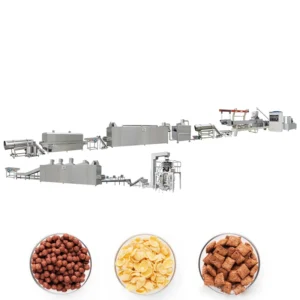
Matched Screw Geometry — Every barrel zone and screw element is specified against your actual grain blend before we release the line layout, not copied from a catalog build.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Extruder Production Line |
| Models Available | MT70, MT85, MT75 |
| Extruder Type | Twin Screw |
| Installed Power | MT70 — 160 kW; MT85 — 190 kW; MT75 — 210 kW |
| Power Consumption | MT70 — 120 kW; MT85 — 140 kW; MT75 — 150 kW |
| Output Capacity | MT70 — 150–200 kg/hr (basis to be confirmed); MT85 — 300–400 kg/hr (basis to be confirmed); MT75 — 300–500 kg/hr (basis to be confirmed) |
| Overall Dimensions | MT70 — 41 × 1.5 × 2.2 m; MT85 — 43 × 1.5 × 3.2 m; MT75 — 45 × 1.5 × 3.5 m |
| Basic Raw Materials | Corn, rice, wheat, oat, barley powder |
| Control System | PLC (flaking station); MCC / PLC for extruder |
| Screw Feature | Special alloy, wear-resistant, automatic lubricating and cooling |
| Flaking System | Hydraulic double-roller, dual motor drive, infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air, vibrating pan, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Production Procedure | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Coating (optional) → Cooling → Packing |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Corn grits and corn flour at controlled moisture |
| Sugar-coated breakfast cereals | Corn, rice, or wheat base with sugar syrup coating |
| Multi-grain flake formats | Blends of oat, barley, wheat, and rice flour |
| Shaped cereal pieces | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart profiles via die exchange |
What "Rated Capacity" Leaves Out About Cereal Extrusion
A nameplate output figure means nothing until the screw profile has run your actual grain formulation at your target moisture.
I spent years watching lines ship out with capacity numbers pulled from generic corn grit trials, only for the buyer to run a multi-grain blend with higher fiber content and see the flakes come out dense and under-expanded. The extruder is not the bottleneck — the mismatch between screw geometry and raw material behaviour is [NEED_CITE: starch gelatinisation thresholds across grain types]. When an oat-heavy blend hits a screw configuration tuned for pure corn, residence time drops, gelatinisation is incomplete, and the corn flakes extruder production line delivers a product that shatters instead of crisping in the roaster.
Barrel Temperature Profiling for Starch Gelatinisation
A corn flakes extruder production line lives or dies by how well the barrel zones manage the transition from raw flour to a fully gelatinised dough. The twin-screw design allows independent control across multiple heating and cooling zones, so moisture injection and shear can be staged rather than applied all at once. For a pure corn formulation, the profile typically ramps aggressively in the feeding and compression zones before levelling off near the die. Shift to a barley or oat blend, and that same profile scorch-fries the outer layer while leaving the core undercooked — the flake blisters unevenly in the roaster and the bowl-life collapses.
Screw Element Arrangement and Residence Time Control
The screw configuration determines how long material stays under shear and heat, which directly governs expansion behaviour at the die face. Kneading blocks, reverse elements, and pitch spacing are arranged to match the gelatinisation window of the specific grain blend. I have seen a Southeast Asian client switch from a pure corn recipe to one containing twenty percent oat flour, and the existing screw setup produced flakes that were noticeably thicker and harder than specification. The entire batch was scrapped before we reconfigured the element sequence to extend residence time in the melting zone. Getting this right before the machine leaves the factory is the reason we run trial batches on the buyer’s actual raw material in our testing workshop [NEED_CITE: twin-screw extrusion screw configuration methodology for cereal applications].
Reading the Specs That Actually Matter for Flake Quality
The installed power range — from 160 kW on the MT70 up to 210 kW on the MT75 — tells you the torque headroom available for high-fiber or high-protein grain blends that resist shear. The hydraulic double-roller flaking station with infrared sensor temperature control determines whether the extruded pellet gets pressed to a uniform gauge or arrives at the roaster with thick and thin spots that toast at different rates. The hot air roasting oven uses a vibrating pan with dual circulating fans and a conciliation burner, which matters because uneven air distribution produces some flakes that are properly blistered and others that are either pale or scorched. The PLC-controlled flaking station keeps roller gap and temperature locked in across long production runs, reducing the drift that causes density variation between the first bag and the last.
The Hidden Cost of a Generic Screw Build
When a corn flakes extruder production line ships with a screw and die configuration pulled from a standard template rather than matched to the buyer’s grain formulation, the failures are rarely dramatic — they are gradual and expensive. Flake density drifts outside the range the market expects, bowl-life shortens, and the sugar coating absorbs unevenly. Production staff compensate by adjusting moisture and line speed, which shifts the problem downstream to the dryer and roaster [NEED_CITE: effect of extruder screw wear on cereal flake density variation]. By the time the buyer traces the root cause back to the screw profile, weeks of off-spec product have already gone to rework or disposal.
Why Procurement Should Centre on Extrusion Engineering
Complete line throughput is matched station by station — extruder output, flaker capacity, dryer residence time, and roaster belt speed are calculated together so no single unit bottlenecks the corn flakes extruder production line. Screw configuration and die design are documented against your specific raw material blend and target flake thickness, not borrowed from a previous project. An in-house testing workshop runs your actual grain formulation on the twin-screw extruder before shipment, producing a trial run report that records barrel temperatures, screw speed, moisture levels, and flake density. The flaking station, roasting oven, and coating system are sourced and integrated under one supplier, which eliminates the finger-pointing that happens when separate vendors blame each other for a density or blister problem.
Documentation & Verification
- Screw and die configuration record matched to your grain blend and target flake gauge
- Trial run report on your raw material documenting barrel zones, moisture, and expansion data
- Line layout with throughput calculation across extruder, flaker, dryer, roaster, and coater
- Machine specification sheet confirming barrel zone count, element arrangement, and utility requirements
- Electrical schematic with voltage, frequency, and control language confirmation for your facility
- Factory test record and packing photographs before dispatch
Installation, Commissioning & Support
- Foundation and utility planning based on the selected model footprint, up to 45 × 1.5 × 3.5 m for the MT75
- Dedicated power circuit sized to the installed power rating, up to 210 kW, with confirmed voltage and frequency
- On-site assembly supervision covering extruder barrel alignment, flaker roller calibration, and roaster ductwork
- First-run commissioning with screw speed, barrel temperature, and moisture parameters set to your trial run baseline
- Operator training covering PLC interface navigation, die changeover, and hydraulic flaker adjustment
- Wear parts list with lead times for screw elements, die plates, and flaker roller surfaces
Preparing Your Inquiry
To configure a corn flakes extruder production line that holds capacity on your actual material, share your grain formulation with percentage breakdown, target flake thickness and density range, and daily output requirement. Include your workshop dimensions and ceiling height, local voltage and frequency, and whether you need the sugar coating station or a natural flake line only. If you plan to run multiple grain blends on the same line, list each formulation so the screw configuration can be specified for the full range.
Frequently Asked Questions
Q: How is the screw configuration specified for my grain blend and target flake density?
A: We take your raw material formulation — including grain type, percentage ratios, and typical moisture content — and design the screw element sequence, kneading block placement, and die geometry to match the gelatinisation and expansion behaviour of that specific blend. The configuration is validated in our testing workshop on your actual material before the line ships.
Q: What barrel temperature profile should I expect for corn versus multi-grain flakes?
A: Pure corn formulations generally require an aggressive ramp in the compression zone with moderate die-zone temperatures. Multi-grain blends with oat or barley need extended residence at lower peak temperatures to avoid surface scorching while achieving full core gelatinisation. The exact profile is established during the pre-shipment trial run and recorded in your documentation.
Q: How does the roasting stage achieve consistent blistering without over-drying?
A: The hot air roasting oven uses a vibrating pan with a conciliation burner, two separate circulating fans, and a cyclone dust removal device. The vibration keeps flakes moving through the hot air stream, while the dual fans maintain even temperature distribution across the pan surface, producing uniform blistering and crispness without localized scorching.
Q: Can I trial my raw material before the line ships, and what does the report cover?
A: Yes. We run your actual grain formulation through the twin-screw extruder in our in-house testing workshop before shipment. The trial run report documents barrel zone temperatures, screw speed, moisture levels, flake density, expansion ratio, and any screw or die adjustments made to reach your target specification.
Q: How do you prevent one station from bottlenecking the rest of the line?
A: Throughput is calculated across every station — extruder output, flaker roller speed, dryer belt residence time, roaster pan capacity, and coating drum volume — before the line layout is finalised. The capacity calculation is included in your documentation so you can verify that no single unit limits the production rate of the others.