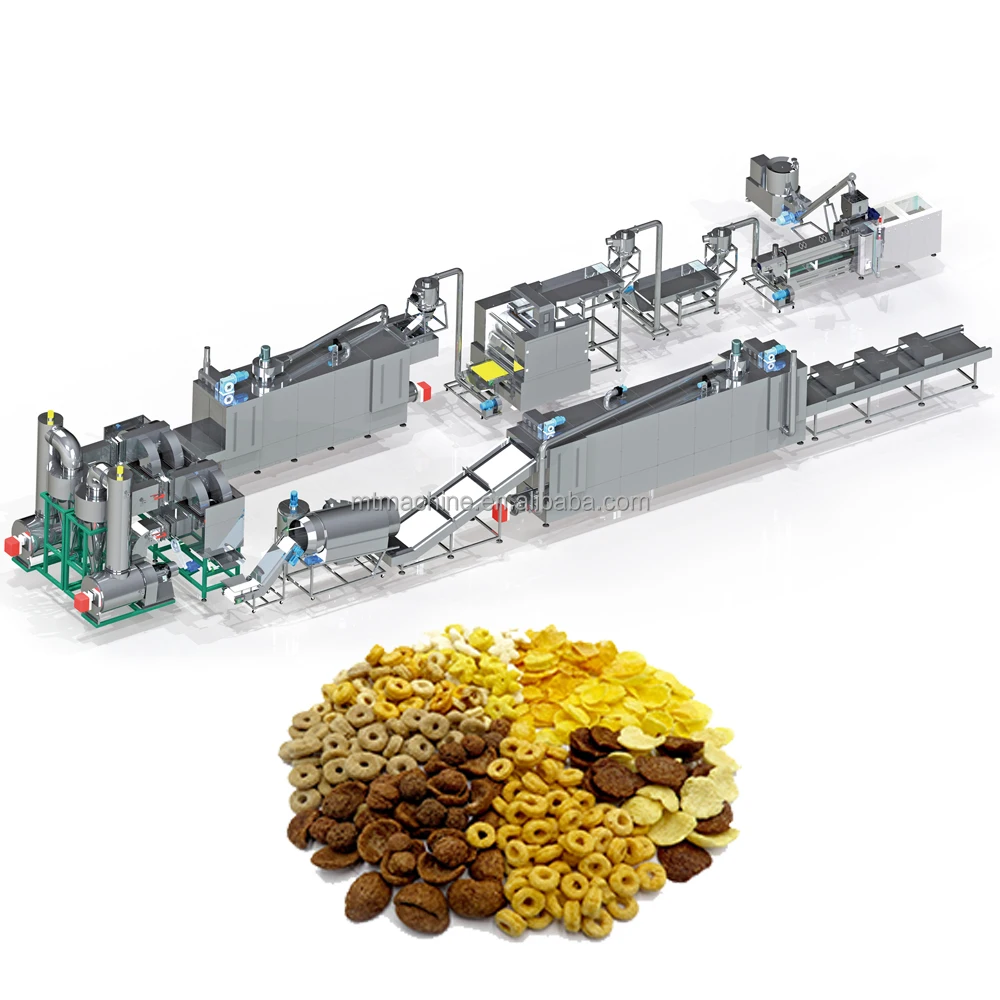
Screw Configuration Matched to Your Grain Blend — Every MT70, MT85, and MT75 barrel section is set up around the starch gelatinisation curve of your actual corn, rice, or oat formulation, not a generic breakfast cereal template.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Production Line (Breakfast Cereal Extrusion Line) |
| Extruder Type | Twin Screw |
| Installed Power (MT70 / MT85 / MT75) | 160 kW / 190 kW / 210 kW |
| Power Consumption (MT70 / MT85 / MT75) | 120 kW / 140 kW / 150 kW |
| Capacity (MT70) | 150–200 kg/h (basis not stated in source — confirm raw material / moisture) |
| Capacity (MT85) | 300–400 kg/h (basis not stated in source — confirm raw material / moisture) |
| Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material / moisture) |
| Dimensions (MT70 / MT85 / MT75) | 41×1.5×2.2 m / 43×1.5×3.2 m / 45×1.5×3.5 m |
| Extruder Features | Automatic lubricating, cooling function, wear-resistant screw |
| Flaking Station | PLC control, hydraulic double-roller system, infrared temperature control |
| Dryer Heating Source | Gas / Electric (configurable) |
| Roasting Oven | Hot air, dual circulating fans, cyclone dust removal, conciliation burner |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Control System | PLC (flaking station); MCC/PLC line-level control |
| Final Products | Natural corn flakes, sugar-coated flakes, shaped cereals (ring, star, ball, tube) |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Commercial natural corn flakes | Corn grits, corn flour |
| Sugar-coated breakfast flakes | Corn, rice, or wheat base with sugar syrup coating |
| Multi-grain extruded cereal shapes | Rice, wheat, oat, and barley powder blends |
| Shaped ready-to-eat cereals | Rings, stars, balls, tubes, fruit loops from cereal flour |
| Fortified breakfast cereal lines | Grain base with added vitamin and mineral premix |
Why Extruder Throughput Numbers Fail on Your Actual Grain
Nominal capacity figures mean nothing until the twin-screw extruder is tested against your specific corn grits and moisture level.
I have seen breakfast cereal producers sign off on a line rated at a certain output, only to find that their particular corn variety gelatinises differently, dragging actual throughput below what was promised. The corn flakes extrusion production line specifications printed in a brochure rarely account for how local grain hardness or ambient humidity changes the shear profile inside the barrel. When the extruder cannot hold steady output, the flaking station downstream starves, and the roasting oven runs half-empty. [NEED_CITE: twin-screw extrusion throughput variance across grain types]
How Screw Geometry Dictates Flake Texture
The twin-screw configuration in the MT series allows operators to adjust screw element sequencing — conveying, kneading, and reverse elements — along the barrel length. This sequencing controls residence time and shear intensity, which directly influence starch gelatinisation. For corn flakes, incomplete gelatinisation produces brittle flakes that shatter during roasting, while over-working the dough yields a dense, hard bite. The corn flakes extrusion production line specifications must therefore include the exact screw arrangement matched to your grain blend, not a default build.
Barrel Temperature Zones and Moisture Management
Each barrel section on the MT70, MT85, and MT75 can be independently heated and cooled, creating distinct thermal zones from feed inlet to die face. Corn flour typically enters at a moisture content that must be raised through steam or water injection inside the barrel to reach the gelatinisation window. Too much moisture at the die causes the extrudate to expand excessively and collapse before flaking; too little leaves raw centres in the pellet. Managing this balance across the full corn flakes extrusion production line specifications is what separates consistent blistering in the roaster from uneven, pale output. [NEED_CITE: starch gelatinisation temperature range for corn-based extrusion]
Reading the Power and Dimension Data
The installed power figures — 160 kW on the MT70, 190 kW on the MT85, and 210 kW on the MT75 — reflect the motor capacity available to drive the screws against the viscosity of a cooked cereal dough. Higher installed power does not automatically mean proportionally higher output; it provides the torque headroom to handle tougher multi-grain blends containing oat or barley without stalling. Line dimensions scale from 41 m to 45 m across the three models, which includes space for the flaking rolls, dryer, roasting oven, and cooling conveyor. Buyers planning factory layout must verify these footprints against available floor space before finalising the corn flakes extrusion production line specifications. The automatic lubricating system and wear-resistant screw elements reduce unplanned stops during long production runs, keeping the thermal profile stable across shifts.
The Hidden Cost of a Mismatched Flaking Station
When the flaking rolls cannot compress extruded pellets at the same rate the twin-screw extruder delivers them, a backlog forms on the cooling belt. The pellets absorb ambient moisture, stick together, and produce uneven flake thickness after rolling. On sugar-coated lines, uneven flakes absorb syrup inconsistently, leaving some batches tacky and others over-crystallised. A flaking station with hydraulic pressure control, separate roller motors, and infrared temperature regulation — as fitted on these lines — addresses this bottleneck, but only if its capacity was calculated against the actual extruder output, not a nominal brochure figure. [NEED_CITE: hydraulic roller pressure requirements for cereal flaking]
Why Buyers Source the Extrusion Platform Here
The line is configured as a single project from batching to packing, so throughput at every station — extruder, flaker, dryer, roaster, coater — is matched rather than assembled from separate vendors. Screw and die configurations are documented against the buyer’s specific grain formulation, creating a reference record for future reorders. An in-house testing workshop allows trial runs on the customer’s raw material before the line ships, producing a report on flake density, expansion, and texture at target output. The PLC and MCC control architecture is confirmed for voltage, frequency, and operator language before manufacturing begins, avoiding on-site commissioning delays. Spare wear parts lists covering screws, dies, and roller surfaces are supplied with the initial delivery.
Documentation & Verification
- Line layout and throughput calculation showing matched station capacities for your target output
- Screw and die configuration record tied to your grain blend and moisture profile
- Electrical schematic with confirmed voltage, frequency, and control language for your market
- Factory trial run report on your raw material documenting flake density and expansion
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Operation manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation plan accounting for the 41–45 m line length and dynamic loads from the roasting oven vibrating pan
- Dedicated power circuit sizing for 160–210 kW installed load with voltage confirmation at your facility
- Extruder barrel assembled on-site with screw element sequence verified against your configuration record
- Flaking station hydraulic pressure and infrared sensor calibrated during first production run on your grain
- Operator training covering screw speed, barrel zone temperatures, and PLC parameter adjustment
- Wear parts inventory — screw elements, die plates, roller shells — stocked before first scheduled changeout
What to Include in Your Inquiry
Provide the grain type and typical moisture content you plan to process, along with your target daily output and shift pattern. Specify whether natural or sugar-coated flakes are the primary product, and list any shaped cereal formats you intend to run on the same extrusion platform. Confirm local voltage, frequency, and preferred control language so the electrical design is finalised before production starts.
Frequently Asked Questions
Q: How is extruder capacity verified against my specific grain blend and moisture content?
A: Before shipment, your raw material is run through the extruder in the testing workshop. The trial documents actual throughput, flake density, and expansion at your target output. Results are compared against the proposed line capacity, and screw configuration is adjusted if needed. You receive the full trial report before approving dispatch.
Q: What screw configuration and die design is selected for my target flake density and shape?
A: Screw elements are sequenced — conveying, kneading, reverse — based on your grain’s starch behaviour and desired pellet firmness. Die opening diameter and pattern are chosen to produce the pellet size that flakes to your target thickness. Both are recorded in the configuration sheet supplied with the line.
Q: How do I confirm voltage, frequency, and control language before commissioning?
A: During the proposal stage, you provide your facility’s electrical supply details and preferred PLC language. The electrical schematic is then drawn to match those parameters and sent for your approval before manufacturing. This prevents rewiring or reprogramming delays during on-site installation.
Q: Can the flaking and roasting stations keep pace with the extruder at rated output?
A: Every station is capacity-matched during the layout design phase. The hydraulic flaking roll speed, dryer belt length, and roasting oven throughput are all calculated against the extruder’s verified output on your material, so no single station becomes a bottleneck during continuous production.