
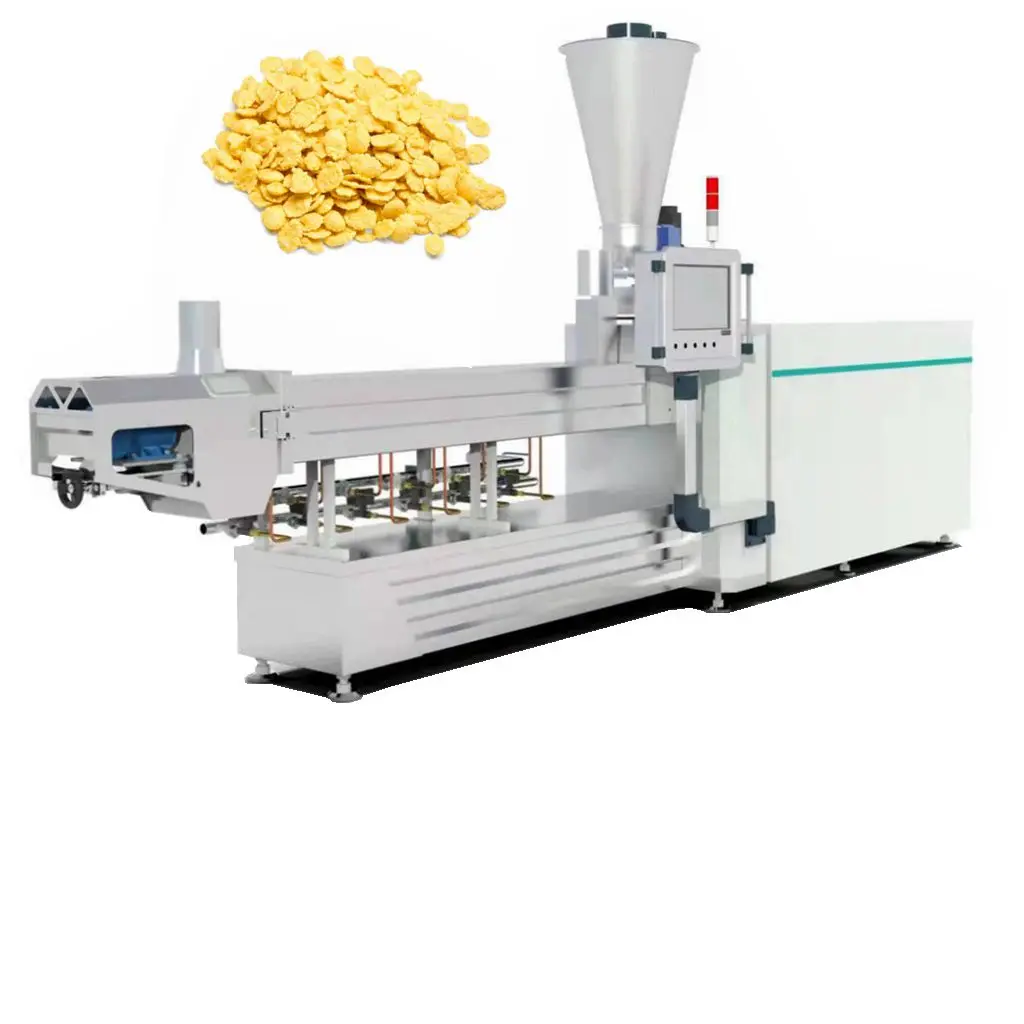
Screw Geometry Matched to Recipe — every barrel zone and die orifice is specified against your actual grain blend, not borrowed from a stock template, so the corn flakes extrusion line technology holds target density across long runs.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Breakfast Cereal Processing Line |
| Screw Type | Twin-screw |
| Installed Power (MT-65 / MT-70 / MT-75 / MT-85) | 84 kW / 132 kW / 186 kW / 239 kW |
| Real Power Consumption (MT-65 / MT-70 / MT-75 / MT-85) | 59 kW / 92 kW / 140 kW / 167 kW |
| Output Capacity (MT-65 / MT-70 / MT-75 / MT-85) | 120–150 / 200–250 / 400–500 / 300–400 kg/h (basis not stated in source — confirm raw material type, moisture content, and specific product format) |
| Overall Dimensions (L×W×H) | MT-65: 21000×1200×2200 mm; MT-70: 23000×1500×2200 mm; MT-75: 24000×1500×2800 mm; MT-85: 28000×3500×4300 mm |
| Control System | PLC and MCC centralized control |
| Line Stations | Mixer → Screw Conveyor → Twin-Screw Extruder → Air Conveyor → Dryer → Hoister → Flavoring Drum & Oil Sprayer → Cooling Machine → Packing Machine |
| Flaking Machine Roller Material | Cast iron |
| Flaking Machine Shaft Material | 45# steel |
| Flaking Machine Frame Material | Carbon steel |
| Flaking Machine Capacity Range | 100–400 kg/h (basis not stated in source — confirm raw material and product thickness) |
| Hot Air Roaster Max Temperature | 400 °C |
| Hot Air Roaster Heating Source | Electric or gas (configurable) |
| Hot Air Roaster Capacity Range | 100–400 kg/h (basis not stated in source — confirm raw material and product format) |
| Dryer Heating Method | Electric or gas |
| Dryer Layers | Three, five, or seven |
| Dryer Capacity | 100–500 kg/h (basis not stated in source — confirm moisture reduction target) |
| Sugar Spraying System Total Power | 28.75 kW |
| Sugar Spraying System Roller Size | Ø600×2700 mm |
| Vertical Packing Machine Models | 420 / 520 / 620 / 720 |
| Raw Material Compatibility | Corn, rice, millets, wheat, oat, barley (powder, flour, or grits form) |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Plain corn flake production | Degerminated corn grits at controlled moisture |
| Sugar-coated and honey-ring cereal | Corn, wheat, or oat flour blends with post-extrusion syrup coating |
| Cocoa flakes and chocolate loops | Wheat-corn blend with cocoa powder incorporated pre-extrusion |
| Fortified breakfast cereal | Multi-grain flour with heat-sensitive vitamin premix added post-drying |
| Oat-based flaked cereal | Rolled or steel-cut oat with modified starch binder |
| Crunch corn balls and star shapes | Corn or rice grits with interchangeable die plates |
Why "Nominal Capacity" Misses the Real Extrusion Story
A breakfast cereal line quoted on a single output figure often fails the moment the buyer switches from standard corn grits to a high-fibre oat blend — the starch gelatinisation window shifts, and the flakes shatter instead of holding their shape. Matching the screw profile and barrel temperature to your specific raw material is what actually determines usable throughput.
I have watched customers sign off on a capacity number, then spend months re-tuning after delivery because nobody checked how their recipe behaved under shear. The corn flakes extrusion line technology only delivers when the die geometry, moisture input and residence time are all validated against the flour or grits you will actually run. [NEED_CITE: starch gelatinisation temperature ranges across common cereal grains]
Shear, Moisture and the Gelatinisation Window
The twin-screw configuration generates both conveying and mixing action, which is critical when cereal blends contain components with different gelatinisation temperatures. Barrel zones are independently heated, allowing the operator to ramp temperature gradually so that starch granules swell uniformly before the dough reaches the die. If moisture is too low entering the extruder, the melt fractures at the die face; too high, and the extrudate sticks to the flaking rollers downstream.
Die Geometry and Flake Density Control
Die orifice diameter and land length together set the expansion ratio of the extrudate rope before it enters the flaking station. A shorter land produces a more expanded rope that yields a lighter, more porous flake after roasting — suited to markets that expect a quick-melt bowl life. A longer land compresses the melt, giving a denser rope that flattens into a thicker flake with extended crispness retention. [NEED_CITE: die land length influence on extrudate expansion in cereal processing]
Reading the Spec Sheet Beyond the Motor Rating
Installed power and real power consumption diverge noticeably across the MT-65, MT-70, MT-75 and MT-85 models, reflecting differences in screw diameter, barrel length and the number of independently controlled heating zones. A higher installed motor rating does not automatically mean more output — it means the extruder can maintain torque when running viscous, high-protein doughs that would stall a smaller unit. The PLC logs amperage draw per zone, so process engineers can spot recipe drift before it affects flake texture. Dryer layer count (three, five or seven) must be selected to match the moisture reduction target; underspecifying layers forces slower line speed and bottlenecks throughput at the roasting stage. Cast-iron flaking rollers with water cooling maintain gap tolerance under continuous load, which directly controls flake thickness uniformity before the hot-air roaster finishes the product at up to 400 °C.
The Cost of Skipping Material-Specific Tuning
When screw elements are selected from a generic catalogue rather than matched to a buyer’s grain blend, the first sign of trouble is usually inconsistent flake thickness — some pieces too thin and brittle, others too dense to puff correctly in the roaster. Downstream, the sugar-spraying drum coats unevenly because surface area varies piece to piece. Customers then blame the roaster or the coater, when the root cause sits inside the extruder barrel. [NEED_CITE: post-extrusion coating uniformity dependence on extrudate geometry]
What Makes This Line Hold Up Past Commissioning
The testing workshop runs your actual raw material before the line is crated, generating a trial-run report that documents screw arrangement, barrel temperatures and die selection — so commissioning on-site is verification, not discovery. Line layout calculations match throughput at every station from mixer to packing, preventing the common trap where the extruder outpaces the dryer. Electrical schematics are drawn with your facility voltage and frequency confirmed before production begins, avoiding the weeks-long delay of rewiring control cabinets on arrival. Spare wear parts lists ship with the line, so the first screw or die replacement does not become an emergency search.
Documentation & Verification
- Line layout with station-by-station throughput calculation for your cereal format
- Screw and die configuration record matched to your grain blend and target flake density
- Trial-run report on your raw material produced in the testing workshop before dispatch
- Electrical schematic with voltage, frequency and PLC language confirmed to your facility
- CE declaration of conformity and ISO certificate included in shipping documentation
- Operation and maintenance manual with wear-parts replacement intervals
Installation, Commissioning & Support
- Foundation plan accounts for the full 21–28 m line length and dryer layer height clearance
- Power supply sizing based on the confirmed real-power draw of your selected model and dryer heating source
- Extruder barrel sections shipped disassembled and re-aligned on site to maintain concentricity
- PLC commissioning includes recipe storage for each cereal format you intend to produce
- Operator training covers screw-element sequencing and flaking-roller gap calibration
- Wear-parts kit with spare screw elements, die plates and flaking-roller bearings supplied at shipment
What We Need from You to Size the Line
Confirm the grain or flour blend, moisture content at the mixer outlet, and the specific flake format you are targeting — plain, sugar-coated, cocoa, or multi-grain. Provide your facility voltage, frequency and available floor length so the layout fits without compromising dryer residence time. If you are developing a new recipe, tell us whether a trial run on your raw material in our testing workshop should precede the build.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal raw materials?
A: We start from the starch composition and protein level of your grain blend, then arrange conveying, kneading and reverse-screw elements to hit the gelatinisation degree your flake format requires. The configuration is documented and shipped with the line so you can replicate or adjust it later.
Q: How many independently controlled heating zones are on the extruder barrel?
A: Zone count varies by model — MT-65 through MT-85 — with each zone monitored and logged by the PLC. This allows the operator to build a gradual temperature profile that matches the gelatinisation curve of the specific raw material being processed.
Q: How does the flaking roller gap affect final product behaviour?
A: The cast-iron rollers are water-cooled and adjustable, setting flake thickness before the hot-air roaster. A tighter gap yields a thinner, faster-toasting flake; a wider gap leaves more moisture for the roaster to drive off, extending crispness and bowl life.
Q: Can the line run a trial on my specific raw material blend before shipment?
A: Yes. The in-house testing workshop runs your flour or grits through the extruder and flaking station, producing sample flakes. A trial-run report documenting screw setup, temperatures and product density is delivered before the line is packed.
Q: How is starch gelatinisation degree monitored during extrusion?
A: The PLC tracks barrel temperature per zone, motor amperage and screw speed in real time, storing batch data for traceability. Operators correlate these readings with periodic off-line gelatinisation tests to confirm the process stays within the window your recipe demands.


