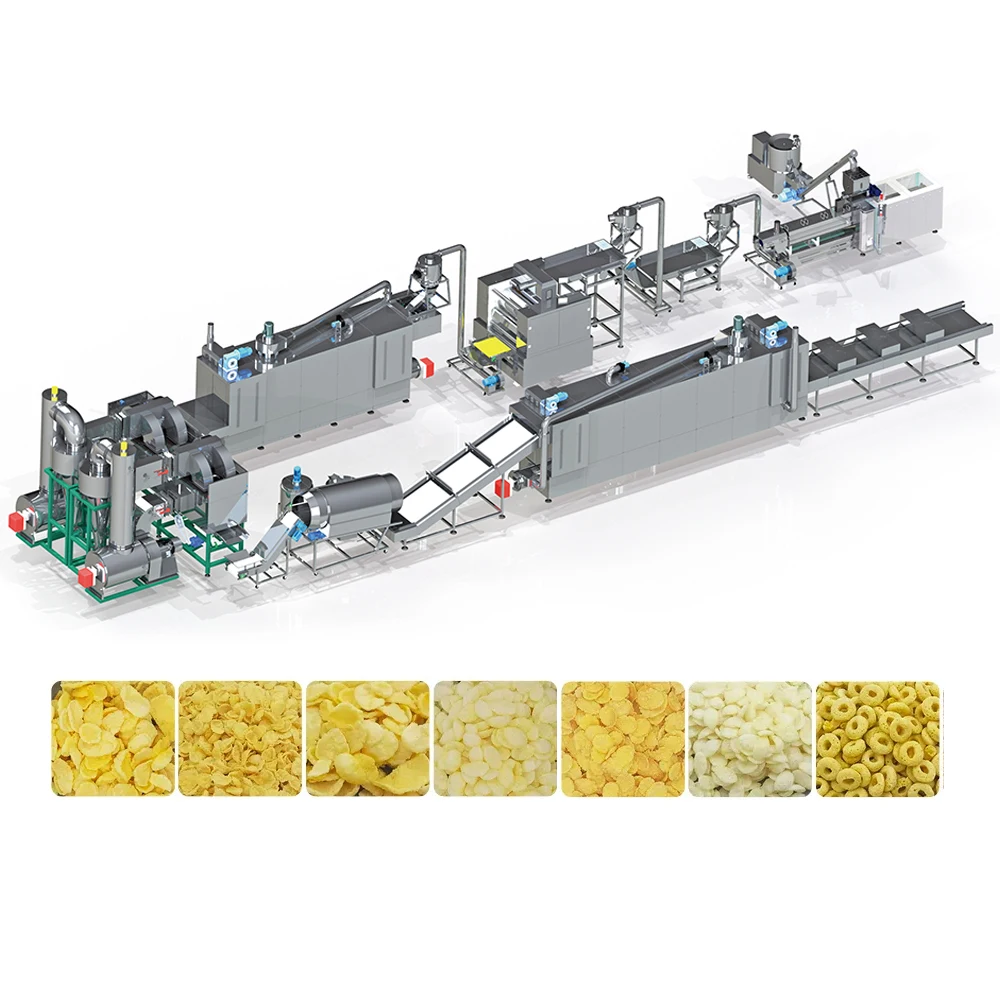
Screw configuration matched to your cereal blend — We specify screw profile and die geometry to the buyer’s actual grain powder and target flake density, verified by trial runs on customer raw material before the extruder leaves our testing workshop.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-75 Twin Screw Extruder |
| Product Type | Corn Flakes Breakfast Cereal Production Line |
| Screw Type | Twin Screw |
| Installed Power (MT75) | 210 kW |
| Power Consumption (MT75) | 150 kW |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material / moisture / product format) |
| Overall Dimensions (MT75) | 45 × 1.5 × 3.5 m |
| Available Models | MT70, MT85, MT75 |
| MT70 Installed Power / Consumption | 160 kW / 120 kW |
| MT70 Output Capacity | 150–200 kg/h (basis not stated in source — confirm raw material / moisture / product format) |
| MT70 Overall Dimensions | 41 × 1.5 × 2.2 m |
| MT85 Installed Power / Consumption | 190 kW / 140 kW |
| MT85 Output Capacity | 300–400 kg/h (basis not stated in source — confirm raw material / moisture / product format) |
| MT85 Overall Dimensions | 43 × 1.5 × 3.2 m |
| Flaking Machinery Capacity | 200–300 kg/h (basis not stated in source — confirm raw material / product format) |
| Extruder Working Principle | Feeding system, extruding system, cutting system, heating system, gearing system, controlling system |
| Key Features | Automatic lubricating, cooling function, screw made by special wear-resistant tech |
| Flaking Machinery Control | PLC control system; hydraulic system for double rollers; double motors for separate roller driving; infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Hot Air Roasting Oven | Vibrating pan with high temperature spraying tubes; conciliation burner combustion chamber; two separate circulating fans and cyclone dust removal device |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Control System | PLC and MCC |
| Voltage & Frequency | Customized to customer’s local voltage |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Powder of corn, processed through extrusion, flaking, drying, and hot air roasting |
| Sugar-coated corn flakes | Corn powder base with sugar spraying and coating stages added post-roasting |
| Multi-grain breakfast cereals | Blends of rice, wheat, oat, and barley powder extruded into various shapes |
| Shaped cereal formats | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart via extruder mould adjustment |
What Generic Screw Profiles Do to Your Flake Density
A corn flakes extrusion production line built on copied screw geometry will produce inconsistent gelatinisation and unpredictable flake behaviour downstream.
I spent years commissioning cereal lines across the Middle East, and the most common failure at startup is not electrical or mechanical — it is product quality. The extruder runs, the flaker turns, but the flakes come out too dense, too fragile, or with uneven browning after roasting. In almost every case, the root cause traces back to a screw configuration that was never adjusted for the buyer’s specific grain blend, particle size, or moisture content [NEED_CITE: twin-screw extrusion parameter effects on starch gelatinisation]. A corn flakes extrusion production line is only as capable as its extrusion stage, and that stage must be engineered around your actual raw material, not a default template.
How Screw Geometry Governs Gelatinisation
The twin-screw configuration in the MT-75 allows operators to adjust screw element sequencing along the barrel to control shear intensity and residence time. For corn-based formulations, achieving the correct degree of starch gelatinisation before the material reaches the die is critical — under-gelatinised dough will not flake evenly, while over-processed material loses the structural integrity needed for a crisp final product. The corn flakes extrusion production line depends on this balance, and it shifts depending on whether you run pure corn, an oat blend, or a multi-grain mix.
Barrel Temperature Zones and Moisture Management
The barrel is divided into multiple heating zones, each independently controlled to build a temperature profile that matches the raw material’s gelatinisation curve. Moisture injection points work in tandem with barrel heat to manage dough plasticity before the die. When I commission a line running coarser corn grits, the barrel profile typically needs adjustment compared to fine corn flour — the residence time and shear energy required to fully hydrate and gelatinise the starch differ substantially. Getting this wrong means the flaking station downstream receives material that compresses unevenly, producing flakes with variable thickness and inconsistent crunch after roasting [NEED_CITE: barrel temperature profiling in twin-screw cereal extrusion].
Reading the Specs That Actually Matter
The MT-75’s 210 kW installed power and 150 kW running consumption reflect the energy available for shear and thermal processing within the barrel. The 45-metre overall line length encompasses every station from mixing through packing, which matters when planning factory floor space and utility routing. The twin-screw design provides self-wiping action that reduces material hang-up and improves batch-to-batch consistency compared to single-screw alternatives — a practical advantage when switching between corn, oat, and barley formulations. The PLC and MCC control system allows operators to store and recall parameter sets for each raw material blend, reducing setup time and eliminating guesswork during product changeovers.
The Hidden Cost of Unmatched Line Stations
When the extruder output is not matched to the flaking, drying, and roasting capacities, the entire line suffers. An extruder producing material faster than the flaker can process forces operators to reduce feed rates, which alters residence time in the barrel and shifts gelatinisation away from the target window. Similarly, a dryer or roasting oven that cannot handle the line’s throughput creates a bottleneck where partially dried flakes accumulate, losing moisture unevenly and developing inconsistent colour and texture. These mismatches rarely appear in a quotation — they surface only during production, when output falls short and product quality drifts outside specification [NEED_CITE: throughput matching in cereal production line engineering].
Why Procurement Should Start with Your Raw Material
Every corn flakes extrusion production line we configure begins with the buyer’s actual grain powder, not a generic specification sheet. Our in-house testing workshop runs your raw material through the extruder before shipment, generating a trial run report that documents screw configuration, barrel temperature profile, moisture settings, and the resulting product texture. The screw and die configuration record travels with the machine, giving your process engineers a verified baseline for production. Line layout and capacity calculations ensure that the extruder, flaker, dryer, and roasting oven are throughput-matched to prevent bottlenecks. Pre-sales consultation covers voltage confirmation, control language, and utility planning so that commissioning proceeds without electrical or interface delays. CE and ISO certification documentation supports import compliance in your destination market.
Documentation & Verification
- Line layout and capacity calculation showing throughput balance across all stations
- Screw and die configuration record matched to your specific cereal raw material
- Trial run report on customer raw material documenting extrusion parameters and product texture
- Machine specification sheet with barrel zone map, screw profile, and electrical schematic
- CE declaration of conformity and ISO certificate for import clearance
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Factory floor layout planning based on the 45 × 1.5 × 3.5 m MT-75 line footprint
- Electrical supply verification for the 210 kW installed power requirement and local voltage standard
- PLC and MCC control system configured to operator language before commissioning begins
- Trial parameter sets loaded from the pre-shipment testing workshop run on your raw material
- Screw and die wear parts inventory established with recommended first replacement schedule
- Barrel zone calibration and flaker hydraulic pressure setting during on-site startup
Preparing Your Inquiry
To configure the extrusion stage correctly, we need your raw material specification including grain type, particle size distribution, and typical moisture content. Share your target flake density and crunch texture expectations, along with the daily production volume you plan to sustain. Confirm your local voltage and frequency standard, preferred control language, and available factory floor dimensions so we can propose a matched line layout.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal raw materials like corn versus oat?
A: Screw element sequencing is adjusted based on the raw material’s starch composition, particle size, and gelatinisation temperature. Corn typically requires a different shear profile than oat or barley blends. We document the screw configuration for your specific material during the pre-shipment trial run, providing a verified baseline that your operators can reference and adjust from during production.
Q: What barrel temperature profile is needed for proper starch gelatinisation in corn flakes?
A: The profile depends on your corn variety, particle size, and moisture content at the feed point. Multiple barrel zones are set to build a progressive temperature curve that fully gelatinises starch without degrading it. We establish the correct profile during the testing workshop trial on your actual raw material and record it in the machine specification sheet delivered with the line.
Q: How does extrusion shear affect final flake density and crunch after roasting?
A: Shear intensity, controlled by screw element design and screw speed, determines how thoroughly the starch matrix is developed before the material exits the die. Insufficient shear produces dense, hard flakes; excessive shear creates fragile structure that shatters during flaking. The twin-screw design allows precise shear adjustment across the barrel length to target the density your market expects.
Q: Can a trial run on my raw material be performed before the extruder ships?
A: Yes. Our in-house testing workshop runs your actual grain powder through the extruder before dispatch. The trial run report documents screw configuration, barrel temperatures, moisture settings, throughput rate, and product texture. This eliminates the risk of discovering raw material incompatibility after the machine is installed in your factory.
Q: How is extruder throughput matched to downstream flaking and drying stations?
A: Line capacity calculations ensure the extruder output aligns with the flaker, dryer, and roasting oven capacities. The flaking machinery in this line processes 200–300 kg/h, and all station capacities are verified during layout design to prevent bottlenecks that force operators to reduce feed rates and compromise extrusion consistency.