Screw Profile Engineering — Every corn flake extrusion run starts with a screw configuration and die layout mapped to the buyer’s actual grain blend, not a generic catalog build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Production Line |
| Extruder Type | Twin Screw |
| Installed Power (MT70) | 160 kW |
| Installed Power (MT85) | 190 kW |
| Installed Power (MT75) | 210 kW |
| Power Consumption (MT70) | 120 kW |
| Power Consumption (MT85) | 140 kW |
| Power Consumption (MT75) | 150 kW |
| Output Capacity (MT70) | 150–200 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| Output Capacity (MT85) | 300–400 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| Output Capacity (MT75) | 300–500 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| Overall Dimensions (MT70) | 41 × 1.5 × 2.2 m |
| Overall Dimensions (MT85) | 43 × 1.5 × 3.2 m |
| Overall Dimensions (MT75) | 45 × 1.5 × 3.5 m |
| Voltage | 380V / 220V, configurable to site requirements |
| Flaking Machinery Control | PLC control system with hydraulic system for double rollers |
| Flaking Machinery Drive | Double motors for separate roller driving |
| Flaking Machinery Temperature Control | Infrared sensor |
| Dryer Heating Source | Gas / Electric |
| Roasting Oven | Hot air roasting with conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
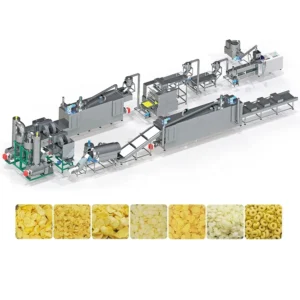
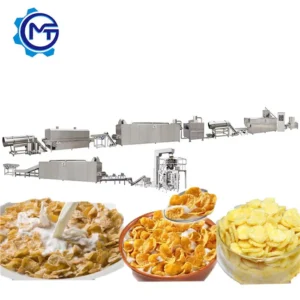
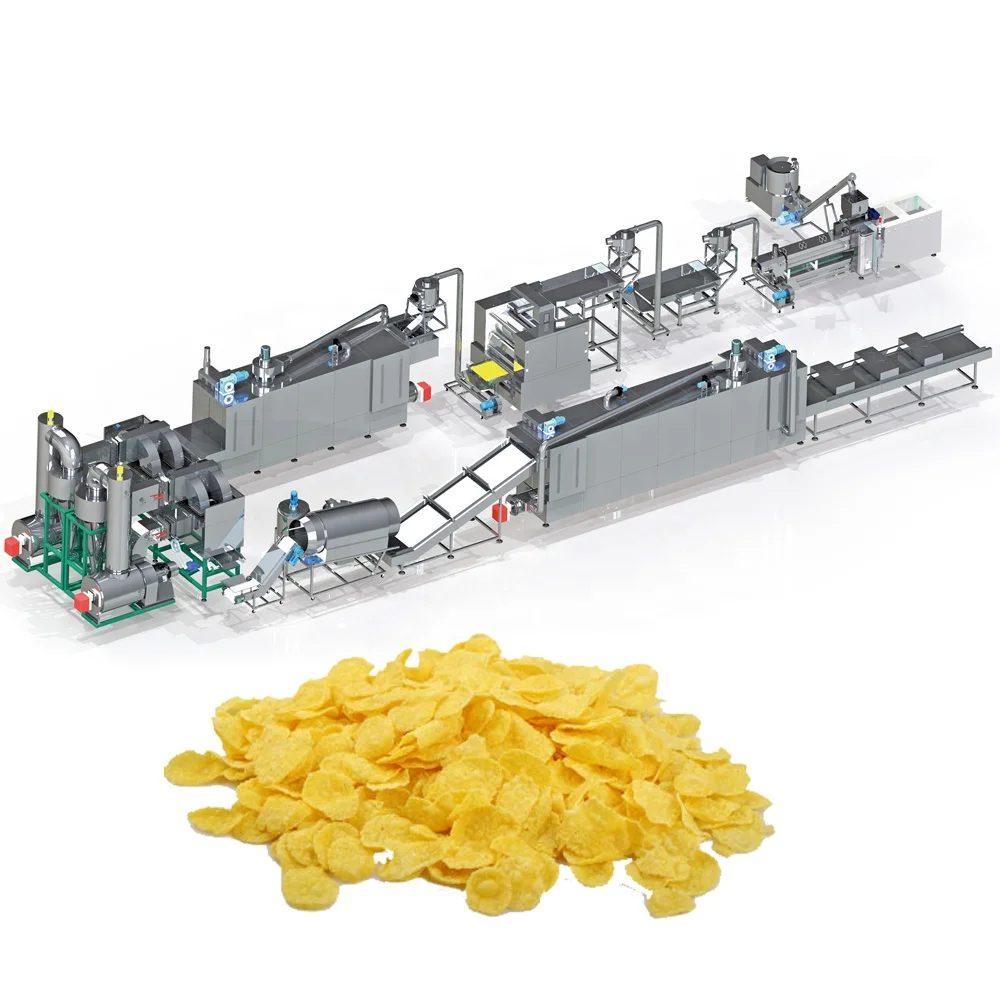
| Line Stations | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Coating → Cooling → Packing |
| Material | Stainless Steel (food-grade contact surfaces) |
| Assembly State | Complete production line |
| MOQ | 1 Set |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal retail | Corn grits or corn flour at controlled moisture |
| Sugar-coated corn flakes with extended bowl-life | Corn base with sugar or honey glaze via double-tumble coating |
| Multi-grain breakfast flakes | Rice, wheat, oat, and barley flour blends |
| Shaped cereal variants from the same extrusion platform | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart dies |
What Your Raw Material Moisture Does to "Rated" Throughput
Capacity numbers printed on a spec sheet mean nothing until they are tested against your grain source at your actual moisture level.
When a breakfast cereal producer quotes a Corn Flakes Extrusion Production Line specifications how to choose based on nameplate output alone, the gap between expectation and reality can be severe. I have watched a line lose half its throughput because the incoming corn flour sat three percentage points higher in moisture than the lab sample used for sizing. The extruder barrel could not flash off the extra water fast enough, the gelatinised mass refused to expand at the die face, and every flake came out with a hard centre that no amount of roasting could fix [NEED_CITE: starch gelatinisation thresholds relative to feed moisture in twin-screw extrusion]. Two weeks of screw profile adjustment and barrel zone tuning were needed before the line stabilised.
Screw Configuration Against Starch Gelatinisation Behaviour
The extrusion stage is where the Corn Flakes Extrusion Production Line specifications how to choose either succeeds or fails. Corn starch requires a specific combination of shear, residence time, and barrel heat to reach full gelatinisation without over-degrading the polymer chains. A twin-screw configuration lets the operator vary the pitch, kneading block angle, and reverse-flight sections zone by zone, tailoring the mechanical energy input to the exact amylose-to-amylopectin ratio of the incoming flour.
Barrel Temperature Profile and Flake Density Control
Each barrel section carries independent heating and cooling circuits. The profile typically starts lower in the feed zone to prevent premature gelatinisation that would cause surging, then climbs through the compression and metering zones to drive moisture flash-off at the die. The die orifice diameter and land length together set the pressure drop, which governs how much the extrudate expands before it hits the flaking rollers. Too much expansion produces a low-density flake that shatters during roasting; too little gives a dense, tough flake that never achieves the crispness the market expects [NEED_CITE: die land length effect on extrudate expansion ratio in cereal processing].
Reading the Power and Capacity Table Correctly
The installed power figures — 160 kW for the MT70, 190 kW for the MT85, 210 kW for the MT75 — represent the total connected load across extruder drive, preconditioner, and auxiliary motors. Actual power consumption sits noticeably lower under typical running conditions. The output ranges listed in the specifications table are not guaranteed rates; they shift with the raw material particle size, initial moisture, and target flake density. Any capacity discussion must begin with a sample of the buyer’s grain sent to the testing workshop for a documented trial run.
The Cost of Skipping the Extrusion Setup Stage
When a line ships with a generic screw build copied from a previous installation, the consequences surface during commissioning. The extruder may run, but the flake texture drifts outside specification — either too fragile for packing or too dense for acceptable bowl-life. Engineers then spend days on-site swapping screw elements and adjusting die configurations that should have been locked before the crate left the factory [NEED_CITE: on-site commissioning delays caused by incorrect screw configuration]. That downtime costs the buyer in idle labour, wasted raw material, and delayed market entry.
Why Sourcing From This Workshop Changes the Outcome
Screw configuration and die design are specified to each buyer’s raw material and target flake density, not pulled from a standard template. An in-house testing workshop runs the buyer’s actual grain through the extruder before shipment, generating a trial report that locks process parameters. Throughput is matched across every station — extruder, flaker, dryer, and roaster — under one supplier, so no single machine bottlenecks the rest. The PLC-controlled flaking machinery uses a hydraulic double-roller system with infrared temperature sensing to hold uniform sheet thickness across the full roller width. Pre-sales consultation extends through installation, commissioning, and operator training on the specific control configuration shipped to the site.
Documentation & Verification
- Line layout with throughput matching calculation between extruder, flaker, dryer, and roaster
- Screw and die configuration record tied to buyer’s raw material sample
- Trial run report from in-house testing workshop on customer-supplied grain flour
- Electrical schematic with voltage, frequency, and control language confirmed for destination country
- CE declaration of conformity and ISO certificate included in shipment package
- Operation and maintenance manual with wear parts list for screw elements and die plates
Installation, Commissioning & Support
- Foundations must accommodate the MT75 line footprint of 45 m length with level tolerance for the hydraulic flaking roller frame
- Dedicated power circuit sized for up to 210 kW installed load with voltage confirmed before cable pull
- Stations ship as pre-assembled modules; final mechanical and electrical connections completed on-site
- First-run parameter setting covers barrel zone temperatures, screw speed, and flaking roller gap to match trial report
- Operator training includes PLC interface navigation, infrared sensor calibration, and sugar coating drum adjustment
- Wear parts list covers screw elements, die plates, and flaking roller bearings with recommended stocking quantities
Before You Send an Enquiry
Prepare a representative sample of the corn flour or multi-grain blend you plan to run, along with the moisture range your supplier typically delivers. Specify the flake thickness and bowl-life target your market demands, plus the daily output you need to justify the investment. Confirm the voltage and frequency at your facility and the control language your operators will use, so the PLC interface and electrical schematics are configured correctly before the line ships.
Frequently Asked Questions
Q: How is screw configuration and L:D ratio selected for corn versus multi-grain raw materials?
A: Corn starch gelatinises at a different temperature and shear threshold than oat or wheat starch. The screw profile is built zone by zone — feed pitch, kneading block angle, metering length — matched to the specific grain blend and target flake density. Multi-grain recipes usually require a longer L:D ratio to give each starch fraction adequate residence time.
Q: What barrel temperature profile controls starch gelatinisation for proper flake expansion?
A: The feed zone stays relatively cool to prevent premature gelatinisation and surging. Temperature climbs through compression and metering zones to drive moisture flash-off at the die. The exact setpoints depend on the grain’s amylose content and initial moisture, which is why a trial run on the buyer’s actual flour is essential before locking parameters.
Q: How is output capacity verified against actual raw material and moisture content?
A: The buyer ships a representative flour sample to the testing workshop. A documented trial run is conducted on the specified extruder model, measuring throughput, flake density, and texture at the buyer’s moisture level. The resulting report accompanies the machine and serves as the baseline for commissioning.
Q: Can a trial run be performed on customer-supplied corn flour before shipment?
A: Yes. The in-house testing workshop is equipped for full extrusion and flaking trials. The buyer provides enough flour for multiple passes, and the trial report records screw configuration, barrel temperatures, die selection, and measured output so the line ships with validated process parameters.
Q: How are die design and flaking roller gap coordinated for target flake thickness?
A: Die orifice diameter and land length set the extrudate strand size and expansion ratio. The hydraulic double-roller flaking station then compresses each strand to the target sheet thickness, monitored by the PLC and infrared sensor. Roller gap and die selection are matched during the trial run to produce consistent flake density.