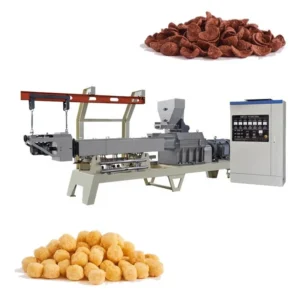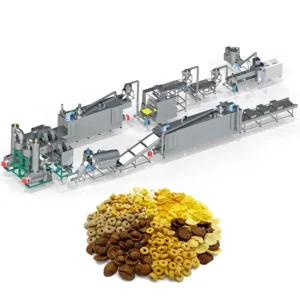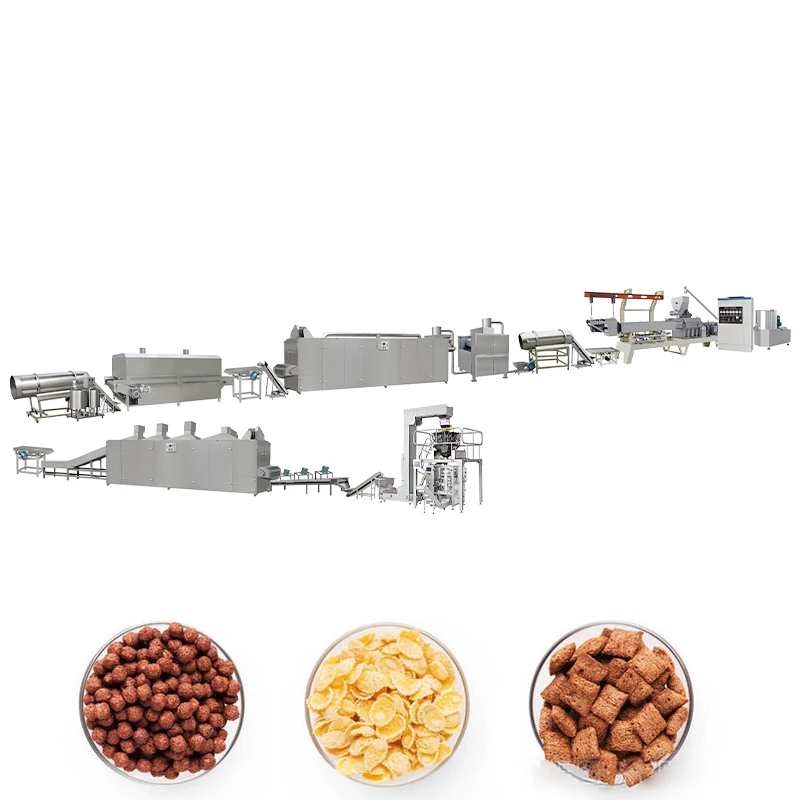
Precision-Matched Extrusion Parameters — Every screw element and die opening is selected against the buyer’s actual flour or grit formulation, ensuring target flake density and crispness before the line ships.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Breakfast Cereal Extrusion Production Line |
| Model Options | MT-65 / MT-70 / MT-85 / MT-75 |
| Screw Type | Twin-screw |
| Installed Power | MT-65: 84 kW · MT-70: 132 kW · MT-85: 239 kW · MT-75: 186 kW |
| Real Power Consumption | MT-65: 59 kW · MT-70: 92 kW · MT-85: 167 kW · MT-75: 140 kW |
| Output Capacity | MT-65: 120–150 kg/h (basis to be confirmed) · MT-70: 200–250 kg/h (basis to be confirmed) · MT-85: 300–400 kg/h (basis to be confirmed) · MT-75: 400–500 kg/h (basis to be confirmed) |
| Overall Dimensions (L×W×H) | MT-65: 21000×1200×2200 mm · MT-70: 23000×1500×2200 mm · MT-85: 28000×3500×4300 mm · MT-75: 24000×1500×2800 mm |
| Control System | PLC with real-time data storage, monitoring, alarm and reminder functions; MCC integrated |
| Extruder Design | 3D software designed, analogue simulation, computer-tested for precision |
| Flaking Machine | Adjustable roller gap; water-cooled cast iron rollers; 45# steel shafts; carbon steel frame |
| Hot Air Roaster | Up to 400 °C; electric or gas heating; high-pressure blower |
| Dryer | Three, five, or seven layers; electric or gas heating; adjustable mesh belt speed |
| Sugar Spraying System | Total power 28.75 kW; roller approx. Ø600×2700 mm |
| Packing Machine | Vertical automatic with combination head weigher; models 420/520/620/720 |
| Line Stations | Mixer → Screw Conveyor → Twin Screw Extruder → Air Conveyor → Dryer → Hoister → Flavouring Drum & Oil Sprayer → Cooling Machine → Packing Machine |
| Raw Material Form | Powder (flour) or grits |
| Standards | CE certified · ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Standard corn flakes breakfast cereal | Corn flour or corn grits |
| Multi-grain breakfast cereal | Blends of corn, rice, millets, wheat, oat, barley in powder or grits form |
| Sugar-coated corn flakes | Corn base with sugar spraying and flavouring drum finish |
| Plain and savoury flakes | Corn or multi-grain without sweet coating |
| Vegan breakfast cereal formulations | Plant-based flour and grit blends with no animal-derived ingredients |
What "Rated Capacity" Doesn’t Tell You About Flake Texture
A throughput figure is meaningless if the screw configuration was never matched to the buyer’s raw material.
I once helped set up a corn flakes line for a Southeast Asian producer. We ran trial material from our local Shandong corn flour and the expansion, thickness, and crunch were exactly on target. When the machine arrived on site and they fed their own higher-fat corn variety, the flakes came out thick, dense, and far too hard for breakfast cereal. The rated output of the extruder was never the problem — the screw elements and barrel temperature profile had been specified for a completely different starch and fat ratio. That single mismatch can shut down a production schedule before the first full shift is completed [NEED_CITE: impact of raw material fat content on extrusion expansion ratio]. Every corn flakes extrusion production line technology discussion should start with the buyer’s exact flour or grit blend, not with a catalogue throughput number.
Barrel Temperature Profiling and Starch Gelatinisation
Corn flakes require a controlled gelatinisation window inside the extruder barrel. Too little heat and the starch remains raw, producing a gritty mouthfeel; too much and the dough over-expands, leading to fragile flakes that shatter in the bowl. The PLC on this line stores the temperature set-point for each barrel zone, letting operators reproduce the exact profile run after run. Real-time monitoring catches drift before it reaches the die, which is critical when switching between a pure corn formulation and a multi-grain blend with different gelatinisation onset temperatures.
Screw Configuration for Flake Density Control
The density of a finished corn flake — and therefore its bowl life — is determined largely by the arrangement of conveying, kneading, and reverse elements on the twin screws. A higher proportion of kneading blocks increases shear and drives more complete starch conversion, yielding a denser, longer-lasting flake. Fewer kneading blocks leave the dough more open, producing a lighter flake that may suit a sugar-coated SKU but will collapse under milk weight. The screw configuration is selected during pre-build trials and documented in a configuration record that travels with the line, so future rebuilds start from a known baseline rather than guesswork [NEED_CITE: twin-screw element arrangement and food extrusion density outcomes].
How Moisture, Shear, and Die Geometry Interact
Moisture content at the feeder, screw speed, and die opening size together govern expansion ratio. Higher feed moisture lowers melt temperature and reduces die-swell, giving a thinner, crisper flake after roasting. Lower moisture raises shear heating and pushes expansion higher — useful for a puffed cereal format but wrong for traditional corn flakes. Die geometry adds another layer: a smaller die land increases back-pressure and homogenises the melt, while a larger opening eases flow but can allow density variation across the strand. These three variables must be balanced as a system, not adjusted in isolation.
Reading the Specs That Actually Matter
Installed power versus real power consumption tells you how much electrical headroom the line leaves for start-up surges and heavier formulations. The MT-85, for example, shows 239 kW installed against 167 kW real consumption — a gap that reflects motor sizing for peak torque during cold starts and high-viscosity dough. The flaking machine’s water-cooled cast iron rollers maintain a stable surface temperature across long runs, preventing the dough sheet from sticking and tearing as ambient workshop temperature rises. Dryer layer count — three, five, or seven — is selected based on the moisture removal curve of the specific flake thickness being produced; more layers give longer residence time at lower belt temperatures, reducing case-hardening on thick flakes.
The Hidden Cost of a Generic Screw Build
When an extruder leaves the factory with a screw configuration copied from a different application — say, pet food kibble — the first corn flakes trial usually shows over-expanded, low-density pellets that flatten unevenly on the flaking rolls. The operator then slows the line, raises barrel moisture, or swaps die plates, each change introducing new variables. Weeks pass before texture stabilises, and the resulting flake may still fall short of the crispness and bowl life that retailers expect [NEED_CITE: consequences of incorrect screw configuration on cereal flake quality]. Rebuilds, element replacements, and lost production shifts add up long before anyone questions the original specification.
Why This Line Is Engineered Differently
Complete line throughput is matched station by station, so the extruder output, flaking roll capacity, roaster throughput, and dryer residence time all align without bottlenecks. Screw configuration and die design are specified against the buyer’s raw material formulation, not pulled from a generic catalogue build. An in-house testing workshop runs the buyer’s actual flour or grits before shipment, producing a trial report that locks expansion ratio, flake density, and texture. The PLC records all barrel zone temperatures and screw speeds in real time, giving the buyer a reproducible baseline from the very first commercial run. CE and ISO certification is maintained across the product range, and electrical schematics are confirmed against the buyer’s facility voltage and frequency before production begins.
Documentation & Verification
- Line layout and capacity calculation matching every station from mixer to packer
- Screw and die configuration record showing exact element arrangement for the buyer’s blend
- Trial run report on buyer’s raw material confirming expansion, density, and flake texture
- Electrical schematic with voltage and frequency matched to the target facility
- CE declaration of conformity and ISO certificate included with shipment
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation plan accounts for the full line length up to 28 m on the MT-85 model
- Dedicated power circuit sized to the installed kW rating of the selected model
- PLC interface language confirmed before dispatch to match operator requirements
- First-run parameter setting based on the pre-shipment trial report baseline
- Wear parts list covering screws, dies, and flaking roll bearings for initial spares stock
- Scheduled maintenance intervals documented for dryer mesh belt and roaster blower
Before You Request a Quote
To size the extruder and balance the downstream stations, share the raw material form — flour or grits — along with the grain blend composition and any fat or fibre percentages. Provide the target flake thickness and the desired coating type so the sugar spraying system and flavouring drum can be specified. Confirm your facility voltage, frequency, and the control interface language your operators need. If you have an existing dryer or packer that must be integrated, include those model details so the throughput calculation accounts for them.
Frequently Asked Questions
Q: How is the screw configuration chosen for a multi-grain blend versus pure corn?
A: Each grain has a different starch gelatinisation temperature and protein matrix. We adjust the ratio of kneading blocks to conveying elements so that the shear profile matches the slowest-gelatinising component in the blend. Trial runs on the buyer’s actual mix confirm the arrangement before the screw set is finalised for shipment.
Q: What barrel temperature profile achieves proper gelatinisation without over-expansion?
A: Typical profiles use a stepped increase from the feed zone to the metering zone, then a slight reduction at the die to control swell. The exact set-points depend on the formulation’s moisture and fat content. The PLC stores and reproduces the validated profile, preventing operator drift across shifts.
Q: Can I send raw material for a trial run before placing an order?
A: Yes. Our testing workshop runs your flour or grits on the same screw configuration proposed for your line. We measure expansion ratio, flake density, and texture, then issue a trial report. Parameters are locked before the extruder is built, so the first commercial run starts from a proven baseline.
Q: How is throughput balanced between the extruder, flaking rolls, and roaster?
A: Each station is sized so its maximum capacity meets or slightly exceeds the extruder’s real output on the buyer’s formulation. This prevents material queuing at the flaking rolls or starvation at the roaster. The line layout document shows the calculated flow rate at every transfer point.
Q: How do you control flake density and crispness through die design?
A: Die land length and opening diameter set the back-pressure and melt homogeneity at the extruder exit. Longer die lands increase pressure, producing a more uniform strand that flakes evenly. Combined with adjustable roller gap and roaster temperature, this gives precise control over final flake density and bowl-life crispness [NEED_CITE: die land geometry and extrudate uniformity in cereal processing].