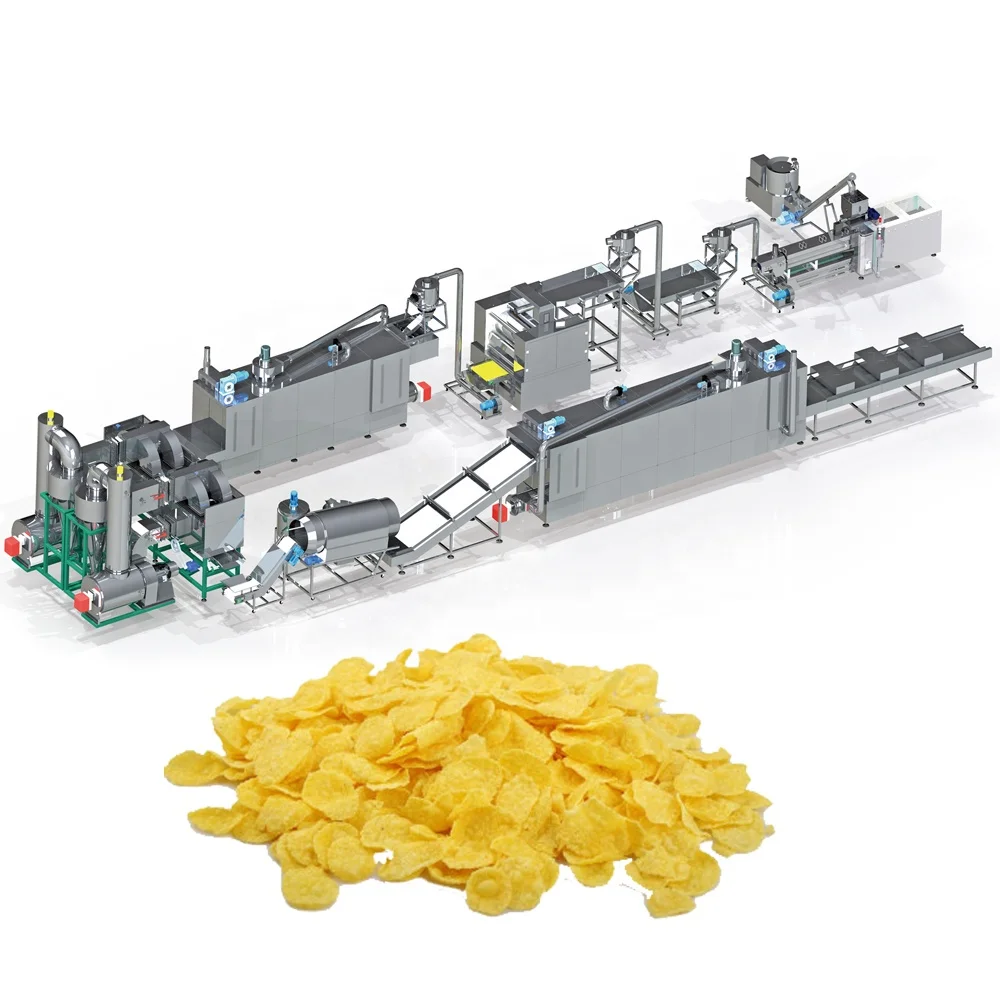
Screw Geometry Matched to Raw Material — Die design and barrel temperature profile configured around the buyer’s actual corn variety and moisture level, verified by trial run before the extruder leaves the workshop.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Corn Flakes Extrusion Line |
| Model Options | MT70 / MT85 / MT75 |
| Extruder Type | Twin Screw |
| Installed Power | 160 kW (MT70) / 190 kW (MT85) / 210 kW (MT75) |
| Power Consumption | 120 kW (MT70) / 140 kW (MT85) / 150 kW (MT75) |
| Output Capacity | 150–200 kg/h (MT70, basis to be confirmed) ; 300–400 kg/h (MT85, basis to be confirmed) ; 300–500 kg/h (MT75, basis to be confirmed) |
| Overall Dimensions (L×W×H) | 41 × 1.5 × 2.2 m (MT70) / 43 × 1.5 × 3.2 m (MT85) / 45 × 1.5 × 3.5 m (MT75) |
| Control System | PLC (flaking machinery), MCC available |
| Flaking Machinery Drive | Double motors for separate roller driving, hydraulic system |
| Flaking Temperature Control | Infrared sensor for even temperature pipe control |
| Dryer Heating Source | Gas / Electric |
| Roasting Oven | Hot air roasting, two circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Screw Feature | Automatic lubricating, cooling function, wear-resistant material |
| Assembly State | Complete line from mixing through extrusion, flaking, drying, roasting, and coating |
| Warranty | 24 months, lifetime service |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Sugar-coated breakfast corn flakes | De-germed corn grits with sugar syrup coating |
| Natural corn flakes without coating | De-germed corn grits or whole corn meal |
| Multi-grain breakfast cereal flakes | Blends of corn, wheat, rice, or oat grits |
| Cereal bar raw material | Extruded and flaked grain granules for downstream binding |
| Alternative grain-based puffed snacks | Rice, wheat, or sorghum formulated for flake expansion |
What a Nameplate Capacity Figure Leaves Out About Corn Flake Extrusion
The number on the motor plate does not tell you whether your corn will gelatinise fully before it reaches the flaking rollers.
A capacity figure quoted without raw material context creates a false expectation. De-germed corn grits at one moisture level behave completely differently from whole corn meal at another. I have seen lines where the extruder was rated for a certain throughput on standard test flour, but when the buyer switched to their local corn supply with higher fibre and moisture, the granules came out undercooked and the flakes turned hard instead of crisp. The twin screw extruder corn flakes process depends on matching screw configuration and barrel temperature to the starch behaviour of your specific grain. Without that match, throughput numbers mean very little [NEED_CITE: raw material variability in cereal extrusion processing].
Screw Configuration and Starch Gelatinisation
The core of corn flakes extrusion technology sits inside the barrel. A twin screw setup allows the flight depth, pitch, and kneading block arrangement to be changed section by section. For corn flakes, the objective is complete starch gelatinisation without premature expansion — the dough must cook thoroughly under pressure and only begin to expand once it exits the die. If the screw elements generate too much shear too early, the starch breaks down and the resulting flakes lack structural integrity. The configuration must account for corn variety, particle size, and incoming moisture content.
Barrel Temperature Profile and Moisture Control
Each barrel zone is independently heated, allowing a temperature gradient that moves the material from hydration through cooking to die forming. Moisture is typically introduced at the feed zone and must be precisely metered. Too little water and the starch never fully gelatinises; too much and the extrudate becomes sticky, fouling the flaking rollers downstream. The barrel profile works together with screw speed and feed rate to hold the material in the barrel for the exact residence time needed [NEED_CITE: residence time distribution in twin screw extrusion for breakfast cereals].
Reading the Specifications Beyond the Motor Rating
Installed power and power consumption figures tell you about the energy envelope but not about how that energy is distributed. The MT70 at 160 kW installed and 120 kW consumption suits a smaller operation running a single shift, while the MT75 at 210 kW installed supports higher throughput demands. The critical parameter for corn flake quality is not total power but how the screw elements convert mechanical energy into shear and heat within the barrel. The PLC-controlled flaking machinery uses infrared sensors to monitor roller temperature, ensuring the extrudate enters the rollers at the correct surface condition for even pressing. The hydraulic system for double rollers allows precise gap adjustment, which directly determines flake thickness and, ultimately, bowl-life performance in milk.
The Hidden Cost of a Generic Screw Build
When screw and die configurations are copied from a standard template rather than designed for the buyer’s corn supply, the problems show up after installation. Flakes may toast unevenly because the granule density varies from batch to batch. The roasting oven cannot compensate for inconsistent upstream forming — hot air circulation and the two separate circulating fans work best when every flake enters at the same moisture and thickness. Buyers who skip the raw material trial often spend weeks adjusting parameters on-site, losing production time and raw material while chasing a stable output [NEED_CITE: cost of unplanned downtime in food extrusion startup].
Why This Line Is Configured Before It Is Built
The screw configuration and die design are specified to the buyer’s raw material and target flake density, not pulled from a generic catalogue. An in-house testing workshop runs trial extrusions on the customer’s actual corn supply before the line ships, locking in barrel temperature, screw speed, and moisture settings. Throughput is matched across every station — extruder output is calculated against flaking roller capacity, dryer belt length, and roasting oven residence time so no single station bottlenecks the line. Twin screw expertise covers corn flakes alongside pet food, aquatic feed, and snack applications, meaning process knowledge transfers across product formats. The PLC control system records all extrusion parameters during the trial, providing a reference baseline that the buyer’s operators can reproduce from day one of commercial production.
Documentation & Verification
- Screw and die configuration record matched to your corn variety and target flake density
- Trial run report on your actual raw material executed in the testing workshop before dispatch
- Line layout showing throughput balance across extrusion, flaking, drying, and roasting stations
- Electrical schematic with voltage and frequency confirmed for your facility’s power supply
- Operation and maintenance manual covering screw wear inspection and roller gap calibration
- CE declaration of conformity and ISO certificate for customs and regulatory compliance
Installation, Commissioning & Support
- Floor space of 41–45 m in length requires a level concrete slab with drainage for wash-down
- Dedicated electrical circuit sized for up to 210 kW installed load with correct voltage and frequency
- Line ships in modular sections for sequential assembly from mixing station through packing end
- First-run commissioning includes barrel temperature calibration and flaking roller gap setting
- Operator training covers PLC parameter adjustment, screw lubrication checks, and die cleaning
- Wear parts list provided for screws, dies, and roller surfaces with recommended replacement intervals
What We Need to Configure Your Line
Send us a sample of the corn grits or corn meal you plan to process, along with the typical moisture content at your receiving dock. Specify whether you intend to produce sugar-coated flakes, natural flakes, or both on the same line. Let us know your target daily output, available floor space and ceiling height, and the voltage and frequency at your facility so we can size the electrical system and confirm control language before production begins.
Frequently Asked Questions
Q: How is screw configuration selected for different corn varieties and moisture levels?
A: The screw elements are arranged based on the starch content, fibre level, and incoming moisture of your specific corn supply. High-fibre de-germed grits require different kneading block placement than whole corn meal. We run your raw material in the testing workshop to determine the flight depth and pitch sequence that achieves full gelatinisation without premature expansion.
Q: What barrel temperature profile is needed for full starch gelatinisation without premature expansion?
A: The barrel is divided into independently heated zones, typically starting lower at the feed section and rising through the cooking zones before a slight drop at the die. This gradient hydrates the starch gradually, then cooks it under pressure so expansion only occurs after the die exit. The exact temperatures depend on your corn variety and are locked during the pre-shipment trial.
Q: How does die design affect the granule shape before flaking?
A: The die plate determines the cross-section and density of the extrudate strands that are then cut into granules. Round orifices produce uniform pellets that flatten predictably between the flaking rollers. Irregular die geometry leads to inconsistent flake thickness, which causes uneven roasting and variable bowl-life. Die selection is part of the configuration record we provide.
Q: Can the extrusion parameters be adjusted to produce both sugar-coated and natural flakes?
A: Yes. The base extrusion settings remain the same for both products since the difference is introduced downstream at the coating station. The double tumble sugar melting system, elevator, and spraying nozzle are engaged for coated flakes and bypassed for natural ones. The PLC stores separate recipes for each product, allowing changeover without mechanical adjustment to the extruder.