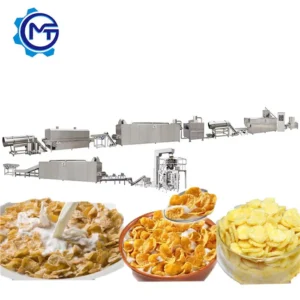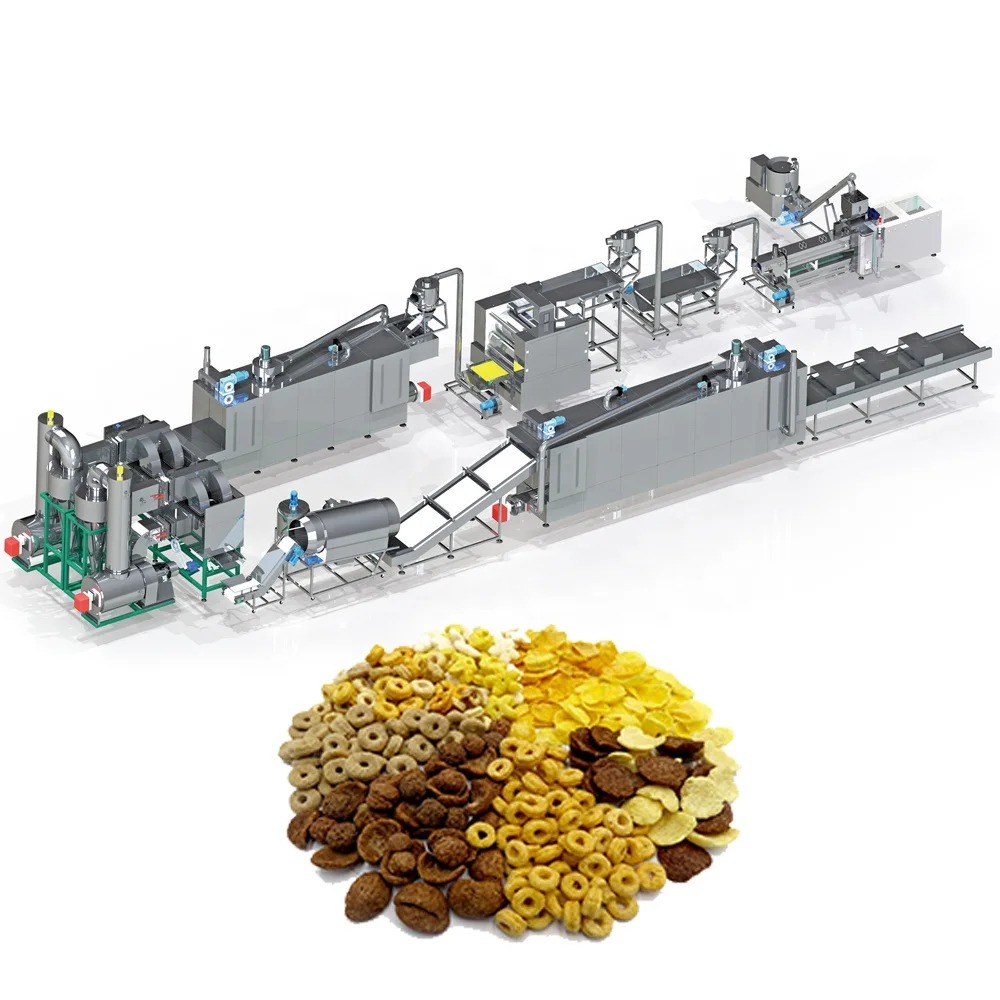
Screw Configuration Matched to Your Grain Blend — Every MT75 twin-screw extruder is specified with screw elements and die geometry tuned to the buyer’s actual corn, rice, or multi-grain formulation, not pulled from a generic catalog build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Twin Screw Extruder for Corn Flakes Breakfast Cereal Production Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/hr (basis not stated in source — confirm raw material, moisture content, and product format) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC and MCC |
| Flaking Station Control | PLC with hydraulic double-roller system, separate dual-motor drive, infrared sensor temperature control |
| Screw Feature | Special-process screw, wear-resistant, automatic lubricating and cooling function |
| Dryer Heating Source | Gas or Electric (options) |
| Roasting Oven | Vibrating pan with high-temperature spraying tubes, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Raw Materials | Powder of corn, rice, wheat, oat, barley |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour blends |
| Sugar-coated corn flakes | Corn base with sugar syrup coating |
| Multi-grain breakfast cereals | Rice, wheat, oat, and barley formulations |
| Shaped cereal snacks | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart via die adjustment |
| High-capacity cereal lines | Continuous extrusion with downstream flaking, drying, and roasting |
What "300 kg/hr" Actually Means When Your Corn Blend Changes
Capacity figures only hold when the screw profile, moisture content, and grain composition match what was tested.
I have watched a corn flakes line stall at barely half its quoted output because the buyer switched from degermed corn grits to a locally sourced whole-corn flour with higher fiber content. The generic screw configuration could not generate enough shear to gelatinise the starch at the new moisture level, and the flakes came out dense and under-expanded. That kind of mismatch does not show up until you run the actual raw material through the barrel [NEED_CITE: starch gelatinisation thresholds across corn varieties].
This is exactly where corn flakes extrusion production line technology separates a working installation from a disappointing one. The MT75 is configured with screw elements and die geometry chosen after reviewing the buyer’s specific grain blend, target flake density, and local moisture conditions. Without that step, a quoted capacity number is little more than a laboratory guess.
Barrel Temperature Profiling and Starch Gelatinisation
The extrusion of corn flakes demands precise thermal management across multiple barrel zones. Corn starch gelatinises within a narrow temperature window, and any deviation produces flakes that either shatter in the bowl or turn to mush within seconds of contact with milk. The MT75 barrel sections are individually heated and monitored through the PLC system, allowing operators to set distinct temperature profiles for each zone. This control ensures that the corn meal progresses from hydration through gelatinisation to the exact degree of cook required before it reaches the die plate.
Shear Control and Expansion Ratio
Twin-screw extrusion gives process engineers independent control over shear rate and residence time, two variables that directly determine how much the extrudate expands when it exits the die. For corn flakes, the target is a half-product pellet that will later be flaked and toasted — not a fully puffed snack. The screw configuration on the MT75 is designed to deliver moderate shear with controlled moisture injection, producing a dense, glassy pellet that flakes cleanly under the hydraulic double-roller system. Adjusting the screw element sequence allows the same extruder to handle oat-based or multi-grain formulations that require different shear profiles [NEED_CITE: twin-screw shear rate effects on cereal pellet density].
Reading the Specification Sheet Beyond the Headline Numbers
The installed power of 210 kW and operating consumption of 150 kW on the MT75 reflect the energy required to maintain barrel temperature, drive the twin screws through viscous cereal dough, and run the feeding and cutting systems simultaneously. The 45-meter line length encompasses every station from mixing through packing, which means throughput must be balanced at each stage — the flaking station at 200–300 kg/hr (basis not stated in source) must be matched to the extruder output to prevent bottlenecking. The PLC and MCC control architecture allows centralized monitoring so that a speed adjustment at the extruder propagates to downstream conveyor rates, dryer retention time, and roasting oven throughput. The infrared sensor temperature control on the flaking rollers maintains consistent roll surface heat, which is critical for achieving uniform flake thickness without edge cracking.
The Hidden Cost of a Copied Screw Profile
When a supplier builds a corn flakes extruder using a screw configuration copied from a different product application, the consequences surface slowly and expensively. The flakes may look acceptable during the first hour of production, but as the barrel wears and the screw elements lose their edge, expansion consistency degrades. Operators compensate by raising barrel temperatures, which accelerates wear further and increases energy draw. Within a few production cycles, the line is consuming more power, producing more off-spec material, and requiring screw replacements well ahead of the expected service interval. I once traced a customer’s recurring flake density complaints back to a screw set that had been specified for a puffed snack, not a flaking pellet — the shear was too aggressive and the pellets were partially pre-expanded before they even reached the rollers [NEED_CITE: screw wear progression in high-starch extrusion].
Why Buyers Choose This Source for Extrusion Technology
The MT75 line is engineered as a complete system from batching to packing under a single supplier, which means the extruder output, flaking throughput, dryer capacity, and roasting oven volume are calculated together rather than assembled from mismatched vendors. Every screw configuration and die design is documented against the buyer’s raw material specification before production begins. An in-house testing workshop runs trial extrusions on the customer’s actual grain blend before the line ships, so the gelatinisation profile and flake density are verified in advance rather than discovered during commissioning. The PLC and MCC control platform is configured to the buyer’s local voltage and frequency, with the control language set before crating. Wear parts including screw elements and die plates are listed and stocked based on the specific configuration, so the first replacement order does not become an emergency.
Documentation & Verification
- Line layout and capacity calculation showing throughput balance across every station from mixer to packer
- Screw and die configuration record matched to your specific corn, rice, or multi-grain formulation
- Trial run report on your actual raw material conducted in the testing workshop before dispatch
- Electrical schematic with voltage and frequency confirmed for your local supply standard
- Machine specification sheet covering all station dimensions, power requirements, and utility connections
- Operation and maintenance manual with wear parts list specific to your screw configuration
Installation, Commissioning & Support
- Foundation planning for the 45-meter line footprint with utility routing for 210 kW total installed power
- Dedicated electrical circuit sized for 150 kW operating draw with voltage matched to local supply
- Assembly sequence from extruder barrel sections through flaking station to roasting oven and packing
- First-run parameter setting including barrel temperature zones, screw speed, and flaking roller pressure
- Operator training on PLC interface for real-time adjustment of expansion and density targets
- Wear parts inventory including screw elements and die plates specific to your configured build
Preparing Your Inquiry
To move from a general inquiry to a line configuration that actually runs your product, we need your grain formulation details including the specific corn variety or multi-grain blend, target moisture content at the extruder inlet, and the flake thickness and bowl-life specifications your market expects. Share your factory floor dimensions so the layout can be drafted around existing structures, and confirm your local voltage and frequency so the MCC and PLC panels are built correctly from the start.
Frequently Asked Questions
Q: How is the screw configuration matched to my specific grain blend and moisture content?
A: We review your raw material data sheet including particle size, starch content, and fiber level, then select screw element types and sequencing to achieve the gelatinisation degree your flake format requires. The die geometry is designed in parallel to produce pellets at the target density. A trial run on your actual material confirms the configuration before the extruder ships.
Q: How do you verify capacity on my raw material before the line leaves the factory?
A: Your grain blend is run through the extruder in our testing workshop under the same barrel temperature profile and screw speed planned for your installation. We measure pellet density, moisture loss, and expansion behavior at the die. The trial run report documents all parameters so commissioning starts from a proven baseline rather than guesswork.
Q: How does barrel temperature profile affect final flake crunch and bowl-life?
A: Each barrel zone is independently controlled through the PLC, allowing a graduated temperature ramp that takes corn starch from hydration through full gelatinisation without overcooking. Under-gelatinised starch produces hard, brittle flakes; over-gelatinised starch yields flakes that absorb milk too quickly. The profile is tuned during the trial run and locked into the PLC recipe.
Q: How are extruder output and downstream station capacities matched to avoid bottlenecks?
A: The flaking station, dryer, and roasting oven are each sized against the extruder’s verified throughput on your material. The PLC coordinates conveyor speeds across stations so that a rate change at the extruder propagates automatically, preventing material pile-up or starvation at any downstream point.