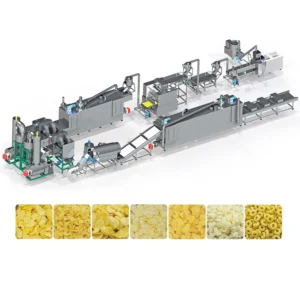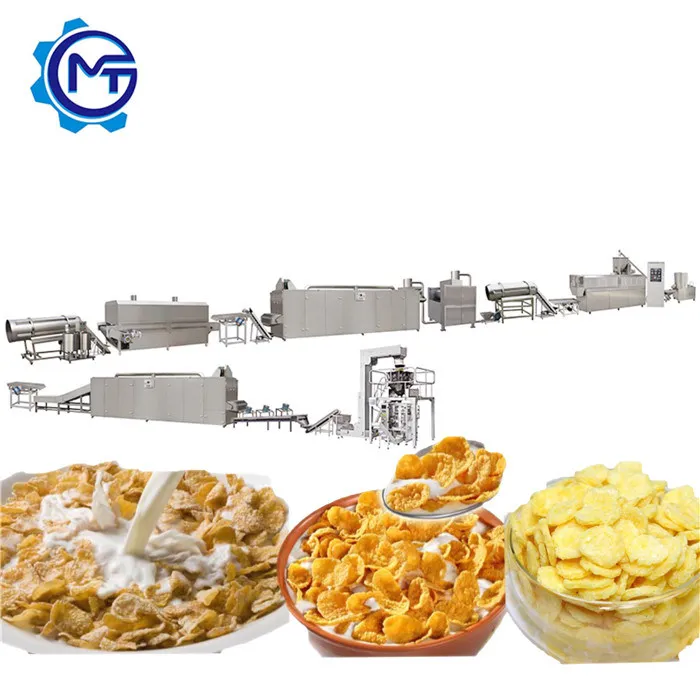
Extrusion Physics First — We match screw configuration and barrel zone profiles to your specific grain formulation before quoting a line, so the flake density and expansion behaviour hold stable through downstream roasting.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Processing Line |
| Extruder Models Available | MT70, MT85, MT75 |
| Extruder Type | Twin Screw |
| MT70 Installed Power | 160 kW |
| MT70 Power Consumption | 120 kW |
| MT70 Capacity | 150–200 kg/hr (basis to be confirmed: raw material, moisture, flake thickness) |
| MT85 Installed Power | 190 kW |
| MT85 Power Consumption | 140 kW |
| MT85 Capacity | 300–400 kg/hr (basis to be confirmed: raw material, moisture, flake thickness) |
| MT75 Installed Power | 210 kW |
| MT75 Power Consumption | 150 kW |
| MT75 Capacity | 300–500 kg/hr (basis to be confirmed: raw material, moisture, flake thickness) |
| MT-75 Extruder Capacity | 200–300 kg/hr (basis to be confirmed: raw material and product format) |
| Flaking Machine Capacity | 200–300 kg/hr (basis to be confirmed: raw material and flake thickness) |
| Flaking Machine Control | PLC control system; hydraulic system for double rollers; double motors for separate roller driving |
| Dryer Heating Source | Gas or Electric (configurable) |
| Hot Air Roasting Oven | Vibrating pan with high-temperature spraying tubes; conciliation burner combustion chamber; two separate circulating fans; cyclone dust removal device |
| Coating System | Double tumble for sugar melting; elevator; coating drum; spraying nozzle |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Control System | PLC (on flaking unit); automatic lubricating and cooling (on extruder) |
| Line Layout | Customized to buyer factory dimensions |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits, maize flour |
| Sugar-coated breakfast cereal | Corn, rice, wheat blends with sugar syrup coating |
| Multi-grain extruded flakes | Oat, barley, and mixed grain powder formulations |
| Shaped cereal formats (via die change) | Ball, tube, ring, fruit loop, star, wheel, flower, heart shapes |
| Fortified breakfast cereal | Grain powder blended with vitamin and mineral premix |
What "Nominal Line Capacity" Hides from Process Engineers
A rated throughput number means nothing if the extruder cannot hold that output on your actual grain formulation at the moisture and flake thickness your market demands.
I have watched a corn flakes line in Nairobi run trials on fine maize flour during factory acceptance, only for the buyer’s coarser corn grits to under-gelatinise on the installed screw profile. The flakes sank in milk instantly. The entire first production batch was scrapped. This happens when line capacity is quoted on a generic basis and the screw configuration is never matched to the real raw material. The corn flakes extrusion production line technology you specify must account for your exact grit particle size, starch content, and target bowl-life before the die design is finalized [NEED_CITE: starch gelatinisation thresholds by grain type and moisture content].
Barrel Temperature Zones and Starch Gelatinisation Control
Twin-screw extrusion forces the cereal dough through distinct thermal and mechanical stages. Each barrel zone applies a specific temperature and shear profile, and the corn flakes extrusion production line technology depends on getting these zones right for your grain. Under-cooked starch produces a dense, glassy pellet that the flaker cannot compress evenly. Over-cooked starch turns gummy and sticks to the flaking rollers. The MT series extruder features automatic lubricating and cooling to maintain thermal stability across extended runs, but the screw element sequence and barrel heating profile must be configured around your raw material before the line leaves the workshop.
Die Geometry and Pellet Expansion Behaviour
The die opening determines the extrudate cross-section and how much the pellet expands as it exits the barrel. For traditional flat corn flakes, a simple round die produces a cylindrical pellet that the hydraulic double-roller flaking machine compresses into a uniform flake. If you plan to run shaped cereal formats — fruit loops, stars, rings — the die must be swapped, and the screw profile often needs adjustment to manage expansion ratio differently. This is where the corn flakes extrusion production line technology either delivers versatility or locks you into a single product. The PLC-controlled flaking station monitors roller temperature with an infrared sensor, helping maintain consistent thickness regardless of pellet geometry [NEED_CITE: die design principles for twin-screw cereal extrusion].
Moisture, Shear, and the Flaker Interface
The moisture content fed into the extruder barrel directly controls how much mechanical energy converts to thermal expansion versus mechanical deformation. Too dry, and the pellet shatters under the flaking rollers. Too wet, and it flattens into an uneven sheet that roasts inconsistently. The hydraulic system on the flaking machine applies adjustable pressure to the double rollers, and the separate motor drives allow independent speed control. This gives the process engineer fine adjustment over flake thickness, but only if the upstream extruder has already delivered a pellet with the correct moisture and gelatinisation balance.
Reading the Specs That Actually Matter
The installed power figures across the MT70, MT85, and MT75 models reflect different screw diameter and barrel length combinations. A higher installed power rating supports longer barrel assemblies, which provide more residence time for starch gelatinisation — critical when running harder grains like barley or coarser corn grits. The overall line dimensions scale accordingly: the MT70 line stretches to approximately 41 metres end-to-end, while the MT75 extends to around 45 metres. That extra length accommodates additional barrel zones, a larger flaking station, and a longer hot air roasting oven with dual circulating fans and cyclone dust removal. For natural corn flakes, the line sequence runs mixing, extruding, flaking, drying, hot air roasting, cooling, and packing. Sugar-coated variants insert sugar spraying and coating drums between the roasting and final drying stages. The choice between gas and electric dryer heating depends on your facility’s utility infrastructure and local energy cost structure.
When Generic Screw Profiles Destroy Your First Production Run
I once visited a plant where the extruder supplier had copied a screw configuration from a standard build without asking about the buyer’s corn source. The local maize had lower starch content than the reference material. The result was incomplete gelatinisation throughout the barrel, and the flaker produced brittle, uneven flakes that broke during conveying. The roasting oven could not compensate because the pellet density was already wrong coming out of the die. Every hour of production generated waste. The buyer had to halt the line, ship the screw elements back, and wait for a redesigned configuration — weeks of lost capacity [NEED_CITE: common extruder screw configuration failure modes in cereal processing].
Why Procurement Teams Choose This Configuration
The complete line runs from batching through mixing, extruding, flaking, roasting, and packing under a single supplier, so throughput at every station is matched rather than patched together from separate vendors. Screw configuration and die design are specified to your raw material and target flake density before the quotation stage. The in-house testing workshop runs trials on your actual grain before the line ships, so product development begins before installation, not after. Twin-screw expertise covers corn, rice, wheat, oat, and barley formulations across the cereal category. Pre-sales engineering consultation covers line layout, utility planning, and barrel zone profiling [NEED_CITE: turnkey cereal line procurement best practices].
Documentation & Verification
- Line layout and capacity calculation showing throughput matching across every station
- Screw and die configuration record specifying elements matched to your grain formulation
- Electrical schematic with voltage, frequency, and control language confirmed for your site
- Trial run report on your raw material processed in the testing workshop before dispatch
- Operation and maintenance manual covering extruder lubrication and flaker hydraulic servicing
- Wear parts list identifying screw elements, die plates, and flaking roller replacement intervals
Installation, Commissioning & Support
- Foundation must support the full line length, up to approximately 45 metres for the MT75 configuration
- Power supply must match the confirmed voltage and frequency, with dedicated circuits for the 150–210 kW extruder motors
- Extruder automatic lubricating and cooling system calibrated during commissioning for continuous run stability
- PLC on the flaking unit configured to your operator’s language before on-site training begins
- Infrared sensor on the flaking station calibrated to your target flake thickness during first production run
- Hot air roasting oven burner and circulating fans adjusted to achieve correct surface blistering on your flake format
Before You Request a Quotation
Send your raw material specification including grain type, particle size distribution, and starch content. Confirm your target flake density and whether the line needs to handle both natural and sugar-coated formats. Provide your facility voltage, frequency, and available floor space so the line layout and electrical schematic can be prepared accurately.
Frequently Asked Questions
Q: How is screw configuration selected for a specific grain formulation and target flake density?
A: We review your raw material data — grain type, particle size, starch and moisture content — and map a screw element sequence and barrel temperature profile to achieve the gelatinisation level your target flake density requires. The configuration is tested on your material in the workshop before the line is finalized.
Q: What moisture and shear conditions produce consistent expansion through the flaker?
A: Moisture must be controlled at the extruder inlet so the pellet reaches a specific gelatinisation window by the time it exits the die. The twin-screw barrel zones apply graduated shear and heat to manage this. The PLC-controlled flaker then compresses the pellet uniformly under hydraulic pressure.
Q: How does die design affect whether the line produces flat flakes versus shaped cereal?
A: A round die produces cylindrical pellets that the flaking rollers compress into flat flakes. Shaped formats like rings or stars require a profiled die and often a modified screw configuration to manage expansion differently. The same extruder platform can run both with appropriate die and screw changes.
Q: Can I run a trial on my raw material before the line ships?
A: Yes. The in-house testing workshop processes your actual grain formulation through the extruder and flaking station. You receive a trial run report documenting screw configuration, barrel temperatures, flake thickness, and roasting results before the line is cleared for shipment.
Q: How is roasting temperature calibrated to produce blistering without over-drying the flake core?
A: The hot air roasting oven uses a conciliation burner with dual circulating fans to control surface heat and airflow independently. Dwell time and temperature are adjusted during commissioning on your specific flake thickness to achieve surface blistering while retaining enough core moisture for crispness.