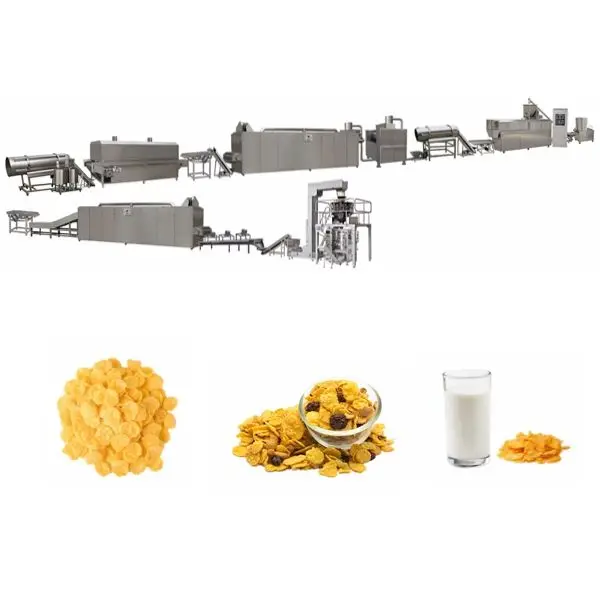
Screw Configuration Matched to Your Grain Formulation — Every barrel zone, screw pitch, and die orifice in these twin-screw extruders is selected against your specific corn, oat, or multi-grain blend, ensuring the gelatinisation window opens and closes exactly where your recipe demands it.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flake Production Line with Twin-Screw Extruder |
| Extruder Type | Twin-screw with integrated feeding, extruding, cutting, heating, gearing, and control systems |
| Installed Power (MT70 / MT85 / MT75) | 160 kW / 190 kW / 210 kW |
| Power Consumption (MT70 / MT85 / MT75) | 120 kW / 140 kW / 150 kW |
| Capacity (MT70) | 150–200 kg/h (basis not stated in source — confirm raw material moisture and formulation) |
| Capacity (MT85) | 300–400 kg/h (basis not stated in source — confirm raw material moisture and formulation) |
| Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material moisture and formulation) |
| Flaking Machine Capacity | 200–300 kg/h (MT-75 reference table) |
| Flaking Machine Drive | Hydraulic double-roller, independent dual-motor, infrared sensor temperature control |
| Dryer Heating Source | Gas or electric (configurable) |
| Roasting Oven | Hot air with vibrating pan, high-temperature spraying tubes, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble drum for sugar melting, elevator, coating drum, spraying nozzle |
| Line Dimensions (MT70 / MT85 / MT75) | 41 × 1.5 × 2.2 m / 43 × 1.5 × 3.2 m / 45 × 1.5 × 3.5 m |
| Lubrication | Automatic lubricating and cooling function |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Corn grits, corn flour — extruded, flaked, roasted without sugar coating |
| Sugar-coated corn flake SKUs | Corn base with sugar syrup spraying, tumble coating, and secondary drying |
| Multi-grain breakfast flakes | Wheat, oat, barley, rice blends requiring adjusted screw profile and moisture conditioning |
| Shaped breakfast cereals | Ball, tube, ring, star, wheel, fruit loop, heart shapes via interchangeable die and mould plates |
| Fortified cereal lines | Grain bases blended with vitamin and mineral premixes for nutritional programmes |
What "300 kg/h" Leaves Out About Corn Flake Extrusion Lines
Nominal capacity is meaningless unless it was measured on the same grain blend you will run in your factory.
I have seen corn flake lines ship with a trial-run report based on standard corn grits, then arrive at a plant running a whole-wheat and oat mixture where the starch gelatinisation degree drops and the flakes come out dense and brittle. The extruder motor is working at the same amperage, the barrel heaters are reading the same temperatures, but the product is wrong — because the screw element combination and moisture profile were never matched to that specific formulation [NEED_CITE: starch gelatinisation behaviour across different grain bases in twin-screw extrusion]. When you review a corn flake production line extruder specification sheet, the capacity row must state which raw material, particle size, and moisture percentage were used to generate the number. Without that, you are buying a guess.
Barrel Temperature Zones and the Gelatinisation Window
Corn starch gelatinises within a narrow temperature band, and the barrel is divided into independently controlled heating zones so that the material passes through that band at precisely the right moment. If zone three is too hot relative to zone four, the starch over-gelatinises before the die, the dough loses elasticity, and the flakes tear during rolling. The corn flakes extrusion technology in these lines uses segmented barrel heating with PLC coordination so that each zone tracks its setpoint against the actual material temperature, not just the heater output.
Die Geometry, Moisture Shear, and Flake Thickness
The die orifice shape and land length determine the extrudate cross-section before it hits the flaking rollers. A longer land increases back-pressure and shear, which tightens the expansion ratio and produces a denser pellet — suitable when the target is a thin, crisp flake with extended bowl-life. Moisture content at the die face is equally critical: even a small shift in conditioning water alters how the sheet behaves between the hydraulic double-rollers of the flaking machine. This is why the flaking station here uses infrared sensor temperature control to monitor the sheet surface in real time, adjusting roller gap and speed to maintain uniform thickness.
Reading the Power and Dimension Data Across Models
The MT70 draws 120 kW in operation across a 41-metre line footprint, positioning it for smaller-volume or pilot-scale cereal runs. The MT85 and MT75 step up to 140 kW and 150 kW respectively, with longer line layouts accommodating higher-capacity flaking, larger roasting ovens, and extended drying tunnels needed to handle increased throughput. Installed power exceeds consumption because start-up surges and the simultaneous operation of the roasting oven’s conciliation burner, dual circulating fans, and the coating system’s sugar-melting drum all pull peak load at different moments. When planning your electrical infrastructure, confirm the voltage and frequency specification early [NEED_CITE: voltage and frequency standards by export market] — a 400 V / 50 Hz motor rewound for a 380 V / 60 Hz market will overheat within weeks.
The Cost of Skipping the Pre-Shipment Trial Run
Lines that ship without a trial run on the buyer’s actual raw material force product development into the commissioning window. I have watched crews spend days adjusting screw element sequences, barrel temperatures, and feed rates on-site — burning raw material, missing launch deadlines, and blaming the machine when the real issue was that no one tested the whole-grain blend before the crate was nailed shut [NEED_CITE: common causes of commissioning delays in food extrusion projects]. A pre-shipment trial run locks in the screw configuration record, the die selection, and the moisture parameters so that the line produces saleable flakes from the first hour of production at your facility.
Why Procure This Line From a Single Extrusion Supplier
The extruder, flaking machine, dryer, roasting oven, and coating system are engineered as one throughput-matched sequence — the dryer capacity is calculated against the extruder output, and the roasting oven’s vibrating pan speed is timed to the flaking machine’s feed rate. Screw configuration and die design are specified against your raw material formulation rather than copied from a generic build. The in-house testing workshop runs your corn, oat, or multi-grain blend before dispatch, producing a trial-run report that documents actual product density, expansion ratio, and flake integrity. Pre-sales engineering covers line layout and utility planning, and the same technical team handles on-site installation, commissioning, and operator training. Wear parts — screws, dies, roller shells — are catalogued and available from the same source, so the first replacement does not become a sourcing project.
Documentation & Verification
- Screw and die configuration record matched to your specific grain formulation
- Trial-run report on your raw material documenting flake density and expansion
- Electrical schematic confirming voltage, frequency, and control language
- Line layout and capacity calculation showing throughput matching across every station
- CE declaration of conformity and ISO certificate
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation plan accounts for the full line length up to 45 metres and the roasting oven’s vibrating load
- Dedicated electrical circuit sized to the model’s installed power, up to 210 kW for the MT75
- Flaking machine hydraulic system and dual-motor drive calibrated on-site to your target flake thickness
- PLC control language and HMI interface confirmed before shipment to match your operator team
- Hot air roasting oven burner tuned to local gas pressure or electrical supply specification
- Automatic lubrication system checked and first wear-part replacement schedule documented during commissioning
What to Include in Your Enquiry
Provide your target raw material formulation — corn, wheat, oat, or a specific blend ratio — along with particle size and expected moisture content at the mixer. State whether you need natural flakes, sugar-coated SKUs, or both, and share your daily production target so the correct extruder model and downstream station sizing can be proposed. Include your factory’s available floor length, ceiling height, and local voltage and frequency so that the line layout and motor specifications are confirmed before production begins.
Frequently Asked Questions
Q: How is screw configuration adapted when switching from corn to a multi-grain blend?
A: Each grain has a different starch gelatinisation temperature and fibre content. Oat and barley, for example, require a gentler shear profile and adjusted barrel zone temperatures to prevent over-gelatinisation. The screw element sequence — conveying, kneading, and reverse elements — is rearranged to match the blend, and a trial run validates the configuration before the line ships.
Q: What role do barrel temperature zones play in controlling flake crispness?
A: Independent heating zones allow precise control of the starch gelatinisation window as material moves through the barrel. Too much heat too early causes premature expansion; too little leaves ungelatinised starch that produces a hard, glassy flake. The PLC monitors each zone against the actual material temperature to maintain the correct profile throughout the run.
Q: How is line capacity verified against my actual formulation before delivery?
A: Your raw material is run through the extruder in the in-house testing workshop. The trial-run report records extrudate density, expansion ratio, flake thickness after rolling, and final crispness after roasting — so you know the line produces your target product before it leaves the factory floor.
Q: How does the roasting oven temperature profile affect bowl-life?
A: The hot air roasting oven uses a conciliation burner and dual circulating fans to control surface blistering and moisture removal. A higher roast temperature drives more moisture from the flake interior, extending bowl-life by slowing milk absorption — but excessive heat scorches the surface and damages flavour. The profile is tuned during commissioning to your target crunch duration.