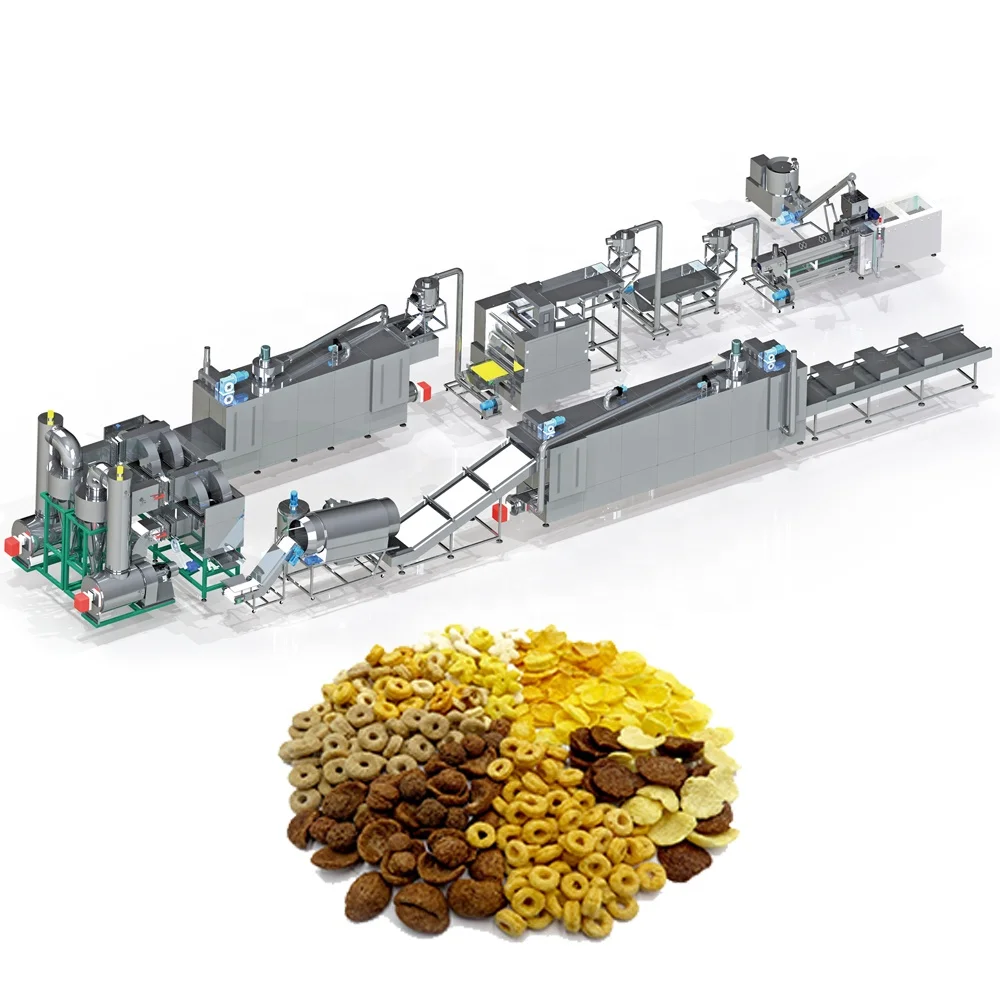
Screw Configuration Matched to Your Grain Formula — Every barrel zone and die cut is dialed in after we test your actual corn or multi-grain blend, not a generic build copied from a stock template.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Breakfast Cereal Corn Flakes Processing Line |
| Extruder Model | MT-65 |
| Screw Type | Co-rotating twin-screw, sectional modules |
| Mixer Output | 10–30 kg/load |
| Mixer Power | 4 kW |
| Mixer Tank Size | φ600 × 500 mm |
| Mixer Dimension | 1000 × 800 × 1200 mm |
| Corn Flakes Press Roller Size | 510 × 310 × 1050 mm |
| Corn Flakes Press Power | 16.12 kW |
| Corn Flakes Press Dimension | 1550 × 1300 × 2000 mm |
| Corn Flakes Press Features | Large roller, integrated cooling system, adjustable roller gap |
| Screw Conveyor Power | 0.75 kW |
| Screw Conveyor Dimension | 2700 × 500 × 2400 mm |
| Screw Conveyor Feature | Sealed stainless steel roller, vibrating sifter for stable feeding |
| High-Temperature Oven Dimension | 4500 × 1400 × 1800 mm |
| High-Temperature Oven Power | 3.75 kW |
| Oven Heating Method | Gas-fired, dual-side baking |
| Sugar Spraying System Power | 28.75 kW |
| Sugar Spraying System Dimension | 4000 × 1900 × 1880 mm |
| Sugar Spraying Roller Size | approx. φ600 × 2700 mm |
| Contact Material | Food-grade stainless steel |
| Output Capacity | Basis to be confirmed with buyer’s raw material and target throughput |
| Control System | PLC or MCC, configuration to be confirmed per buyer preference |
| Voltage and Frequency | Customizable (e.g., 3ph 380V 50Hz, 3ph 415V 60Hz, 3ph 220V 60Hz) |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn flakes production | Corn grits, corn flour, degerminated corn |
| Multi-grain flakes | Rice, oat, barley blended grain powders |
| Fortified breakfast cereals | Grain base with added vitamin and mineral premix |
| Shaped cereal pieces | Rings, balls, stars, sticks via interchangeable die moulds |
| Coated ready-to-eat snacks | Sugar syrup or honey glazed puffed cereal |
Why "Rated Capacity" on Corn Flakes Lines Often Misleads Buyers
The throughput number on the quote only holds when screw configuration, barrel heating, and die geometry match the buyer’s exact grain formulation and moisture content.
I once watched an entire batch of corn flakes shatter into dust on the dryer belt because the extruder was set up for standard corn flour while the customer ran a high-fat whole-grain blend. The starch gelatinisation was incomplete, the pellet structure was weak, and the flakes could not survive the flaking press. Two weeks of downtime followed while replacement screws were machined and shipped [NEED_CITE: starch gelatinisation thresholds for high-lipid grain formulations]. With corn flakes extrusion technology breakfast cereal processing, the extrusion parameters must be locked to your specific recipe before capacity claims mean anything. A line running standard corn grits at a given moisture level behaves very differently from one running oat-heavy or fibre-enriched blends, and screw module arrangement directly controls residence time, shear intensity, and final pellet density.
Barrel Zone Profiling and Starch Gelatinisation Control
The MT-65 co-rotating twin-screw extruder uses sectional screw modules that can be rearranged to alter convey, knead, and shear zones along the barrel. For corn flakes, achieving full starch gelatinisation without over-expansion requires a precise barrel temperature gradient — typically starting lower in the feed zone and ramping through the cooking and metering zones. This corn flakes extrusion technology breakfast cereal processing approach ensures the pellet exits the die with the internal structure needed to survive pressing and baking without cracking.
Die Geometry and Pellet Structure for Flaking
The die plate determines the cross-section and initial expansion ratio of the extrudate before it enters the flaking press. A die orifice that is too large produces pellets with a low-density core that collapses under roller pressure; one that is too small creates excessive back-pressure and inconsistent throughput. Die selection is paired with screw configuration to produce pellets of uniform moisture and density, which is the prerequisite for consistent flake thickness downstream [NEED_CITE: die land length effects on extrudate expansion in twin-screw systems].
Reading the Specs That Actually Shape Your Flakes
The MT-65 co-rotating twin-screw design allows sectional module reconfiguration, which is significant because corn flakes require a longer cooking zone and moderate shear compared to fully puffed snacks. The large 510 × 310 mm flaking press rollers with adjustable gap give operators direct control over final flake thickness — a parameter that market buyers judge immediately when they open the box. Gas-fired dual-side baking in the 4.5 m oven ensures heat penetrates both faces of each flake simultaneously, preventing the case-hardening effect where the outside crisps but the centre remains leathery. The sealed screw conveyor with vibrating sifter feeding the extruder keeps material flow consistent, which matters because intermittent feeding causes pressure fluctuation in the barrel and uneven gelatinisation. Finally, the food-grade stainless steel contact surfaces across every station prevent contamination and meet hygiene standards expected in breakfast cereal production [NEED_CITE: food contact material regulations for cereal processing equipment].
What Happens When Extrusion Parameters Are Not Matched to Your Formula
When screw configuration is copied from a generic setup instead of tuned to the buyer’s grain blend, the consequences show up fast. Under-gelatinised pellets fracture at the flaking press, producing broken flakes that fall below the visual and textural standards retail buyers expect. Over-expanded pellets from incorrect die selection absorb too much coating syrup, driving up raw material cost and altering the nutritional profile per serving. Inconsistent barrel temperatures cause batch-to-batch variation that forces operators to re-adjust settings every run, increasing waste and slowing effective output [NEED_CITE: common causes of batch inconsistency in twin-screw cereal extrusion]. These problems are not visible in the quote — they surface only after installation, when the line is expected to produce saleable product immediately.
Why This Extrusion Setup Stands Apart
Complete thermal profiling from extrusion through drying and baking is designed as one integrated system, not assembled from mismatched standalone units. Screw configuration and die design are specified against the buyer’s actual raw material and target flake geometry, not copied from a catalogue build. The in-house testing workshop runs trial production on the customer’s grain blend before shipment, so gelatinisation degree and expansion ratio are confirmed before the line leaves the factory. Every supporting station — mixing, conveying, flaking, coating, cooling — is throughput-matched to prevent bottlenecks that occur when stations are sourced from separate vendors. Documentation includes a screw and die configuration record specific to your formulation, so re-ordering wear parts is straightforward. Pre-sales consultation carries through to on-site installation, commissioning, and operator training, ensuring the extrusion parameters validated during trial are replicated on your production floor.
Documentation & Verification
- Line layout with throughput calculation across every station from mixer to cooling conveyor
- Screw and die configuration record matched to your grain formulation and target flake shape
- Trial run report on your raw material documenting gelatinisation degree and pellet density
- Electrical schematic with voltage and frequency confirmed for your facility
- CE declaration of conformity covering the complete processing line
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation plan based on the 4.5 m oven and full line footprint for level concrete floor preparation
- Dedicated electrical circuit sized for the combined 28.75 kW coating system and 16.12 kW flaking press
- Line arrives in modular stations for sequential assembly from mixer through cooling conveyor
- First-run commissioning includes barrel temperature profiling and screw speed calibration on your grain blend
- Operator training covers roller gap adjustment on the flaking press and oven zone temperature setting
- Wear parts inventory with spare screw elements and die plates listed in the delivery documentation
What We Need From You to Size This Line Correctly
Share the specific grain formulation you plan to run — including the percentage of corn, oat, rice, or any added fibre or protein ingredients — along with your target flake thickness and daily production volume. We also need your facility’s voltage and frequency standard, the available floor space and ceiling height for the full line layout, and whether you require sugar or honey coating as a final stage. If you can send a sample of your raw material, we will run a trial in the testing workshop and include the results with the line proposal.
Frequently Asked Questions
Q: How is screw configuration selected for different grain raw materials and target flake textures?
A: We map the ratio of forward-conveying, kneading, and reverse elements to the starch content, lipid level, and fibre percentage of your specific grain blend. High-corn formulas need a longer cooking zone with moderate shear, while oat-heavy blends require adjusted kneading intensity to achieve full gelatinisation without over-densifying the pellet. The configuration is recorded and reproducible.
Q: How do you verify that the stated capacity holds on my actual raw material formulation?
A: Before shipment, we run your grain blend through the extruder in our testing workshop and document the output rate, pellet density, and gelatinisation percentage. This trial run report is included with the delivery. If throughput at your target specification differs from the initial estimate, the screw configuration is adjusted until the numbers align.
Q: What barrel temperature profile is used for corn flakes versus other breakfast cereal formats?
A: Corn flakes require a graduated profile that starts moderate in the feed zone to prevent premature gelatinisation, then ramps through the cooking and metering zones to build a dense, uniform pellet. Fully puffed cereals use higher peak temperatures for greater expansion. The profile for your product is established during the trial run and documented in the commissioning record.
Q: Can the flaking press produce different thicknesses, and how is roller distance calibrated?
A: The press features an adjustable roller gap mechanism that allows operators to set flake thickness within the range your market requires. Calibration is performed during commissioning using feeler gauges and confirmed by measuring sample flakes. The 510 × 310 mm roller width provides a consistent pressing surface across the full pellet bed.
Q: Is a trial run performed on my raw material before the line ships, and what does the report include?
A: Yes. Your grain blend is processed through the extruder and flaking press in our testing workshop. The report documents screw configuration, barrel temperature settings, pellet moisture content, gelatinisation degree, flake thickness measurement, and achieved output rate. This gives you confirmed production data before the equipment leaves the factory.