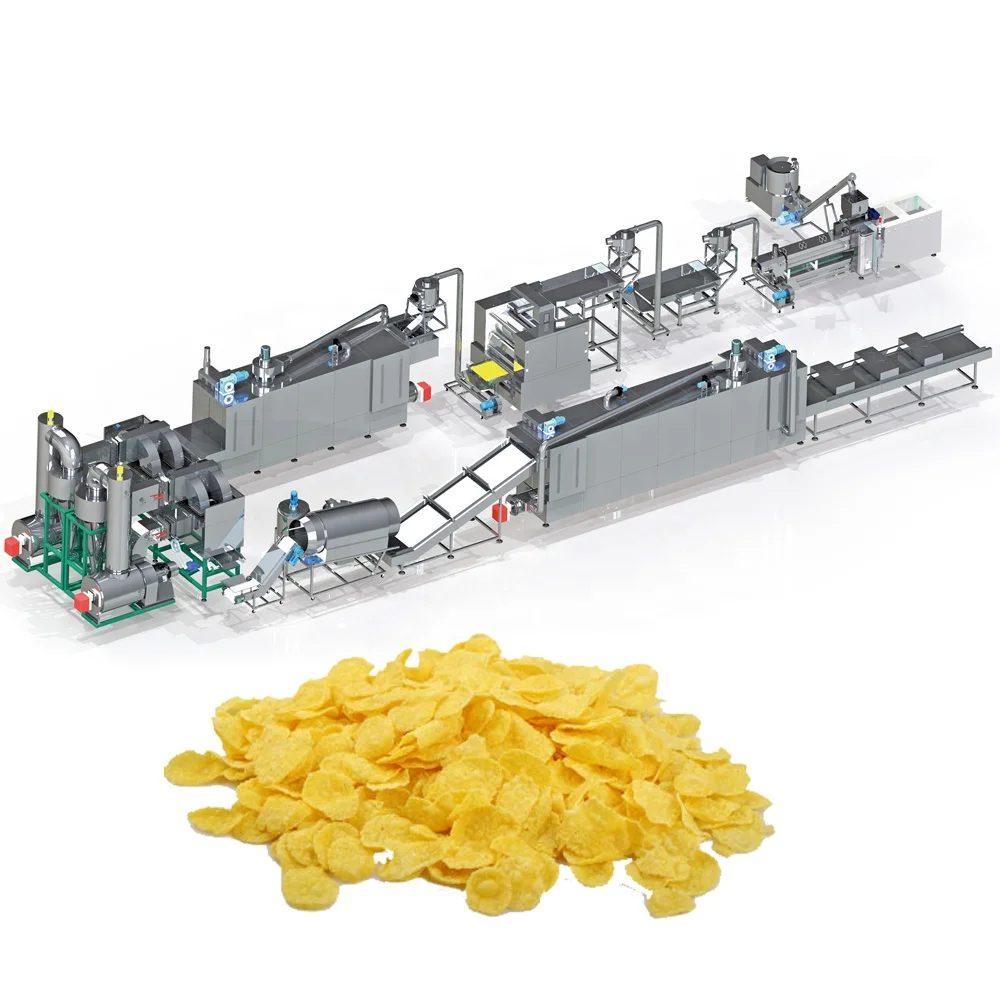
Screw Configuration Engineering — Every MT75 barrel zone and die profile is matched to your cereal substrate before the line ships, validated by an in-house trial run on your actual raw material.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Twin Screw Extrusion Corn Flakes Production Line |
| Screw Type | Twin-screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material, moisture content, and product format) |
| Voltage | 380V / 220V |
| Control System | PLC control system |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Material | Stainless Steel (food-contact parts) |
| Flaking Station | Hydraulic double-roller with infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal packaging | Corn flour, corn grits |
| Sugar-coated flakes with extended bowl-life | Corn base with sugar glaze coating |
| Multi-grain extruded cereal shapes | Rice, wheat, oat, barley powder blends |
| Extruded pellet formats | Ball, tube, ring, star, flower shapes via die exchange |
Why Generic Screw Builds Fail on Local Cereal Blends
A twin screw corn flakes extruder how to choose decision starts with one question: was the screw configuration designed for your exact raw material, or copied from a catalog default? The wrong element sequence produces flakes that either shatter in the bowl or never crisp at all.
I spent two weeks in a Bangkok plant where the local supplier was blending cassava starch into broken corn to cut costs. The standard screw build delivered gelatinisation that was uneven across the barrel — flakes came out dense on one side, over-expanded on the other, and dissolved the moment they hit milk. The entire screw element stack and die plate had to be torn out and rebuilt from scratch. This is not a rare edge case; it happens whenever a process engineer assumes corn is corn [NEED_CITE: starch gelatinisation behaviour across cereal substrates in twin-screw extrusion].
Barrel Temperature Profiling for Starch Gelatinisation
The MT75 uses independently controlled barrel zones managed through the PLC system. Each zone holds a set-point that the operator can adjust in real time, which matters because corn flour, oat, and barley all demand different heat curves to reach full starch gelatinisation without scorching. A corn flakes extrusion line specifications sheet that omits barrel zone count leaves the buyer guessing about process control granularity. Proper profiling means the cereal mass exits the die at the exact moisture and temperature where it can be flaked without tearing.
Die Geometry and Flake Density Control
Die aperture shape and land length determine the expansion ratio of the extrudate rope as it leaves the barrel. For natural corn flakes, the die must produce a consistent rope diameter so that the hydraulic double-roller flaking station can press it to uniform gauge. The infrared sensor on the flaking rollers feeds temperature data back to the PLC, compensating for ambient shifts across a production shift. When targeting sugar-coated formats, the die profile shifts to a denser extrudate that can survive the tumble coating drum without breaking apart.
Reading the Spec Sheet Like a Process Engineer
The 210 kW installed power on the MT75 reflects the torque demand of pushing a viscous cereal dough through a twin-screw barrel at continuous throughput. Power consumption sits at approximately 150 kW during steady-state operation, which is the number that matters for your utility planning. The 45-meter line footprint covers every station from mixing through packing, so floor space allocation must account for the full sequence, not just the extruder. The hydraulic flaking station uses separate motors for each roller, giving independent speed control that prevents shear marks on the flake surface. The roasting oven’s conciliation burner paired with dual circulating fans produces the surface blistering that defines a premium corn flake [NEED_CITE: hot air roasting parameters for breakfast cereal finishing].
The Hidden Cost of Skipping a Pre-Shipment Trial
When a line ships without a documented trial run on the buyer’s raw material, every process variable becomes an on-site experiment. Commissioning stretches from days into weeks. Screw elements get swapped, barrel temperatures drift through trial-and-error ranges, and the flaking station gets adjusted repeatedly until flake gauge finally stabilises. Meanwhile, raw material is wasted, packaging film sits unused, and the buyer’s launch timeline slips. This is the scenario that turns a capital equipment purchase into a liability [NEED_CITE: commissioning delays in food extrusion installations without pre-shipment testing].
Why This Line Is Built Around Extrusion Process Control
The screw and die configuration is specified against your raw material formulation before order confirmation, not selected from a generic menu. An in-house testing workshop runs your actual cereal blend and produces a trial run report covering expansion ratio, flake density, and texture before the machine ships. PLC control language and voltage are confirmed to your destination market, so the first power-on is not the first problem. Every station — extruder, flaker, dryer, roaster, coater — is throughput-matched so that no single unit bottlenecks the sequence. Food-grade stainless steel contact surfaces meet CE and ISO standards, documented in the conformity file that ships with the line.
Documentation & Verification
- Screw and die configuration record matched to your cereal formulation
- Trial run report on customer-supplied raw material validating flake density and texture
- Electrical schematic with voltage and frequency confirmed to destination market
- Line capacity calculation showing throughput balance across every station
- CE declaration of conformity and ISO certificate included in shipping file
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation must support the 45-meter line footprint with level tolerance for the flaking station
- Dedicated 380V circuit rated for 210 kW infeed with isolator at the main panel
- Extruder barrel sections and flaking rollers ship separated for site assembly
- PLC commissioning includes barrel zone tuning and flaker speed calibration on your material
- Operator training covers screw element inspection and die changeover procedure
- Wear parts list specifies replacement intervals for screws, dies, and roller surfaces
What to Include in Your Inquiry
Send your raw material specification including cereal type, blend ratios, and target moisture content. Confirm your local voltage, frequency, and preferred PLC control language. Share your workshop floor plan with ceiling height so the line layout can be drafted before quotation.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal substrates?
A: Each cereal — corn, rice, oat, barley — has a distinct starch gelatinisation temperature and shear sensitivity. The screw element sequence and L:D ratio are adjusted to match, then validated on your raw material in the testing workshop before the extruder ships.
Q: How is output capacity verified before shipment?
A: The stated throughput depends on raw material density, moisture content, and target flake format. A trial run on your supplied material produces a test report documenting actual output, expansion ratio, and flake gauge under controlled conditions.
Q: What barrel profile is needed for proper starch gelatinisation?
A: The PLC manages multiple independently heated barrel zones. Temperature set-points and moisture targets are tuned to your specific cereal blend during the trial run, then saved as a recipe in the control system for repeatable production.
Q: Is a trial run on our raw material possible before shipment?
A: Yes. The in-house testing workshop runs your cereal blend through the configured screw and die set. The resulting report covers expansion, density, flake texture, and throughput, giving you validated process data before the line leaves the factory.