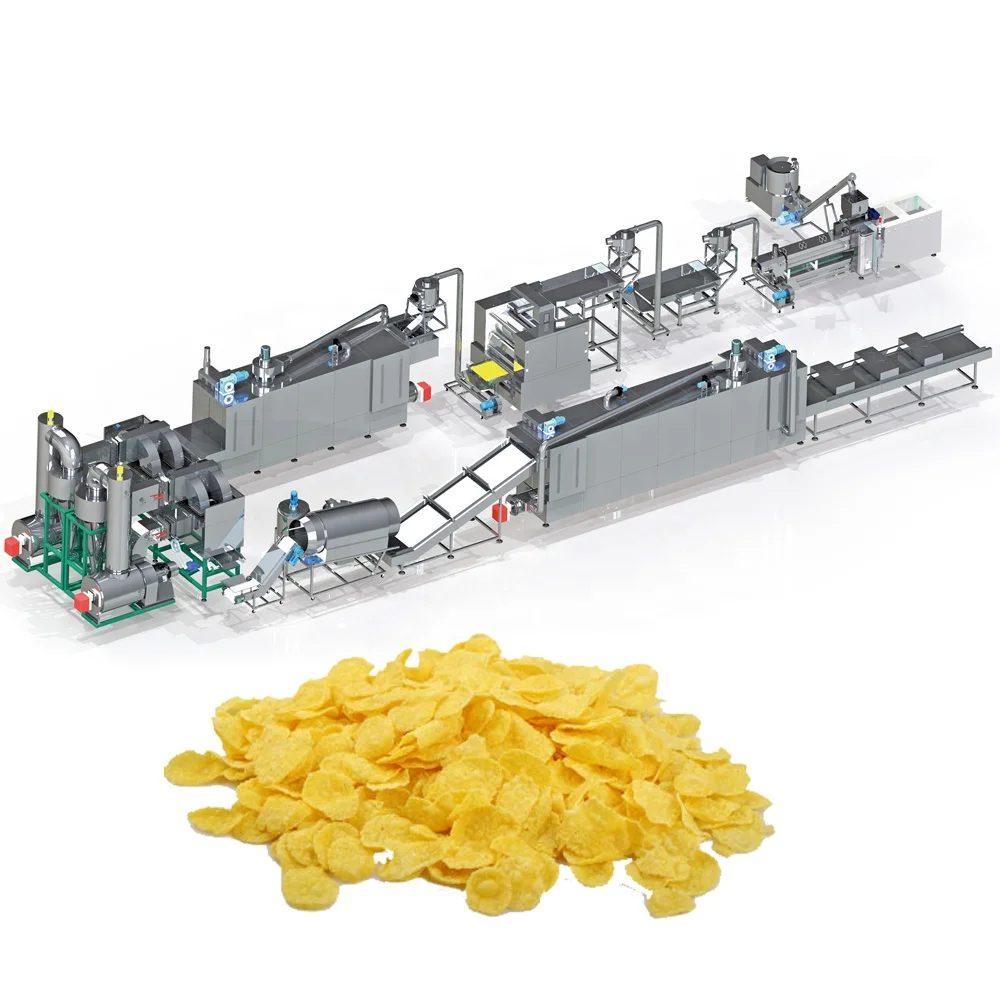
Screw Configuration Matched to Your Flour Blend — our twin-screw corn flakes extrusion line starts with your exact raw material profile, not a generic build copied from a catalog.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/hr (basis to be confirmed against raw material and moisture content) |
| Voltage | 380V / 220V (configurable) |
| Control System | PLC control system |
| Overall Dimensions (L×W×H) | 45 × 1.5 × 3.5 m |
| Material | Stainless Steel |
| Flaking System | Hydraulic double-roller with infrared temperature sensing |
| Dryer Heating Source | Gas or Electric |
| Hot Air Roasting Oven | Conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, coating drum, spraying nozzle |
| Assembly State | Complete integrated line |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn grits, corn flour |
| Sugar-coated corn flakes | Corn base with sugar syrup coating |
| Multi-grain breakfast cereals | Rice, wheat, oat, barley blends |
| Shaped cereal variants | Ball, tube, ring, star, wheel, heart, fruit loop profiles |
What a "500 kg/hr" Corn Flakes Line Quote Often Overlooks
A capacity figure without the raw material specification is not a capacity figure — it is a placeholder.
I have watched buyers sign contracts for a corn flakes extrusion production line turnkey based on a number that evaporated the moment their specific flour blend hit the barrel. The problem is almost always the same: the screw profile was configured for pure maize grits, while the buyer runs a multi-grain mix with different starch behaviour. The extruder struggles, the flake density drifts, and the roasting oven cannot correct what the barrel got wrong. We ran a test once where the flake looked perfect on standard maize — golden, crisp, clean snap. When the buyer’s defatted soy-and-corn blend went through the same configuration, the output was thick and barely expanded. The entire batch had to be scrapped before we re-profiled the screws. [NEED_CITE: starch gelatinisation behaviour across cereal flour blends]
Barrel Zones and Screw Profile Define Your Flake
The corn flakes extrusion production line turnkey begins with what happens inside the barrel. The MT75 uses a twin-screw configuration where each screw segment can be selected and positioned to match the starch content and particle size of your cereal flour. Barrel temperature zones are set independently, giving the operator control over how aggressively the material is cooked and sheared before it reaches the die.
Why Flaking Pressure Cannot Be an Afterthought
Once the extrudate leaves the die and is cut into pellets, the hydraulic double-roller flaking station determines final flake thickness. Infrared sensors monitor roller surface temperature continuously, which matters because inconsistent roller heat leads to uneven moisture distribution across the flake. That uneven moisture then shows up in the roasting oven as patches of blistering next to under-cooked areas. Matching flaking pressure to the pellet density produced upstream is where throughput balance either holds or breaks down. [NEED_CITE: hydraulic roller pressure settings and flake uniformity in cereal processing]
Reading the Specs That Actually Matter
The installed power of 210 kW and running consumption of 150 kW indicate a line built around sustained thermal and mechanical load — the extruder motor, the hydraulic flaking rollers, the dryer, and the hot air roasting oven all draw from this total. The PLC control system ties these stations together so that barrel zone temperatures, roller gap, and oven fan speed can be adjusted from a single interface rather than requiring manual coordination at each station. Stainless steel construction across food-contact surfaces meets the hygiene expectations for breakfast cereal production in regulated markets. The 45-metre line length reflects the sequential nature of the process: mixing, extruding, flaking, drying, roasting, optional sugar coating, then cooling and packing — each stage needs physical space and cannot be compressed without sacrificing retention time.
The Hidden Cost of Mismatched Station Capacity
When an extruder is sized correctly but the downstream dryer or roasting oven is not, the entire line slows to the pace of its weakest station. I have seen installations where the corn flakes extrusion production line turnkey could extrude far more than the oven could roast, forcing operators to idle the extruder for stretches of each shift. The result is not just lost output — it is inconsistent product, because material sitting in intermediate conveyors loses moisture unpredictably. Sizing every station to the same verified throughput, based on your actual material, is the only way to avoid this. [NEED_CITE: throughput balancing across cereal processing line stations]
Why Procurement Happens Here
Screw configuration and die design are specified to your cereal flour composition and target flake density, not pulled from a standard template. Every station from mixing through packing is supplied as one integrated line, so throughput is matched by design rather than assembled from separate vendors hoping their capacities align. Trial runs on your actual raw material take place in the in-house testing workshop before the line ships, which means screw profiles and barrel zones are validated — not guessed. The hot air roasting oven is built with a conciliation burner and dual circulating fans to deliver uniform surface blistering, matched to the flake thickness your flaking station produces. Pre-sales consultation covers factory layout, utility planning, and phased installation so the line fits your floor space and local power supply.
Documentation & Verification
- Line layout showing throughput calculation across every station
- Screw and die configuration record matched to your cereal blend
- Trial run report on your raw material before dispatch
- Electrical schematic with voltage and frequency confirmed
- Operation and maintenance manual with wear parts list
- Factory test record documenting all station performance
Installation, Commissioning & Support
- Foundation planning based on the 45 × 1.5 × 3.5 m line footprint
- Electrical supply verified against 380V / 220V requirements and PLC language
- Sequential station commissioning from extruder through roasting oven
- On-site training covering PLC operation and screw changeover procedures
- Spare screws, dies, and flaking roller components supplied with first shipment
- Scheduled maintenance intervals for hydraulic flaking system and burner assembly
What We Need to Build Your Line
To configure a corn flakes extrusion production line turnkey that holds its rated output on your actual material, we need your specific cereal flour composition, target flake dimensions and density, daily production volume, factory floor dimensions and ceiling height, and local voltage and frequency. If you plan to run both natural and sugar-coated variants, let us know the coating ratio so the coating drum and drying stages can be sized accordingly.
Frequently Asked Questions
Q: How is output capacity verified against my specific raw material?
A: We run your actual cereal flour blend through the extruder in our testing workshop, adjusting screw configuration and barrel zones until the flake density and expansion meet your specification. The trial run report documents the verified throughput at your material’s moisture level, so the capacity figure in your contract reflects real production conditions rather than a generic estimate.
Q: What screw profile is chosen for corn flour versus multi-grain blends?
A: Pure corn flour with high starch content uses a screw profile designed for controlled gelatinisation and moderate shear. Multi-grain blends with lower starch or added protein require reconfigured flighting and compression zones to maintain expansion and prevent dense, under-cooked output. Each configuration is recorded in your build documentation.
Q: How are voltage and PLC language confirmed before the line ships?
A: During specification confirmation, we verify your factory supply voltage and frequency against the motor and heating element ratings. The PLC interface language is set to your operator’s preference. The electrical schematic in your documentation package reflects these confirmed values before production begins.
Q: Can the line produce both natural and sugar-coated corn flakes?
A: Yes. The line includes a coating system with a double tumble sugar melting unit, coating drum, and spraying nozzle. Switching between natural and coated variants involves engaging or bypassing the coating station and adjusting the downstream drying stage — no major mechanical changeover is required.
Q: What spare wear parts are included with the first shipment?
A: The initial spare parts package covers the wear items most likely to need replacement during early production: extruder screw segments, die plates, and flaking roller components. A full wear parts list with part numbers is included in your documentation so reordering is straightforward.