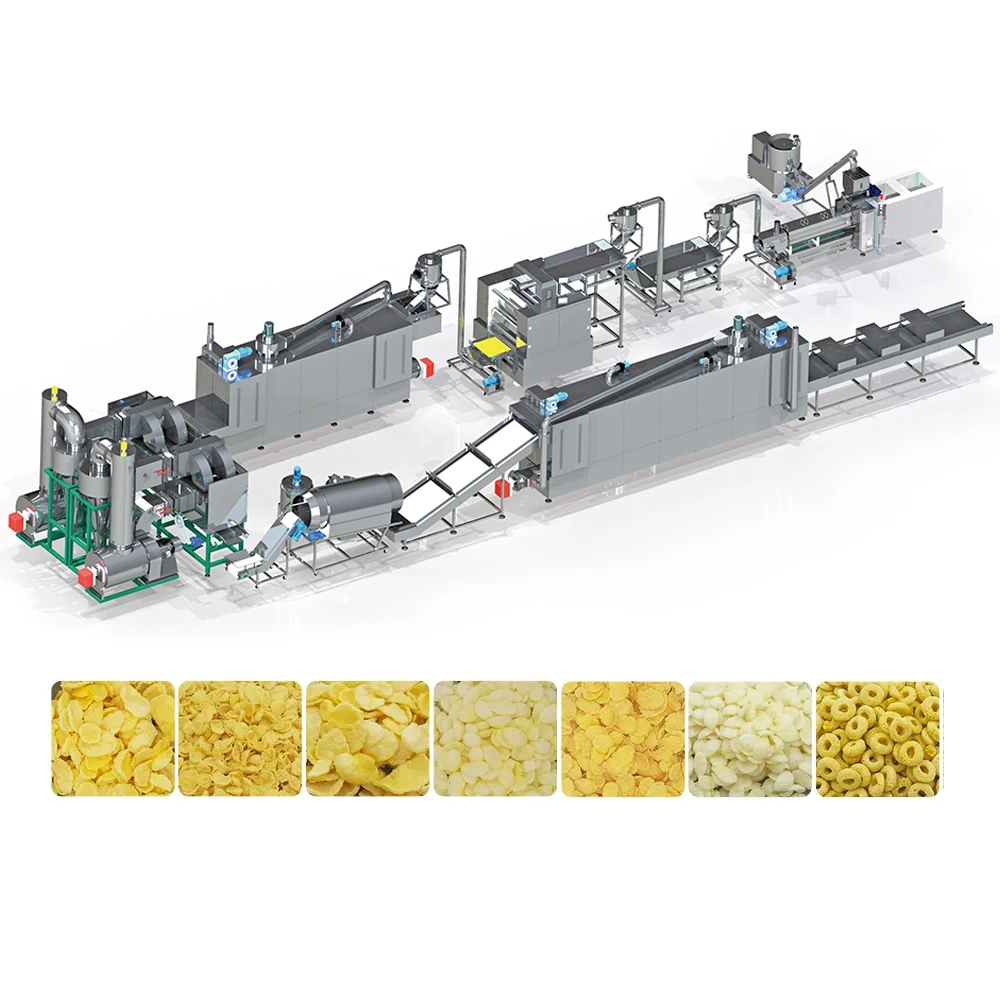
Screw & Die Matching — Configuration is specified to your cereal raw material and target flake density, not copied from a generic build, ensuring controlled expansion from corn, wheat, oat, or barley inputs.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Breakfast Cereal Corn Flake Production Line |
| Models Available | MT70 / MT85 / MT75 |
| Screw Type | Twin Screw |
| Installed Power | MT70: 160 kW / MT85: 190 kW / MT75: 210 kW |
| Power Consumption | MT70: 120 kW / MT85: 140 kW / MT75: 150 kW |
| Output Capacity | MT70: 150–200 kg/h (basis to be confirmed) / MT85: 300–400 kg/h (basis to be confirmed) / MT75: 300–500 kg/h (basis to be confirmed) |
| Overall Dimensions (L×W×H) | MT70: 41 × 1.5 × 2.2 m / MT85: 43 × 1.5 × 3.2 m / MT75: 45 × 1.5 × 3.5 m |
| Control System | PLC with MCC integration |
| Flaking Rollers | Hydraulic double-roller system, dual-motor drive, infrared temperature pipe control |
| Dryer Heating Source | Gas or Electric (configurable) |
| Roasting Oven | Hot air with conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Basic Materials | Corn, rice, wheat, oat, barley powder |
| Final Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Extruder Features | Automatic lubrication, cooling function, wear-resistant screw elements |
| Standards | CE / ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal | Corn grits and corn flour at controlled moisture |
| Sugar-coated corn flakes | Corn base with sugar syrup glazing post-roast |
| Shaped cereal snacks (fruit loops, wheat circles) | Wheat, oat, and barley blends through die changes |
| Fortified breakfast cereal formats | Grain powder mixes with added nutritional premix |
| Multi-grain flake production | Blends of corn, rice, and oat with adjusted barrel profile |
Why Nominal Capacity Means Nothing Without Material Context
A corn flakes extrusion production line rated on one grain blend will behave differently on yours until screw geometry, die aperture, and barrel zones are matched to your actual formula.
I once watched an entire batch of wheat-circle product get rejected because the extrusion setup was built around a corn-only assumption. The client had signed off on a line capacity figure, but their recipe included a significant whole-wheat and oat fraction. The screw profile never saw reconfiguration, so starch gelatinisation was incomplete. The flakes came out dense, the roaster could not open up the texture, and the final bowl-life was unacceptable. Nobody caught it until commissioning on-site, where rework costs multiply fast [NEED_CITE: cost of on-site rework versus factory trial validation]. That is why a corn flakes extrusion production line must be validated on the buyer’s actual raw material before the configuration is locked.
Barrel Temperature Profiling Across Grain Types
Corn, wheat, oat, and barley each demand a different thermal history inside the barrel to reach full starch gelatinisation without premature moisture flash-off. The corn flakes extrusion production line allows zone-by-zone heating adjustment so that a high-fibre wheat blend can receive more gradual heat input, while a pure corn grit formula can run a steeper profile. Getting this wrong shows up as uneven expansion downstream at the flaking rollers, where some pellets flatten cleanly and others crack or split.
Die Aperture and Pellet Geometry Before Flaking
The die plate determines pellet cross-section and wall thickness, which in turn governs how the hydraulic flaking rollers compress each piece. A fruit loop die with a thin annular gap will respond to roller pressure differently than a solid star die. Die design on this line is specified against the target flake thickness and the raw material’s elastic recovery after compression [NEED_CITE: relationship between die geometry and flake integrity in twin-screw cereal extrusion]. Mismatched die and roller settings produce flakes that either shatter during roasting or remain too dense to achieve the expected crispness.
Reading the Specs That Actually Matter
The installed power figures — ranging from 160 kW on the MT70 to 210 kW on the MT75 — reflect motor capacity available for shear and pressure generation inside the barrel, not direct energy draw. Actual power consumption sits lower at 120 kW to 150 kW depending on model and load. The hydraulic flaking system uses dual motors for independent roller driving, which allows differential speed adjustment when processing pellets of varying moisture content. Infrared temperature sensors on the flaking rollers prevent overheating that can cause surface tackiness before the product enters the dryer. The roasting oven’s conciliation burner paired with two circulating fans and a cyclone dust collector ensures that fine particulate does not recirculate and scorch onto the flake surface.
The Hidden Cost of a Copied Screw Configuration
When screw elements and die plates are selected from a standard catalogue rather than matched to a specific grain formulation, the consequences surface late and expensively. Under-gelatinised starch produces flakes with a chalky centre that consumers notice immediately. Over-sheared material generates excessive fines at the cutting stage, reducing yield and loading the dryer with dust. The roaster then has to work harder to achieve colour uniformity across a mix of intact flakes and fractured pieces [NEED_CITE: impact of screw wear and configuration drift on cereal flake consistency]. These issues compound across every downstream station because throughput balancing was designed around a product specification that the extruder is not actually delivering.
Why Procurement Should Start With a Trial Run
The in-house testing workshop runs your actual raw material through the configured screw and die set before the line ships. This step catches the mismatch between a quoted capacity and what your specific corn, wheat, or oat blend will produce in practice. Screw configuration records are documented against your formula, so re-ordering wear parts later does not require re-engineering. Throughput calculations across every station — extruder, flaker, dryer, roaster, coater — are validated with real product, not theoretical mass flow.
What Sets This Engineering Approach Apart
Complete line design from batching through packing means the extruder output is matched to flaker intake, dryer residence time, and roaster capacity as a single system rather than assembled from disconnected vendors. Barrel temperature profiles and moisture-shear parameters are developed for cereal applications specifically, not adapted from snack or pet food builds. Pre-sales consultation includes line layout and capacity calculation grounded in your target flake density and bowl-life requirement. The control system supports PLC automation with MCC integration, configurable to your facility’s voltage and preferred operator language [NEED_CITE: PLC and MCC control standards for food processing machinery exports].
Documentation & Verification
- Line layout and throughput calculation matched across extruder, flaker, dryer, and roaster
- Screw and die configuration record documented against your grain formula
- Trial run report on your raw material from the testing workshop
- Electrical schematic with voltage and frequency confirmed to your facility
- CE declaration of conformity and ISO certificate for export compliance
- Wear parts list specifying screw elements, die plates, and roller covers
Installation, Commissioning & Support
- Foundation planning accounts for the 41–45 m line footprint and 2.2–3.5 m headroom across models
- Dedicated power circuit sized for up to 210 kW installed load on the MT75
- Assembly from shipped modules with station-by-station alignment verification
- First-run parameter setting for barrel zones, flaker pressure, and roaster temperature on your material
- Operator training covering PLC interface navigation and MCC safety interlocks
- Spare screw elements and die plates supplied with initial delivery for first replacement cycle
What We Need to Configure Your Line
Share your grain formulation — whether it is a single-source corn grit or a multi-grain blend with oat and barley fractions — along with the target flake density and bowl-life specification your market expects. Confirm your facility voltage, frequency, and preferred control language so that electrical schematics and PLC programming are finalised before production. If you are planning shaped formats like fruit loops or wheat circles alongside standard flakes, indicate the full product range so the die inventory and flaker setup cover every SKU from day one.
Frequently Asked Questions
Q: How is screw configuration and die design matched to my specific cereal raw material and target flake density?
A: Each screw element sequence and die aperture is selected based on your grain type, moisture content, and the flake density your market requires. The configuration is documented and validated through a trial run on your actual material in the testing workshop before shipment, so the extrusion parameters are locked to your formula rather than a generic template.
Q: Can a trial run be performed on my actual raw material before shipment to verify expansion and texture?
A: Yes. The in-house testing workshop runs your grain formulation through the configured extruder, flaker, and roaster to verify starch gelatinisation, flake thickness, and final crispness. A trial run report is provided, and any necessary screw or die adjustments are made before the line is released for shipping.
Q: How is throughput balanced between extruder, flaker, dryer, and roaster to avoid bottlenecking?
A: Line layout and capacity calculation treat every station as a linked system. Extruder output is matched to flaker intake rate, dryer residence time is sized for the moisture removal load, and roaster capacity accounts for the surface expansion required. This prevents any single station from constraining the others.
Q: What barrel temperature profile and moisture range are needed for corn versus wheat or oat-based flakes?
A: Corn typically requires a steeper barrel temperature ramp and lower feed moisture to achieve clean expansion. Wheat and oat blends with higher fibre content need more gradual heating and slightly elevated moisture to ensure full gelatinisation without premature flash-off. Both profiles are developed and verified during the trial run stage.
Q: How are voltage, frequency, and control language confirmed before commissioning?
A: Electrical schematics and voltage specifications are confirmed during the pre-production stage based on your facility’s power supply. The PLC interface and MCC labels are prepared in your preferred operator language, and all settings are verified at the factory before the control cabinets are sealed for dispatch.