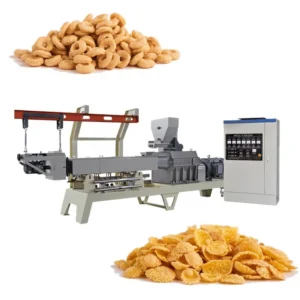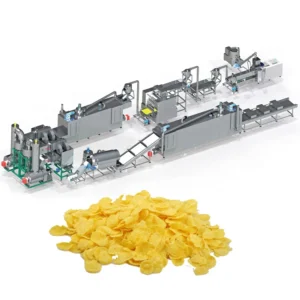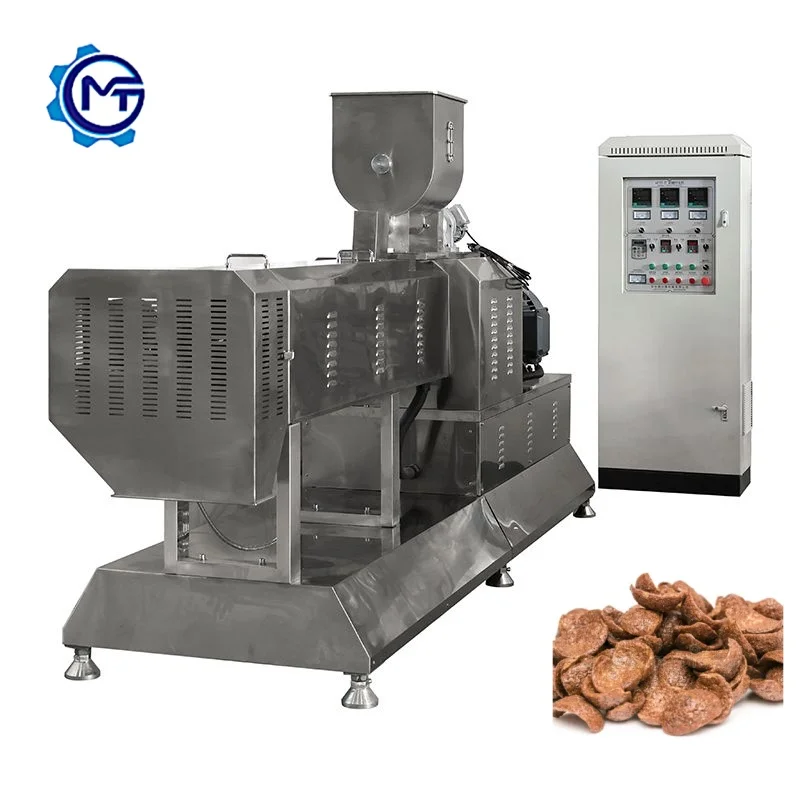
Matched Screw Configuration — Every MT70 / MT85 / MT75 corn flakes extrusion line is configured with screw elements and die geometry selected against the buyer’s actual cereal blend and target flake density before production begins.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes and Breakfast Cereal Extrusion Line |
| Models Available | MT70, MT85, MT75 |
| Screw Type | Twin-screw |
| Installed Power | MT70 — 160 kW; MT85 — 190 kW; MT75 — 210 kW |
| Power Consumption | MT70 — 120 kW; MT85 — 140 kW; MT75 — 150 kW |
| Output Capacity | MT70 — 150–200 kg/hr (basis to be confirmed); MT85 — 300–400 kg/hr (basis to be confirmed); MT75 — 300–500 kg/hr (basis to be confirmed) |
| Overall Dimensions | MT70 — 41 × 1.5 × 2.2 m; MT85 — 43 × 1.5 × 3.2 m; MT75 — 45 × 1.5 × 3.5 m |
| Control System | PLC control (flaking machinery); MCC and PLC available per line configuration |
| Screw Features | Automatic lubricating and cooling function; wear-resistant screw material |
| Flaking Machinery | Hydraulic double-roller system; double motors for separate roller driving; infrared sensor temperature control |
| Dryer Heating Source | Gas / Electric / Steam (multi-fuel) |
| Hot Air Roasting Oven | Conciliation burner; two separate circulating fans; cyclone dust removal device; vibrating pan with high-temperature spraying tubes |
| Basic Raw Materials | Corn, rice, wheat, oat, barley powder |
| Final Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (by adjusting extruder mould) |
| Certifications | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour through mixing, extrusion, flaking, drying and hot air roasting |
| Sugar-coated corn flakes | Corn base with sugar spraying and coating drum added after roasting stage |
| Multi-grain breakfast flakes | Rice, wheat, oat and barley blends processed through the same extrusion platform |
| Shaped puffed cereal formats | Rings, balls, stars, fruit loops and other shapes by changing extruder die |
| Cocoa-based breakfast cereal | Cocoa flour mixed with cereal base for flavoured extruded cereal production |
Why a Generic Screw Build Ruins Your Corn Flake Texture
A twin-screw extruder shipped with a default screw configuration rarely produces the flake density and surface blistering that breakfast cereal buyers expect on the shelf.
I have watched corn flakes come off a roasting oven looking like flat, dense chips because the extruder barrel was running a standard screw build designed for a different starch matrix. The starch gelatinisation was incomplete, the moisture window was too narrow, and the flake had no internal structure to develop crispness during roasting. When that same line was reconfigured with screw elements matched to the buyer’s specific corn variety and moisture content, the flake thickness, expansion behaviour and bowl-life changed completely. The corn flakes extrusion line production technology only delivers consistent results when the screw profile, die geometry and barrel temperature zones are specified against the actual raw material going into the hopper, not against a catalogue default [NEED_CITE: starch gelatinisation requirements for cereal extrusion].
How Screw Elements Shape the Corn Flake
The twin-screw extruder in this line uses interchangeable screw elements that control shear intensity, residence time and pressure profile along the barrel. For corn flakes, the goal is partial gelatinisation — enough to bind the dough sheet but not so much that the material puffs uncontrollably when it hits the flaking rollers. By adjusting the ratio of conveying elements to kneading blocks, the extrusion process can hold a stable dough ribbon at the die face, which is essential for uniform flake thickness downstream.
Barrel Temperature Zones and Moisture Control
Each barrel section on the MT70, MT85 and MT75 has independent heating and cooling circuits. The operator sets a temperature gradient that starts lower in the feed zone and rises through the compression and metering sections. Combined with controlled steam or water injection at the mixer, this gradient determines how much moisture the starch absorbs before it reaches the die. Too much moisture and the flake sticks to the rollers; too little and the sheet cracks before it enters the dryer. Getting this window right is the core of corn flakes extrusion line production technology, and it can only be validated by running the buyer’s actual material through the machine before the line ships [NEED_CITE: moisture-temperature interaction in cereal extrusion processes].
Reading the Power and Capacity Data
The installed power ratings across the MT70 at 160 kW, MT85 at 190 kW and MT75 at 210 kW reflect the total connected load of every station from mixer to packing conveyor, not just the extruder motor. Actual power consumption sits lower — 120 kW, 140 kW and 150 kW respectively — because not all motors run at full draw simultaneously. The output capacity figures depend entirely on the raw material formulation, target moisture at the die and the flake thickness setting on the hydraulic rollers. A denser multi-grain blend will move through the line at a different mass flow rate than pure corn grits, which is why the capacity ranges should be confirmed against the specific recipe before the line is finalised. The automatic lubricating and cooling function on the screw shaft extends wear-resistant screw element life under continuous operation at these power levels.
What Happens When the Flaker and Roaster Are Undersized
A common failure on cereal lines is an extruder that runs at its rated output while the flaking rollers cannot keep pace, creating a bottleneck that forces the operator to throttle back the entire line. The hydraulic double-roller system on this flaking machinery uses separate motors for each roller and infrared temperature sensing to maintain consistent gap and surface condition. If the downstream hot air roasting oven does not have adequate residence time — governed by the vibrating pan speed and the two circulating fans — the flakes emerge without proper surface blistering and the crispness that the market expects. The cyclone dust removal device on the roasting oven also prevents fine particle buildup that would otherwise affect heat transfer and create inconsistent batch colour [NEED_CITE: cereal roasting oven airflow requirements for uniform blistering].
Sourcing the Line Based on Extrusion Science
The screw configuration and die design are documented against your raw material specification before the extruder is assembled, not selected from a standard build sheet. Every station from the batching system through the mixer, extruder, flaker, dryer, roasting oven and packing conveyor is throughput-matched so that no single machine bottlenecks the rest. The in-house testing workshop runs your actual corn, rice or multi-grain blend through the extruder and flaker before the line ships, producing a trial run report that confirms flake density, thickness and expansion behaviour. Multi-fuel dryer options across gas, electric and steam allow the line to match your facility’s utility infrastructure. The PLC control system on the flaking machinery and MCC panel on the main extruder give operators repeatable batch settings rather than relying on manual adjustment.
Documentation & Verification
- Screw and die configuration record matched to your specific cereal blend and target flake density
- Trial run report on your raw material confirming flake thickness, expansion and crispness before shipment
- Line layout drawing with throughput calculation showing matched capacity at every station
- Electrical schematic with voltage, frequency and control language confirmed for your facility
- Operation and maintenance manual covering screw element replacement intervals and roller gap adjustment
- CE declaration of conformity and ISO certificate for import clearance
Installation, Commissioning & Support
- Foundation plan accounting for the MT75 line footprint of 45 × 1.5 × 3.5 m and vibration from the roasting oven vibrating pan
- Dedicated electrical circuit sized for 210 kW installed power on the MT75 with voltage and frequency matching local supply
- Modular station delivery with on-site mechanical assembly and belt alignment across all conveying sections
- First-run commissioning with screw speed, barrel temperature profile and flaking roller gap set to trial-run parameters
- Operator training covering PLC interface navigation, recipe storage and hydraulic roller pressure adjustment
- Wear parts list including replacement screw elements, die plates and roller covers with recommended stock quantities
What to Include in Your Inquiry
To configure the corn flakes extrusion line production technology correctly, share your base raw material type and any blend ratios for multi-grain formats. Specify the target flake thickness and whether you need natural or sugar-coated output, as this determines whether the coating drum and sugar melting system are included. Provide your facility voltage and frequency so the MCC panel and motor specifications are matched before production, and confirm available fuel type for the dryer to select between gas, electric or steam heating.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal raw materials?
A: The screw element sequence is chosen based on the starch type, fat content and particle size of your raw material. Kneading block placement and conveying element pitch are adjusted to achieve the correct shear and residence time for partial gelatinisation. A configuration record is generated for your specific blend and kept on file for future reference.
Q: What barrel temperature and moisture range work for corn flakes?
A: Barrel zones typically run a gradient from the feed section to the metering section, with steam or water added at the mixer to reach the moisture window needed for proper dough formation. Exact values depend on the corn variety and grind size, which is why a trial run on your material is the only way to confirm the working range before shipment.
Q: How does a pre-shipment trial run validate the extrusion parameters?
A: Your raw material is fed through the extruder, flaker and roasting oven in the testing workshop. Flake thickness, density, expansion ratio and surface blistering are measured against your product specification. Any adjustments to screw elements, die geometry or barrel temperatures are made during this run, and the final settings are recorded in the trial report.
Q: How is throughput matched between the extruder, flaker, dryer and roaster?
A: Each station is sized so that its maximum processing rate aligns with the extruder output on your specific material. The flaker roller width, dryer belt length and roasting oven pan speed are all calculated during the layout phase. This prevents situations where one machine runs below capacity while another creates a bottleneck upstream.