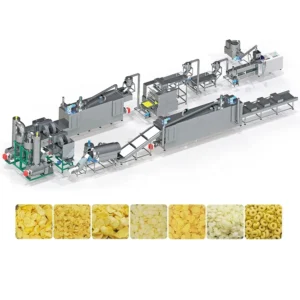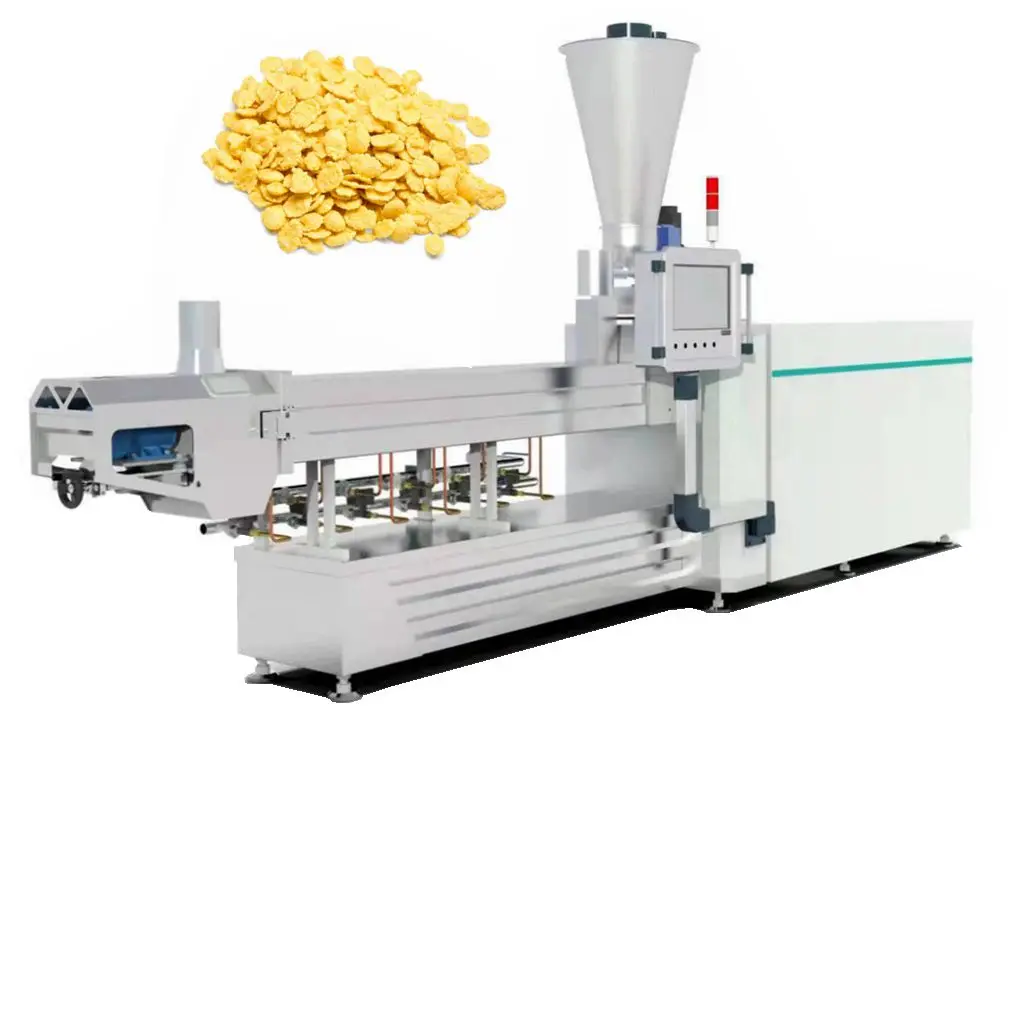
Precision-matched screw geometry — Every MT75 corn flake line ships with screw elements and die profiles selected against your declared cereal blend, not copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Corn Flakes Production Line |
| Extruder Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Capacity | 300-500 kg/h (basis not stated in source — confirm raw material, moisture content and product format) |
| MT-75 Extruder Output | 200-300 kg/h (basis to be confirmed) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | MCC and PLC |
| Heating Source (Dryer) | Gas or Electric |
| Flaking Machinery | Hydraulic double rollers, double motors, infrared sensor temperature control |
| Hot Air Roasting Oven | Vibrating pan, high-temperature spraying tubes, two circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Screw Feature | Automatic lubricating and cooling, wear-resistant screw elements |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Corn grits, corn flour, de-germed corn |
| Sugar-coated breakfast cereal | Corn, rice, wheat, oat, barley powder blends |
| Shaped cereal formats | Same cereal blends through interchangeable die plates (ball, tube, ring, star, wheel, flower, heart) |
| Fortified breakfast cereals | Multi-grain blends with vitamin and mineral premix addition |
Why Your Corn Flake Texture Fails Before It Reaches the Dryer
Extrusion screw configuration and die geometry determine whether your flakes crisp properly or shatter on contact with milk.
Process engineers often trace poor bowl life back to the dryer or roaster, but the root cause sits inside the extruder barrel. A screw profile that delivers insufficient shear leaves starch under-gelatinised, producing dense half-rounds that never blister properly in the hot-air oven. Conversely, excessive shear with the wrong L:D ratio causes premature expansion, and the resulting flakes collapse during flaking into thin, fragile sheets [NEED_CITE: starch gelatinisation thresholds in cereal extrusion]. When the corn flakes extrusion line specifications and screw configuration are not matched to the buyer’s actual flour blend and moisture input, no amount of downstream adjustment recovers the texture.
Matching Screw Profile to Your Cereal Blend
The degree of starch gelatinisation inside the barrel dictates everything downstream — flake integrity, roasting response, and final crispness. For de-germed corn grits, the screw elements need moderate shear and a specific residence time to achieve full cook without over-expanding the dough mass before it exits the die. Multi-grain blends containing oat or barley behave differently due to varying protein and fibre content, requiring a distinct screw arrangement and barrel temperature profile to reach the same gelatinisation endpoint.
Thermal Sequencing from Flaking Through Roasting
The hydraulic double-roller flaker compresses the extruded half-rounds into sheets of controlled thickness, with infrared temperature monitoring keeping the roller surface within a tight band. Sheet thickness at this stage directly governs how the hot-air roasting oven performs: thicker flakes require longer residence and higher air velocity to develop surface blisters without scorching. The vibrating pan and dual circulating fans in the roaster distribute heat across the bed, while the cyclone dust removal captures fines that would otherwise recirculate and burn. Getting corn flakes extrusion line specifications and screw configuration right at the front end ensures the flaker and roaster operate within their designed thermal envelope rather than compensating for upstream inconsistency [NEED_CITE: thermal profiling in breakfast cereal roasting ovens].
Reading the Specification Sheet Against Your Raw Material
The 210 kW installed power on the MT75 reflects the energy required to drive twin-screw extrusion at volumes suitable for commercial corn flake output. However, rated power alone does not predict how the extruder handles your specific blend — a high-fibre oat mix demands more torque at lower screw speed than pure corn grits. The PLC-controlled system at the flaker synchronised with MCC across the full line allows operators to adjust extruder throughput and roller gap in tandem, maintaining consistent flake weight per unit area. Barrel zones are independently heated, so the temperature gradient from feed to die can be profiled to the raw material’s gelatinisation curve. When evaluating any corn flakes extrusion line specifications and screw configuration, the critical question is whether the vendor has mapped those zones to your declared blend, not whether the machine reaches a nominal temperature.
The Hidden Cost of a Generic Screw Build
A production line configured from generic screw elements and a standard die plate will run, but it will produce flakes that deviate from your target density and bowl life. Buyers discover this only after commissioning, when adjusting dryer temperature and roaster airflow fails to correct texture faults that originated inside the barrel. The cost includes weeks of lost production, repeated raw material waste, and in some cases replacement of the entire screw assembly to achieve the specification the market expects [NEED_CITE: extrusion screw retrofit costs in cereal processing].
Why Procurement Starts With Your Raw Material Sample
Every MT75 line configuration begins with the buyer’s declared cereal blend and target flake specification, not a catalogue default. The in-house testing workshop runs your actual raw material through the extruder before shipment, generating a trial run report that documents gelatinisation, flake integrity, and roasting behaviour. Screw element arrangement and die geometry are recorded and shipped with the machine, so replacements match the original build. Line layout and capacity calculation show throughput matching across extruder, flaker, dryer, roaster, and coater, preventing the bottleneck that occurs when stations are assembled from unmatched standalone units. Electrical schematics and voltage are confirmed to the buyer’s site standard before production begins, eliminating commissioning delays from incompatible power supply or untranslated PLC interfaces [NEED_CITE: voltage and frequency confirmation in export machinery contracts].
Documentation & Verification
- Screw and die configuration record matched to your declared corn or multi-grain blend
- Trial run report on your actual raw material confirming gelatinisation and flake integrity
- Line layout showing throughput balance from extruder through roaster to coater
- Electrical schematic with voltage and PLC language confirmed to your site standard
- Factory test record documenting barrel temperature profile and flaker roller gap settings
Installation, Commissioning & Support
- Foundation plan sized to the 45 m line footprint with utility connection points marked
- Dedicated electrical circuit rated for 210 kW installed load at confirmed voltage and frequency
- Modular station delivery with extruder, flaker, dryer, roaster, and coater assembled on-site
- First-run parameter setting using your raw material with screw speed and barrel zone mapping
- Operator training covering PLC adjustments at the flaker and MCC line-wide controls
- Wear parts list specifying screw elements, die plates, and flaker roller surfaces for reorder
What We Need to Configure Your Line
Provide your cereal blend composition — including whether you use de-germed corn grits, whole corn flour, or a multi-grain mix — along with your target flake thickness and bowl-life specification. Share your workshop dimensions and ceiling height so the line layout accommodates the 3.5 m equipment height and dryer ducting. Confirm your local voltage, frequency, and preferred PLC language to ensure electrical and control compatibility from day one.
Frequently Asked Questions
Q: How is screw configuration selected for corn versus multi-grain blends?
A: Corn grits require a screw profile that delivers moderate shear for full gelatinisation without over-expansion, while blends containing oat or barley need adjusted element spacing and barrel zone temperatures to account for different protein and fibre behaviour. The configuration is set based on trial runs with your actual blend before the extruder ships.
Q: What barrel temperature profile prevents premature expansion in corn flake extrusion?
A: The barrel is divided into independently heated zones, with lower temperatures at the feed section to prevent flash expansion and progressively higher zones toward the die to complete starch cook. The exact gradient depends on your raw material moisture and composition, verified during the in-house testing workshop trial.
Q: How does flaker roller gap and temperature influence roasting results?
A: The hydraulic double-roller flaker compresses extruded half-rounds into sheets whose thickness determines how the hot-air roaster develops surface blisters and crispness. Infrared temperature control on the rollers keeps the sheet surface within a consistent range, preventing sticking or uneven compression that leads to variable roasting response.
Q: How is line throughput verified to prevent bottlenecks between stations?
A: Throughput is calculated across the extruder, flaker, dryer, roaster, and coating drum so each station handles the output of the one before it. The PLC and MCC control system synchronises extruder feed rate with downstream conveyor speed and dryer residence time, documented in the line capacity calculation before build begins.