
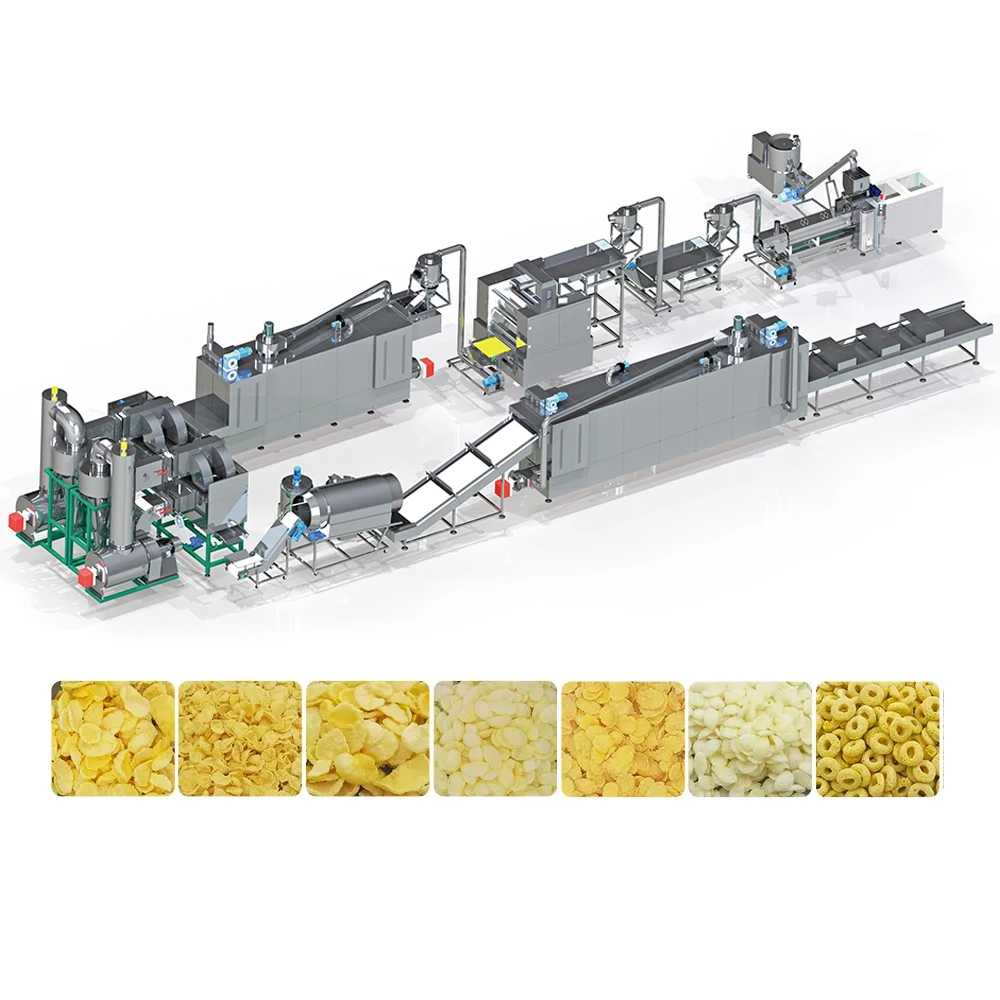
Customized Screw and Die Design — screw configuration and die geometry matched to your specific corn formulation and target flake density, verified by in-house trial before dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Model Options | MT70 / MT75 / MT85 |
| Screw Type | Twin Screw |
| Installed Power | 160 kW (MT70) / 190 kW (MT85) / 210 kW (MT75) |
| Power Consumption | 120 kW (MT70) / 140 kW (MT85) / 150 kW (MT75) |
| Output Capacity | 150–200 kg/h (MT70) / 300–400 kg/h (MT85) / 300–500 kg/h (MT75) (basis to be confirmed) |
| Overall Dimensions (L×W×H) | 41 × 1.5 × 2.2 m (MT70) / 43 × 1.5 × 3.2 m (MT85) / 45 × 1.5 × 3.5 m (MT75) |
| Control System | PLC |
| Flaking Drive | Double motors with separate roller driving; hydraulic system |
| Flaking Temperature Control | Infrared sensor for even temperature pipe management |
| Dryer Heating Source | Gas or Electric (configurable) |
| Hot Air Roasting Oven | Vibrating pan, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Extruder Features | Automatic lubricating and cooling function; wear-resistant screw material |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits or corn flour at controlled moisture |
| Sugar-coated breakfast cereals | Corn, rice, or multi-grain base with sugar or honey coating |
| Multi-grain cereal flakes | Blends of wheat, oat, barley, and rice powder |
| Shaped cereal snacks | Ball, tube, ring, star, wheel, heart shapes via die exchange |
Why Nominal Capacity Figures Fail on Corn Flakes Lines
A corn flakes extrusion production line rated at a fixed throughput on generic corn grits often cannot sustain that rate when the buyer switches to a locally sourced, higher-fat or higher-fiber corn variety.
Extruder throughput must be verified against your actual raw material profile, moisture content, and target flake thickness before the line is finalized.
I have seen lines where the extruder was pushing volume, but the flakes came out dense and under-expanded because the screw profile was not matched to the starch composition of the buyer’s corn. The dryer then struggled with residual moisture, and the roaster could not achieve proper blistering. The bottleneck was never the motor size — it was the gap between assumed and actual material behaviour [NEED_CITE: starch gelatinisation behaviour across corn varieties].
How Screw Profile and Barrel Temperature Shape the Flake
The corn flakes extrusion production line relies on the twin-screw extruder to cook, shear, and form the dough in a single pass. Screw element arrangement — mixing blocks, kneading discs, and conveying sections — controls residence time and mechanical energy input. A profile optimized for pure corn grits may over-shear a multi-grain blend, breaking starch chains and reducing expansion potential downstream at the flaking rollers.
Barrel temperature zones work in tandem with screw configuration. Early zones hydrate and pre-cook the starch, while later zones build the pressure needed for uniform die discharge. Infrared-monitored temperature pipes on this line help maintain that thermal balance through the flaking stage.
Moisture, Shear, and the Gelatinisation Window
Starch gelatinisation requires a precise combination of moisture, heat, and shear. Too little moisture and the corn meal passes through undercooked, producing hard, glassy flakes that shatter in the bowl. Too much and the extrudate becomes sticky, adhering to flaking rollers and tearing rather than compressing into clean sheets.
The hydraulic flaking system with independent roller drives addresses this by allowing differential speed and pressure adjustments. When a batch arrives at the rollers with slightly higher moisture than target, the operator can increase roller gap and reduce pressure to compensate, maintaining flake integrity without halting the corn flakes extrusion production line [NEED_CITE: moisture tolerance windows in twin-screw cereal extrusion].
Reading the Specs That Actually Matter
The installed power figures — ranging from 160 kW to 210 kW across the MT70, MT75, and MT85 — tell you what the motors can deliver, but the power consumption values (120 kW to 150 kW) reflect real operating load under typical conditions. The gap between installed and consumed power indicates thermal and mechanical headroom.
The twin-screw design matters directly for corn flakes: it provides positive conveying of viscous, high-moisture dough that a single screw would struggle to push consistently through a flaking die. The automatic lubricating and cooling function on the extruder barrel reduces friction-induced hot spots that can scorch starch and create dark specks on the final flake.
The roasting oven uses a vibrating pan with high-temperature spraying tubes and two separate circulating fans, which distributes heat evenly across the flake bed. This prevents the common defect of surface-blistered but internally-soggy flakes that lose crispness within minutes of hitting milk.
What Happens When Stations Are Mismatched
An extruder running at full output feeds flakes into a dryer that cannot evaporate moisture fast enough. Flakes arrive at the roaster still tacky, clumping together and blocking the vibrating pan. The coating drum receives uneven product, and sugar glaze pools on some flakes while others pass through bare.
This cascade starts with a single mismatch: the dryer capacity was specified against a nominal extruder output rather than the actual throughput on the buyer’s formulation. The line physically runs, but effective yield drops and operators spend shifts clearing blockages rather than monitoring quality [NEED_CITE: throughput matching across cereal line stations].
What Meiteng Delivers on This Line
Every station on this corn flakes extrusion production line — from the batching mixer through extrusion, flaking, drying, roasting, coating, cooling, and packing — is specified as a single package, so throughput is matched at each transfer point rather than assembled from separate vendor quotes.
Screw configuration and die geometry are selected based on your raw material sample and target flake specification, not copied from a generic build. The in-house testing workshop runs your actual corn or multi-grain formulation before the line ships, producing a trial run report that confirms expansion, flake thickness, and roasting behaviour.
The PLC control system manages the full sequence, and electrical schematics are confirmed against your facility voltage and frequency before production begins. Wear parts — screws, dies, roller shells — are documented and available from the first replacement cycle.
Documentation & Verification
- Line layout and capacity calculation matched to your factory footprint
- Screw and die configuration record tied to your raw material trial
- Trial run report on your corn or multi-grain formulation before dispatch
- Electrical schematic with voltage and frequency confirmed for your market
- Operation and maintenance manual with wear parts list
- CE declaration of conformity
Installation, Commissioning & Support
- Foundation planning based on the 41–45 m line length and station weights
- Dedicated power circuits sized to the 120–150 kW operating consumption range
- Modular station delivery with on-site assembly and alignment of flaking rollers
- First-run parameter setting for barrel zones, roller pressure, and roaster temperature
- Operator training on PLC interface, die changes, and hydraulic roller adjustment
- Wear parts inventory including screws, dies, and roller shells for initial spares
Before You Request a Quote
To configure a corn flakes extrusion production line that matches your production target, share your raw material type and typical moisture content, your target flake thickness and whether you plan to run natural, sugar-coated, or both variants. Include your facility voltage, frequency, and available floor space with ceiling height. If you have existing upstream milling or downstream packing equipment, note the interface requirements so the line layout accounts for those connections.
Frequently Asked Questions
Q: How is extruder capacity verified against my specific raw material?
A: Your corn or multi-grain sample is run through the extruder in the testing workshop before shipment. The trial records throughput, expansion ratio, and moisture at each station. The configuration — screw profile, die geometry, barrel temperatures — is then adjusted if the results deviate from your target flake specification.
Q: How do screw configuration and die design affect flake density?
A: The arrangement of kneading blocks and conveying elements determines how much shear energy the dough receives and how long it stays in the barrel. Die geometry controls the extrudate shape and thickness entering the flaking rollers. Together, they set the cooked dough structure that determines final flake density and bowl-life.
Q: What barrel temperature profile is used for corn versus multi-grain blends?
A: Pure corn grits typically require a progressive temperature ramp that builds gradually through the barrel zones. Multi-grain blends containing oat or barley often need lower peak temperatures because their starch and fiber composition gelatinises at different thresholds. The exact profile is established during the raw material trial run.
Q: How are downstream stations matched to extruder throughput?
A: The dryer evaporation rate, roaster pan capacity, and coating drum volume are each calculated against the confirmed extruder output on your specific formulation. This prevents situations where the extruder produces faster than the dryer can handle, which causes flake sticking and downstream blockages.
Q: Can I run a trial on my own raw material before the line ships?
A: Yes. The testing workshop accepts your raw material samples and runs the full extrusion, flaking, and roasting sequence. You receive a trial run report documenting output rate, flake dimensions, expansion behaviour, and roasting results, so product development begins before installation rather than after.



