Configurable Screw Geometry — Die and screw elements are matched to your specific grain flour moisture and starch content rather than copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Corn Flakes Extruder Production Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Capacity | 300–500 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC control with MCC available |
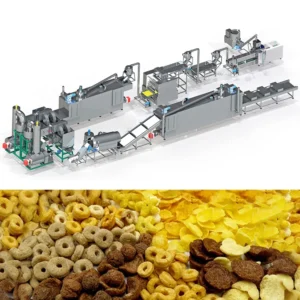
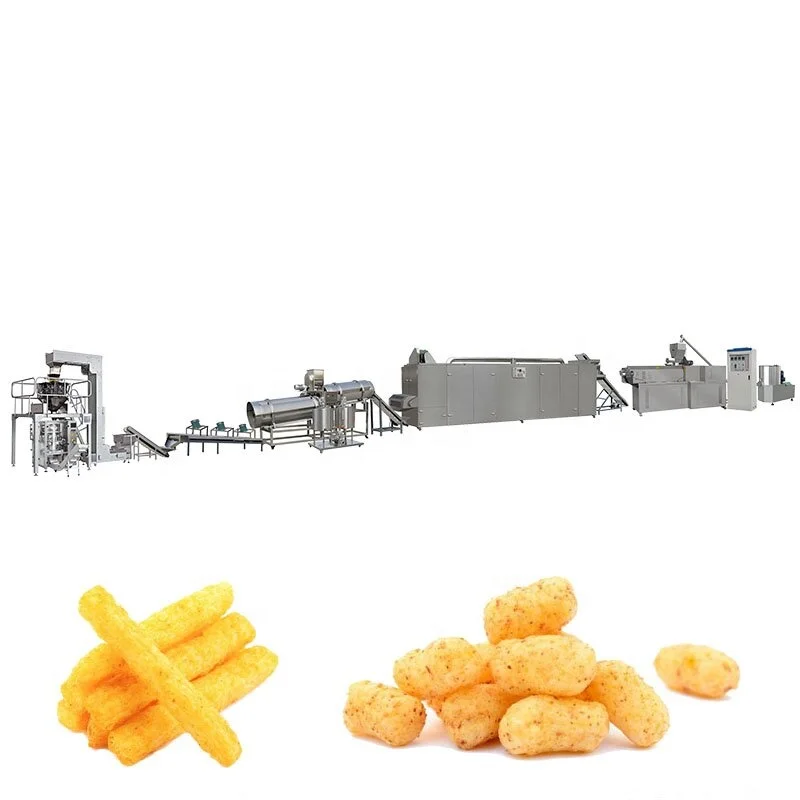
| Line Stations | Mixing, Extruding, Flaking, Drying, Hot Air Roasting, Sugar Spraying, Sugar Coating, Drying, Cooling, Packing |
| Dryer Heating Source | Gas or Electric |
| Flaking Machinery | Hydraulic double rollers with separate motor drive and infrared temperature control |
| Hot Air Roasting Oven | Vibrating pan with high-temperature spraying tubes, two circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melter, elevator, coating drum, spraying nozzle |
| Extruder Screw Feature | Automatic lubricating and cooling function |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn flour, corn grits at target moisture |
| Sugar-coated corn flakes | Corn base with sugar spray and coating drum |
| Multigrain breakfast cereals | Blends of rice, wheat, oat, and barley flour |
| Shaped cereal formats | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart via die change |
What "300 kg per Hour" Actually Depends On
Output on a corn flakes extruder machine is meaningless without the raw material formula and moisture content behind it.
I once configured a line for a breakfast cereal plant running standard corn flour. The trial went well. Then the customer blended in oat and barley after delivery, and the expansion collapsed — thick, dense flakes that could not pass through the roasting oven. The corn flakes extruder machine specifications on paper meant nothing because the actual feedstock changed. That is why confirming flour composition and moisture before screw configuration matters more than any headline capacity number [NEED_CITE: starch gelatinisation behaviour across grain types].
Shear Profile and Starch Gelatinisation in the Barrel
The twin-screw configuration inside the MT75 generates controlled shear across multiple barrel zones. Corn starch requires a precise thermal and mechanical input window to achieve full gelatinisation without over-degrading the polymer chains. Automatic lubricating and cooling within the extruder maintains barrel temperature stability, which directly governs how uniformly the dough expands when it exits the die. Inconsistent shear leads to flakes that shatter during roasting or remain doughy in the centre.
Die Geometry and the Flaking Interface
Die design determines the pellet shape and wall thickness before the material reaches the flaking rollers. A tube-shaped die produces a different compression behaviour under hydraulic rollers compared to a solid pellet. The PLC-controlled flaking machinery uses infrared sensors to monitor roller temperature evenly, ensuring that each pellet flattens to a consistent thickness. If the die geometry and roller gap are mismatched, the resulting flakes vary in density — some sink in milk while others float too high and break during packaging [NEED_CITE: cereal flake density and bowl-life performance standards].
Reading the Power and Dimension Data
The MT75 draws 150 kW in continuous operation from a 210 kW installed base, leaving headroom for start-up surges and hard material batches. The 45-metre line length encompasses every station from mixing to packing, which means the floor plan must accommodate a straight or L-shaped layout with utility drops at the dryer, roaster, and coating drum. The hot air roasting oven alone requires dedicated exhaust ducting for its cyclone dust removal system. Buyers comparing corn flakes extruder machine specifications should verify whether the quoted dimensions include all downstream stations or only the extruder section.
The Cost of a Copied Screw Configuration
When a supplier copies a screw and die setup from a previous build without adjusting for your grain blend, the consequences show up weeks after commissioning. Barrel wear accelerates because the shear distribution does not match the material’s viscosity. Flakes emerge with uneven moisture profiles, forcing the dryer to run longer and consume more energy. The roasting oven cannot correct texture defects introduced upstream. These problems are expensive to diagnose because they appear across multiple stations, and operators tend to blame the dryer or coater rather than the extrusion parameters set on day one [NEED_CITE: extrusion screw configuration impact on downstream equipment performance].
Why Engineers Specify From This Platform
Screw and die configurations are documented per order, recording the L:D ratio and element arrangement matched to the buyer’s flour blend. The in-house testing workshop runs trial batches on your actual raw material before shipment, generating expansion and moisture data that travel with the machine. Every station — from the mixer through the sugar coating drum to the cooler — is sized so throughput does not bottleneck at any single point. Electrical schematics confirm voltage, frequency, and PLC language before the panel is wired, avoiding on-site rewiring delays. CE compliance covers the full assembly, not just the extruder head.
Documentation & Verification
- Line layout and capacity calculation matched to your grain flour blend
- Screw and die configuration record with element arrangement drawing
- Trial run report on your raw material documenting expansion ratio
- Electrical schematic confirming voltage and PLC programming language
- Machine specification sheet with barrel zone temperature ranges
- CE declaration of conformity covering the complete production line
Installation, Commissioning & Support
- Foundation must support the 45-metre line footprint and vibrating roaster pan load
- Dedicated 210 kW supply circuit with confirmed voltage and frequency before wiring
- Hydraulic flaking rollers calibrated on-site to target flake thickness
- PLC parameters set during commissioning using your actual flour formulation
- Wear parts list covering screws, dies, and roller surfaces with reorder codes
- Operator training on barrel temperature zones and moisture adjustment routines
Before You Request a Quote
Provide your grain flour composition, including any oat, barley, or rice blend ratios, along with the target moisture content at the mixer outlet. Share your workshop dimensions and ceiling height so the line layout fits existing infrastructure. Specify your local voltage and frequency, and indicate the PLC interface language your operators require. If you run existing upstream milling or downstream packing equipment, note the connection points.
Frequently Asked Questions
Q: How is the screw configuration matched to a specific grain flour blend?
A: The screw element sequence — conveying, kneading, and reverse elements — is selected based on your flour’s starch content and moisture absorption rate. A trial run in the testing workshop confirms expansion behaviour before the configuration is locked in for production and documented in the configuration record shipped with the machine.
Q: What barrel temperature zones control flake density?
A: Multiple independently heated barrel zones manage starch gelatinisation progressively. Early zones hydrate the flour while later zones build the melt temperature needed for expansion at the die. The PLC monitors each zone, allowing process engineers to adjust the profile when switching between corn, wheat, or multigrain recipes.
Q: How do extrusion parameters differ between natural and sugar-coated flakes?
A: Natural flakes require higher expansion and lower exit moisture so they crisp during roasting without coating. Sugar-coated variants are extruded to a slightly denser pellet that can absorb sugar syrup in the coating drum without collapsing. Die geometry and barrel moisture targets shift accordingly between the two formats.
Q: What does the pre-shipment trial run cover?
A: Your raw material runs through the extruder, flaking rollers, and roaster under production conditions. The trial report records expansion ratio, moisture at each station, and flake thickness uniformity. Any screw or die adjustments needed are made before the machine leaves the factory, not after installation on your floor.