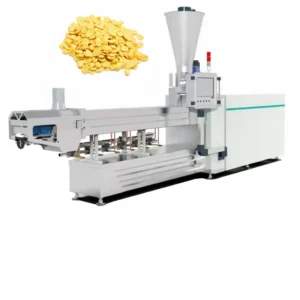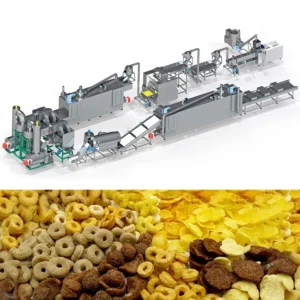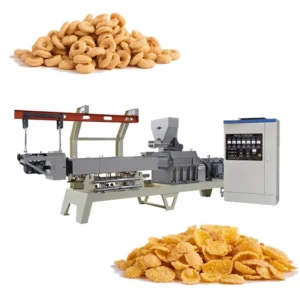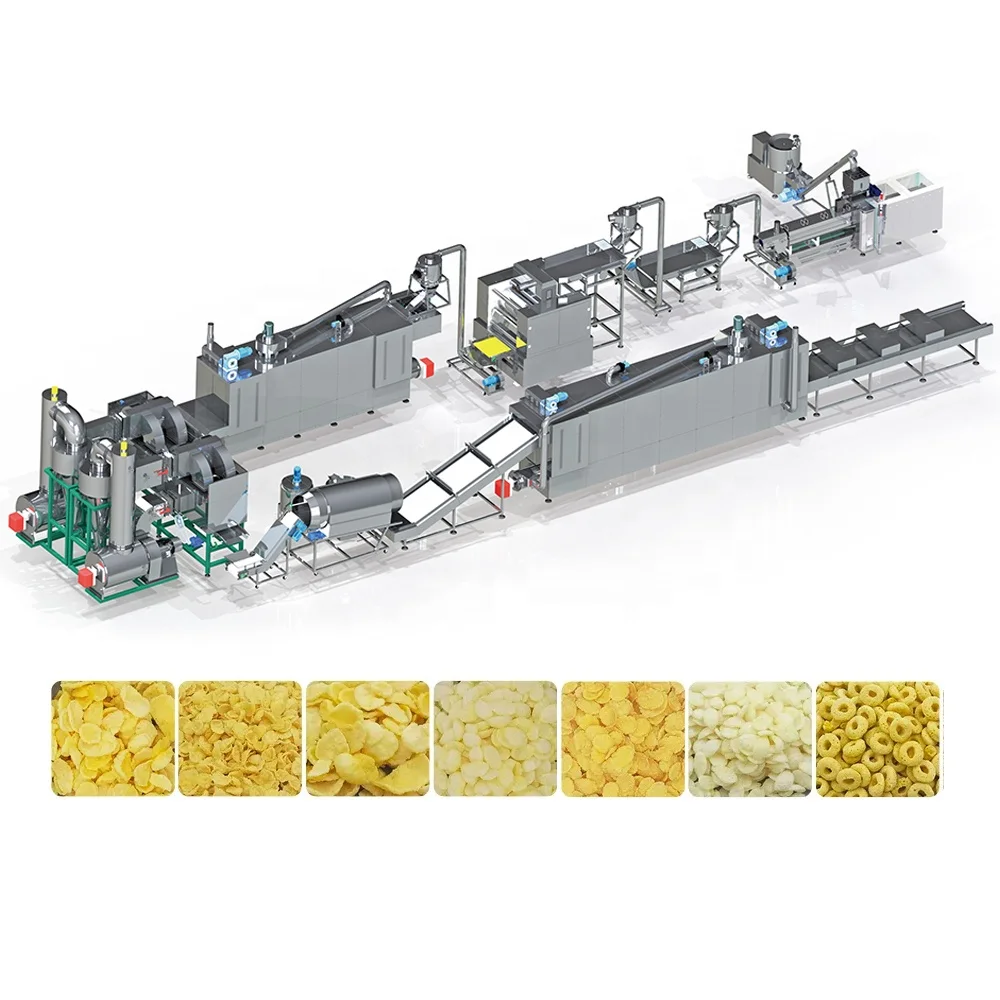
Twin-Screw Extrusion Configuration — Screw element layout and die geometry matched to the buyer’s grain blend for controlled gelatinisation and consistent flake density.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Breakfast Cereal Production Line |
| Extruder Type | Twin Screw |
| Raw Material Compatibility | Corn, rice, wheat, oat, barley powder |
| MT70 Installed Power | 160 kW |
| MT70 Power Consumption | 120 kW |
| MT70 Capacity | 150–200 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| MT70 Overall Dimensions | 41 × 1.5 × 2.2 m |
| MT85 Installed Power | 190 kW |
| MT85 Power Consumption | 140 kW |
| MT85 Capacity | 300–400 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| MT85 Overall Dimensions | 43 × 1.5 × 3.2 m |
| MT75 Installed Power | 210 kW |
| MT75 Power Consumption | 150 kW |
| MT75 Capacity | 300–500 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| MT75 Overall Dimensions | 45 × 1.5 × 3.5 m |
| Flaking Roller Drive | Hydraulic system with dual independent motors |
| Flaking Temperature Control | Infrared sensor for even temperature monitoring |
| Dryer Heating Source | Gas or electric (configurable to site utility) |
| Hot Air Roasting Oven | Vibrating pan, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Control System | PLC |
| Key Features | Automatic screw lubrication and cooling, wear-resistant screw construction, food-grade contact materials |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour at controlled moisture |
| Sugar-coated breakfast cereals | Corn, rice, or multi-grain base with sugar or honey coating |
| Multi-grain flake formats | Blends of wheat, oat, barley, and rice powder |
| Shaped cereal pieces | Ball, tube, ring, star, fruit loop, wheel, and heart profiles via die exchange |
| Fortified cereal lines | Grain base with added vitamin and mineral premix |
Why Nominal Capacity Fails When the Grain Blend Changes
A corn flakes extrusion production line technology rated on pure corn grits may not hold that throughput on a high-fibre multi-grain blend without screw and die reconfiguration.
I once watched a line stall on a customer’s proprietary high-fibre杂粮 formulation because the extruder was set up for standard corn meal. The flakes came out dense and hard, nothing like the target bowl-crisp texture. We spent two nights adjusting barrel temperature zones and feed moisture before the product finally met spec [NEED_CITE: starch gelatinisation behaviour in high-fibre grain matrices]. The lesson was that corn flakes extrusion production line technology must be validated against the actual grain blend, not a generic reference material. When fibre content, particle size, or fat ratio shifts, the screw element arrangement and die geometry need to follow.
Barrel Temperature Profiling and Starch Gelatinisation
Achieving the correct degree of starch gelatinisation inside the barrel is what separates a flake that blisters properly in the roasting oven from one that stays flat and tough. The corn flakes extrusion production line technology relies on a sequence of heating zones along the barrel, each tuned to the thermal behaviour of the specific grain being processed. Corn requires a different ramp than oat-heavy blends because the gelatinisation onset temperature and moisture absorption rate differ. PLC control allows operators to store and recall temperature profiles for each formulation, reducing changeover variability between production runs.
Die Geometry and Flake Expansion Behaviour
The die opening determines the cross-section of the extrudate rope before it enters the flaking rollers, and its shape directly influences how the material compresses and expands. Round, slotted, and shaped dies produce different internal cell structures that respond differently to flaking pressure and roasting heat. For shaped cereals like rings or fruit loops, the die geometry must coordinate with the cutting system to maintain dimensional consistency [NEED_CITE: die design principles for direct-expanded cereal products]. A mismatch between die profile and target flake thickness leads to uneven density across the batch, which the roasting oven cannot correct downstream.
Reading the Specs Beyond the Nameplate
The installed power figures — 160 kW for the MT70, 190 kW for the MT85, and 210 kW for the MT75 — indicate the thermal and mechanical headroom available for processing different grain viscosities. Higher installed power allows the screws to maintain RPM under the increased shear resistance of dense multi-grain blends. The hydraulic flaking station with independent dual motors lets each roller adjust separately, which matters when the extrudate rope has slight temperature variation across its width. Infrared temperature monitoring on the flaking rollers prevents the common failure mode where one side of the flake sheet is over-compressed while the other remains too thick. The hot air roasting oven uses a conciliation burner with dual circulating fans and cyclone dust removal, which keeps surface blistering uniform and prevents fine particulate from scorching inside the chamber.
The Cost of Skipping Screw and Die Matching
When screw elements are chosen from a generic build rather than matched to the buyer’s formulation, the extruder may run but the product density falls outside the specification the market expects. Floating versus sinking kibble is an extreme example, but even within corn flakes, a density variance of a few percentage points changes how the flake sits in milk and how long it stays crisp [NEED_CITE: cereal density testing standards for bowl-life performance]. Flakes that absorb moisture too quickly are rejected by retailers, and the entire production run may need to be diverted to secondary channels. The root cause is almost always a screw configuration that was never tested against the buyer’s actual raw material before the line shipped.
Why Procurement Through This Engineering Lens Matters
Screw configuration and die design are specified to the buyer’s raw material formulation and target flake density rather than pulled from a standard template. The in-house testing workshop runs trial batches on the customer’s actual grain blend before shipment, so gelatinisation degree, flake thickness, and roasting response are verified ahead of installation. Every station — mixing, extrusion, flaking, drying, roasting, coating — is throughput-matched within the same line build, eliminating the bottleneck that occurs when stations are sourced from separate vendors. Electrical schematics include voltage and frequency confirmation for the destination market, and PLC programming accommodates the local operator language. Documentation covers the full chain from line layout and capacity calculation through screw configuration records and factory test reports.
Documentation & Verification
- Line layout drawing with throughput calculation across all stations from mixer to packer
- Screw element layout and die geometry record matched to your grain formulation
- Trial run report on your raw material conducted in the testing workshop
- Electrical schematic with confirmed voltage, frequency, and control language
- CE declaration of conformity and ISO certificate for the complete line
Installation, Commissioning & Support
- Foundation plan reflecting MT75 dimensions of 45 × 1.5 × 3.5 m and total line footprint
- Dedicated circuit sizing based on confirmed installed power and start-up inrush requirements
- PLC parameter library loaded with temperature profiles for each of your grain formulations
- Flaking roller gap and hydraulic pressure calibrated on-site during first production run
- Operator training covering screw element changeover and die replacement procedures
- Wear parts inventory list for screws, dies, and flaking roller surfaces with lead times
What to Include in Your Enquiry
Share your target grain formulation, including the ratio of corn, rice, wheat, oat, or barley and any added fibre or protein ingredients. Specify the flake dimensions and density range your market requires, along with the daily output target so we can match the correct model. Confirm the local voltage, frequency, and preferred control language, and indicate whether you need natural, sugar-coated, or both product variants from the same line.
Frequently Asked Questions
Q: How are screw elements and die geometry chosen for a specific grain blend?
A: The screw element arrangement — conveying, kneading, and shearing sections — is configured based on the starch content, fibre level, and particle size of your grain mix. Die opening shape and land length are then selected to produce the correct extrudate density before flaking. A trial run in the testing workshop validates the configuration on your actual raw material before the extruder ships.
Q: What barrel temperature and moisture conditions are needed for proper gelatinisation?
A: Each barrel zone is set independently through the PLC to create a temperature ramp that matches the gelatinisation onset of your specific grain. Feed moisture is typically adjusted at the mixer stage. Corn-based formulations require a different profile than oat or barley-heavy blends, and both are stored as recallable recipes in the control system.
Q: How is line capacity confirmed before the equipment leaves the factory?
A: A trial production run is conducted in the in-house testing workshop using the buyer’s raw material formulation. Output rate, flake thickness, and product density are measured and documented. The resulting trial run report accompanies the shipment so you have verified performance data before installation begins.
Q: What role does the hot air roasting stage play in final product quality?
A: The roasting oven reduces moisture to the target level for bowl crispness and creates the characteristic surface blister pattern on the flake. The conciliation burner and dual circulating fans ensure even heat distribution, while the cyclone dust removal prevents fine particles from burning inside the chamber and affecting flavour.
Q: How is flake thickness kept uniform during long production runs?
A: The hydraulic flaking station uses independent dual motors for each roller, allowing separate pressure adjustment. An infrared sensor continuously monitors roller surface temperature, which directly affects how the extrudate compresses. The PLC logs these parameters so operators can detect drift and correct it before thickness moves outside specification.