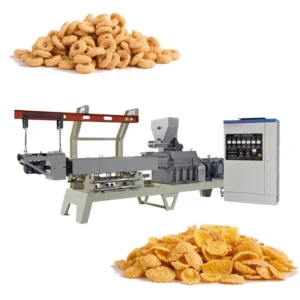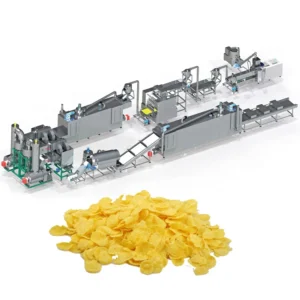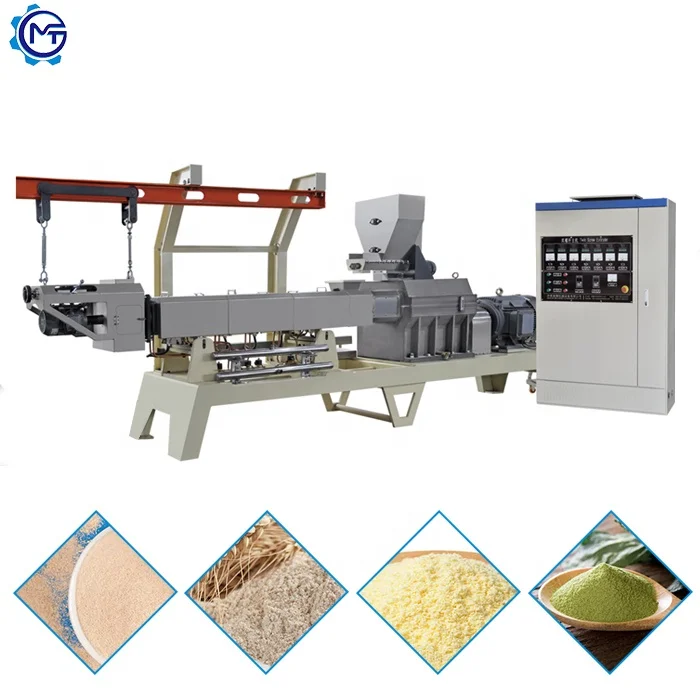
Matched Screw Geometry — every barrel zone and die insert is specified against the buyer’s actual corn grits formulation, not copied from a generic build.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Processing Line |
| Model | MT70 / MT75 / MT85 |
| Screw Type | Twin Screw |
| Installed Power | MT70: 160 kW; MT75: 210 kW; MT85: 190 kW |
| Power Consumption | MT70: 120 kW; MT75: 150 kW; MT85: 140 kW |
| Output Capacity | MT70: 150–200 kg/h (basis not stated in source); MT75: 300–500 kg/h (basis not stated in source); MT85: 300–400 kg/h (basis not stated in source) |
| Overall Dimensions | MT70: 41 × 1.5 × 2.2 m; MT75: 45 × 1.5 × 3.5 m; MT85: 43 × 1.5 × 3.2 m |
| Control System | PLC with automatic lubrication and cooling |
| Heating Source (Dryer / Roaster) | Gas or Electric |
| Flaking Station | Hydraulic double-roller, independent dual motors, infrared temperature pipe |
| Hot Air Roasting Oven | Vibrating pan, conciliation burner, dual circulating fans, cyclone dust removal |
| Voltage & Frequency | Configurable (e.g. 415 V 50/60 Hz, 440 V 50/60 Hz, 220 V 60 Hz) |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Degerminated corn grits, maize flour |
| Sugar-coated corn flakes | Corn grits with sugar spraying and coating drum |
| Multi-grain breakfast cereals | Rice, wheat, oat, barley powder blends |
| Shaped cereal formats | Ball, tube, ring, star, wheel, flower, heart via die change |
| Instant porridge base | Pre-gelatinised cereal powder for nutritional or infant formula |
Why Nominal Throughput Rarely Survives Contact with Real Corn Grits
Starch gelatinisation is governed by the interaction of screw profile, barrel heat and moisture — not by nameplate motor size.
A corn flakes extrusion production line technology rated at a certain hourly output on standard maize flour can behave entirely differently when the buyer switches to coarser degerminated grits with a different lipid residue. Particle size alters residence time inside the barrel, which shifts the gelatinisation window and changes how the dough sheet behaves at the flaking rolls. I have watched lines that performed flawlessly in the workshop produce fragile, uneven flakes on the customer’s first production day because the screw configuration had never been adjusted for the actual raw material [NEED_CITE: raw material variability in twin-screw extrusion].
How Screw Elements Dictate Flake Density and Blister Formation
The L:D ratio and the sequence of conveying, kneading and reverse-flight elements determine how much mechanical shear the corn dough receives before it exits the die. Higher shear promotes complete starch gelatinisation, which in turn governs how uniformly the pellet expands once it is flattened and toasted. On this corn flakes extrusion production line technology, the screw configuration is rebuilt for each buyer’s formulation so that the gelatinisation curve matches the target flake density.
Barrel Temperature Zones and Moisture Injection Points
Each barrel section has independent heating and cooling circuits. The operator sets a gradient that typically rises through the melting zone and stabilises before the die. Moisture is injected at defined ports; too much water too early causes premature flash-off and leaves the pellet under-cooked at the core, while too little results in a brittle sheet that shatters under the flaking rolls [NEED_CITE: barrel temperature profiling in cereal extrusion]. Balancing these two variables is where process experience matters more than installed kilowatt rating.
Reading the Spec Sheet Like a Process Engineer
Installed power tells you what the motors can deliver, not what the product receives. The MT75 model, for instance, carries a higher motor rating than the MT85, yet its throughput range overlaps — the difference lies in screw diameter and free volume inside the barrel, which together define residence time. A longer residence time allows lower barrel temperatures to achieve the same degree of cook, useful when working with heat-sensitive oat or barley blends. The hydraulic flaking station uses an infrared-controlled temperature pipe to keep the roller surface within a narrow band, preventing the dough sheet from sticking or tearing as thickness is reduced to the target gauge.
The Hidden Cost of a Generic Die and Screw Build
When an extruder ships with a one-size-fits-all screw profile, the first sign of trouble is usually flake thickness variation. Thin spots toast too fast and burn; thick spots stay soft and pack with excess moisture. Downstream, the roaster cannot compensate, so the packing station receives a mix of over-dried and under-dried product. Line stoppages for manual sorting become routine, and buyers blame the roaster when the real fault sits inside the extrusion barrel [NEED_CITE: die design impact on cereal flake uniformity].
Why Process Engineering Matters at the Quotation Stage
Every station on the line — mixer, extruder, flaker, dryer, roaster, coater — is matched for throughput so that no single unit bottlenecks the next. Screw and die geometry is documented against the buyer’s specific grain blend, not pulled from a catalogue default. Before dispatch, the line runs a trial on the buyer’s actual raw material inside the testing workshop, generating a report that records real barrel temperatures, moisture levels and flake density. Electrical schematics confirm voltage, frequency and PLC language for the destination market, avoiding commissioning delays caused by mismatched panels.
Documentation & Verification
- Trial run report on buyer’s corn grits recording gelatinisation degree and flake density
- Screw and die configuration sheet matched to the specified grain formulation
- Electrical schematic confirming voltage, frequency and PLC interface language
- Line layout with throughput balance across extruder, flaker, dryer and roaster
- CE declaration of conformity and ISO certificate for the complete processing line
Installation, Commissioning & Support
- Foundation plan scaled to the MT75 line length of up to 45 m including roaster
- Dedicated electrical circuit sized for 210 kW installed load with confirmed voltage
- PLC parameter set uploaded on-site to match the trial-run screw profile
- Operator training covering barrel zone tuning and hydraulic flaker pressure adjustment
- Wear-parts list specifying screw elements, die inserts and flaker roller sleeves
What to Include in a Technical Inquiry
Provide the particle size distribution and moisture content of your corn grits or alternative grain blend, along with the target flake thickness and final pack density. Confirm the local voltage and frequency standard, the PLC language preference, and whether the line must switch between natural and sugar-coated variants within a single shift.
Frequently Asked Questions
Q: How is output capacity verified against my specific corn grits formulation?
A: We run your raw material in the testing workshop before shipment, recording barrel temperatures, moisture injection rates and flake density. The resulting trial report becomes the baseline for your commissioning parameters, so the capacity figure you see on-site reflects your actual grain rather than a generic maize flour benchmark.
Q: What screw and die configuration do you recommend for a rice-oat-barley blend?
A: Alternative grains gelatinise at different temperatures and absorb moisture at different rates. We adjust the kneading-block sequence, reverse-flight positions and die orifice diameter to match the blend’s starch profile. The configuration record ships with the line and is referenced during operator training.
Q: Can the line produce both natural and sugar-coated flakes on the same day?
A: Yes. The sugar-coating variant adds a spraying and tumbling station between roasting and final cooling. Changeover involves flushing the coating drum, adjusting nozzle flow rate and updating the PLC recipe. No mechanical rebuild is required, keeping downtime proportional to standard cleaning intervals.
Q: How do flake thickness and roasting profile affect milk-bowl behaviour?
A: Thinner flakes toast faster and yield a crisper texture with higher milk absorption; thicker flakes retain more bite. The hydraulic flaker holds thickness within a tight band, while the dual-fan roaster with conciliation burner controls surface blister formation and final moisture, giving you repeatable bowl-life characteristics across batches.
Q: What happens if my local voltage differs from the standard options listed?
A: Voltage and frequency are confirmed during the quotation stage and written into the electrical schematic. Motor windings, heating elements and PLC power supplies are specified to your grid standard, so the control cabinet arrives ready for connection without on-site transformer swaps or phase-converter add-ons.