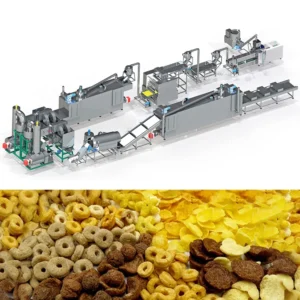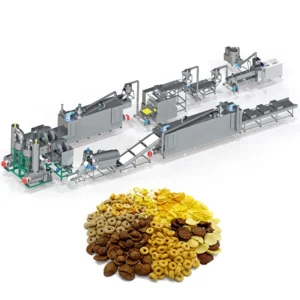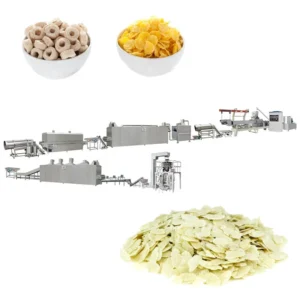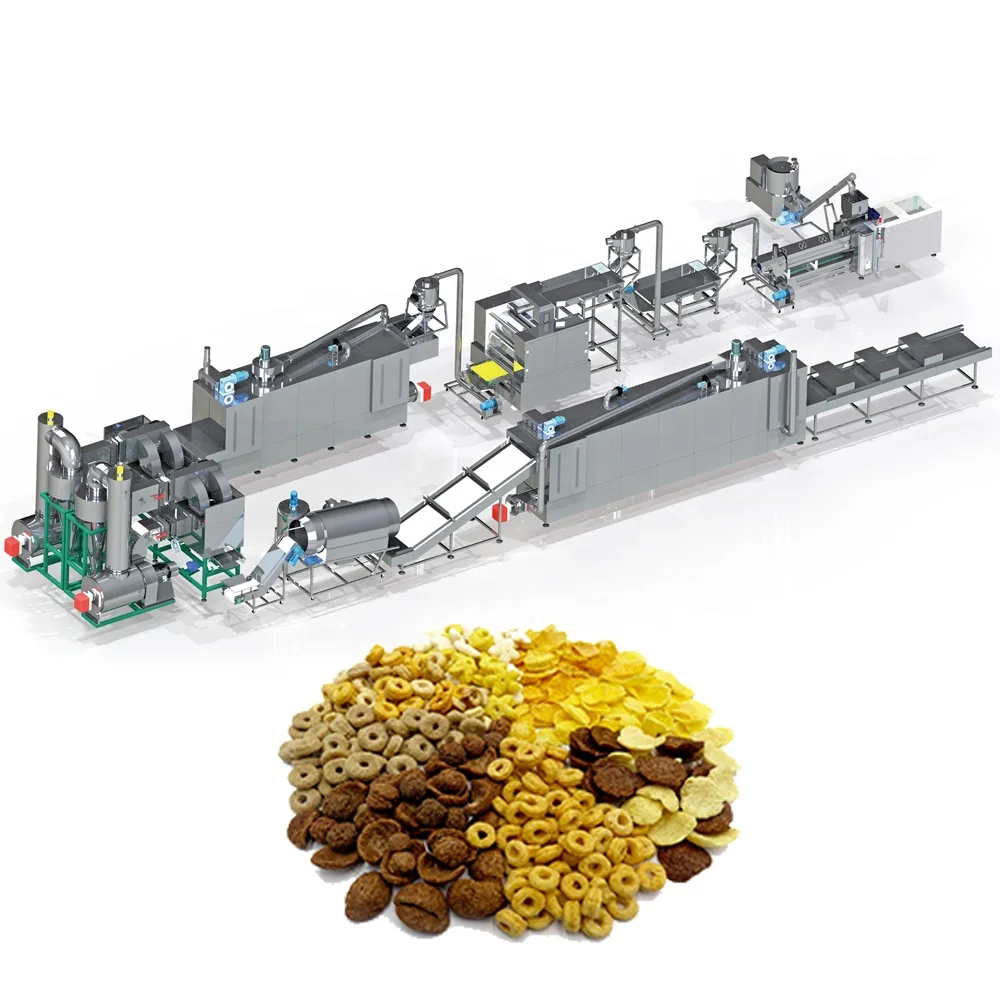
Precision Screw Profiling — every MT70 / MT85 / MT75 barrel zone and die land length is matched to the buyer’s grain base and target flake density before the machine leaves the factory.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Breakfast Cereal Processing Line |
| Model Options | MT70 / MT85 / MT75 |
| Installed Power | 160 kW (MT70) / 190 kW (MT85) / 210 kW (MT75) |
| Power Consumption | 120 kW (MT70) / 140 kW (MT85) / 150 kW (MT75) |
| Output Capacity | 150–200 kg/hr (MT70, basis not stated in source) / 300–400 kg/hr (MT85, basis not stated in source) / 300–500 kg/hr (MT75, basis not stated in source) |
| Overall Dimensions (L×W×H) | 41 × 1.5 × 2.2 m (MT70) / 43 × 1.5 × 3.2 m (MT85) / 45 × 1.5 × 3.5 m (MT75) |
| Screw Type | Twin Screw |
| Control System | PLC and MCC control |
| Flaking Machine | Hydraulic double-roller, dual motor drive, infrared sensor temperature control |
| Dryer Heating Source | Gas / Electric (configurable) |
| Roasting Oven | Hot air with conciliation burner, dual circulating fans, cyclone dust removal, vibrating pan |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Basic Raw Materials | Corn, rice, wheat, oat, barley powder |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits or corn flour, dried and roasted without coating |
| Sugar-coated breakfast cereal | Corn, rice, or wheat base with sugar or honey glaze applied post-roast |
| Multi-grain flaked cereal | Blends of oat, barley, and rice flour requiring adjusted screw profile |
| Puffed cereal shapes | Ball, tube, ring, star, wheel, flower, heart via die exchange |
| Small-scale market entry | Producers validating corn flake format before committing to high-capacity lines |
Why "Rated Capacity" Means Nothing Without the Grain Specification
A 300 kg/hr rating on standard maize grits tells you nothing about throughput on high-fiber local corn.
Every time I arrive at a site in Lagos or Colombo, the first thing I check is what grain the buyer actually stocks. Corn flakes extrusion technology twin screw configurations behave completely differently when starch content drops or fiber rises. The extruder may run, but the flakes emerge dense, refuse to blister in the roasting oven, and shatter in the bowl instead of holding their crunch. I have spent entire weeks rebuilding screw elements and rewriting barrel temperature curves because the trial back at the factory used a different maize variety [NEED_CITE: raw material variability in African and South Asian grain supply chains]. Capacity numbers only become real once the screw profile, moisture window, and die geometry are locked to the specific grain the line will actually process.
Starch Gelatinisation and the Barrel Temperature Curve
Proper corn flakes extrusion technology twin screw performance depends on a controlled gelatinisation window. The barrel is divided into feeding, compression, and metering zones, each with independent heating. Corn starch gelatinises between specific temperature thresholds, and the screw elements must generate enough shear to rupture granules without scorching the melt. If the compression zone runs too cool, the dough passes the die under-gelatinised and the flakes will not expand during roasting. Too hot, and the sugars caramelise inside the barrel, fouling the screw flights and forcing unplanned shutdowns for cleaning.
Moisture, Shear, and Expansion Before the Flaking Rolls
Moisture content at the feed inlet governs how the dough behaves between the die face and the flaking rolls. The twin-screw design allows operators to inject steam or water at precise barrel zones, adjusting the shear rate and residence time simultaneously. Higher moisture lowers viscosity, reducing mechanical energy input and producing a softer pellet that flattens evenly under the hydraulic rollers. Lower moisture increases shear, generating more internal steam at the die — useful when the roasting oven needs pellets with enough trapped moisture to blister on their surface. The hydraulic flaking machine with infrared temperature control then compresses these pellets to a uniform thickness, which is where corn flakes extrusion technology twin screw engineering either pays off or falls apart [NEED_CITE: relationship between extrudate moisture and flake blistering in hot air roasting].
Reading the Spec Sheet Against Your Actual Production Goals
The installed power difference across models — 160 kW, 190 kW, 210 kW — reflects the mechanical energy available for shear and conveying. A higher-power twin-screw extruder handles denser dough formulations with less screw wear and maintains throughput when processing high-fiber grains that resist compression. The flaking machine’s hydraulic double-roller system with separate motor drives ensures each roller can be adjusted independently, compensating for uneven feed distribution. PLC control over the entire line — from batching through the roasting oven’s dual circulating fans — means barrel temperature, flaking pressure, and roasting airflow respond to a single control logic rather than operating as disconnected islands. Gas or electric dryer options accommodate local utility costs and availability, which varies significantly across South Asian and African markets [NEED_CITE: industrial energy cost comparison for food processing in developing markets].
The Hidden Cost of a Generic Screw Build
I once commissioned a corn flakes line where the factory had shipped a standard screw configuration designed for low-fiber yellow maize. The buyer’s grain was a local white corn variety with noticeably higher bran content. The flakes came off the flaking rolls thin but brittle — they cracked during conveying and arrived at the packing station as fragments rather than intact flakes. The roasting oven could not compensate because the pellets entering it lacked the internal structure needed for surface blistering. We replaced six screw elements and adjusted three die land lengths to recover acceptable output, and the buyer lost an entire production week [NEED_CITE: screw configuration impact on flake integrity during downstream processing].
Engineering Decisions Backed by Workshop Trials
Complete line throughput is balanced station by station — the extruder output is matched to the flaking machine capacity, the dryer residence time, and the roasting oven airflow so no single station bottlenecks the next. Screw configuration and die geometry are specified to the buyer’s submitted raw material, not copied from a reference build. The in-house testing workshop runs the buyer’s actual grain before the machine ships, producing a trial report that locks in screw arrangement, barrel temperatures, and moisture targets. PLC and MCC control panels are configured to the buyer’s local voltage, frequency, and preferred operator language before dispatch. Twin-screw expertise spans corn, rice, wheat, oat, and barley bases, meaning a producer switching grains does not need a new extruder — only a reconfigured screw set and updated process parameters.
Documentation & Verification
- Line layout with throughput calculation across extruder, flaker, dryer, and roasting oven
- Screw and die configuration record matched to your grain sample and target flake density
- Trial run report on your raw material conducted in the testing workshop before shipment
- Electrical schematic confirming voltage, frequency, and control language for your facility
- Operation and maintenance manual with wear parts list and replacement intervals
- CE declaration of conformity and ISO certificate for import and compliance filing
Installation, Commissioning & Support
- Foundation and floor space planned around the 41–45 m line length and 2.2–3.5 m height clearance
- Dedicated electrical circuits sized to the 120–150 kW operating draw with voltage confirmed pre-shipment
- Extruder barrel zones, flaking rolls, and roasting oven commissioned sequentially with process parameter logging
- PLC interface language and alarm labels configured to operator preference before installation begins
- Twin-screw elements and die plates inventoried with a wear parts list for first replacement planning
- Routine maintenance schedule covering screw clearance checks, hydraulic fluid intervals, and burner calibration
What We Need to Move Forward
Share your grain type and any available analysis — starch percentage, fiber content, moisture at delivery — along with the flake thickness and bowl-life crunch your market expects. Confirm your facility voltage and frequency, and whether gas or electric heating suits your energy costs. If you have existing mixing or packing equipment, note the throughput so the line can be matched to those stations.
Frequently Asked Questions
Q: How is screw configuration selected for different grain bases like corn versus oat?
A: Each grain has a distinct starch gelatinisation temperature and fiber behaviour under shear. The screw element arrangement — conveying, kneading, and reverse elements — is designed around lab analysis of your specific grain, adjusting compression ratio and residence time to achieve target pellet density before flaking.
Q: What barrel moisture level is needed for proper corn flake expansion?
A: Moisture is typically conditioned at the feed inlet and adjusted via steam injection at mid-barrel zones. The exact level depends on grain starch content and the blistering behaviour your roasting oven requires — too low and pellets shatter, too high and flakes turn leathery instead of crisp.
Q: Can a trial run be performed on our specific raw material before shipment?
A: Yes. The testing workshop processes your submitted grain through the configured extruder, flaker, and roasting oven. The resulting trial report documents screw arrangement, barrel temperatures, and flake density so the line arrives with parameters already set.
Q: How is throughput balanced between the extruder and the roasting oven?
A: Each station — extruder, flaking machine, dryer, roasting oven — is sized so that residence time and capacity match. The roasting oven’s dual circulating fans and vibrating pan are specified to handle the extruder’s output without creating a backlog or under-drying the flakes.
Q: What control options are available for consistent batch-to-batch quality?
A: PLC and MCC control govern barrel temperature zones, flaking roller pressure, and roasting airflow from a single interface. The system logs process parameters per batch, allowing operators to recall proven settings when switching between grain types or flake thickness targets.