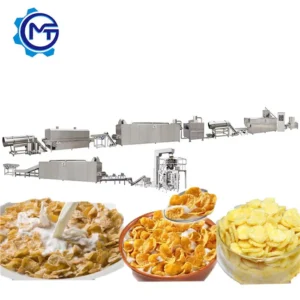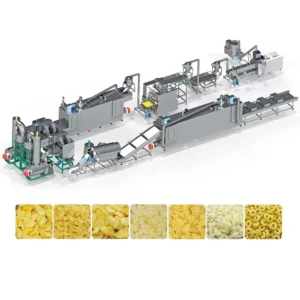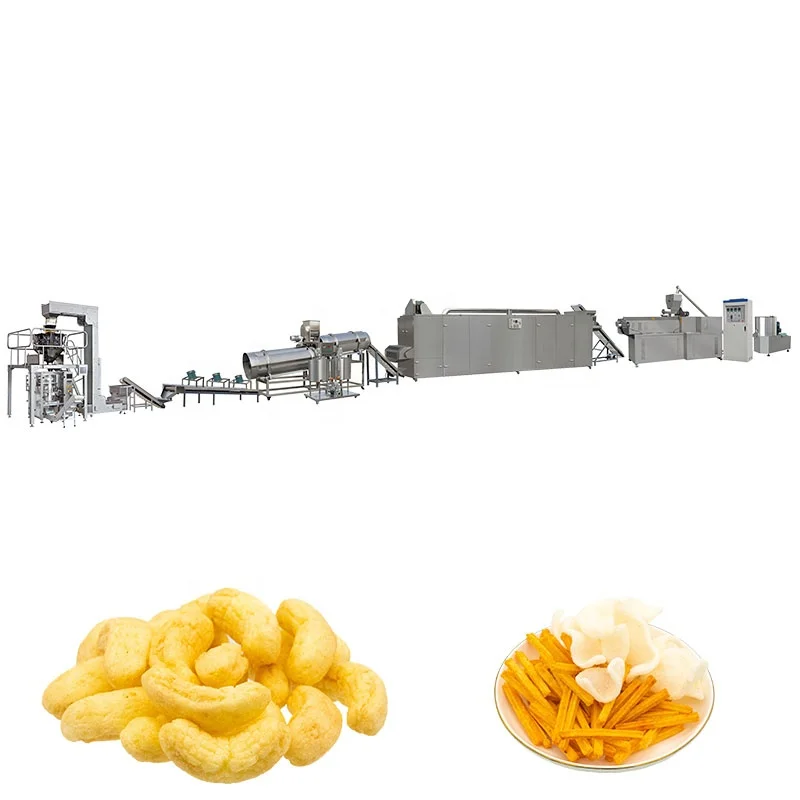
Screw configuration matched to your grain blend — We calibrate every barrel zone and die geometry to your exact corn, rice, or oat formulation so the corn flakes extrusion technology actually performs on your recipe, not just on ours.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-75 Twin Screw Extruder |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin-screw |
| Output Capacity | 200-300 kg/hr (basis not stated in source — confirm raw material / moisture content / flake thickness) |
| Control System | PLC control for flaking machine; MCC for line |
| Heating Source | Gas or Electric (dryer) |
| Flaking Drive | Double motors, separate roller driving; hydraulic system |
| Flaking Temperature Control | Infrared sensor for even temperature pipe control |
| Roasting Oven | Hot air roasting, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, precision spray nozzle |
| Assembly State | Complete production line |
| Warranty | 1 Year |
| Certification | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Traditional corn flakes | Corn grits, maize flour |
| Multigrain breakfast flakes | Rice, wheat, oat, barley blends |
| Sugar-coated cereal flakes | Corn or mixed grain base with sucrose or maltose glazing |
| Fortified breakfast cereals | Grain matrix with added vitamin or mineral premix |
What "200-300 kg/hr" Leaves Out About Corn Flake Density
A twin-screw corn flakes production line only hits its nameplate output when the screw profile, barrel zones, and raw material moisture align precisely.
I once watched a corn flakes extrusion technology line stall mid-run because a client’s high-sugar recipe made the dough tack up inside the die. The rated capacity meant nothing when the material behaviour changed [NEED_CITE: starch gelatinisation thresholds under high-sugar formulations]. Throughput claims without material context lead to lines that run well during factory tests on standard grits but choke the moment your actual grain blend hits the barrel.
Barrel Temperature Zones and Starch Gelatinisation
Each zone along the twin-screw barrel governs a different phase of the corn flakes extrusion technology process — from initial hydration through starch gelatinisation to final dough conditioning before the die. If the first zones run too hot, moisture flashes off prematurely and the gelatinisation front stalls. Too cool in the later zones, and the dough exits undercooked, producing flakes that shatter rather than crisp during roasting.
Die Geometry and Flake Integrity
The die orifice shape and land length determine how the cooked dough strand releases and cools. A die cut too short lets the dough expand unpredictably, creating uneven half-products that flake into irregular thicknesses. Our die designs are specified to the buyer’s target flake dimension and raw material viscosity, so the strand exiting the die holds a consistent cross-section all the way to the flaking rollers [NEED_CITE: die land length effects on extrudate dimensional stability].
Hydraulic Flaking Rollers and Thickness Uniformity
The flaking station uses hydraulic pressure on double rollers, each driven by its own motor, to compress the half-product into a uniform sheet. The infrared sensor monitors temperature across the roller face in real time. If one side runs hotter, the dough softens unevenly and flakes emerge thicker on one edge — which then roast inconsistently and pack with different bulk densities, causing fill-weight drift at the packing station.
Hot Air Roasting and Surface Blistering
The roasting oven uses a conciliation burner with two separate circulating fans and a cyclone dust removal device. Controlled surface blistering gives corn flakes their characteristic toasted appearance and final crispness. Insufficient air circulation leaves the centre of the tray under-roasted while the edges scorch, directly affecting bowl life — the duration a flake stays crisp after milk is poured [NEED_CITE: hot air circulation uniformity in cereal roasting ovens].
When a Generic Build Becomes a Bottleneck
A flaking machine rated for a certain throughput means nothing if the upstream extruder cannot feed it continuously, or if the downstream dryer lacks the residence time to handle the moisture load. Lines assembled from mismatched stations create choke points that no single machine specification can reveal. The result is a line that technically meets every individual spec sheet yet never reaches a stable running rhythm during actual production.
Why Procurement Starts With Your Material, Not a Catalogue
Every screw configuration and die design is specified against the buyer’s raw material blend and target flake specification, not pulled from a generic template. An in-house testing workshop runs trial batches on the customer’s actual grain formulation before shipment, so the trial run report documents real flake density, texture, and gelatinisation degree on your recipe. Electrical schematics are confirmed for voltage and frequency at the installation site, preventing commissioning delays. Line layout and capacity calculations show throughput matching across the extruder, flaker, dryer, and roaster — not just isolated machine ratings. The twin-screw corn flakes production line ships as a coordinated system, not a collection of standalone units [NEED_CITE: CE machinery directive documentation requirements for food processing lines].
Documentation & Verification
- Screw and die configuration record matched to your grain blend and target flake density
- Trial run report on your raw material documenting gelatinisation, expansion, and texture
- Electrical schematic with voltage, frequency, and control language confirmed for your market
- Line layout and capacity calculation showing matched throughput at every station
- Machinery test report and video outgoing inspection provided before dispatch
Installation, Commissioning & Support
- Floor plan and utility routing based on the MT-75 footprint and MCC panel placement
- Power circuit sized for the twin-screw main drive and electric or gas dryer heating source
- Assembly sequence for the flaking rollers, roasting oven, and coating drum on-site
- First-run parameter log covering barrel zones, hydraulic pressure, and roasting temperature
- Operator training on PLC interface for the flaking station and MCC line controls
- Wear parts list covering screws, dies, and roller surfaces with reorder intervals
Before You Request a Quotation
Share your grain formulation — corn, rice, wheat, oat, or barley percentages — along with target flake thickness and whether sugar coating is required. Specify your local voltage and frequency so the electrical schematic matches your facility from day one. If you have existing upstream mixing or downstream packing equipment, provide model details so the line layout accounts for integration points.
Frequently Asked Questions
Q: How is screw configuration matched to specific grain blends for corn flakes?
A: We select screw element sequence, compression ratio, and die land length based on the starch content, protein level, and fibre percentage of your grain blend. The configuration is documented in a screw and die record that ships with the line, and a trial run on your material validates gelatinisation and expansion before dispatch.
Q: What trial runs are conducted before shipment?
A: Your raw material is run through the MT-75 in our testing workshop. The trial run report records barrel temperatures, screw speed, moisture content, flake density, and visual texture. You receive this report alongside video inspection footage so you can verify performance on your exact recipe before the line is crated.
Q: How are voltage and control language confirmed for the installation site?
A: During the specification confirmation stage we collect your local voltage, frequency, and preferred control language. The electrical schematic is then finalised so the MCC panel and PLC interface match your facility standards, avoiding rewiring or reprogramming during on-site commissioning.
Q: How is throughput balanced between extruder, flaker, and roaster?
A: Line layout and capacity calculation documents show the mass flow at each station based on your target moisture reduction and flake thickness. The extruder output, flaking roller speed, dryer residence time, and roasting oven belt speed are all cross-checked so no single station becomes a bottleneck during continuous production.