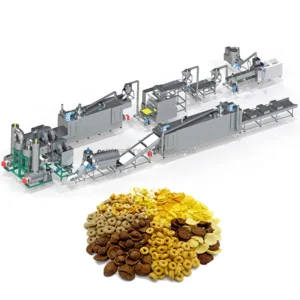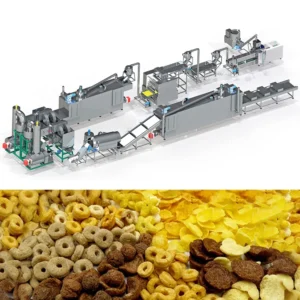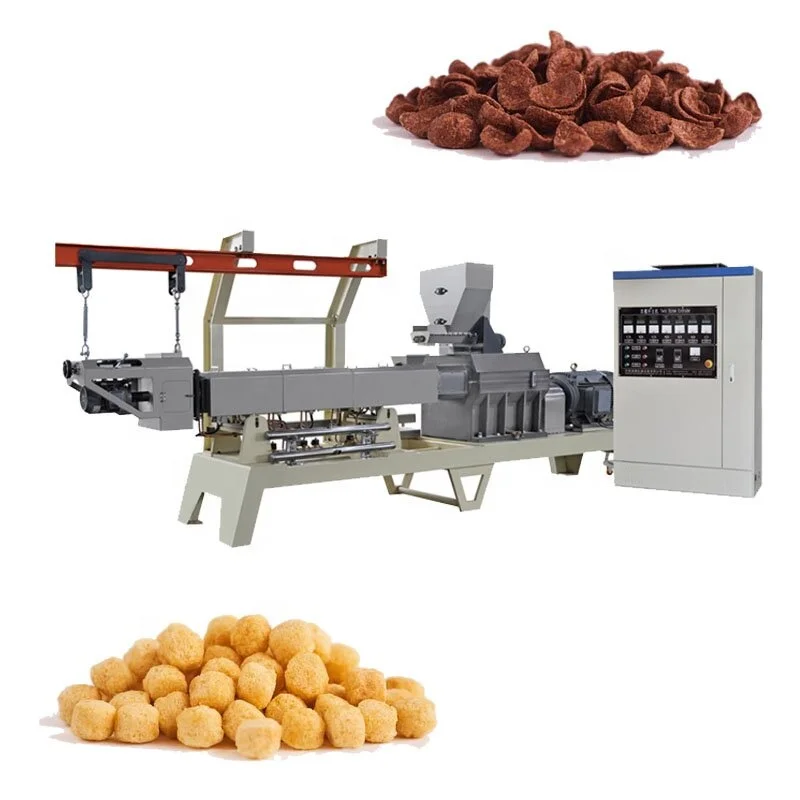
Screw Configuration Matched to Raw Material — Every MT series corn flakes line ships with a documented screw and die setup tuned to the buyer’s specific cereal blend, validated through an in-house trial run before dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin Screw |
| Installed Power | 160 kW (MT70) / 190 kW (MT85) / 210 kW (MT75) |
| Power Consumption | 120 kW (MT70) / 140 kW (MT85) / 150 kW (MT75) |
| Capacity | 150–200 kg/h (MT70, basis to be confirmed) / 300–400 kg/h (MT85, basis to be confirmed) / 300–500 kg/h (MT75, basis to be confirmed) |
| Overall Dimensions | 41 × 1.5 × 2.2 m (MT70) / 43 × 1.5 × 3.2 m (MT85) / 45 × 1.5 × 3.5 m (MT75) |
| Basic Material | Powder of corn, rice, wheat, oat, barley |
| Control System | PLC integrated with MCC across the line |
| Dryer Heating Source | Gas or Electric |
| Flaking System | Hydraulic double-roller, independent dual-motor drive, infrared temperature control |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn grits and corn flour with controlled gelatinisation |
| Sugar-coated corn flakes | Corn or multi-grain base with post-roasting syrup coating |
| Multi-grain breakfast flakes | Blends of rice, wheat, oat, and barley requiring screw reconfiguration |
| Shaped cereal formats | Rings, balls, tubes, sticks, stars, and loops via die changes |
What "Nominal Capacity" Leaves Out About Corn Flakes Lines
A throughput number without a raw material basis is not a capacity — it is a guess.
I have watched lines arrive at a factory floor, get wired up, and then fail to hold their quoted output because the local corn flour had a different particle size and starch profile than whatever the seller tested with. The extruder barrel could not deliver enough shear, expansion collapsed, and the flakes came off the roaster flat and dense. That mismatch between the corn flakes extrusion production line specifications on paper and the reality of a buyer’s actual cereal blend is where most breakfast cereal projects stall. The installed power and screw speed might be adequate on paper, but if the screw configuration was never matched to the grain composition you are actually buying, the line will never reach its intended throughput [NEED_CITE: starch gelatinisation behaviour across corn varieties and milling grades].
Barrel Temperature and Shear Control Across the Extrusion Zone
Starch gelatinisation in corn flakes demands a precise combination of moisture, barrel temperature, and mechanical shear inside the extruder barrel. The twin-screw configuration on the MT70, MT85, and MT75 allows operators to stage the corn flakes extrusion production line specifications across multiple heating zones, building the temperature profile gradually so the cereal mass cooks evenly before it reaches the die. Each model’s installed power — from 160 kW to 210 kW — provides the thermal headroom needed for sustained gelatinisation at production speed.
Die Design and Expansion Behaviour at the Cut-Off Point
The moment the cooked cereal mass exits the die, pressure drops instantly and moisture flashes off, driving expansion. Die geometry — orifice diameter, land length, and face pattern — determines whether the extrudate emerges as a dense half-pellet ready for flaking or an over-expanded shape that shatters under the rollers. Matching the die to the buyer’s target flake thickness and blister profile is a step that generic builds skip entirely [NEED_CITE: die land length influence on extrudate density in cereal processing].
Reading the Power and Throughput Data Correctly
Installed power and actual power consumption are different numbers, and the gap between them tells you how much thermal and mechanical reserve the extruder carries. The MT70 draws 120 kW against a 160 kW installation, while the MT75 pulls 150 kW from a 210 kW supply — that headroom matters when raw material moisture fluctuates and the barrel heaters must compensate mid-run. The throughput figures in the table above carry a note that the basis is to be confirmed: the actual capacity depends on the buyer’s cereal formulation, moisture content entering the extruder, and target flake density. Any supplier who quotes a flat number without asking for your recipe and particle size distribution is guessing.
When the Wrong Screw Combination Reaches Your Factory
If the screw elements are assembled in a generic sequence rather than configured for your specific corn or multi-grain blend, the consequences show up quickly. Under-gelatinised starch produces flakes that remain hard in the centre after roasting. Excessive shear from too many kneading blocks can over-cook the mass, causing it to stick to the flaking rollers and tear. Downstream, the dryer and roasting oven receive product that does not behave as designed — blistering is uneven, moisture removal stalls, and the final crunch profile misses the market specification [NEED_CITE: twin-screw element sequencing effects on cereal extrudate texture].
Why Procurement Should Start with the Extrusion Profile
Sourcing a corn flakes line from a single supplier who configures every station around the extrusion output prevents the most common failure mode: stations that do not match. The flaking machine, dryer, hot air roasting oven, and coating drum must all handle the volume and moisture profile the extruder actually produces — not a nominal number. Our in-house testing workshop runs your raw material through the extruder before the line ships, generating a trial run report that documents screw configuration, barrel temperatures, and product density so you know what to expect at commissioning. The PLC and MCC control system is programmed to your voltage and frequency, and the control language is set before crating.
Documentation & Verification
- Screw and die configuration record matched to your cereal formulation and target flake density
- Trial run report from in-house testing workshop using your actual raw material before shipment
- Line layout and capacity calculation showing throughput balance from extruder through roasting and packing
- Electrical schematic with voltage, frequency, and control language confirmed to your market
- CE declaration of conformity and ISO certificate included with shipping documentation
Installation, Commissioning & Support
- Foundation plan provided for line lengths up to 45 m, with load points at extruder and flaking stations
- Dedicated electrical circuits sized to the model’s installed power, up to 210 kW for the MT75
- PLC and MCC panels pre-wired and labelled in the confirmed control language before dispatch
- On-site commissioning includes screw configuration verification and barrel temperature profiling on your material
- Wear parts list covering screws, die inserts, and flaking roller surfaces with recommended replacement intervals
What We Need to Configure Your Line
To specify the correct screw arrangement, die set, and station sizing, we need your cereal formulation including grain types and particle size distribution, target flake density and blister profile, daily production volume, and your facility’s available floor length and ceiling height. Voltage, frequency, and preferred control language should be confirmed early so the MCC and PLC are built to match.
Frequently Asked Questions
Q: How is screw configuration and die design selected for different cereal raw materials?
A: The screw element sequence — conveying, kneading, and reverse elements — is arranged based on the starch content, particle size, and moisture behaviour of your specific cereal blend. Die orifice diameter and land length are then chosen to produce the expansion ratio your target flake requires. This configuration is documented and validated in a trial run before the line ships.
Q: What barrel temperature profile is needed for proper starch gelatinisation in corn versus multi-grain blends?
A: Corn typically requires a gradual temperature ramp across the barrel zones to fully gelatinise without surface burning, while oat or barley blends may need lower peak temperatures due to different starch and fibre compositions. The twin-screw extruder’s multiple heating zones allow each profile to be set independently and adjusted during commissioning.
Q: How is capacity verified on the buyer’s actual raw material before shipment?
A: We run your supplied raw material through the configured extruder in our in-house testing workshop and document throughput, expansion behaviour, moisture content at the die exit, and flake density. The trial run report accompanies the shipment so your team can compare commissioning results against a known baseline.
Q: How are moisture level and shear force controlled during extrusion to manage flake density?
A: Moisture is managed through preconditioning before the extruder and steam injection at the barrel, while shear force is controlled by the screw element arrangement and screw speed on the PLC. Together these determine the degree of starch gelatinisation and the expansion that occurs at the die, directly setting the density of the half-pellets entering the flaking rollers.