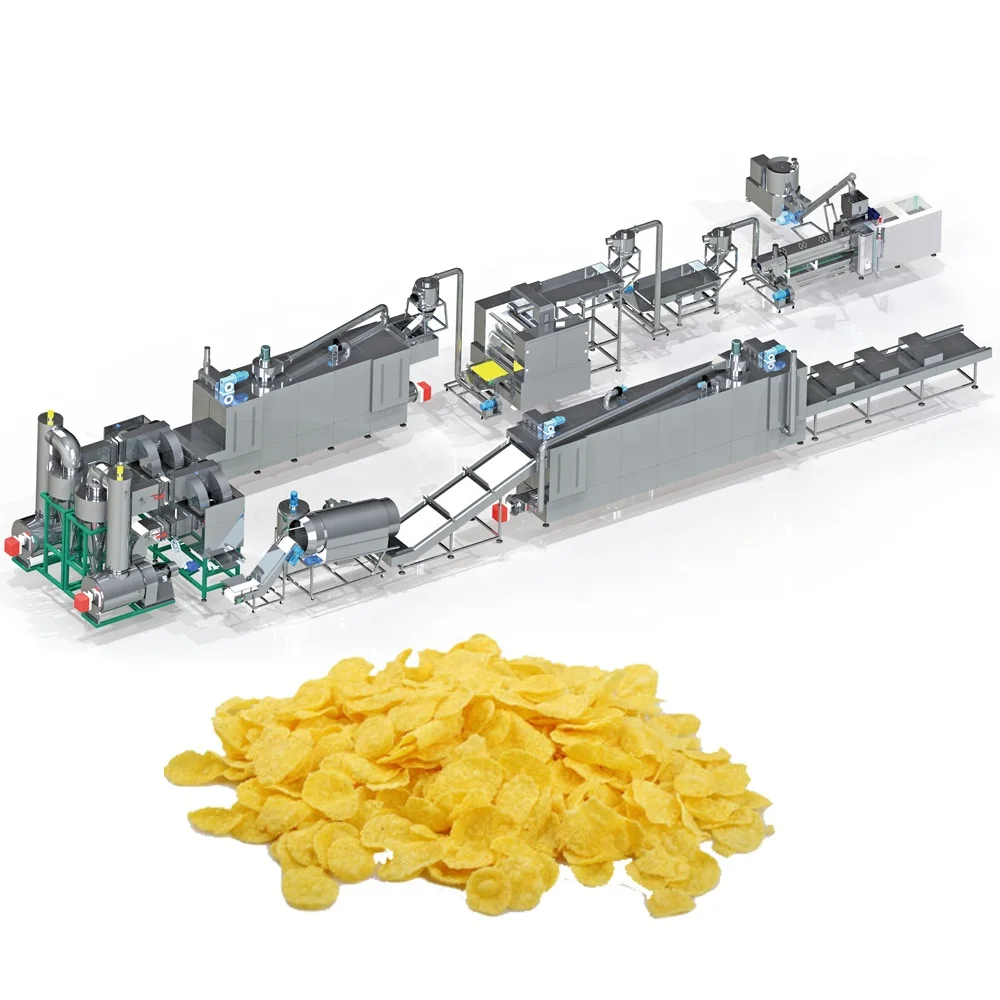
Extrusion Process Engineering — twin-screw configuration and barrel profile specified to the buyer’s grain formulation, ensuring controlled gelatinisation and target flake density from first run.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Output Capacity | Up to 750 kg/hr (basis not stated in source — confirm raw material, moisture content, flake thickness) |
| Screw Type | Twin-screw extrusion |
| Control System | Available with PLC or MCC control options |
| Product Range | Natural corn flakes, sugar-coated flakes, multi-grain breakfast cereals |
| Voltage & Frequency | Configurable per target market grid standard |
| Line Layout | Customizable to specific factory dimensions |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Degerminated corn grits, maize meal |
| Sugar-coated and frosted flakes | Corn base with syrup coating and drying stages |
| Multi-grain breakfast cereals | Blends of corn, wheat, rice, oat grits requiring gelatinisation and flaking |
| Fortified cereal products | Grain matrices with added vitamin and mineral premix |
When Corn Flakes Go Soggy Before Breakfast Is Over
Flake density and bowl-life crunch are decided inside the extruder barrel, not at the toaster.
The corn flakes extrusion technology that determines whether your product survives three minutes in cold milk comes down to how starch gelatinisation is managed across the barrel zones. I once set up a line for a Middle Eastern buyer who ordered against a sample capacity figure, then switched his raw material to include high-protein flour. The shear profile inside the barrel was wrong for that formulation, expansion collapsed, and the flakes came out dense and lifeless. The line stalled because throughput at every downstream station — flaking mill, toaster, coating drum — was calculated around a product geometry that never materialised [NEED_CITE: starch gelatinisation behaviour under varying protein content in twin-screw extrusion]. Generic screw builds copied from a standard corn grits setup will not protect you when your formulation drifts even slightly from the original assumption.
Barrel Zone Mapping for Controlled Gelatinisation
The barrel on a corn flakes line is divided into independently heated zones, each governing a different phase of starch conversion. Feed intake, compression, melting, and metering all demand different thermal inputs. Corn flakes extrusion technology depends on matching the temperature ramp to the specific corn variety’s gelatinisation onset temperature, which varies by starch composition and particle size distribution.
Moisture Injection and Steam Management
Pre-conditioning moisture and direct steam injection into the barrel determine how uniformly the starch granules swell before the material reaches the die. Too little moisture leaves ungelatinised cores that produce brittle, uneven flakes downstream. Too much creates a sticky melt that sheets poorly through the flaking mill and delivers a gummy bowl-life texture. The injection rate must track the corn meal’s initial moisture content at intake, which itself fluctuates with storage conditions and seasonal harvest variation [NEED_CITE: moisture content variability in stored cereal grains].
Reading the Specification Sheet Beyond the Headline Numbers
The screw L:D ratio dictates residence time inside the barrel, which directly controls the degree of starch conversion achievable at a given throughput. A ratio suited to highly refined corn grits may under-process a coarser, whole-grain formulation. The die orifice geometry upstream of the flaking mill determines pellet shape and size, which in turn governs how evenly the material sheets between the flaking rolls. Twin-screw configuration — the arrangement of conveying, kneading, and reverse elements along the shaft — sets the shear intensity the material experiences at each stage. Control system selection between PLC and MCC options affects whether barrel zone temperatures and screw speed can be logged and recipe-locked for batch-to-batch consistency across shift changes.
The Downstream Bottleneck Nobody Quoted For
When extrusion parameters produce a denser, under-expanded pellet, the flaking mill must work harder to achieve target flake thickness, and the toaster requires extended dwell time to drive off residual moisture. The coating drum then receives a product that absorbs syrup unevenly because the internal pore structure was never properly formed during extrusion. I have seen entire lines where the extruder ran within spec on paper, but the downstream stations were sized for a flake geometry that the actual screw configuration could not produce. The buyer’s effective throughput fell well below the quoted line capacity, and the bottleneck diagnosis took weeks because everyone was looking at the wrong end of the process [NEED_CITE: throughput balance between extrusion and downstream stations in cereal lines].
Why Sourcing the Extrusion Section Decides the Whole Line
Every line we configure starts with the buyer’s raw material specification — corn variety, particle size distribution, protein and fat content — because screw configuration and die design are set against those inputs, not pulled from a generic build. Our in-house testing workshop runs trial batches on customer-supplied grain before shipment, so flake density, toast colour, and bowl-life behaviour are validated before the equipment leaves the factory. The line layout documents throughput matching between the extruder, flaking mill, toaster, and coating drum, preventing the downstream bottleneck scenario. Voltage, frequency, and control language are confirmed against the target market grid standard before production begins. Twin-screw expertise across grain-based applications means the barrel profile is specified by someone who understands starch behaviour, not copied from a catalogue.
Documentation & Verification
- Screw and die configuration record matched to your corn variety and target flake thickness
- Trial run report on customer-supplied grain conducted in testing workshop before dispatch
- Electrical schematic and voltage confirmation aligned to destination market grid standard
- Line layout and capacity calculation showing throughput balance across all stations
- CE declaration of conformity and ISO certificate included with shipment documentation
- Operation and maintenance manual with wear parts list for screw elements and die inserts
Installation, Commissioning & Support
- Foundation and floor plan provided based on your confirmed line layout and station footprint
- Power supply specification listing voltage, frequency, and dedicated circuit requirements per station
- Barrel heating zones and PLC or MCC control interface calibrated on-site during commissioning
- Screw element arrangement verified and die alignment set during initial production trial
- Operator training covering barrel temperature profiling, moisture injection adjustment, and die changeover
- Wear parts inventory recommended based on projected screw and die replacement intervals
What We Need to Configure Your Line
Send your corn meal specification sheet — variety, particle size, moisture content at storage, and any protein or fibre additions in your formulation. Confirm your target flake thickness and whether you are running natural, sugar-coated, or fortified variants. We also need your factory floor dimensions, ceiling height, and local voltage and frequency standard so the line layout and electrical build are correct from the start.
Frequently Asked Questions
Q: How is screw configuration specified to my corn variety and target flake thickness?
A: We review your corn meal’s particle size, starch content, and any protein or fibre additions, then map the screw element arrangement and L:D ratio to achieve the gelatinisation degree your flake thickness requires. A trial run on your supplied raw material in our testing workshop validates the configuration before shipment.
Q: What barrel zone count and temperature profile is needed for full starch gelatinisation?
A: The number of independently controlled heating zones and their temperature setpoints are determined by your corn variety’s gelatinisation onset and the residence time dictated by screw speed. Too few zones limit your ability to control the conversion ramp, risking under-processed or over-expanded output.
Q: Can a trial run be done on my raw material before shipment?
A: Yes. We run your actual corn meal through the configured extruder in our testing workshop and document flake density, expansion behaviour, and bowl-life crunch in a trial report. This confirms the line will produce to your specification before any equipment leaves the factory.
Q: How do moisture and steam injection levels affect final flake crunch?
A: Insufficient moisture leaves ungelatinised starch cores that produce brittle, uneven flakes. Excess moisture creates a sticky melt that sheets poorly and delivers a gummy texture in milk. Injection rates are calibrated to your corn meal’s intake moisture during the pre-shipment trial run.
Q: What is the relationship between extrusion parameters and downstream toasting capacity?
A: Extrusion moisture and expansion directly determine how much residual water the toaster must remove and how evenly the flake browns. If the extruder delivers denser pellets than the toaster was sized for, dwell time must increase, reducing effective line throughput.