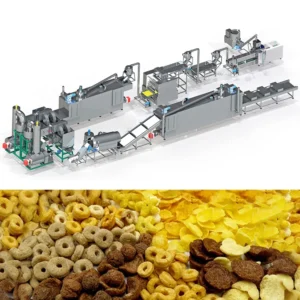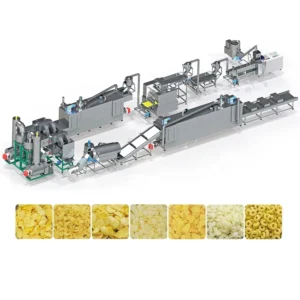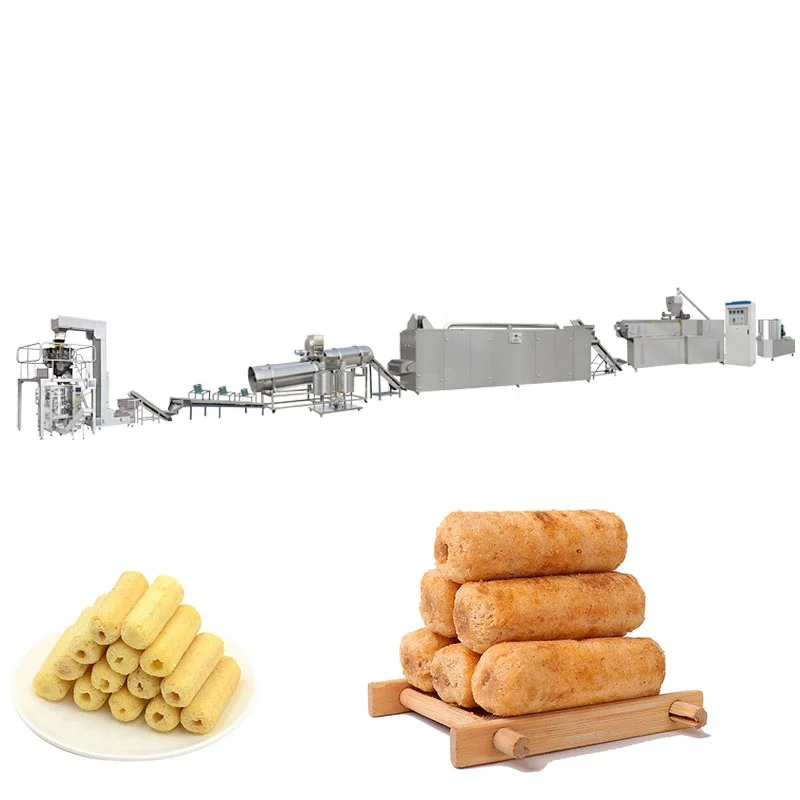
Screw configuration matched to your material — Every corn flakes run starts with a trial on your exact grain blend and moisture level before the screw profile is finalized.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Twin Screw Food Extruder for Corn Flakes Production Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC control system; MCC available |
| Flaking Machinery | Hydraulic double-roller system with independent dual-motor drive and infrared temperature control |
| Dryer Heating Source | Gas or Electric (configurable) |
| Hot Air Roasting Oven | Vibrating pan with high-temperature spray tubes, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Raw Materials | Corn, rice, wheat, oat, and barley powder |
| Final Product Shapes | Natural flakes, coated flakes; ball, tube, stick, ring, fruit loop, star, wheel, flower, heart via die change |
| Line Configuration | Complete turnkey from mixing through packing |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for breakfast cereal retail | Corn powder or grits, single-grain or blended |
| Sugar-coated corn flakes for mass-market cereal boxes | Corn base with sugar glaze applied in double-tumble coating drum |
| Multi-grain extruded flakes | Blends of rice, wheat, oat, and barley powder |
| Extruded cereal shapes beyond flakes | Fruit loops, rings, stars, and balls by swapping extruder die |
| Turnkey cereal line projects for new plants | Full line from batching through packing under single-vendor responsibility |
What "300–500 kg/h" Actually Means on a Corn Flakes Extrusion Line
Rated capacity only holds when your grain formulation, particle size, and moisture match the conditions the screw profile was built for.
I once configured a corn flakes line to catalog output numbers, only to find the customer’s corn powder was coarser than assumed. The extruder pushed material through, but the flakes came out fractured and uneven in thickness. Actual throughput dropped to roughly half the quoted figure because the downstream flaking rolls could not handle the inconsistent sheet. The problem was not the motor or the barrel — it was a screw configuration copied from a generic setup instead of being dialed to the buyer’s specific grind. That is the gap between a nameplate number and a line that actually runs at rate. [NEED_CITE: raw material particle size and moisture impact on twin-screw extrusion output]
How Screw Geometry Controls Flake Texture
The twin-screw extruder in this corn flakes extrusion production line turnkey configuration is not a fixed machine — the screw elements are arranged in sections that control conveying, kneading, and pressure build-up differently depending on your grain type. Corn requires a different shear profile than oat or barley, and the die opening determines the sheet thickness that enters the flaking rolls. When the geometry is wrong, the extrudate arrives at the flaker either too dense or too fragile, and no amount of roll pressure adjustment can fix it upstream.
Temperature Profile Across the Barrel Zones
Each barrel zone on the MT75 is independently heated and monitored, which matters because starch gelatinization in corn happens within a narrow temperature window. Too low and the flake will be gritty and opaque; too high and the material burns at the die face, causing blockages that force a full line stop. The PLC control system tracks these zones continuously, so operators can adjust the profile in real time rather than waiting for a bad batch to reach the roasting oven. [NEED_CITE: starch gelatinization temperature ranges for corn and multi-grain blends]
Reading the Spec Sheet Beyond Motor Power
The installed power of 210 kW tells you what the extruder can draw at peak load, but the 150 kW power consumption figure reflects what a typical corn flakes run actually uses. The 45-meter overall line dimension includes every station from mixing to packing, which means floor planning must account for the full footprint rather than just the extruder alone. The hydraulic flaking system with dual independent motors allows each roller to be driven separately, preventing the sheet from pulling to one side — a detail that directly affects flake uniformity and the final bowl-life of the cereal. Infrared temperature sensors on the flaking rolls keep the surface heat even, so the sheet does not stick or tear during pressing.
The Cost of Mismatched Stations Downstream
An extruder that runs fine in isolation can still bottleneck the entire line if the dryer or roasting oven cannot handle its output. I have seen cereal lines where the extruder pushed material faster than the hot air roaster could blister the flakes evenly, resulting in a mix of under-toasted and over-toasted product in the same batch. The vibrating pan in this roasting oven uses a conciliation burner and two separate circulating fans to keep temperature distribution uniform, but that only works if the feed rate from upstream is matched correctly. When stations are sourced from different vendors, no single supplier owns the throughput balance. [NEED_CITE: throughput mismatch consequences in multi-vendor food processing lines]
Why Sourcing the Full Line Under One Roof Matters
Every station on this line — mixing, extruding, flaking, drying, roasting, coating, cooling, and packing — is configured together so that throughput is balanced before the first weld is made. The screw and die setup is specified to your grain formulation, not pulled from a standard shelf build. The in-house testing workshop runs your actual raw material before the line ships, which means product development happens before installation rather than after. The PLC and MCC control architecture is designed as a single system, so operators manage the entire sequence from one interface rather than juggling separate panels from different suppliers. Electrical schematics, voltage, and HMI language are confirmed before production starts, eliminating the commissioning delays that come from discovering a 60 Hz machine was built for a 50 Hz market.
Documentation & Verification
- Line layout drawing with throughput calculation matched to your corn or multi-grain formulation
- Screw and die configuration record specific to your raw material particle size and moisture target
- Factory trial run report using your actual grain blend before the line leaves the workshop
- Electrical schematic with voltage, frequency, and PLC language confirmed prior to build
- CE declaration of conformity and ISO certificate included with shipping documentation
Installation, Commissioning & Support
- Floor plan must accommodate the full 45-meter line length with clear access around the hot air roasting oven for maintenance
- Dedicated electrical circuit sized for 210 kW installed extruder load plus dryer and roaster heating elements
- Line arrives in modular sections; flaking rolls and roasting oven require on-site alignment and leveling
- First-run commissioning includes screw speed, barrel zone temperatures, and flaking roll gap calibration to your target flake thickness
- Operator training covers PLC interface navigation, die changeover for shape switching, and coating drum sugar melt temperature control
- Wear parts inventory includes replacement screw elements, die inserts, and flaking roll surface components with documented replacement intervals
What to Include in Your Inquiry
Send your grain type and grind specification, target daily output, and workshop floor dimensions with ceiling height. Confirm your local voltage and frequency, the preferred PLC language, and whether you need the natural flake path or the sugar-coated variant. If you have an existing upstream mixer or downstream packing system, let us know so the line interfaces correctly. We can also schedule a trial run with your material in the testing workshop before the quotation is finalized.
Frequently Asked Questions
Q: How do you prevent throughput bottlenecks between the extruder, flaker, and roasting oven?
A: Every station is sized against the same throughput target during the line layout phase. The MT75 extruder output, flaking roll feed rate, and roasting oven capacity are calculated together so no single station restricts the others. This avoids the common problem where one vendor’s extruder outpaces another vendor’s dryer.
Q: How is the screw configuration determined for my specific corn or grain blend?
A: The screw element arrangement — conveying, kneading, and metering sections — is selected based on your raw material particle size, moisture content, and the target flake density. This is documented in the screw configuration record you receive before shipment, so the build is traceable and repeatable.
Q: Can I test my own raw material before the line ships?
A: Yes. The testing workshop runs your actual grain blend through the extruder and flaking system to verify flake thickness, texture, and throughput before the line is packed. The trial run report is included in the documentation package, so you know the line will perform on your material from day one.
Q: How are voltage and control language confirmed before production?
A: The electrical schematic is reviewed with you during the specification confirmation stage. Voltage, frequency, and PLC/HMI language are locked in writing before the control cabinet is wired. This prevents the situation where a machine arrives on site and cannot be powered or operated in the local language.
Q: What wear parts should I plan to replace, and how often?
A: The wear parts list covers screw elements, die inserts, and flaking roll surfaces. Replacement intervals depend on your grain abrasiveness and daily run hours, but the initial spare set is included with the line. The operation manual documents the inspection schedule so you can order replacements before they are needed.