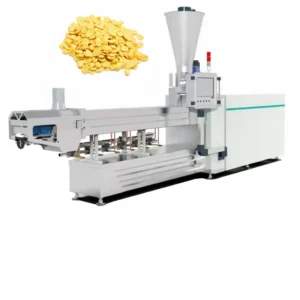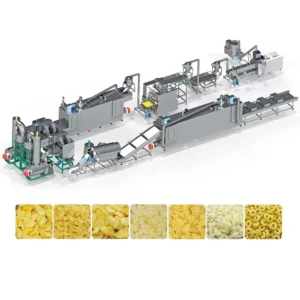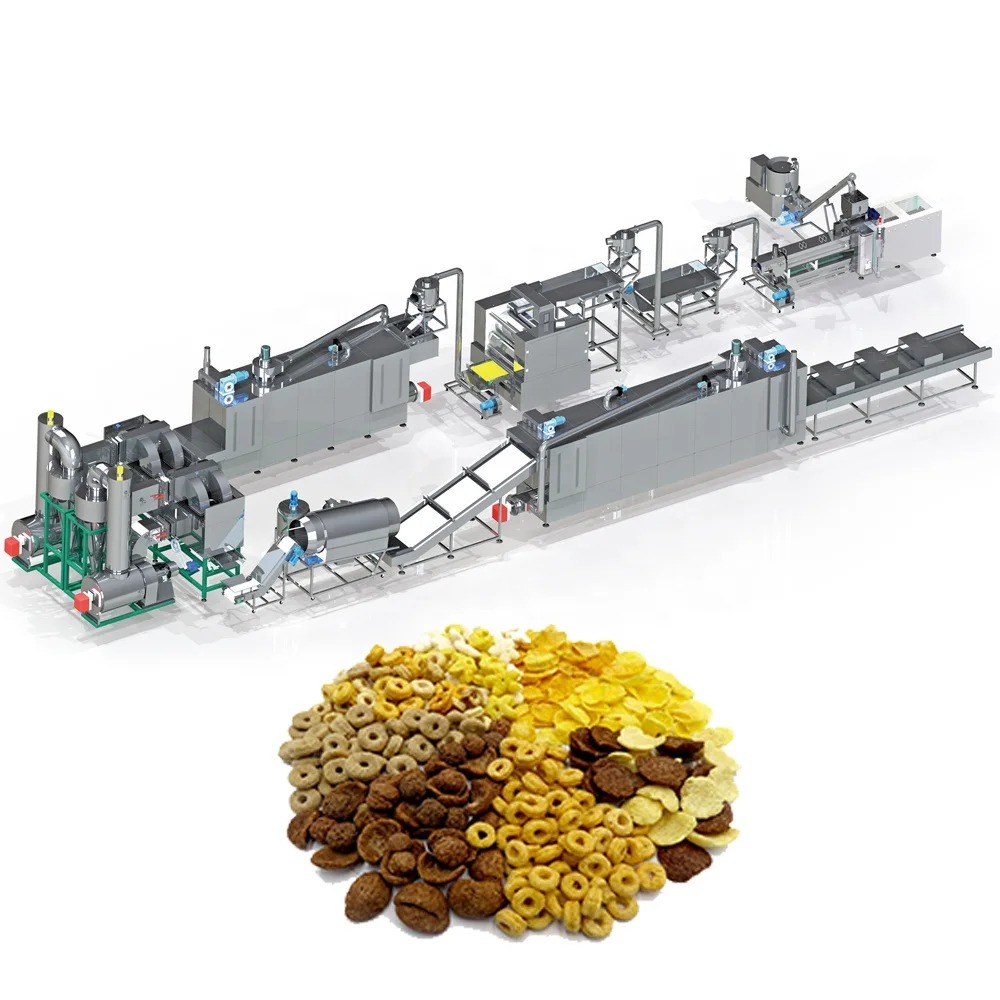
Thermodynamics-Matched Line Design — Every station from the twin-screw extruder through flaking, roasting and coating is sized to the buyer’s grain blend and moisture profile, preventing bottlenecks that silently cap real-world output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Breakfast Cereal Production Line |
| Available Models | MT70 / MT85 / MT75 |
| Extruder Type | Twin Screw |
| Installed Power | 160 kW (MT70) / 190 kW (MT85) / 210 kW (MT75) |
| Operating Power | 120 kW (MT70) / 140 kW (MT85) / 150 kW (MT75) |
| Output Capacity | 150–200 kg/h (MT70), 300–400 kg/h (MT85), 300–500 kg/h (MT75) — basis to be confirmed with buyer’s raw material and moisture |
| Line Footprint (L×W×H) | 41 × 1.5 × 2.2 m (MT70) / 43 × 1.5 × 3.2 m (MT85) / 45 × 1.5 × 3.5 m (MT75) |
| Screw Material | Wear-resistant alloy |
| Control System | PLC with automatic lubricating and cooling |
| Flaking Unit | Hydraulic double-roller, independent motor drives, infrared temperature sensor |
| Dryer Heating Source | Gas or Electric (configurable) |
| Roasting Oven | Hot air circulation, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spray nozzle |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes for retail and foodservice | Corn grits, corn flour |
| Sugar-coated breakfast cereal | Corn, rice, wheat blends with sugar glaze |
| Multi-grain extruded cereal shapes | Oat, barley, rice and wheat powder mixes |
| Puffed snack shapes on the same extrusion platform | Rings, balls, stars, tubes via die change |
What "Rated Capacity" Actually Means for Your Corn Flake Output
A capacity number without a grain specification is not a capacity — it is a guess.
I spent years on workshop floors in the Pearl River Delta watching extrusion lines get installed, and the most expensive failures are never mechanical. They are the lines that run fine on the factory acceptance test with standard corn grits at controlled moisture, then choke the moment a buyer switches to a local grain variety with higher oil content or different starch behaviour. The extruder barrel fills unevenly, gelatinisation drops off, the flakes come off the rollers as碎渣 instead of intact sheets, and the roasting oven cannot keep up because the upstream throughput has collapsed. Nobody lied about the capacity. The capacity was simply quoted against a material the buyer will never use [NEED_CITE: starch gelatinisation temperature variance across corn varieties].
Screw Geometry and Barrel Profile: Where Flake Integrity Begins
The twin-screw extruder in this corn flakes extrusion production line turnkey system is configured around the buyer’s specific grain formulation. Corn, rice, wheat, oat and barley each demand a different balance of shear, residence time and barrel temperature to achieve the partial gelatinisation that corn flakes require — enough to bind the dough, but not so much that it puffs like a snack. The screw elements are selected and sequenced to hold that narrow window, and the die design controls the dough strand shape that feeds into the flaking rolls downstream.
Flaking, Roasting and Coating: The Stations That Define Final Texture
Flake thickness is set at the hydraulic double-roller station, where independent motor drives on each roller prevent drag marks and the infrared sensor holds surface temperature steady across long runs. The hot air roasting oven then does the work that creates the characteristic blistered surface and crispness buyers expect — dual circulating fans move air through the vibrating pan while the cyclone device pulls fines out before they can scorch. For sugar-coated variants, the dual-tumble system separates melting, spraying and drying into distinct stages so the glaze builds up in even layers rather than clumping.
Reading the Specs: What the Numbers Mean on the Floor
The installed versus operating power gap across all three models — roughly 25% lower operating draw — reflects the automatic lubricating and cooling system on the extruder, which keeps barrel friction predictable over extended shifts rather than drifting as components heat up. Line footprint spans over 40 metres in length for every model, which tells a buyer immediately that this is a multi-stage process requiring significant floor space with clear access on both sides for maintenance. The hydraulic flaking unit with separate roller motors matters because a single shared drive will transmit vibration from one roller to the other, creating thickness variation that shows up as uneven roasting [NEED_CITE: roller drive vibration transfer in cereal flaking]. The PLC control ties lubrication, temperature and feed rate together so that batch-to-batch consistency does not depend on operator memory.
The Cost of Underspecifying the Line
When an extruder is quoted without matching dryer or coating capacity, the line hits a wall that no amount of extruder tuning can fix. Wet flakes pile up waiting for oven space, sugar coating backs up because the tumble drum cannot process what the roaster delivers, and the rated output becomes a theoretical number the line never reaches in continuous production. Grain moisture variation compounds this — a formulation that runs cleanly at 13% moisture may require different screw compression and longer drying at 16%, and if those adjustments were never mapped, the buyer discovers the problem during commissioning instead of before shipment [NEED_CITE: moisture content impact on extrusion throughput stability].
Why Source This Line From Meiteng
Every station in the corn flakes extrusion production line turnkey package is throughput-matched under a single supplier, so the flaking rolls, dryer, roasting oven and coating drum are sized to what the extruder actually delivers rather than assembled from mismatched vendors. Screw configuration and die design are specified to the buyer’s raw material and target flake density, not copied from a generic build. The in-house testing workshop runs the buyer’s actual grain blend before the line ships, which means product development happens in Jinan, not on the buyer’s factory floor during commissioning. Voltage, frequency and PLC language are confirmed before production begins, avoiding the weeks of delay that happen when a control panel arrives with the wrong motor ratings. Wear parts lists for screws, dies and roller surfaces are provided with the shipment so the first replacement cycle does not become a sourcing emergency.
Documentation & Verification
- Line layout and capacity calculation matched to your grain blend and target flake weight
- Screw and die configuration record specified to your product density and expansion target
- Trial run report on your raw material conducted in the testing workshop before dispatch
- Electrical schematic with voltage, frequency and PLC language confirmed to your market
- Factory test record covering every station from batching through coating
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Floor space planning for line footprint exceeding 40 m with utility connection points mapped
- Dedicated power circuit sized to the model’s installed power, up to 210 kW for the MT75
- Extruder screw elements and barrel sections shipped assembled, with flaking and roasting stations positioned on-site
- First-run parameter setting for barrel temperature profile, roller gap and oven air flow on your grain
- Operator training covering PLC interface, die changes and hydraulic roller adjustment
- Wear parts stock including replacement screw segments, die plates and roller surfaces
What We Need to Configure Your Line
To build an accurate line proposal, we need to know your base grain or grain blend, the moisture range you will be working with, and the target flake thickness and final product weight per unit volume. Your local voltage and frequency, preferred PLC language, and available factory floor dimensions including ceiling height will determine the electrical build and layout. If you are running an existing upstream milling system or downstream packing line, share the interface specifications so the conveyor and buffer stations are matched correctly.
Frequently Asked Questions
Q: How do you verify that the line will hold rated capacity on my specific grain?
A: We run your actual raw material in our testing workshop before the line ships. The trial covers extrusion stability, flake integrity off the rollers and behaviour through the roasting oven at your target moisture. The results are documented in a trial run report that becomes the baseline for screw configuration and die selection, so the line arrives already tuned to your formulation rather than requiring weeks of adjustment on your floor.
Q: Can the same line produce both natural and sugar-coated corn flakes?
A: Yes. The natural line runs mixing through extruding, flaking, drying, hot air roasting, cooling and packing. For sugar-coated production, three additional stations are integrated after roasting: a sugar melting system, a spray coating drum and a secondary drying stage. The extruder and flaking stations remain the same; the coating section is added as an extension to the same PLC-controlled line.
Q: How is screw configuration matched to my target flake density?
A: Corn flakes require partial starch gelatinisation — enough to bind but not enough to puff. We select screw element types and sequence them to control shear and residence time for your specific grain. The die design then shapes the extruded strand that feeds the flaking rollers. Both are recorded in a configuration document that is provided with the line and referenced during operator training.
Q: What electrical details do I need to confirm before production starts?
A: We need your local voltage, frequency and preferred control language for the PLC interface. These are confirmed against the electrical schematic before the line enters production so that motor ratings, heating elements and sensor calibrations match your facility. Arriving with mismatched voltage is one of the most common causes of delayed commissioning on imported processing lines.