
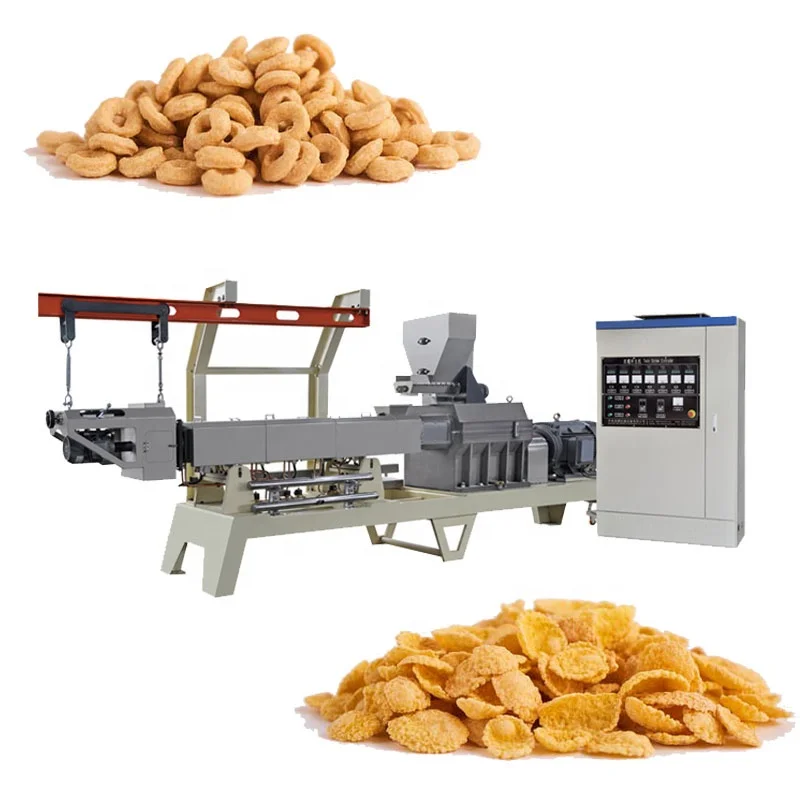
Twin-Screw Extrusion Expertise — screw configuration and barrel temperature profile specified to your corn formulation, ensuring consistent gelatinisation and flake density before the line ever ships.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Models Available | MT-65 / MT-70 / MT-75 / MT-85 |
| Screw Type | Twin Screw (co-rotating, sectional modules) |
| Line Stations | Mixer → Screw Conveyor → Double Screw Extruder → Corn Flakes Press Machine → High-Temperature Oven → Sugar Spraying System |
| Mixer Output | 10–30 kg/load |
| Mixer Power | 4 kW |
| Screw Conveyor Power | 0.75 kW |
| Corn Flakes Press Machine Power | 16.12 kW |
| Corn Flakes Press Machine Roller Size | 510×310×1050 mm |
| High-Temperature Oven Heating Source | Gas |
| High-Temperature Oven Power | 3.75 kW |
| High-Temperature Oven Dimension | 4.5×1.4×1.8 m |
| Sugar Spraying System Total Power | 28.75 kW |
| Sugar Spraying System Roller Size | Ø600×2700 mm |
| MT-65 Installed / Real Power | 84 kW / 59 kW |
| MT-65 Output Capacity | 120–150 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| MT-70 Installed / Real Power | 132 kW / 92 kW |
| MT-70 Output Capacity | 200–250 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| MT-75 Installed / Real Power | 186 kW / 140 kW |
| MT-75 Output Capacity | 300–400 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| MT-85 Installed / Real Power | 239 kW / 167 kW |
| MT-85 Output Capacity | 400–500 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Gear Box Lubrication | Oil forced automatic lubrication system |
| Cutting System | Non-stop cutting system |
| Extruder Self-Cleaning | Yes |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn flakes breakfast cereal | Corn grits, corn flour with sugar coating |
| Rice-based flaked cereal | Rice flour, blended grain formulations |
| Wheat flakes and multigrain cereal | Wheat flour, composite grain mixes |
| Fortified breakfast cereal | Grain flour with added vitamin and mineral premix |
Why "Rated Output" Means Nothing Without Your Raw Material
A corn flakes extrusion production line quoted at a fixed throughput figure tells you what the machine does on someone else’s corn formulation, not yours. Capacity only matters when it is tied to your exact grits particle size, fat content, and moisture level.
I once watched a line rated for steady output choke within the first hour because the buyer switched from standard corn flour to high-fat degerminated grits after signing the contract. The starch gelatinisation window shifted, barrel temperatures were wrong for the new material, and the flakes turned to mush the moment they hit milk. The entire first batch was reworked [NEED_CITE: starch gelatinisation behaviour in high-fat corn grits during twin-screw extrusion]. That is why every capacity figure in the table above carries a note — those numbers must be validated against your specific raw material before they mean anything.
Screw Configuration and Barrel Profile for Corn Gelatinisation
The twin-screw co-rotating extruder uses sectional screw modules, meaning the screw elements can be rearranged along the barrel to control shear intensity and residence time at each zone. For a corn flakes extrusion production line, this matters because starch gelatinisation in corn grits requires a precise balance of heat, moisture, and mechanical shear. Too little shear and the starch remains partially raw, producing flakes that crumble in the bowl. Too much shear and the dough overheats, causing premature expansion before the pressing stage. The barrel temperature profile is set zone by zone to match the gelatinisation curve of your specific corn formulation.
Die Geometry and Moisture Control at the Extrusion Stage
The die plate at the extruder discharge determines the shape and initial moisture content of the extruded pellet before it reaches the corn flakes press machine. Die hole diameter and land length influence how much the dough expands as it exits the barrel. On this corn flakes extrusion production line, the die is selected to produce a compact, low-expansion pellet that can be flattened uniformly by the press rollers without tearing or sticking. Moisture addition during extrusion is calibrated to the target flake thickness and the cooling capacity of the press [NEED_CITE: die land length effect on extrudate expansion in cereal processing]. Getting this step wrong cascades through every downstream station.
Reading the Power and Capacity Data
The installed power versus real power gap across the MT-65 through MT-85 models reflects the difference between peak motor rating and typical operating draw. For a corn flakes extrusion production line running continuously, real power is the figure that determines your energy cost and transformer sizing. The oil forced automatic lubrication system on the gearbox extends service intervals under sustained load, which matters when you are running multi-shift cereal production. The non-stop cutting system ensures pellets are cut to uniform length without halting the extruder, keeping the press machine fed at a steady rate. Roller dimensions on the press at 510×310×1050 mm define the maximum pellet width the machine can flatten, and the adjustable roller gap lets you dial in flake thickness from thin and crispy to thick and hearty.
The Cost of Skipping the Trial Run
When a corn flakes extrusion production line ships without a factory trial on the buyer’s actual raw material, the first real test happens on your floor with your utilities, your operators, and your deadline. If the screw configuration does not match your grits, you will see it in the flake density — either too dense and hard, or too porous and fragile to survive packaging and transport. Adjusting barrel zones, screw elements, and die selection on-site takes days of downtime and raw material waste that could have been resolved in the testing workshop before the machines left the factory [NEED_CITE: cost of post-installation process correction versus pre-shipment trial runs].
Why Source This Line Here
Screw configuration and die design are specified to your raw material and target flake texture, not copied from a generic build. The in-house testing workshop runs your actual corn grits or flour through the extruder before shipment, producing a trial run report you can review. Every station from the mixer through the sugar spraying system is throughput-matched so the extruder is never starved or bottlenecked by a downstream station. Electrical schematics, voltage, and control language are confirmed for your target market before production begins, avoiding commissioning delays. CE and ISO certified documentation accompanies every shipment.
Documentation & Verification
- Line layout and capacity calculation showing throughput balance across every station
- Screw and die configuration record matched to your corn formulation
- Trial run report on your raw material from the testing workshop
- Electrical schematic with voltage and frequency confirmation
- CE declaration of conformity and ISO certificate
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation and floor space planning based on the selected model dimension up to 28 m line length
- Dedicated power circuit sized to the installed power rating of the chosen extruder model
- Separate station assembly with throughput-matched connections between each unit
- First-run parameter setting including barrel zone temperatures and press roller gap adjustment
- Operator training on screw module changes and non-stop cutting system operation
- Wear parts list covering screws, dies, and press roller surfaces with replacement intervals
What to Include in Your Inquiry
To move forward on a corn flakes extrusion production line, share your raw material type and particle size distribution, target flake thickness and bowl-life specification, and daily production volume. Include your facility voltage and frequency, available floor space and ceiling height, and whether you need the sugar spraying system configured for a specific coating recipe. If you can send a sample of your corn grits or flour, a trial run can be scheduled in the testing workshop before any equipment is built.
Frequently Asked Questions
Q: How is output capacity verified for a corn flakes extrusion production line?
A: Capacity figures listed for each model are baseline values that must be confirmed against your specific raw material formulation, moisture content, and target flake density. A trial run in the testing workshop using your actual corn grits or flour is the only reliable way to verify real throughput before the line ships.
Q: How is screw configuration chosen for my corn formulation?
A: The twin-screw extruder uses sectional modules that are arranged along the barrel to match the shear and residence time your material requires. High-fat degerminated grits need a different screw profile than standard corn flour, and the configuration is documented in a record you receive with the line.
Q: What barrel temperature profile controls starch gelatinisation?
A: Barrel zones are set individually to follow the gelatinisation curve of your corn material. Moisture addition and zone temperatures are adjusted together so the dough reaches the correct degree of cook before it exits the die, producing a pellet that presses into flakes with consistent crispness.
Q: Can the line be configured for my local voltage and control language?
A: Electrical schematics, voltage, and frequency are confirmed for your market before production starts. The control system language is set to match your operators, and all documentation is provided accordingly so commissioning proceeds without electrical or interface delays.
Q: Is a trial run performed before the line ships?
A: Yes. Your raw material is run through the extruder in the in-house testing workshop, and a trial run report documenting screw configuration, barrel temperatures, and flake quality results is provided before dispatch. This prevents process surprises during on-site commissioning.


