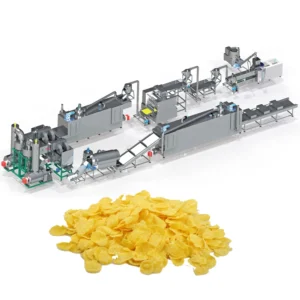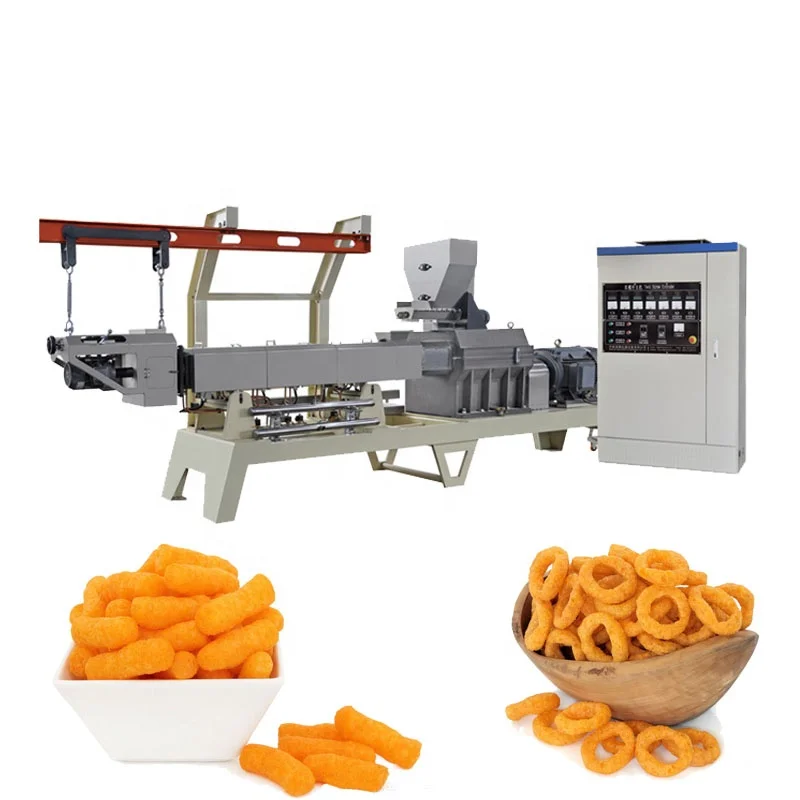
Screw Configuration Matched to Formulation — extrusion geometry and barrel profile specified after reviewing your cereal blend, ensuring consistent flake expansion and texture from the first batch.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Twin Screw Corn Flakes Extrusion Line |
| Screw Type | Twin-screw with automatic lubricating and cooling |
| Installed Power | 210 kW (MT75) |
| Power Consumption | 150 kW (MT75) |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material, moisture, and flake spec) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC and MCC |
| Dryer Heating Source | Gas or electric (selectable) |
| Flaking System | Hydraulic double-roller, separate motor drive, infrared temperature control |
| Roasting Oven | Hot air with conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Basic Materials | Corn, rice, wheat, oat, barley powder |
| Final Products | Natural and sugar-coated flakes; ball, tube, stick, ring, fruit loop, star, wheel, flower, heart shapes |
| Voltage & Frequency | Customized to buyer’s local standard (confirm before production) |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Corn grits or corn flour base |
| Sugar-coated breakfast cereal | Corn, rice, or multi-grain blend with sugar spraying and coating |
| Multi-grain flake formats | Blends of wheat, oat, barley, rice, and corn |
| Extruded cereal shapes | Fruit loops, rings, stars, balls, tubes, sticks on the same extrusion platform |
| Fortified breakfast cereals | Vitamin- or mineral-enriched grain formulations requiring controlled gelatinisation |
Why the Flaking Gap Ruins Bowl-Life
A corn flakes extrusion machine production line that delivers perfect pellets but leaves flaking, drying, and roasting unmatched will produce flakes that either shatter in the bowl or stay stubbornly hard.
When extruder throughput outpaces flaker capacity, pellets pile up, cool unevenly, and resist rolling. The result is inconsistent flake thickness across the batch. Downstream, the roasting oven cannot develop uniform surface blistering because some flakes carry more residual moisture than others. Buyers who evaluate only the extruder specification frequently discover these mismatches during commissioning, when the line cannot hold its rated output without sacrificing texture [NEED_CITE: throughput matching across extrusion line stations]. I once saw a South American installation where the extruder ran well on pure corn flour during factory trials, but the buyer’s actual formula included oat and rice flour. The expansion dropped, flakes came out thick and dense, and the entire screw configuration and barrel temperature profile had to be rebuilt on site.
Shear and Moisture Control Through the Barrel
The twin-screw design on this corn flakes extrusion machine production line manages two variables that determine flake quality: mechanical shear and moisture distribution. Automatic lubricating and cooling circuits in the screw assembly keep barrel temperatures stable across long runs. When processing multi-grain blends, different starches gelatinise at different thresholds, so a consistent barrel temperature profile prevents partial cooking in one zone and over-shearing in another. The screw elements are selected and sequenced to match your raw material’s starch composition, moisture target, and desired pellet density before the material ever reaches the die.
Flaking Precision Before the Roasting Stage
The hydraulic double-roller flaking station uses separate motors for each roller and infrared sensors to monitor roller surface temperature. Uniform roller gap and temperature are critical because even a slight thickness variation translates into uneven roasting. Thinner flakes scorch while thicker ones retain internal moisture, leading to a short shelf life. The infrared feedback loop keeps the roller surface within a narrow band, which is particularly important when switching between corn, oat, and wheat-based formulations that respond differently to pressure and heat [NEED_CITE: flaking roller temperature influence on cereal shelf stability].
Reading the Specification Sheet for What Matters
The installed power of 210 kW on the MT75 reflects the combined demand of the extruder drive, barrel heaters, and feeding system, while actual consumption of 150 kW indicates typical running load. The 45-meter line length encompasses every station from mixing to packing, meaning floor space planning must account for material flow and operator access along the full run. The PLC and MCC control architecture separates motor control from process logic, so adjustments to barrel temperature zones or screw speed do not interfere with conveyor or dryer sequencing. Voltage and frequency remain configurable, which is essential because a 50 Hz motor on a 60 Hz supply will overspeed the extruder and alter residence time inside the barrel, directly affecting starch gelatinisation and pellet density.
The Cost of Skipping a Trial Run
When a corn flakes extrusion machine production line ships without a trial run on the buyer’s actual raw material, the first weeks of production become an expensive experiment. Screw combinations and die openings set for generic corn grits may produce pellets that are too dense for oat-heavy blends or too fragile for wheat-rich formulas. Operators spend shifts adjusting barrel temperatures and feed rates while generating off-spec product. Flakes that fail the bowl-life test — becoming soggy within minutes or refusing to soften at all — reach the market and erode brand trust [NEED_CITE: breakfast cereal texture and consumer retention]. Downtime during this adjustment window also means lost throughput and delayed order fulfilment.
Why Procurement Starts with the Formulation
Every corn flakes extrusion machine production line shipped from our testing workshop carries a screw and die configuration record matched to the buyer’s raw material, not a generic build copied from a previous order. The in-house testing workshop runs your actual grain blend through the extruder before shipment, generating a trial run report that documents expansion ratio, pellet density, and moisture content at each station. Line layout and capacity calculations show how the extruder output matches the flaker, dryer, and roaster capacities so no station becomes a bottleneck. Electrical schematics include confirmed voltage and frequency for your facility, and the PLC/HMI language is set before the control panels are wired. Documentation covers every step from the initial formulation review through factory test records, so your engineering team has the data to validate the installation against the original specification [NEED_CITE: industrial line documentation standards for food processing equipment].
Documentation & Verification
- Screw and die configuration record matched to your grain blend and target flake density
- Trial run report on your raw material documenting expansion, moisture, and pellet dimensions
- Electrical schematic with voltage, frequency, and PLC language confirmed to your facility
- Line layout showing throughput matching between extruder, flaker, dryer, and roaster stations
- CE declaration of conformity and ISO certificate for the complete assembled line
Installation, Commissioning & Support
- Foundation plan for the 45-meter line layout covering extruder, flaking, and roasting zones
- Power supply specification for the 210 kW installed load with dedicated circuit requirements
- On-site assembly of flaking rollers, roasting oven, and coating drum by commissioning engineers
- First-run parameter setting for barrel temperature zones and screw speed on your raw material
- Operator training on PLC interface, hydraulic roller gap adjustment, and roaster temperature profile
- Wear parts list covering screws, dies, and roller surfaces with recommended replacement intervals
What We Need to Configure Your Line
Before we build a proposal for a corn flakes extrusion machine production line, share your grain formulation — the percentage of corn, rice, oat, wheat, or barley in the blend — along with your target flake thickness and whether you need natural or sugar-coated output. We also need your facility voltage, frequency, and preferred PLC/HMI language so the control system ships ready for your electricians. If you have existing upstream mixers or downstream packing equipment, send their throughput ratings so we can confirm station matching across the full line.
Frequently Asked Questions
Q: How is screw configuration matched to different cereal raw materials?
A: Each grain blend has a distinct starch gelatinisation temperature and moisture absorption rate. We review your formulation, select screw elements that provide the right shear and residence time, and choose a die opening that delivers the target pellet density. A trial run on your material in our testing workshop validates the configuration before the line ships.
Q: What is the relationship between extrusion moisture, flake thickness, and roasting blistering?
A: Higher extrusion moisture produces softer pellets that flatten more easily but require longer drying. Flake thickness determines how quickly the roasting oven can drive off residual moisture and develop surface blisters. If moisture and thickness are not balanced, flakes either scorch on the surface or remain doughy inside.
Q: Can the die produce multiple breakfast cereal shapes on one extruder?
A: Yes. The die plate is interchangeable, allowing formats such as fruit loops, stars, rings, balls, and tubes on the same extruder. Changing the die is part of normal production changeover, and each shape requires a corresponding adjustment to cutting speed and downstream drying parameters.
Q: How is throughput verified before shipment?
A: We run your actual raw material through the extruder, flaker, and dryer in our testing workshop and document output rate, flake dimensions, moisture content, and expansion ratio. The trial run report is shared with your team so you can confirm the line meets your specification before it leaves the factory.
Q: What voltage and language options are confirmed before production?
A: We confirm your facility voltage, frequency, and preferred PLC/HMI language during the specification stage. The electrical schematic and control panel wiring reflect these values so the line is ready for connection on arrival without motor or drive replacements.