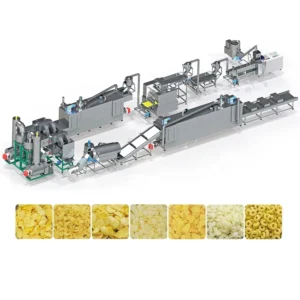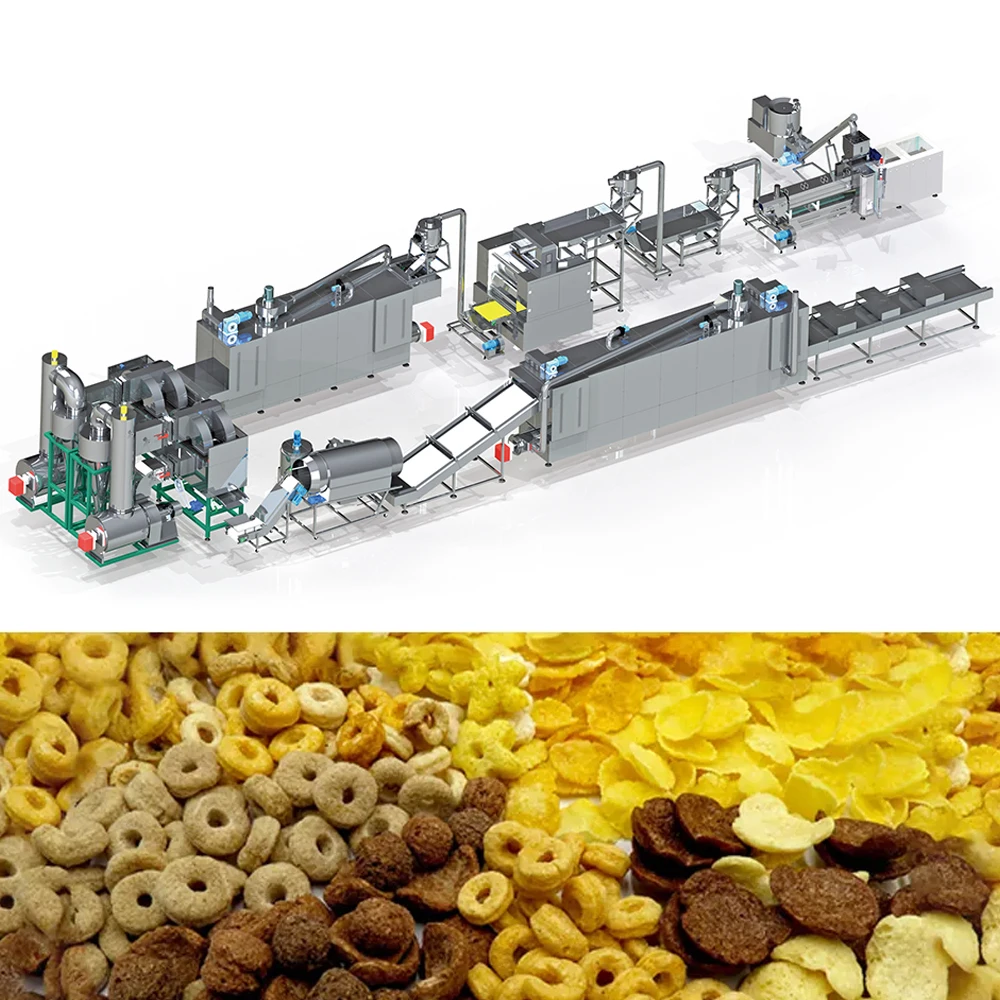
Screw configuration and die design — every MT75 barrel profile and downstream station is matched to your raw material and target flake density, verified through in-house trial runs before the line ships.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Breakfast Cereal Production Line |
| Models Available | MT70 / MT75 / MT85 |
| Extruder Screw Type | Twin-screw |
| MT75 Installed Power | 210 kW |
| MT75 Power Consumption | 150 kW |
| MT75 Overall Dimensions | 45 × 1.5 × 3.5 m |
| MT70 Installed Power | 160 kW |
| MT70 Power Consumption | 120 kW |
| MT70 Capacity | 150–200 kg/hr (basis not stated in source) |
| MT85 Installed Power | 190 kW |
| MT85 Power Consumption | 140 kW |
| MT85 Capacity | 300–400 kg/hr (basis not stated in source) |
| Control System | PLC control (flaking machinery); MCC and PLC control (line-level) |
| Flaking Machinery | Hydraulic double-roller system with separate motor drives; infrared sensor temperature control |
| Dryer Heating Source | Gas or electric (configurable) |
| Roasting Oven | Hot air roasting with conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Screw Material | Wear-resistant alloy |
| Lubrication | Automatic lubricating and cooling function |
| Voltage & Frequency | Configurable to target market standard (basis to be confirmed) |
| Warranty | 24 months with lifetime service |
| Standards | CE certified; ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Plain corn flakes breakfast cereal | Corn grits processed through extrusion, flaking, and roasting |
| Sugar-coated corn flakes | Flaked cereal with sugar glaze applied via double tumble coating drum |
| Chocolate-coated breakfast cereal | Extruded and flaked base with chocolate or cocoa-based coating |
| Various shaped breakfast cereal snacks | Same line configured with alternative die plates for different formats |
What "Rated Capacity" Actually Means for Your Corn Flake Line
Capacity is only real when it is measured against your specific corn grit formulation and target moisture content.
A production line quoted at a nominal throughput often cannot sustain that output once the buyer’s actual raw material enters the extruder barrel. Corn grits vary in particle size, fat content, and starch composition across regions and suppliers, and each variation shifts how the material behaves under heat and shear inside the twin-screw chamber. When the corn flakes extrusion production line screw configuration die design is copied from a generic template rather than specified to the buyer’s formulation, the result is a line that either underproduces or generates flakes with inconsistent density and blistering [NEED_CITE: twin-screw extrusion process parameters for cereal flaking]. Process engineers evaluating this equipment should always request a capacity calculation that references the exact raw material specification and moisture targets, not a brochure figure.
Barrel Temperature Profiling and Starch Gelatinisation Control
The twin-screw extruder at the heart of this line uses multiple heating zones along the barrel, each independently controlled to manage how corn starch gelatinises as it moves through the chamber. The corn flakes extrusion production line screw configuration die design determines the residence time and shear intensity at each zone, which directly governs the degree of starch conversion. Insufficient gelatinisation produces brittle flakes that shatter during roasting, while excessive gelatinisation creates a gummy texture that collapses after flaking. The PLC-controlled system maintains stable temperature profiles across extended production runs, reducing batch-to-batch variation that manual systems typically introduce.
Die Geometry and Flake Density Specification
Die plate design controls the shape, thickness, and expansion ratio of the extrudate before it reaches the flaking rollers. For corn flakes, the die must produce a continuous ribbon or pellet that flattens uniformly under the hydraulic double-roller system without cracking at the edges. The die geometry is selected based on the target flake density that the buyer’s market expects — thinner flakes toast faster and deliver a lighter crunch, while thicker flakes hold up better in milk [NEED_CITE: cereal flake density and consumer texture preference]. The infrared sensor temperature control on the flaking machinery further refines thickness consistency by monitoring roller surface conditions in real time.
Reading the Power and Dimension Data
The MT75 model draws 210 kW installed power with 150 kW typical consumption, reflecting the energy required to drive the twin-screw mechanism, barrel heating zones, and automatic lubrication system simultaneously. The 45-meter line length accounts for every station from mixing through extrusion, molding, drying, flaking, roasting, and coating — a layout that ensures throughput matching between stations rather than bottlenecking at the dryer or roaster. The hydraulic double-roller flaking machinery uses separate motor drives for each roller, allowing differential speed adjustment that influences flake surface texture. Hot air roasting with dual circulating fans and cyclone dust removal ensures even surface blistering while capturing particulate before it accumulates on the product or the workshop floor.
The Cost of Generic Screw Configurations
When an extruder is supplied with a screw and die setup copied from a standard build rather than engineered for the buyer’s corn grit source, the consequences extend beyond throughput loss. Flakes may sink instead of floating in the bowl, or the surface may lack the characteristic blistering that consumers associate with quality corn flakes. Downstream stations — the dryer, flaker, and roaster — are all calibrated to an expected extrudate density, so a mismatch at the extruder cascades through every subsequent process step. Correcting this after installation means replacing screw elements, re-cutting die plates, and recalibrating temperature profiles, all of which delay commercial production [NEED_CITE: extrusion screw element replacement and production downtime].
Engineering Accountability Across the Full Line
Screw configuration and die design are specified to the buyer’s raw material and target flake density, not borrowed from a generic catalogue. Every downstream station — dryer, flaker, roaster, coater — is throughput-matched to the extruder output, so the line runs at rated capacity without one station holding back another. The in-house testing workshop conducts trial runs on the customer’s actual corn grit formulation before shipment, generating a test report that documents product texture, expansion ratio, and line parameter settings. The PLC-controlled flaking machinery and MCC line-level control provide consistent operational repeatability across shifts and operators. Pre-sales consultation, on-site installation, commissioning, and operator training are handled by a single engineering team, eliminating coordination gaps between multiple vendors.
Documentation & Verification
- Line layout and capacity calculation showing throughput matching from mixing through packing
- Screw and die configuration record matched to your specific corn grit formulation
- Trial run report on your raw material documenting flake density, expansion, and texture
- Electrical schematic with voltage and frequency confirmed to your facility standard
- CE declaration of conformity and ISO certificate for regulatory compliance
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation planning for the 45-meter line length with utility connection points mapped to your facility layout
- Dedicated electrical circuit sized for the MT75 at 210 kW installed power with voltage confirmed before production
- Modular station delivery with reassembly sequence documented in the installation manual
- First-run parameter setting for barrel temperature, roller pressure, and roaster airflow by on-site engineers
- Operator training covering PLC interface navigation, screw element inspection, and hydraulic roller adjustment
- Wear parts inventory including replacement screw elements and die plates with lead time guidance
Preparing Your Technical Inquiry
To move from general interest to a configured line proposal, share your corn grit specification including particle size distribution and moisture content, your target daily output in finished flake weight, and the flake density or texture your market expects. Confirm your facility voltage and frequency standard, preferred control language, and available workshop dimensions so the line layout fits your floor plan. If you have an existing upstream batching system or downstream packing line, describe those interfaces so the new stations integrate without modification.
Frequently Asked Questions
Q: How is extruder capacity verified against my specific corn grit formulation?
A: The in-house testing workshop runs your actual raw material through the twin-screw extruder before shipment. The trial documents throughput at your target moisture level, extrudate expansion ratio, and the screw speed and barrel temperature settings required. This report becomes the baseline for your commissioning parameters, replacing generic brochure capacity figures with data tied to your formulation.
Q: How are screw configuration and die design selected for corn flakes versus other cereal formats?
A: Corn flakes require a specific degree of starch gelatinisation and a ribbon or pellet extrudate that flattens cleanly under the hydraulic rollers. The screw element arrangement and die geometry are chosen to deliver that profile at your target throughput. Other cereal formats — such as extruded balls or shaped pieces — use different element sequences and die plates on the same extruder platform.
Q: What barrel temperature profile and moisture settings control flake expansion and density?
A: Each barrel heating zone is set to progressively gelatinise the corn starch without overcooking the outer layer before the material reaches the die. Moisture content at the extruder inlet influences how much steam expands the extrudate upon exit. The PLC system maintains these settings consistently across production runs, reducing the density variation that manual adjustment typically produces.
Q: How is throughput matched between the extruder, dryer, flaker, and roaster to prevent bottlenecks?
A: The line layout calculation accounts for the capacity of every station, not just the extruder. Dryer belt speed, flaker roller feed rate, and roaster conveyor dwell time are each specified so that material flows continuously without accumulation or starvation at any point. This matching is documented in the capacity calculation provided before order confirmation.
Q: Can a trial run be done on my raw material before shipment, and what does the trial report cover?
A: Yes. The testing workshop runs your corn grit formulation through the configured extruder and downstream stations. The report covers extrudate shape and expansion, flake thickness after the hydraulic rollers, roasting surface quality, and coating adhesion if a glazed variant is specified. These results confirm the line produces your target product before it leaves the factory.