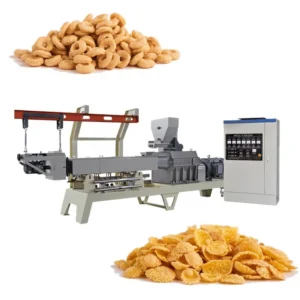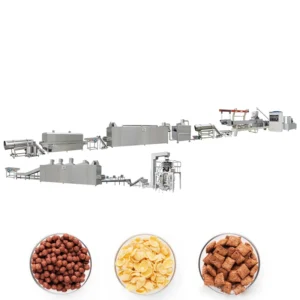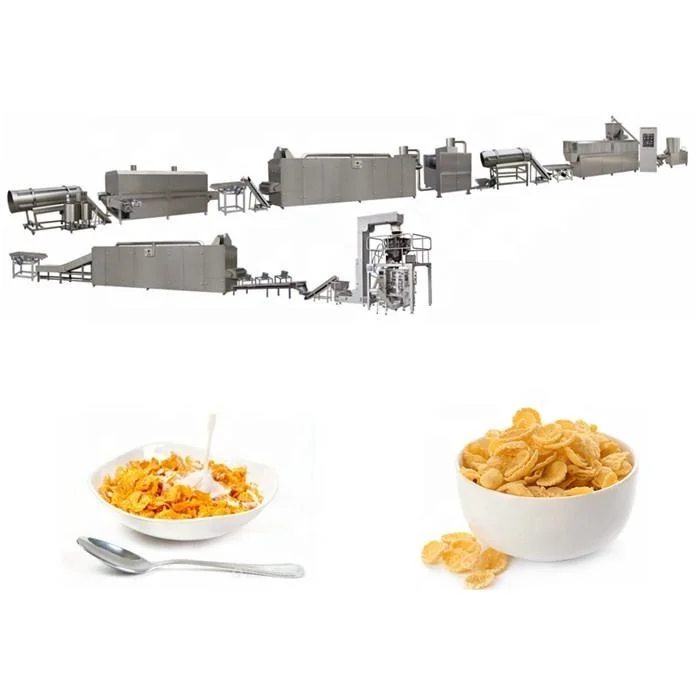
Screw Configuration Matched to Your Formulation — Barrel profiles and die geometries are specified against the buyer’s actual corn, oat, or barley recipe before the MT-75 leaves the testing workshop, ensuring expansion and density targets are met on the production floor.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-75 Twin Screw Extruder |
| Product Type | Breakfast Cereal Corn Flakes Production Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material / moisture content) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC and MCC control |
| Basic Raw Materials | Corn, rice, wheat, oat, barley powder |
| Dryer Heating Source | Gas / Electric |
| Shape Options | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (via die/mould change) |
| Standards | CE (certified since 2014); ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural Corn Flakes | Corn grits processed through mixing, extruding, flaking, drying, hot air roasting, cooling, and packing |
| Sugar-Coated Corn Flakes | Corn or rice base with sugar spraying, coating drum application, and secondary drying before packing |
| Shaped Breakfast Cereals | Wheat, oat, or barley powder formed into rings, balls, fruit loops, or stars via interchangeable die plates |
| Multi-Grain Flake Production | Blended grain formulations requiring adjusted barrel temperature profiles and screw pitch configurations |
Why "Nominal Capacity" Misses the Real Picture on Extruded Cereal Lines
A breakfast cereal corn flakes extrusion production line specifications sheet means little if the capacity rating was never tested on your actual flour blend.
I have watched buyers commit to a line based on a brochure number, only to find the extruder chokes when they switch from standard corn grits to a high-fiber oat mix. The moisture absorption rate changes, the starch gelatinisation window shifts, and the throughput drops to half the promised volume [NEED_CITE: throughput variance across grain formulations in twin-screw extrusion]. The line then bottlenecks at the extruder while the dryer and flaking rollers sit idle, burning energy for no output.
Barrel Temperature Profiling and Starch Gelatinisation Control
Twin-screw extrusion depends on precise thermal zones along the barrel to manage how starch molecules absorb moisture and expand under pressure. The breakfast cereal corn flakes extrusion production line specifications define multiple heating zones, each independently managed through the PLC interface. When the raw material shifts from corn to a wheat-barley blend, the gelatinisation temperature changes, requiring a revised thermal profile to maintain consistent dough viscosity before the die plate.
Die Geometry and Its Effect on Flake Expansion
The shape and aperture of the die directly determine how the extrudate expands upon exiting the barrel. For corn flakes, a flat, wide die produces a ribbon that the hydraulic double-roller flaking unit then compresses to the target thickness. Infrared sensors on the flaking machinery monitor roller surface temperature to prevent sticking or uneven compression, which would otherwise create flakes that shatter during hot air roasting rather than developing the expected crispness [NEED_CITE: die design influence on extrudate expansion in cereal processing].
Hydraulic Flaking and Roasting Dynamics Explained
The installed power of 210 kW on the MT-75 drives both the twin-screw mechanism and the upstream mixing conveyance, but the flaking station operates on a separate hydraulic circuit with dual motors driving each roller independently. This separation allows operators to adjust roller gap and pressure without altering extruder speed. Downstream, the hot air roasting oven uses a vibrating pan with high-temperature spraying tubes and separate circulating fans to develop surface bubbling — a visual and textural marker that consumers associate with properly roasted corn flakes. The cyclone dust removal device captures fine particulate generated during roasting, keeping the production environment within acceptable air quality thresholds.
When Extruder Output Exceeds Downstream Capacity
A frequent failure pattern occurs when the extruder is specified at a higher throughput than the dryer or roasting oven can handle. Wet flakes pile up at the dryer infeed, moisture remains trapped inside the flake body, and the final product reaches the packing station with a water activity level that invites mould growth during storage [NEED_CITE: moisture migration and shelf stability in breakfast cereal manufacturing]. The buyer then blames the extruder for a problem that originated in throughput mismatch between stations.
Why Procurement Starts with a Material Trial
Every grain formulation behaves differently under shear and heat inside a twin-screw barrel. Our testing workshop runs the buyer’s actual raw material — whether it is a standard corn grit or an oat-fortified blend — through the MT-75 before the line ships. The screw configuration record and die selection are then locked to that specific recipe, and the trial run report documents barrel temperatures, screw speed, moisture addition rate, and the resulting flake density. This is also where voltage, frequency, and control language are confirmed against the buyer’s facility requirements, so the PLC screens read in the correct language on day one of commissioning.
Documentation & Verification
- Screw and die configuration record matched to your grain formulation and target flake density
- Trial run report on your raw material documenting barrel temperatures and expansion behaviour
- Electrical schematic with voltage and frequency confirmed to your facility specification
- Line layout showing throughput matching between extruder, flaking unit, dryer, and roasting oven
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Wear parts list covering screw segments, die plates, and flaking roller surfaces
Installation, Commissioning & Support
- Foundation pad sized to the 45 × 1.5 × 3.5 m line footprint with vibration isolation for the extruder and flaking unit
- Dedicated power circuit rated for 210 kW installed capacity with voltage confirmed before cable termination
- PLC and MCC panels configured to local frequency and operator language before arrival on site
- First-run commissioning includes barrel temperature profiling and screw speed adjustment on your grain blend
- Operator training covers die changeover for shape variants and hydraulic roller gap calibration
- Spare screw segments and die plates shipped with the initial order to cover the first replacement cycle
What to Include in Your Inquiry
To configure the breakfast cereal corn flakes extrusion production line specifications correctly, share your target raw material blend, the flake thickness or shape you intend to produce, and the daily output volume your market requires. Confirm your facility voltage and frequency, as well as the preferred control language for the PLC interface. If you have existing upstream mixing or downstream packing equipment, provide the model and throughput so the line can be matched end to end.
Frequently Asked Questions
Q: How is output capacity verified on my actual raw material rather than a nominal rating?
A: We run your specific grain formulation through the MT-75 in our testing workshop before shipment. The trial run report records barrel temperatures, screw speed, moisture addition, and the resulting flake density. Capacity figures are then confirmed against your actual recipe, not a generic corn grit baseline.
Q: How are screw configuration and die design specified for my corn flake formulation?
A: Screw element arrangement and die aperture are selected based on your raw material’s starch content, fiber ratio, and target flake density. The configuration record is documented and shipped with the machine so your team can replicate the setup during future production runs.
Q: What voltage, frequency, and control language options are confirmed before production?
A: Electrical specifications are locked during the quotation stage based on your facility data. The PLC interface and MCC panel are configured to your local voltage and preferred operator language before the line enters final assembly, avoiding commissioning delays.
Q: How are downstream station capacities matched to the extruder to prevent bottlenecks?
A: Dryer surface area, flaking roller width, and roasting oven throughput are all calculated against the extruder’s verified output on your material. This ensures wet flakes do not accumulate between stations, maintaining consistent moisture removal and flake texture throughout the line.