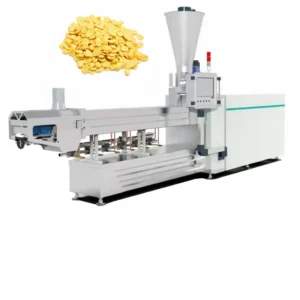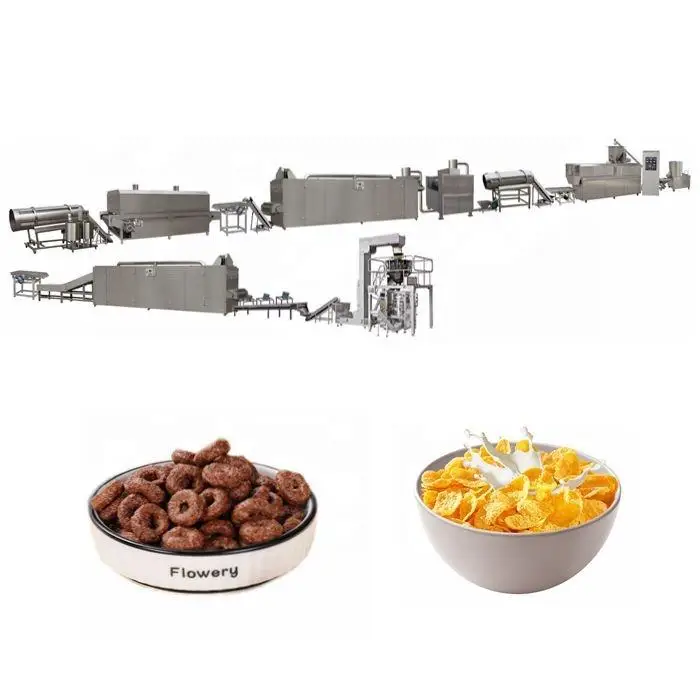
Screw Configuration Matched to Your Cereal Blend — MT75 twin-screw setup is specified to the buyer’s actual corn, rice, or multi-grain raw material and target flake density, verified through in-house trial runs before shipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/h (basis not stated in source — confirm raw material / moisture) |
| Extruder Standalone Capacity | 200–300 kg/h (basis to be confirmed) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC (flaking machinery); line-wide MCC / PLC control |
| Heating Source (Dryer) | Gas / Electric |
| Flaking Machinery Drive | Double motors for separate roller driving; hydraulic system for double rollers |
| Flaking Temperature Control | Infrared sensor for even temperature pipe control |
| Roasting Oven | Hot air roasting with vibrating pan, high temperature spraying tubes, conciliation burner, two circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Screw Feature | Automatic lubricating, cooling function |
| Assembly State | Complete production line |
| Standards | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flake production | Corn grits and corn flour blends |
| Sugar-coated breakfast cereals | Corn, rice, wheat, oat, barley powder with sugar or honey coating |
| Multi-grain flake formats | Blends of rice, wheat, oat, and barley with corn base |
| Shaped cereal production | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart shapes via die change |
Why the Wrong Barrel Profile Ruins Flake Crispness Before It Reaches the Oven
Corn flakes live or die in the extruder barrel — starch gelatinisation must be complete and uniform before the dough ever touches the flaking rollers.
A generic barrel temperature profile assumes a standard corn grit with predictable protein and starch ratios. When the actual raw material arrives at the factory floor with lower protein content or different moisture behaviour, the gelatinisation window shifts. Flakes come out of the roasting oven soft, chewy, or unevenly blistered. I once watched a line produce perfect flakes during a factory trial using standard corn flour, only for the same setup to generate sticky, under-expanded sheets when the buyer switched to a locally sourced corn variety with different gelatinisation characteristics [NEED_CITE: starch gelatinisation temperature variation across corn varieties]. The corn flakes extrusion production line technology requires screw and barrel settings that respond to what you actually mill, not what a catalogue assumes.
Starch Gelatinisation Through Shear and Moisture Control
The twin-screw extrusion stage determines whether the cereal dough achieves full starch gelatinisation without over-shearing the matrix. Screw configuration — the arrangement of conveying, kneading, and reverse elements — is selected based on the specific cereal blend and the target flake density. Corn grits demand a different shear profile than an oat-heavy multi-grain mix, because each grain’s starch granule size and gelatinisation onset temperature differ. The corn flakes extrusion production line technology hinges on matching screw element sequencing to these material-specific thresholds so that expansion remains controlled and predictable.
Barrel Temperature Zones and Expansion Behaviour
Multiple independent heating zones along the barrel allow the process engineer to build a temperature gradient that guides the dough through preconditioning, cooking, and metering stages before it exits the die. Too steep a gradient causes premature expansion and surface tearing; too flat a profile leaves the centre undercooked. The die aperture works in concert with the final barrel zone — a smaller die opening increases back-pressure and shear, which influences how the extrudate behaves when it hits the flaking rollers. Getting this relationship right is what produces the surface bubbling and internal structure that consumers associate with a quality corn flake [NEED_CITE: twin-screw extrusion die design principles for breakfast cereal applications].
Power, Throughput, and What the Numbers Actually Mean
The MT75 carries an installed power rating of 210 kW with operating consumption around 150 kW, driving a twin-screw assembly designed for continuous cereal dough processing. The listed output capacity of 300–500 kg/h carries an important caveat: actual throughput depends on the raw material formulation, moisture content at the feed point, and the degree of cook required for the target flake texture. The extruder’s standalone capacity is noted separately at 200–300 kg/h, which reflects the screw throughput before downstream flaking, drying, and roasting stages impose their own rate limits. Line-wide MCC and PLC control ensures that extruder speed, feeder rate, and barrel temperatures remain synchronised — a mismatch at any point introduces density variation that compounds through the roasting oven.
The Cost of Skipping a Pre-Shipment Trial
When an extruder ships without a trial run on the buyer’s actual cereal blend, the first production day becomes an expensive experiment. Screw combinations that work on the manufacturer’s test material may produce the wrong expansion ratio on the buyer’s locally sourced grain. Flakes that are too dense fail to crisp in the roasting oven; flakes that over-expand shatter under the flaking rollers and generate excessive breakage through the coating drum. The result is days of line downtime while technicians swap screw elements and adjust barrel zones — time that could have been spent in the testing workshop before the machine ever left the factory [NEED_CITE: impact of raw material variability on extrusion line commissioning time].
Why the Extrusion Stage Defines the Entire Line
The MT75 is engineered as one station within a coordinated sequence — mixing, extruding, flaking, drying, hot air roasting, cooling, and packing — where throughput at each stage must align. Screw configuration and die design are specified to the buyer’s cereal formulation and target flake density, not pulled from a standard library. The in-house testing workshop runs trial batches on the buyer’s actual raw material before shipment, generating a trial run report that documents screw combination, barrel profile, and output characteristics. Line layout and capacity calculations are prepared to show how extruder throughput matches flaking roller speed, dryer residence time, and roasting oven capacity, so no single station becomes a bottleneck. The flaking machinery uses a hydraulic double-roller system with infrared temperature sensing to maintain uniform flake thickness, which only works if the extrudate arriving at the rollers has consistent density and moisture content.
Documentation & Verification
- Line layout and capacity calculation showing throughput balance across extrusion, flaking, drying, and roasting stations
- Screw and die configuration record documented to buyer’s specific cereal blend and target flake density
- Trial run report on customer’s actual raw material from the in-house testing workshop before dispatch
- Electrical schematic with voltage and frequency confirmation for the target market
- Operation and maintenance manual covering extruder, flaking machinery, roasting oven, and coating system
Installation, Commissioning & Support
- Overall line dimensions of 45 × 1.5 × 3.5 m require adequate floor space and headroom for the roasting oven exhaust and cyclone dust removal
- 210 kW installed power demands dedicated electrical circuits with voltage and frequency matched to local supply standards
- Twin-screw extruder ships with automatic lubricating and cooling system pre-assembled; barrel sections align on-site
- PLC and MCC control panels configured to buyer’s preferred operating language before commissioning begins
- Flaking machinery hydraulic system and infrared sensors calibrated during first production run with operator training
- Wear parts list provided for screws, die inserts, and flaking roller surfaces with recommended replacement intervals
What We Need to Specify Your Line
To configure the extrusion stage correctly, share your cereal formulation — the grain types, ratios, and typical moisture content of the raw material entering the mixer. Confirm your target flake density, bowl-life expectations, and whether the line will produce natural, sugar-coated, or both formats. Provide your local voltage, frequency, and preferred control language so that electrical schematics and PLC programming are finalised before production.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal raw materials and target flake densities?
A: Screw elements — conveying, kneading, and reverse sections — are arranged based on the specific grain blend’s starch gelatinisation temperature and the density required in the final flake. Corn-dominant formulations need a different shear profile than oat or barley-heavy mixes. The configuration is documented and verified through a trial run on your actual material before the extruder ships.
Q: What barrel temperature profile and moisture range are needed for proper starch gelatinisation?
A: The barrel is divided into independent heating zones that create a gradient from preconditioning through full cook. The exact temperature at each zone depends on your cereal blend’s gelatinisation onset and the moisture added at the mixer. These parameters are established during the pre-shipment trial and recorded in the configuration report provided with the line.
Q: How does die design affect expansion behaviour and downstream flaking quality?
A: Die aperture size and land length control back-pressure at the extruder exit, which directly influences how much the extrudate expands before reaching the flaking rollers. A die matched to the target flake thickness produces consistent sheet density, reducing breakage during flaking and ensuring even blistering in the roasting oven.
Q: Can a trial run be performed on our specific cereal blend before shipment?
A: Yes. The in-house testing workshop runs production trials using your actual raw material formulation. The trial run report documents screw combination, barrel temperature settings, expansion ratio, and output characteristics. This eliminates guesswork during on-site commissioning and confirms that the line produces your target flake specification.
Q: How is extruder throughput matched to flaking, roasting, and coating capacity?
A: A line layout and capacity calculation is prepared during the proposal stage, mapping extruder output against flaking roller speed, dryer residence time, roasting oven throughput, and coating drum capacity. Each station is sized so that no single point restricts the line, and the PLC control system synchronises feed rates across the entire sequence.