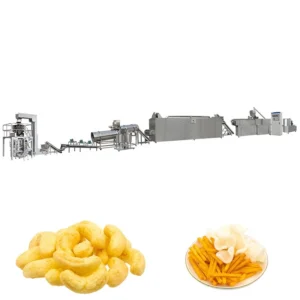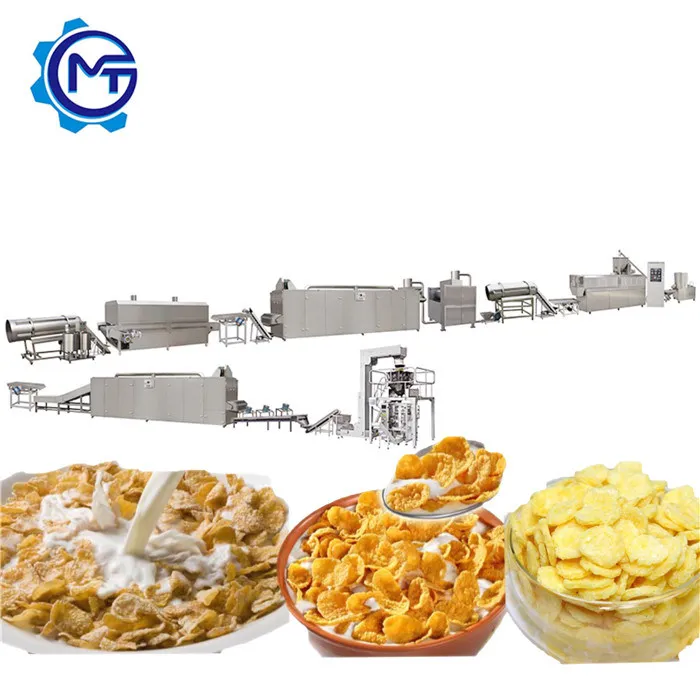
Twin-Screw Precision — screw configuration and die geometry matched to your raw material blend so flake density holds at full throughput instead of drifting off-spec.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Model | MT75 |
| Extruder Type | Twin-screw |
| Installed Power | 210 kW (MT75) |
| Power Consumption | 150 kW (MT75) |
| Output Capacity | 300–500 kg/hr (MT75; basis not stated in source) |
| Control System | PLC (flaking unit); full-line MCC/PLC integration |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Flaking Unit | Hydraulic double-roller, dual independent motors, infrared temperature sensor |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot-air circulation, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melter, elevator, coating drum, spraying nozzle |
| Line Stations | Mixing → Extruding → Flaking → Drying → Hot-air Roasting → Sugar Spraying → Sugar Coating → Drying → Cooling → Packing |
| Alternative Line | Natural line (omits sugar stages) |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Final Products | Natural corn flakes, sugar-coated corn flakes, shaped cereals (ball, tube, stick, ring, loop, star, wheel, flower, heart) |
| Assembly State | Complete turnkey line from batching to packing |
| Layout | Customizable to buyer’s factory dimensions |
| Certifications | CE; ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits with target moisture and flake thickness |
| Sugar-coated corn flakes | Corn base with sugar glaze coating for retail packs |
| Multi-grain breakfast flakes | Rice, wheat, oat, barley powder blends |
| Shaped cereal formats | Extruded loops, stars, rings, tubes from corn and grain mixes |
What Generic Screw Configurations Cost You at Scale
A copied screw profile might produce acceptable flakes at trial volume, but density and crispness drift once the line runs continuously.
I have watched a corn flakes extrusion technology production line stall for weeks because the supplier used a standard screw layout that worked for a different starch ratio. The extruder ran, the flaker pressed, but the final flakes came out too dense and refused to blister properly in the roasting oven. The buyer’s lab formulation had lower sugar content than the generic build expected, which changed how the dough expanded through the die and how the flakes behaved under hydraulic roller pressure [NEED_CITE: twin-screw extrusion screw profile selection for varying starch blends]. Retooling the screw elements and adjusting barrel temperature zones took longer than the original factory build.
Barrel Temperature Zones and Starch Gelatinisation
The corn flakes extrusion technology production line uses multiple independently controlled barrel heating zones along the twin-screw extruder. Each zone governs how quickly starch gelatinises inside the barrel before the dough exits through the die. If the profile runs too cool in the mid-section, the corn meal passes through under-gelatinised and the resulting flakes stay soft and resist proper toasting. If it runs too hot, the dough skins over and expansion becomes uneven across the die face.
Die Geometry and Flake Expansion Control
Die aperture size and land length determine how much the extrudate expands the moment it leaves the barrel. For traditional flat flakes, the die must produce a uniform ribbon that the hydraulic double-roller flaking unit can press to consistent thickness. Shaped formats like loops and stars require a different die plate entirely, with land lengths calculated for the specific geometry. Switching between flat flake dies and shaped cereal dies on the same MT75 platform lets producers serve multiple product categories without adding a second extruder [NEED_CITE: die land length calculation for expanded cereal products].
Hydraulic Flaking Pressure and Infrared Feedback
The flaking unit uses a hydraulic double-roller system with dual independent motors and an infrared temperature sensor. Roller pressure and gap determine final flake thickness, while the infrared sensor monitors dough temperature entering the nip. If the dough arrives too cool, it cracks under pressure instead of flattening; too hot and it sticks to the rollers. Consistent feedback from the sensor lets the PLC adjust roller speed and gap in real time, which matters when the line runs multi-grain blends that change thermal conductivity between batches.
Reading the Spec Sheet Against Your Formulation
The MT75 carries 210 kW installed power and draws around 150 kW during operation across the full 45-metre line. Those numbers matter less than how they distribute between extrusion, flaking, drying and roasting. A line where the extruder motor is oversized but the dryer burner is undersized will bottleneck at drying — the extruder pushes out material faster than the dryer can handle, and moisture content at the roaster inlet drifts above the target window. The roasting oven uses hot-air circulation with dual circulating fans and a cyclone dust removal system, which keeps temperature uniform across the vibrating pan and prevents fines from burning onto the heating tubes. For sugar-coated variants, the double tumble sugar melter and coating drum must also match throughput, or the coating stage becomes the constraint.
When Throughput Mismatch Hits the Roaster
If the flaking unit runs faster than the roasting oven can toast, flakes pile up on the vibrating pan and receive uneven heat exposure. The result is a mix of properly blistered flakes alongside pale, under-roasted ones that go stale within days. I have seen operators try to compensate by raising oven temperature, which scorches the outer layer while the core stays moist. The cyclone dust removal then pulls charred fines into the collection bin — a sign the process is running outside its design window rather than a maintenance issue [NEED_CITE: cereal roasting temperature uniformity and product shelf life].
Why This Line Is Built Around Extrusion Parameters
Every station on this corn flakes extrusion technology production line is specified together rather than sourced independently. The twin-screw extruder screw configuration is documented to your raw material blend, and the die design is matched to your target flake or shape. The flaking unit, dryer, roaster and coating system are all capacity-matched so no single station becomes the constraint at the throughput you need. Before shipment, your actual raw material runs through our in-house testing workshop, producing a trial run report that records screw profile, barrel temperatures, flake thickness and roasting curve — the same parameters your operators will use on day one. Electrical schematics confirm voltage and frequency against your site supply before the control panels are wired, avoiding commissioning delays caused by mismatched motor ratings or PLC language settings.
Documentation & Verification
- Screw and die configuration record matched to your grain blend and target flake density
- Trial run report from in-house testing workshop on your actual raw material
- Line layout drawing with throughput matching across extruder, flaker, dryer and roaster
- Electrical schematic with voltage, frequency and control language confirmed to your site
- CE declaration of conformity and ISO certificate for the complete line
Installation, Commissioning & Support
- Foundation plan based on the 45 × 1.5 × 3.5 m line footprint and local floor load rating
- Dedicated power circuit sized for 210 kW installed capacity with confirmed voltage and frequency
- Modular station assembly with mechanical and electrical connections completed on site
- Initial run with your raw material to verify screw profile and barrel temperature settings
- Operator training covering PLC interface, flaking unit gap adjustment and roaster fan balance
- Wear parts list for screws, dies and roller surfaces with recommended replacement intervals
What We Need to Configure Your Line
To size the extruder, flaking unit and roaster correctly, share your grain formulation, moisture content at the mixer outlet, and target flake thickness or shaped format. Confirm your site voltage, frequency and preferred control language. If you plan to run both natural and sugar-coated variants, specify the sugar coating percentage so the coating drum and tumble melter are matched to the same throughput as the extruder.
Frequently Asked Questions
Q: How is screw configuration and die design selected for a specific raw material blend and target flake density?
A: We test your actual grain blend in the in-house testing workshop, recording expansion ratio at different barrel temperature profiles and screw element arrangements. The screw configuration that holds your target density at full throughput is then documented and built into the production extruder, not copied from a generic template.
Q: What trial runs are performed on the buyer’s actual raw material before shipment?
A: Your grain blend runs through the test extruder and flaking unit under production-equivalent conditions. The trial report records screw profile, barrel zone temperatures, die geometry, flake thickness measurements and roasting curve data, which becomes the baseline parameter set for your operators at commissioning.
Q: How is throughput matched between the extruder, flaker, dryer, roaster and coater?
A: Each station is specified during the layout phase so its maximum capacity exceeds the extruder output by a defined margin. The line layout document shows calculated throughput at every stage, confirming that drying and roasting can handle peak extruder output without material backlog.
Q: What barrel temperature profile and moisture parameters are set for natural versus sugar-coated corn flakes?
A: Natural flakes typically need a slightly higher barrel exit temperature to achieve full gelatinisation before the roasting stage, while sugar-coated variants run a cooler profile since the sugar coating and second drying pass add thermal load. Both profiles are established during the trial run on your material.
Q: How are voltage, frequency and control language confirmed before commissioning?
A: The electrical schematic is reviewed with the buyer during the specification stage, and motor ratings, transformer sizing and PLC language are locked before the control panels are assembled. This prevents on-site rewiring and programming delays during installation.