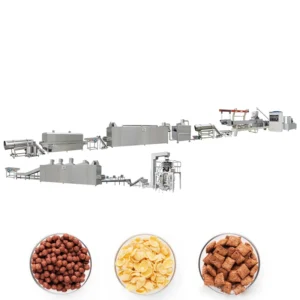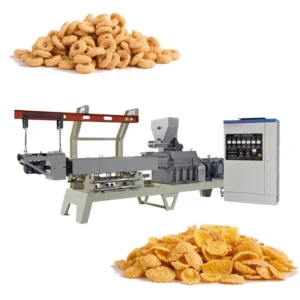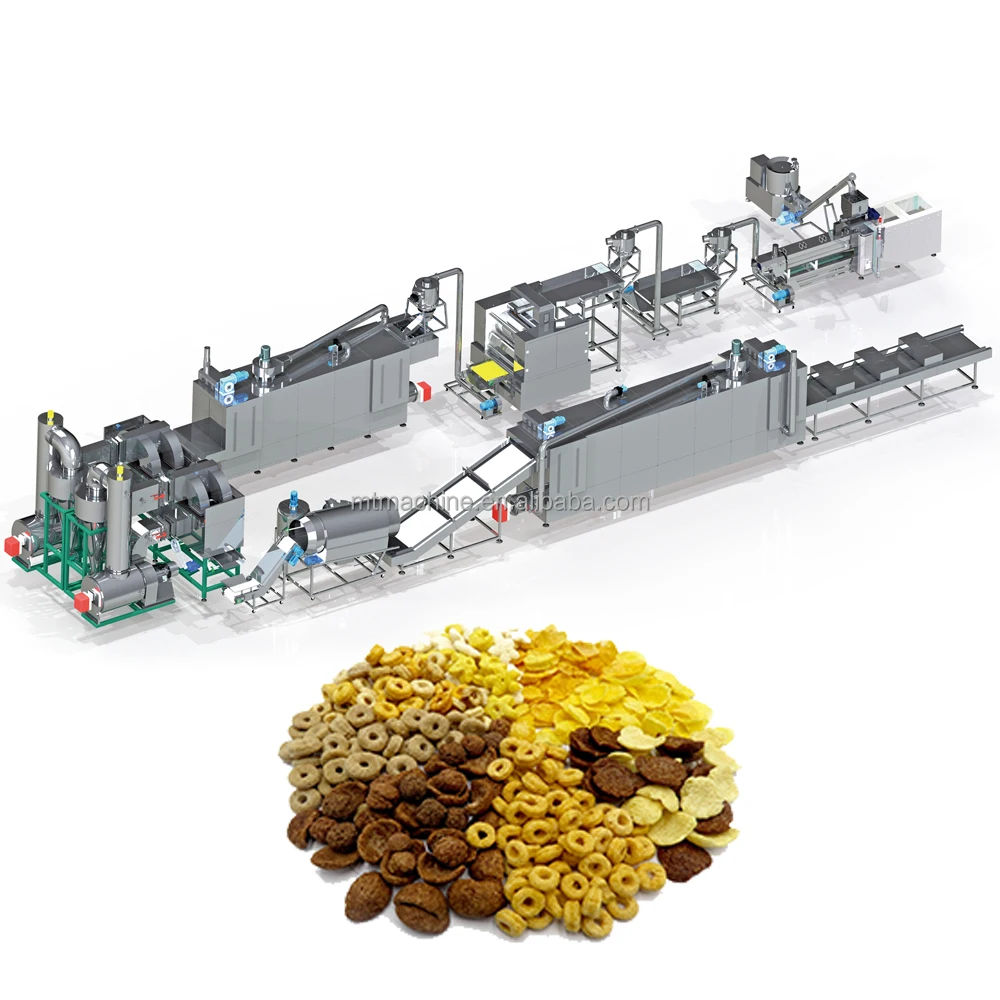
Custom Extrusion Geometry — Screw pitch and barrel zone mapping are matched to your corn blend and target flake density before production starts.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT75 / MT85 |
| Product Type | Corn Flakes and Breakfast Cereal Production Line |
| Extruder Type | Twin Screw |
| Installed Power | 160 kW (MT70) / 190 kW (MT85) / 210 kW (MT75) |
| Power Consumption | 120 kW (MT70) / 140 kW (MT85) / 150 kW (MT75) |
| Output Capacity | 150–200 kg/h (MT70) / 300–400 kg/h (MT85) / 300–500 kg/h (MT75) (basis not stated in source — confirm raw material type, moisture content, flake thickness) |
| Overall Dimensions | 41 × 1.5 × 2.2 m (MT70) / 43 × 1.5 × 3.2 m (MT85) / 45 × 1.5 × 3.5 m (MT75) |
| Control System | PLC control (flaking machinery); MCC and PLC (line level) |
| Flaking Machinery | Hydraulic double-roller system, double motors for separate roller driving, infrared sensor temperature control |
| Dryer Heating Source | Gas / Electric |
| Roasting Oven | Hot air roasting with conciliation burner, two circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn grits, milled corn flour |
| Sugar-coated corn flakes | Corn base with sucrose or glucose coating |
| Multi-grain breakfast flakes | Blends of rice, wheat, oat, and barley powder |
| Shaped breakfast cereals | Rings, balls, stars, tubes, and fruit loops via die variation |
What "Nominal Throughput" Leaves Out When Starch Gelatinisation Is Uncontrolled
Throughput figures are meaningless if the screw profile cannot hold stable gelatinisation on your actual grain blend.
A line rated at a specific hourly output often drops to a fraction of that rate once the buyer introduces a raw material with a different fat or fiber ratio. When the barrel temperature profile is copied from a generic build instead of mapped to the specific corn or oat blend, the starch granules either rupture too early or pass through under-cooked. The result reaches the flaking rollers with inconsistent moisture and hardness, producing cracked or uneven flakes that fail the bowl test. [NEED_CITE: starch gelatinisation temperature ranges for cereal grains] The correct corn flakes extrusion technology requires matching the screw compression ratio to the raw material’s gelatinisation window so that expansion and density remain within specification across every production run.
Barrel Temperature Profiling and Shear Control
The twin-screw configuration allows independent adjustment of shear and residence time across each barrel zone. For corn flakes and breakfast cereals, the feed section must keep the material below gelatinisation temperature while the compression and metering zones apply the precise thermal and mechanical energy needed to cook the starch fully. Adjusting screw element spacing and pitch along the barrel length controls how much mechanical shear supplements external heating, preventing both under-processed centers and over-processed surface scorching.
Die Geometry and Flake Density
The die plate determines the shape, size, and initial density of the extruded rope before it reaches the flaking rollers. For natural corn flakes, a narrow slit die produces a continuous sheet that the rollers flatten to the target thickness. For shaped breakfast cereal twin screw extrusion products such as rings or stars, interchangeable die inserts and a rotating face cutter define the final geometry. Selecting the right die aperture relative to the screw discharge pressure ensures the extrudate holds its form without collapsing or over-expanding before flaking or cutting. [NEED_CITE: die swell ratio and extrudate density relationship]
Reading the Specification Sheet for Process Impact
The installed power ranging from 160 kW to 210 kW across the three models directly determines the available thermal and mechanical energy inside the barrel, which sets the upper limit for starch conversion at a given throughput. The hydraulic double-roller flaking system with infrared sensor temperature control addresses a common failure point — if the roller surface temperature drifts, the flake sticks or shatters regardless of how well the extruder performed upstream. Power consumption figures of 120 kW to 150 kW reflect the running load under typical operating conditions, which is what determines the transformer sizing and circuit requirements at the installation site. The PLC control across the flaking station and MCC at the line level allows operators to lock in barrel temperature profiles and roller gap settings, maintaining batch-to-batch consistency once the correct parameters are established for a given raw material.
The Hidden Cost of Mismatched Drying and Extrusion Capacity
When the dryer or roasting oven is sized to a nominal line output but the extruder cannot sustain that rate on the buyer’s specific grain blend, the material spends too long in the drying tunnel or too little time in the roasting chamber. Over-dried flakes lose their characteristic surface blistering and become brittle, while under-roasted flakes retain internal moisture that causes sogginess within minutes of contact with milk. [NEED_CITE: moisture content targets for shelf-stable breakfast cereals] This mismatch is often invisible during a factory test using the manufacturer’s standard raw material and only surfaces after installation when the buyer switches to their local supply.
Why This Configuration Approach Differs
The screw configuration and die design are specified to the buyer’s raw material and target flake density rather than pulled from a standard library. An in-house testing workshop runs trial production on the customer’s actual grain blend before shipment, generating a trial run report that documents the barrel temperature profile, moisture levels, and flake thickness achieved. Throughput matching across the extruder, flaker, dryer, and roaster is calculated during the line layout phase so that no single station bottlenecks the line or leaves material waiting. Electrical schematics and voltage confirmation are prepared for the target market’s power grid before production begins, preventing commissioning delays caused by transformer or motor incompatibility.
Documentation & Verification
- Line layout drawing with throughput calculation across each station matched to your cereal blend
- Screw and die configuration record documenting element profile selected for your raw material
- Trial run report on your grain blend produced in the testing workshop before shipment
- Electrical schematic with voltage and frequency confirmed for your local grid
- Factory test record showing flake thickness and moisture readings at discharge
- Operation and maintenance manual with wear parts list for screws, dies, and rollers
Installation, Commissioning & Support
- Foundation plan reflecting overall line dimensions up to 45 m length and 3.5 m height
- Power supply specification based on installed power up to 210 kW with dedicated circuit requirements
- MCC and PLC control system configured to operator language before on-site commissioning
- Roller gap calibration and infrared sensor verification during first production run
- Screw and die wear parts list provided with recommended replacement intervals
- Gas or electric dryer heating source connected and balanced with extruder discharge rate
Preparing Your Line Specification Inquiry
To configure the screw profile and die geometry accurately, provide the specific grain blend composition, target flake thickness, and desired bowl-life characteristics. Include your facility’s available floor space and ceiling height to determine which model’s footprint fits the production area. Confirming local voltage, frequency, and preferred control language at this stage prevents rework during commissioning.
Frequently Asked Questions
Q: How is screw configuration selected for different cereal raw materials?
A: The screw element sequence is designed around the gelatinisation temperature and moisture absorption rate of the specific grain blend. Corn, oat, wheat, and rice each require different compression ratios and residence times. The configuration record documents every element position and is validated during a trial run on your raw material before the extruder ships.
Q: What barrel temperature profile produces correct starch gelatinisation for corn flakes?
A: The profile typically stages heat from the feed zone through the metering zone, keeping the material below gelatinisation initially and then applying controlled shear and heat in the compression sections. Exact zone temperatures depend on the corn variety and moisture content, which are confirmed during the pre-shipment trial run on your grain supply.
Q: How is flake thickness controlled during the flaking stage?
A: The hydraulic double-roller system maintains consistent pressure while double motors drive each roller independently. An infrared sensor monitors roller surface temperature in real time. The gap setting is adjusted through the PLC control to hold the target flake thickness throughout the production run.
Q: Can the same extrusion platform produce shaped cereals and flat flakes?
A: The twin-screw extruder accommodates different die inserts and cutting mechanisms. A slit die produces continuous sheets for flaking, while shaped dies paired with a rotating face cutter produce rings, balls, stars, or tubes. The screw configuration is adjusted for each product format to maintain correct expansion and density.
Q: How is roasting temperature set to achieve blistering without over-drying?
A: The hot air roasting oven uses a conciliation burner with two circulating fans to distribute heat evenly. Temperature and residence time are calibrated to the flake’s moisture content entering the oven. The cyclone dust removal device keeps the air stream clean, preventing particle buildup that could cause uneven roasting across the tray surface.