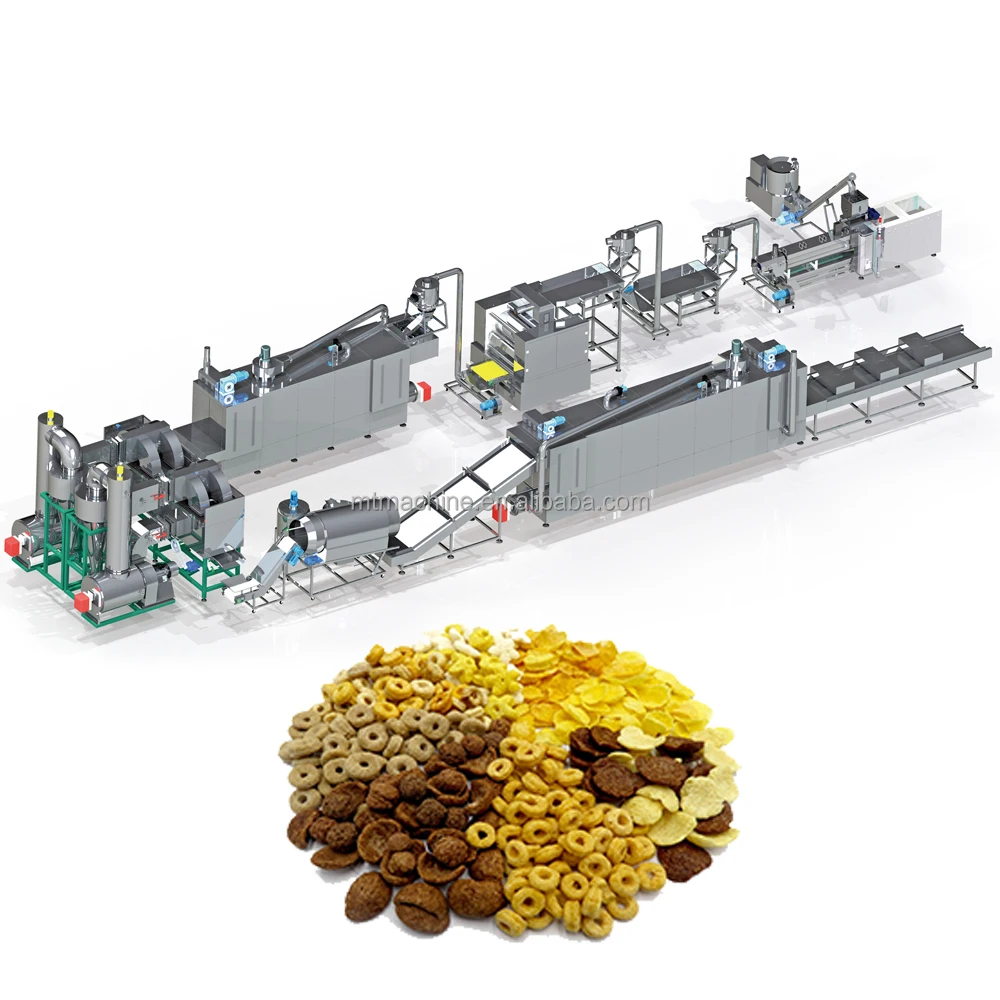
Screw Configuration Matched to Your Grain — die geometry, barrel profile, and flaking roller gap set on your actual raw material during in-house trial runs, not copied from generic builds.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Breakfast Cereal Production Line |
| Extruder Model | MT-75 Twin Screw Extruder |
| Screw Type | Twin-screw with automatic lubricating and cooling |
| Output Capacity | 200-300 kg/hr (basis not stated in source — confirm raw material / moisture content) |
| Voltage & Frequency | 220V / 380V (frequency configurable to site requirement) |
| Rated Power | 3 kW (verify against full line total power) |
| Flaking Station | Hydraulic double-roller system, dual-motor separate drive, infrared sensor temperature pipe control |
| Roasting Oven | Hot air roasting, high-temperature spraying tubes, conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle array |
| Dryer Heating Source | Gas or Electric (selectable) |
| Process Flow (Natural) | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Cooling → Packing |
| Process Flow (Sugar-Coated) | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Sugar Spraying → Sugar Coating → Drying → Cooling → Packing |
| Control System | PLC at flaking station; MCC/PLC line-level control |
| Assembly State | Complete line from batching through packing |
| Standards | CE certified, ISO certified |
| Warranty | 1 Year (1 Year on Gearbox core component) |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn grits, milled corn, or corn-rice blends at controlled moisture |
| Sugar-coated corn flakes | Same base grains with sugar slurry or honey coating application |
| Multi-grain breakfast cereals | Wheat, oat, rice, barley, or mixed-grain formulations |
| Fortified cereal production | Grain blends with added vitamin and mineral premixes |
| Puffed snack shapes | Alternative die configurations on the same extrusion platform |
What Your Corn Flakes Extrusion Production Line Specifications Must Account For Before Shipment
The extrusion parameters that work on standard corn grits will fail on a whole-wheat or multi-grain blend.
When I was commissioning a corn flakes line overseas, the buyer had quoted everything based on standard corn meal. Their actual production mix included a high-fibre whole-wheat component with a different moisture absorption profile. The flaking rollers produced uneven thickness, the roasting oven blistered the surface inconsistently, and the final crunch was off-spec. We spent four days on-site re-tuning screw speed, barrel temperature zones, and roller gap before the line held stable output [NEED_CITE: moisture and starch variability across grain types in extrusion processing]. The corn flakes extrusion production line specifications you evaluate must therefore be tied to the exact grain formulation you intend to run — not a generic datasheet figure.
Barrel Temperature Profile and Starch Gelatinisation
The MT-75 twin-screw extruder uses automatic lubricating and cooling across the barrel sections to maintain a stable temperature gradient. This matters because corn flakes require partial gelatinisation of starch inside the barrel — enough to bind the dough, but not so much that the extrudate expands fully before it reaches the flaking rollers. If the corn flakes extrusion production line specifications do not specify barrel zone temperatures matched to your grain’s gelatinisation onset point, the extrudate arrives at the flaking station either too stiff or too puffy, and neither condition produces an acceptable flake.
Flaking Roller Precision and Surface Quality
The hydraulic double-roller system on the flaking station runs separate dual motors so each roller can be driven independently, reducing drag-induced surface tearing. Infrared sensor temperature control on the roller body prevents condensation buildup that would otherwise stick dough to the roller surface. Achieving the target flake thickness — typically under one millimetre for a crisp corn flake — depends entirely on consistent roller gap and surface temperature across the full roller width [NEED_CITE: flaking roller gap tolerance and flake thickness uniformity in cereal processing].
Hot Air Roasting and Surface Blistering Control
The roasting oven uses high-temperature spraying tubes with a conciliation burner and two separate circulating fans to direct hot air uniformly across the flake bed. Cyclone dust removal captures fines generated during roasting so they do not recirculate and scorch. This stage creates the characteristic surface blistering and final moisture reduction that defines corn flake crispness. The corn flakes extrusion production line specifications should state the roasting temperature range and residence time, because both must be tuned to the flake thickness produced upstream.
Interpreting the Core Parameters for Cereal Production
The twin-screw design over a single-screw extruder matters directly for multi-grain cereal work. Twin screws provide positive conveying and self-wiping action, which prevents high-fibre materials like oat or barley from accumulating dead zones inside the barrel. The screw construction uses wear-resistant materials and special technology to extend service intervals when processing abrasive grain blends. At the line level, throughput matching between extruder output and downstream flaking, drying, and roasting capacity is essential — an extruder producing faster than the roasting oven can handle creates a backlog that cools the flakes before they enter the oven, destroying blister consistency. The PLC control at the flaking station, combined with MCC/PLC line-level control, allows each section’s speed and temperature to be coordinated from a single interface so that a change at the extruder propagates correctly downstream.
The Hidden Cost of Generic Screw and Die Builds
A screw configuration lifted from a standard corn grits setup and applied to a wheat-oat blend will produce extrudate with the wrong density and moisture distribution. Downstream, the flaking station cannot compensate — thin spots crack during roasting while thick spots remain doughy. I have watched production runs yield unsaleable product for days because the screw profile was never validated against the buyer’s actual raw material before the machine left the factory [NEED_CITE: screw configuration impact on extrudate density and texture]. That rework cost far exceeds the time required for a pre-shipment trial run.
Why Source This Line Here
Every station on this corn flakes line — mixing, extrusion, flaking, drying, roasting, coating, cooling, packing — is supplied as one matched system rather than assembled from separate vendors, which eliminates throughput mismatches. The screw configuration and die design are specified to the buyer’s raw material formulation and target flake density, not selected from a catalogue of generic builds. An in-house machine testing workshop runs trial production on the buyer’s shipped raw material before the line is approved for dispatch. PLC and MCC control architecture covers the full process, including the sugar coating variant with its double tumble melting and spray nozzle array. Pre-sales engineering consultation through on-site installation, commissioning, and operator training is provided as a continuous engagement, not a handoff at the factory gate.
Documentation & Verification
- Line layout and capacity calculation matching extruder output to roasting oven throughput
- Screw and die configuration record tied to your grain blend and target flake thickness
- Electrical schematic with voltage, frequency, and PLC language confirmation before build
- Trial run report on your shipped raw material from the in-house testing workshop
- Factory test record covering full process flow from mixing through packing
- CE declaration of conformity and ISO certificate included with shipment documentation
Installation, Commissioning & Support
- Foundation and floor space planning based on the full line footprint including roasting oven and cooling conveyor
- Dedicated electrical circuit sizing for the 220V/380V supply and confirmed frequency requirement
- Complete line arrives in sectional assemblies for staged installation across mixing, extrusion, flaking, and roasting stations
- First-run commissioning includes barrel temperature profiling and roller gap calibration on your production material
- Operator training covers PLC interface navigation, screw speed adjustment, and sugar coating drum operation
- Wear parts list covering screws, dies, and flaking roller surfaces with recommended replacement intervals
What to Include in Your Inquiry
Provide your target grain formulation — whether straight corn grits, a corn-rice blend, or a multi-grain mix with wheat or oat — along with the moisture content you plan to feed into the extruder. Specify your local voltage and frequency standard, the PLC interface language your operators require, and whether you need the natural process flow or the sugar-coated variant. If you can ship a sample of your production raw material, the testing workshop will run it before the line configuration is finalised.
Frequently Asked Questions
Q: How is output capacity verified against my specific raw material blend?
A: Capacity is confirmed through a trial run in the in-house testing workshop using your shipped raw material. The extruder screw speed, barrel temperature, and moisture addition are adjusted until stable output is achieved, and the result is documented in a trial run report before the line is cleared for production and shipment.
Q: How are screw configuration and die design selected for multi-grain formulations?
A: Each grain type has a different starch gelatinisation temperature and fibre content. The screw element arrangement and die geometry are configured based on your specific blend to achieve the correct extrudate density and surface quality needed for downstream flaking, rather than applying a single standard build across all materials.
Q: What barrel temperature and moisture range are needed before flaking?
A: Partial starch gelatinisation is required — the extrudate must be cohesive enough to hold together through the flaking rollers but not fully expanded. Barrel zone temperatures and moisture addition are set during the trial run to match your grain’s gelatinisation onset, and these parameters are recorded in the configuration documentation.
Q: How are flaking roller gap and roasting temperature coordinated?
A: Flake thickness from the hydraulic double-roller station directly determines the roasting oven temperature and residence time needed for proper surface blistering and final moisture reduction. Both parameters are tuned together during commissioning so that the roasting profile matches the exact flake geometry your line produces.
Q: How is voltage, frequency, and control language confirmed before shipment?
A: Electrical specifications including voltage, frequency, and PLC interface language are documented in the electrical schematic and confirmed with the buyer before the control panels are built. This prevents commissioning delays caused by incompatible power supply or unintelligible operator screens at the installation site [NEED_CITE: voltage and frequency standards by export market].